Help needed to get my 7i76E + 7i85S + 7i73 on my mill going.

More
8 years 1 month ago #117214 by tecno
Compiles but will not install
Code:
bengt@CombiMll ~/linuxcnc/configs/GB_2speed $ sudo halcompile --install GB_2speed.comp Compiling realtime GB_2speed.c GB_2speed.comp: In function ‘_’: GB_2speed.comp:25:23: error: expected identifier or ‘(’ before ‘double’ GB_2speed.comp:38:20: error: ‘motor_max_speed’ undeclared (first use in this function) GB_2speed.comp:38:20: note: each undeclared identifier is reported only once for each function it appears in /usr/share/linuxcnc/Makefile.modinc:113: receptet för målet ”GB_2speed.o” misslyckades make: *** [GB_2speed.o] Fel 1

Please Log in or Create an account to join the conversation.
More
8 years 1 month ago #117216 by tecno
FUNCTION(_){
int actual, message, motor_max_speed;

deleted word double and now it installs.

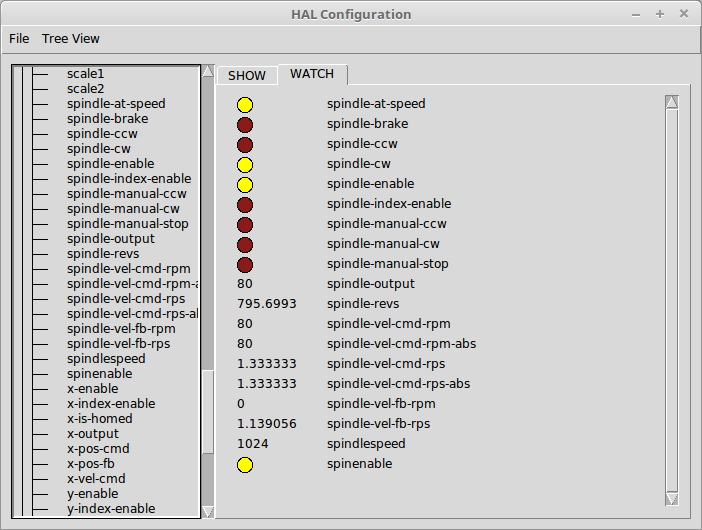
S80 now spinning at 63rpm

Please Log in or Create an account to join the conversation.

More
8 years 1 month ago - 8 years 1 month ago #117217 by tecno


I have no rpm fb only rps fb, that explaines why gmoccapy does not show rpm meter.


edit//
net spindle-vel-cmd-rpm-abs => gmoccapy.spindle_feedback_bar

Above line only gives numer correct but nothing on colored bar.
Last edit: 8 years 1 month ago by tecno. Reason: added text

Please Log in or Create an account to join the conversation.

More
8 years 1 month ago #117219 by tecno
I noticed one thing that must be addressed and that is to implement a delay before spindle to start.

If I command S80 and have the correct gear the spindle starts = OK
If I have wrong gear I get prompted to change gear but as soon as I get that gear close or near it starts to spin with the risk of damaging gears within the gearbox. It is in this situation a delay is a must.

How can this be done?

Please Log in or Create an account to join the conversation.

More
8 years 1 month ago #117240 by tecno
Changed value 1450 to 1875 = S80 is very close to 80rpm with a few tenths over.
if (motor_high)
motor_max_speed = 2500;
else
motor_max_speed = 1875;

But there is other problems, see picture below


Commanded S100
suggestion is wrong gear setting
No output to VFD when High-Gear is involved

Please Log in or Create an account to join the conversation.

More
8 years 1 month ago #117243 by tecno
Maybe this is the right medicine to get gear ranges in place?

// These need to be edited to suit the gearbox
int speeds[13] = {80, 125, 160, 215, 270, 360, 450, 595, 750, 1000, 1190, 1500, 2500};
int reqd_gear[13] = {0x01, 0x21, 0x02, 0x22, 0x04, 0x24, 0x08, 0x28, 0x10, 0x48, 0x68, 0x50, 0x70};

for (i = 0; spindle_speed_in > speeds && i < 12; i++);

Please Log in or Create an account to join the conversation.

Moderators: cmorley
Time to create page: 0.588 seconds
Powered by Kunena Forum
