
- Posts: 155
- Thank you received: 6
Gmoccapy - A new screen for linuxcnc
- DaOne
- Offline
- Premium Member
-

Less
More
12 years 11 months ago - 12 years 11 months ago #40718
by DaOne
Replied by DaOne on topic Gmoccapy - A new screen for linuxcnc
Norbert,
Here is a link to the image files I made for my screen set.
dl.dropboxusercontent.com/u/75606622/IPS_IMAGES.zip
Wes
Here is a link to the image files I made for my screen set.
dl.dropboxusercontent.com/u/75606622/IPS_IMAGES.zip
Wes
Last edit: 12 years 11 months ago by DaOne.
Please Log in or Create an account to join the conversation.
- DaOne
- Offline
- Premium Member
-
Less
More
- Posts: 155
- Thank you received: 6
12 years 11 months ago #40719
by DaOne
Replied by DaOne on topic Gmoccapy - A new screen for linuxcnc
Norbert,
Here are a few screen shots of my design. Hopefully it will help spark some new ideas.
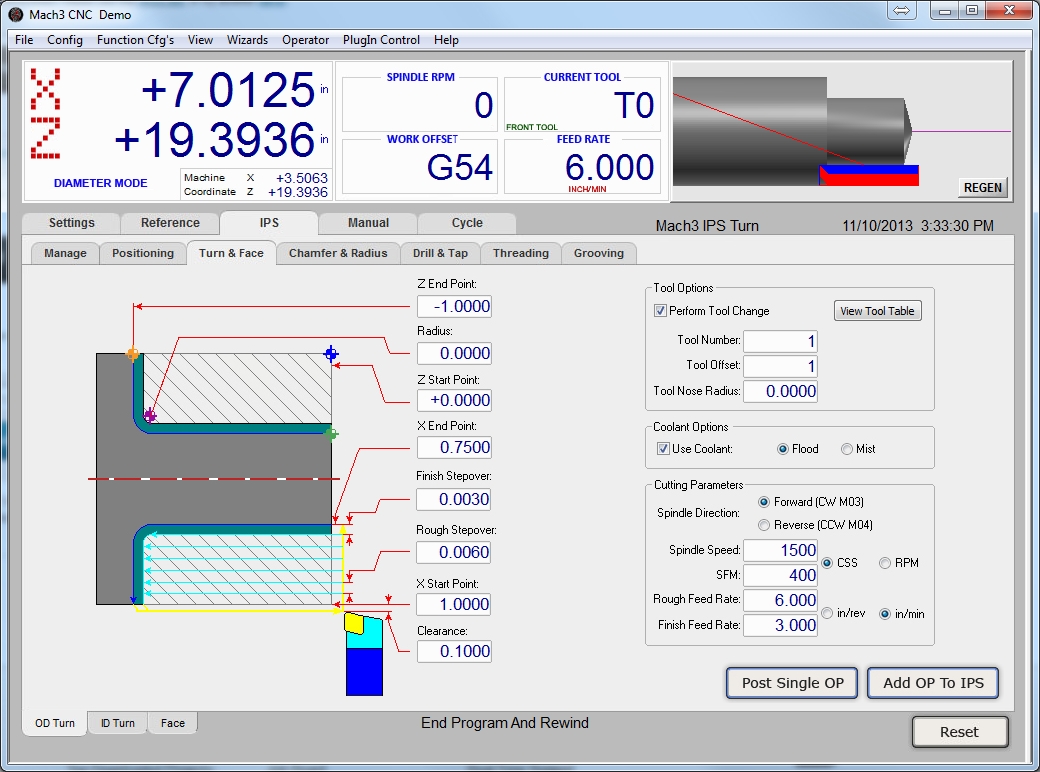
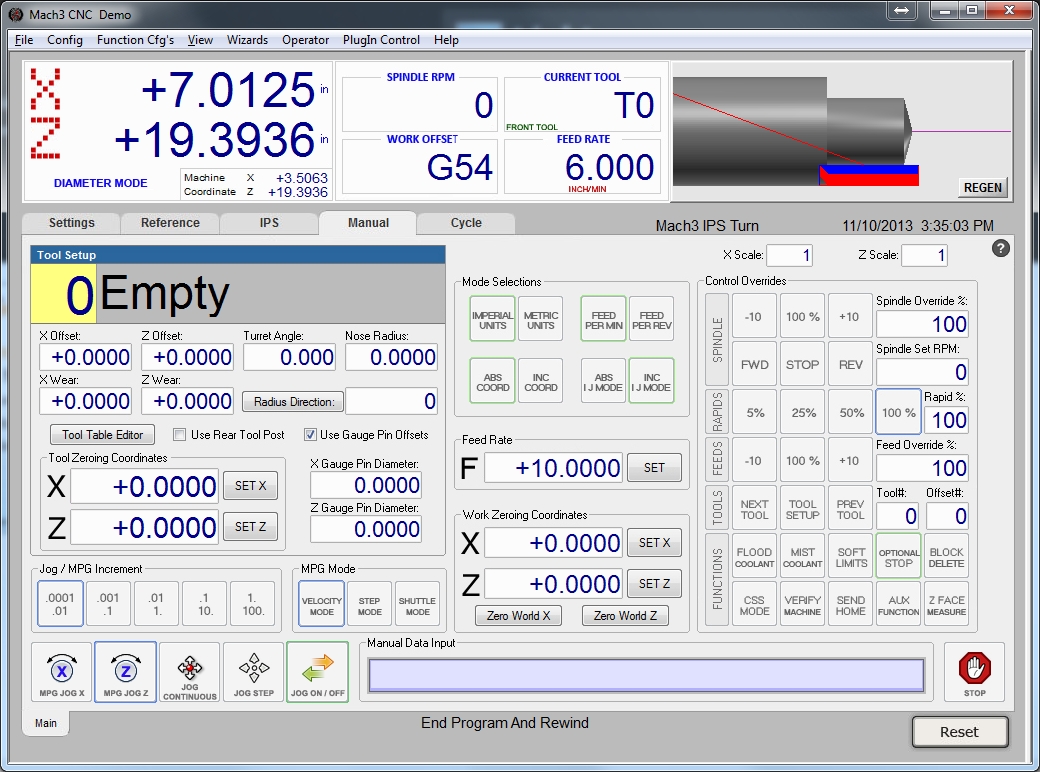
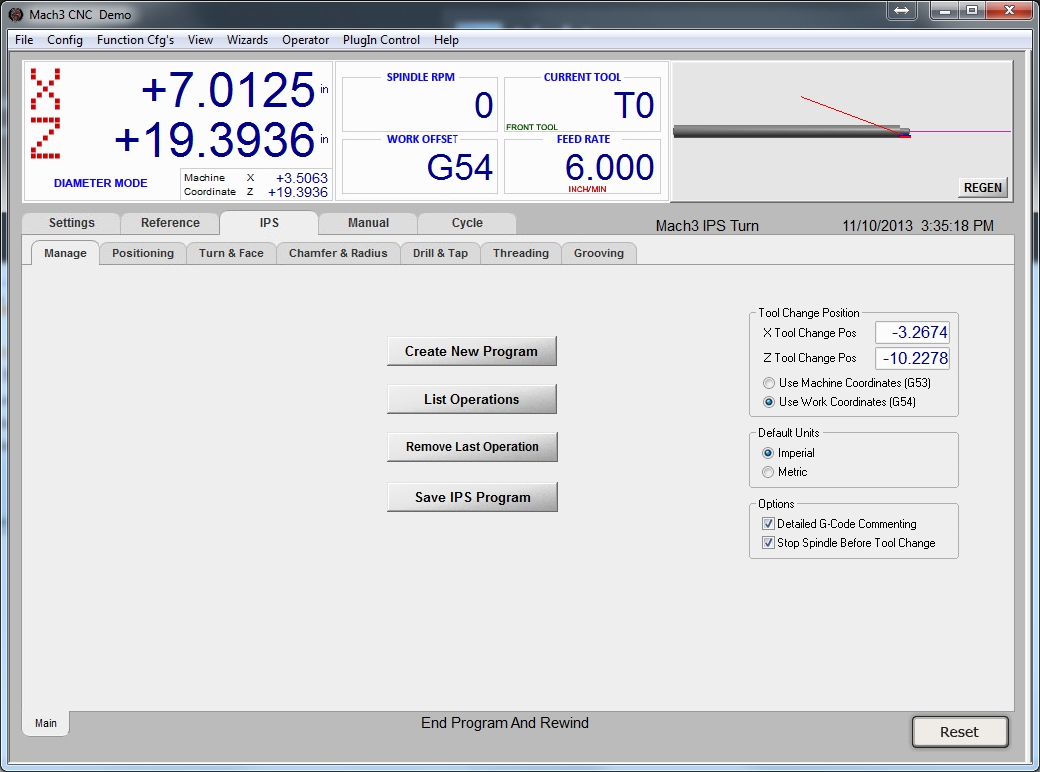
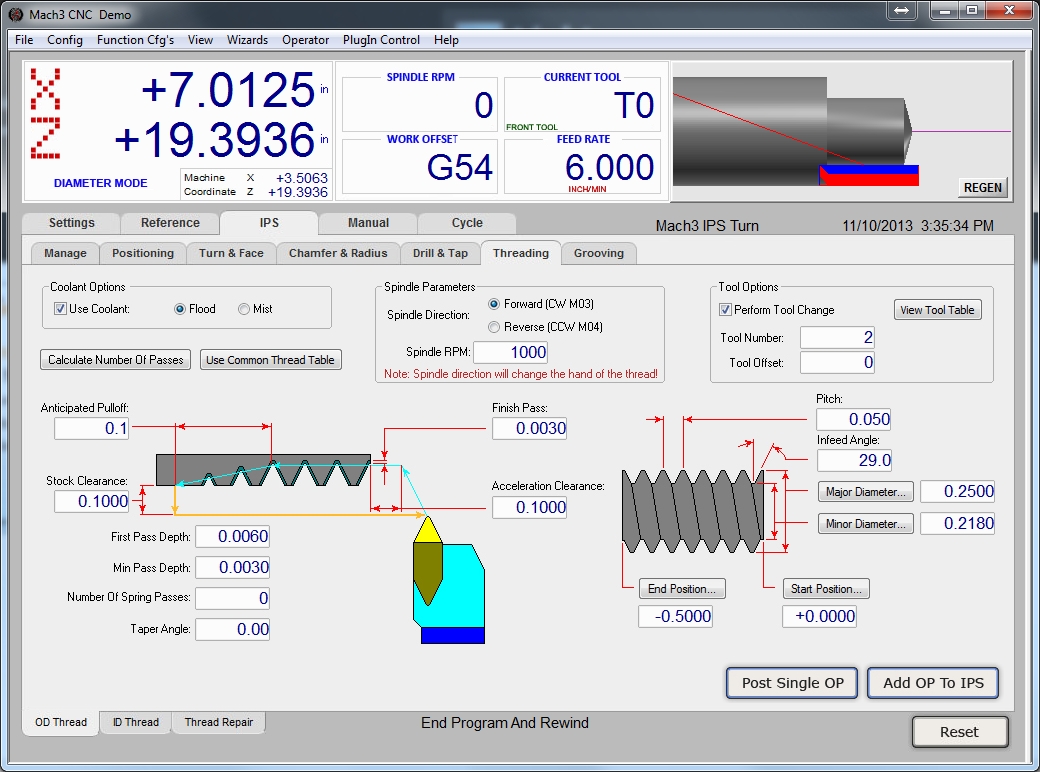
Let me know you thoughts.
Wes
Here are a few screen shots of my design. Hopefully it will help spark some new ideas.
Let me know you thoughts.
Wes
Please Log in or Create an account to join the conversation.
- sliptonic
- Offline
- Premium Member
-
Less
More
- Posts: 132
- Thank you received: 22
12 years 11 months ago #40720
by sliptonic
Hey Norbert,
I can't say that it belongs there. I just know that the equivalent button in Axis was useful to me. With my current config, the brake activates automatically with the spindle so to turn the spindle by hand (like with a dial indicator) I need to release the brake.
I'm not afraid of tackling some glade customization so if that's not typical workflow for others, I can look at the examples and give it a shot. Thanks.
Replied by sliptonic on topic Gmoccapy - A new screen for linuxcnc
newbynobi wrote:
I've been playing with migrating my mill config from Axis to Gmoccapy and I'm really impressed. With the touchscreen, it's a pleasure to use. Thank you.
The only thing I haven't found is a way to toggle the spindle brake. If I need to customize this myself, I'd like to replace the coolant mist button with the brake toggle since I don't have mist.
Is there a guide to basic customization that I haven't found?
Thanks again!
The third way it to explain to me, why you need the spindle brake button on the screen and convince me to add the button, even if I do not know jet where to place it. In my knowledge there is no need for a special button, as motion does include the spindle-brake hal pin so the brake should be connected there.
Norbert
Hey Norbert,
I can't say that it belongs there. I just know that the equivalent button in Axis was useful to me. With my current config, the brake activates automatically with the spindle so to turn the spindle by hand (like with a dial indicator) I need to release the brake.
I'm not afraid of tackling some glade customization so if that's not typical workflow for others, I can look at the examples and give it a shot. Thanks.
Please Log in or Create an account to join the conversation.
- andypugh
- Offline
- Moderator
-

Less
More
- Posts: 19899
- Thank you received: 4655
12 years 11 months ago #40721
by andypugh
I think that a lot of people use ngcgui for this: www.linuxcnc.org/docs/html/gui/ngcgui.html
I use my own macros, a similar interface to your version, but it doesn't actually generate any G-code, just runs a pre-programmed cycle. This suits the way that I work, generally making one-offs from a vague idea.
www.linuxcnc.org/index.php/english/forum...s/26550-lathe-macros
Replied by andypugh on topic Gmoccapy - A new screen for linuxcnc
DaOne wrote: Are you familiar with IPS? Here is a PDF of what I am talking about..
www.haascnc.com/doclib/manual/es0610.pdf
Its basically an interactive program builder.
I think that a lot of people use ngcgui for this: www.linuxcnc.org/docs/html/gui/ngcgui.html
I use my own macros, a similar interface to your version, but it doesn't actually generate any G-code, just runs a pre-programmed cycle. This suits the way that I work, generally making one-offs from a vague idea.
www.linuxcnc.org/index.php/english/forum...s/26550-lathe-macros
Please Log in or Create an account to join the conversation.
- DaOne
- Offline
- Premium Member
-
Less
More
- Posts: 155
- Thank you received: 6
12 years 11 months ago #40725
by DaOne
Replied by DaOne on topic Gmoccapy - A new screen for linuxcnc
Andy,
I have seen your macros and I must say that is great work. Basically the IPS system builds on what your already doing. Instead of a one time op you can basically build a program by recording all those simple steps so you can make another part or many quickly. You can still do just a single op at a time if you want. On a lathe its great because most programs are simple anyways and it beats hand coding. The Haas TL-1 lathe here is used exclusively like this.
Here is the docs on the lathe side for a Haas TL lathe. Starts on page 34...
www.productivity.com/content/customer/do...as%20TL%20Manual.pdf
Wes
I have seen your macros and I must say that is great work.
Basically the IPS system builds on what your already doing. Instead of a one time op you can basically build a program by recording all those simple steps so you can make another part or many quickly. You can still do just a single op at a time if you want. On a lathe its great because most programs are simple anyways and it beats hand coding. The Haas TL-1 lathe here is used exclusively like this.Here is the docs on the lathe side for a Haas TL lathe. Starts on page 34...
www.productivity.com/content/customer/do...as%20TL%20Manual.pdf
Wes
Please Log in or Create an account to join the conversation.
- andypugh
- Offline
- Moderator
-
Less
More
- Posts: 19899
- Thank you received: 4655
12 years 11 months ago #40737
by andypugh
I am pretty sure that this is exactly what NGCGUI does. But you would need input from someone who actually uses it, like JT.
Replied by andypugh on topic Gmoccapy - A new screen for linuxcnc
DaOne wrote: Basically the IPS system builds on what your already doing. Instead of a one time op you can basically build a program by recording all those simple steps so you can make another part or many quickly
I am pretty sure that this is exactly what NGCGUI does. But you would need input from someone who actually uses it, like JT.
Please Log in or Create an account to join the conversation.
Moderators: newbynobi, HansU
Time to create page: 0.662 seconds