
Useful Plasma Thread

8 years 2 months ago #116627
by rodw
Replied by rodw on topic Useful Plasma Thread
I vote for the russian guy to do the coding :woohoo: :blink: :silly:
But as far as kerf allowance goes I believe it simple as LinuxCNC supports a tool offset in Gcode doesn't it?
But as far as kerf allowance goes I believe it simple as LinuxCNC supports a tool offset in Gcode doesn't it?
Please Log in or Create an account to join the conversation.
- islander261
- Offline
- Platinum Member
-

Less
More
- Posts: 757
- Thank you received: 216
8 years 2 months ago #116669
by islander261
Replied by islander261 on topic Useful Plasma Thread
Rod
I have not tried to to use cutter compensation to allow for kerf width. Based on my experience using it with milling machines I think that for most engineering work that use mostly rectilinear shapes it will be worth while to try. I am not sure when trying to use it for cutting artwork with compound arcs and many arc to arc and arc to linear transitions that there may be some problems.
I have several reasons for this, and please remember that all of this is from my prospective of cutting parts (artwork) with lots of compound curves, guys doing mostly engineering work will not have these problems often. First I use a popular low cost CAM program to produce all my cutting code. It has a lot of trouble producing good code when outside kerf compensation (outside offset) is turned on. This is combined with the current trajectory planner arc transition error really makes a mess of things with the feedrate going to zero at unplanned places. Now my current work around is to make all my art work with the defined path being kerf compensated in Inkscape. I actually draw with lines that are the kerf width wide so I know what the actual cutting result will be.
I have used Gcodetools in Inkscape in the past. It actually works quite well and generated good code most of the time. The reason I don't use Inkscape for my final CAM any more is it doesn't have built in nesting capability (yes, I hand nested completed code as subroutines for multiple part files but it is still a PITA), you have to redefine the cuts for each instance of a part which is a PITA for me. Again this is my work flow for cutting full sheets only. I used Inkscape and Gcodetools when I first started and cut out one piece at a time. I bet Nick can produce a nice solution if he wants to.
I will fix a couple of simple files and try to use cutter compensation later this week and see if it makes the TP puke at arc transitions.
John
I have not tried to to use cutter compensation to allow for kerf width. Based on my experience using it with milling machines I think that for most engineering work that use mostly rectilinear shapes it will be worth while to try. I am not sure when trying to use it for cutting artwork with compound arcs and many arc to arc and arc to linear transitions that there may be some problems.
I have several reasons for this, and please remember that all of this is from my prospective of cutting parts (artwork) with lots of compound curves, guys doing mostly engineering work will not have these problems often. First I use a popular low cost CAM program to produce all my cutting code. It has a lot of trouble producing good code when outside kerf compensation (outside offset) is turned on. This is combined with the current trajectory planner arc transition error really makes a mess of things with the feedrate going to zero at unplanned places. Now my current work around is to make all my art work with the defined path being kerf compensated in Inkscape. I actually draw with lines that are the kerf width wide so I know what the actual cutting result will be.
I have used Gcodetools in Inkscape in the past. It actually works quite well and generated good code most of the time. The reason I don't use Inkscape for my final CAM any more is it doesn't have built in nesting capability (yes, I hand nested completed code as subroutines for multiple part files but it is still a PITA), you have to redefine the cuts for each instance of a part which is a PITA for me. Again this is my work flow for cutting full sheets only. I used Inkscape and Gcodetools when I first started and cut out one piece at a time. I bet Nick can produce a nice solution if he wants to.
I will fix a couple of simple files and try to use cutter compensation later this week and see if it makes the TP puke at arc transitions.
John
The following user(s) said Thank You: rodw
Please Log in or Create an account to join the conversation.
- tommylight
-

- Offline
- Moderator
-

8 years 2 months ago #116672
by tommylight
Replied by tommylight on topic Useful Plasma Thread
Icelander, can please post one of those gcode files or just a snippet of it, as i am fairly certain that the trajectory planer problem you mention is not a problem at all, i would venture a guess that the CAM is outputting separate pieces of lines and arcs so that would be the normal trajectory planner behaviour.
From my experience with using several CNC plasma cutters with Linuxcnc and exclusively Inkscape with gcodetools, i have seen that same issue when the lines are cut in the drawings. There is a simple solution to that, selecting everything and going to menu "path>combine" usually solves that problem if everything is already a path, otherwise everything has to be selected and converted to path. That can also be checked by F2 or "edit paths by nodes" tool and checking that all the dots are a single node, as there can be several nodes at the same spot and that causes the above mentioned issue.
From my experience with using several CNC plasma cutters with Linuxcnc and exclusively Inkscape with gcodetools, i have seen that same issue when the lines are cut in the drawings. There is a simple solution to that, selecting everything and going to menu "path>combine" usually solves that problem if everything is already a path, otherwise everything has to be selected and converted to path. That can also be checked by F2 or "edit paths by nodes" tool and checking that all the dots are a single node, as there can be several nodes at the same spot and that causes the above mentioned issue.
Please Log in or Create an account to join the conversation.
8 years 2 months ago - 8 years 2 months ago #116674
by Grotius
Replied by Grotius on topic Useful Plasma Thread
Hi,
I have also tried the G.. tool offset's in linuxcnc with a simple dxf object. It was not very easy to do and next problem is
to define the lead in and lead out's. So i stopped at that moment.
I have tried Inkscape gcode a few times, but i need some help. Tommylight, can you make a tiny document how you program a dxf drawing to g code with inkscape? That would be usefull. Also included with your latest menu path>combine issue. I assume it's the
same as converting a drawing or path to polyline?
Today i made the auto restart function. I will test this function on the machine this week. This function set's the machine 25-30mm back on the cutting path and restarts with the full probe or non-probe procedure again. The restart attemps the user can select.
Also added the pierce speed and the probe speed parameters to the code, and implemented the adaptive speed into the c component. When not enable the adaptive speed is passed trough.
A sample code that i will try at the machine, and if not working good, i can modify it directly at the machine and try again. :whistle:
@Islander :
Yes i saw his inkscape solution, it's not finished, the project is half open. So if we look good at his python code,
we can make it complete and finish it.
We don't need the cutting speed, etc from inkscape. We use excel tool libraries with everything in it. We only need the M3 and M5. Lead in and lead out.
Autonesting module for python we can make later on. My feeling say's that i can better produce a nesting module in c language.
I have also tried the G.. tool offset's in linuxcnc with a simple dxf object. It was not very easy to do and next problem is
to define the lead in and lead out's. So i stopped at that moment.
I have tried Inkscape gcode a few times, but i need some help. Tommylight, can you make a tiny document how you program a dxf drawing to g code with inkscape? That would be usefull. Also included with your latest menu path>combine issue. I assume it's the
same as converting a drawing or path to polyline?
Today i made the auto restart function. I will test this function on the machine this week. This function set's the machine 25-30mm back on the cutting path and restarts with the full probe or non-probe procedure again. The restart attemps the user can select.
Also added the pierce speed and the probe speed parameters to the code, and implemented the adaptive speed into the c component. When not enable the adaptive speed is passed trough.
A sample code that i will try at the machine, and if not working good, i can modify it directly at the machine and try again. :whistle:
Code:
// Restart procedure :
Adaptive_feed_out = -1; // set value backward's.
Time_restart_procedure += fperiod;
Torch_on_out = 0;
Count_restart_procedure = Count_restart_procedure + 1;
if(Count_restart_procedure >= Auto_restart_times){
Pause_machine = 1;// Wait for machine operator.
}
else {
Pause_machine = 0; // move backward's
if(Time_restart_procedure > 3){ // We begin with 3 second's moving backward.
Pause_machine = 1;
Adaptive_feed_out = 1; // set value forward's.
goto Start_loop; // start torch again following probe procedure.
}
}
//Pin's :
//Adaptive_feed_in
//Adaptive_feed_out
//Auto_restart_times
//time_restart_procedure;
//Count_restart_procedure;
@Islander :
I bet Nick can produce a nice solution if he wants to.
Yes i saw his inkscape solution, it's not finished, the project is half open. So if we look good at his python code,
we can make it complete and finish it.
We don't need the cutting speed, etc from inkscape. We use excel tool libraries with everything in it. We only need the M3 and M5. Lead in and lead out.
Autonesting module for python we can make later on. My feeling say's that i can better produce a nesting module in c language.
Last edit: 8 years 2 months ago by Grotius.
Please Log in or Create an account to join the conversation.
- islander261
- Offline
- Platinum Member
-
Less
More
- Posts: 757
- Thank you received: 216
8 years 2 months ago #116684
by islander261
Replied by islander261 on topic Useful Plasma Thread
Grotius
Yes, I have hacked Nick's python code to produce nonRS274 code to run my non RS274 mill. I have never tried to use a offset with Gcodetools. Yes I agree we don't need cutting parameters from Inkscape. I am not looking for an automated nesting solution like Pronest just a way to manually nest multiple parts while only defining the cuts once for the first instance of each part? Look at the work flow in SheetCAM.
Tommy
Thanks, I am aware of the problems that can happen if you don't have continuous lines. I am very careful with my drawings to make sure that each path is a single object. I did a lot of work trying to get rid of witness marks when I worked out my corner hold component because I thought it was causing the marks. That is when I found out that the motion.reqested-vel pin does not reflect the contents of the active F block but the speed the TP thinks the machine can move at. When I fixed that problem the witness marks still where at several locations. On further investigation I found they are at code locations perfectly described by the bug tracker.
github.com/LinuxCNC/linuxcnc/issues/447
and
github.com/LinuxCNC/linuxcnc/issues/426
I am sorry but I do not have the coding skills to tackle either one of these bugs.
John
Yes, I have hacked Nick's python code to produce nonRS274 code to run my non RS274 mill. I have never tried to use a offset with Gcodetools. Yes I agree we don't need cutting parameters from Inkscape. I am not looking for an automated nesting solution like Pronest just a way to manually nest multiple parts while only defining the cuts once for the first instance of each part? Look at the work flow in SheetCAM.
Tommy
Thanks, I am aware of the problems that can happen if you don't have continuous lines. I am very careful with my drawings to make sure that each path is a single object. I did a lot of work trying to get rid of witness marks when I worked out my corner hold component because I thought it was causing the marks. That is when I found out that the motion.reqested-vel pin does not reflect the contents of the active F block but the speed the TP thinks the machine can move at. When I fixed that problem the witness marks still where at several locations. On further investigation I found they are at code locations perfectly described by the bug tracker.
github.com/LinuxCNC/linuxcnc/issues/447
and
github.com/LinuxCNC/linuxcnc/issues/426
I am sorry but I do not have the coding skills to tackle either one of these bugs.
John
The following user(s) said Thank You: tommylight
Please Log in or Create an account to join the conversation.
8 years 2 months ago - 8 years 2 months ago #116685
by Grotius
Replied by Grotius on topic Useful Plasma Thread
Hi John,
I will do the greetings to Nick from you at the Russian Federation.
John :
This is the boss of linuxcnc not of russian federation :
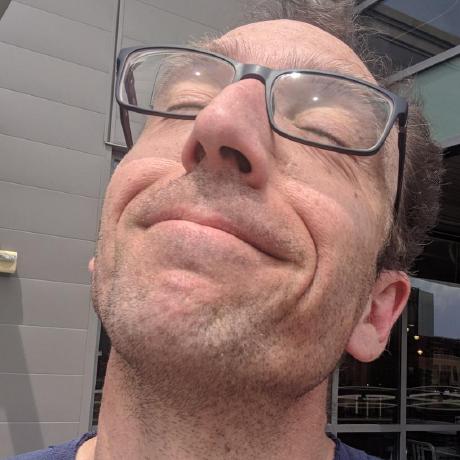
He looks like enjoying the Sun.
I think we need a new boss. Linuxcnc needs more update's.
I am awere of tunneling devices on linuxcnc preemt rt, server type instruments.
The one with the bird on github is dangerous. He eat's me at once.
I will do the greetings to Nick from you at the Russian Federation.
John :
I have hacked Nick's python code
This is the boss of linuxcnc not of russian federation :
He looks like enjoying the Sun.
I think we need a new boss. Linuxcnc needs more update's.
I am awere of tunneling devices on linuxcnc preemt rt, server type instruments.
The one with the bird on github is dangerous. He eat's me at once.
Last edit: 8 years 2 months ago by Grotius.
Please Log in or Create an account to join the conversation.
Moderators: snowgoer540
Time to create page: 0.244 seconds