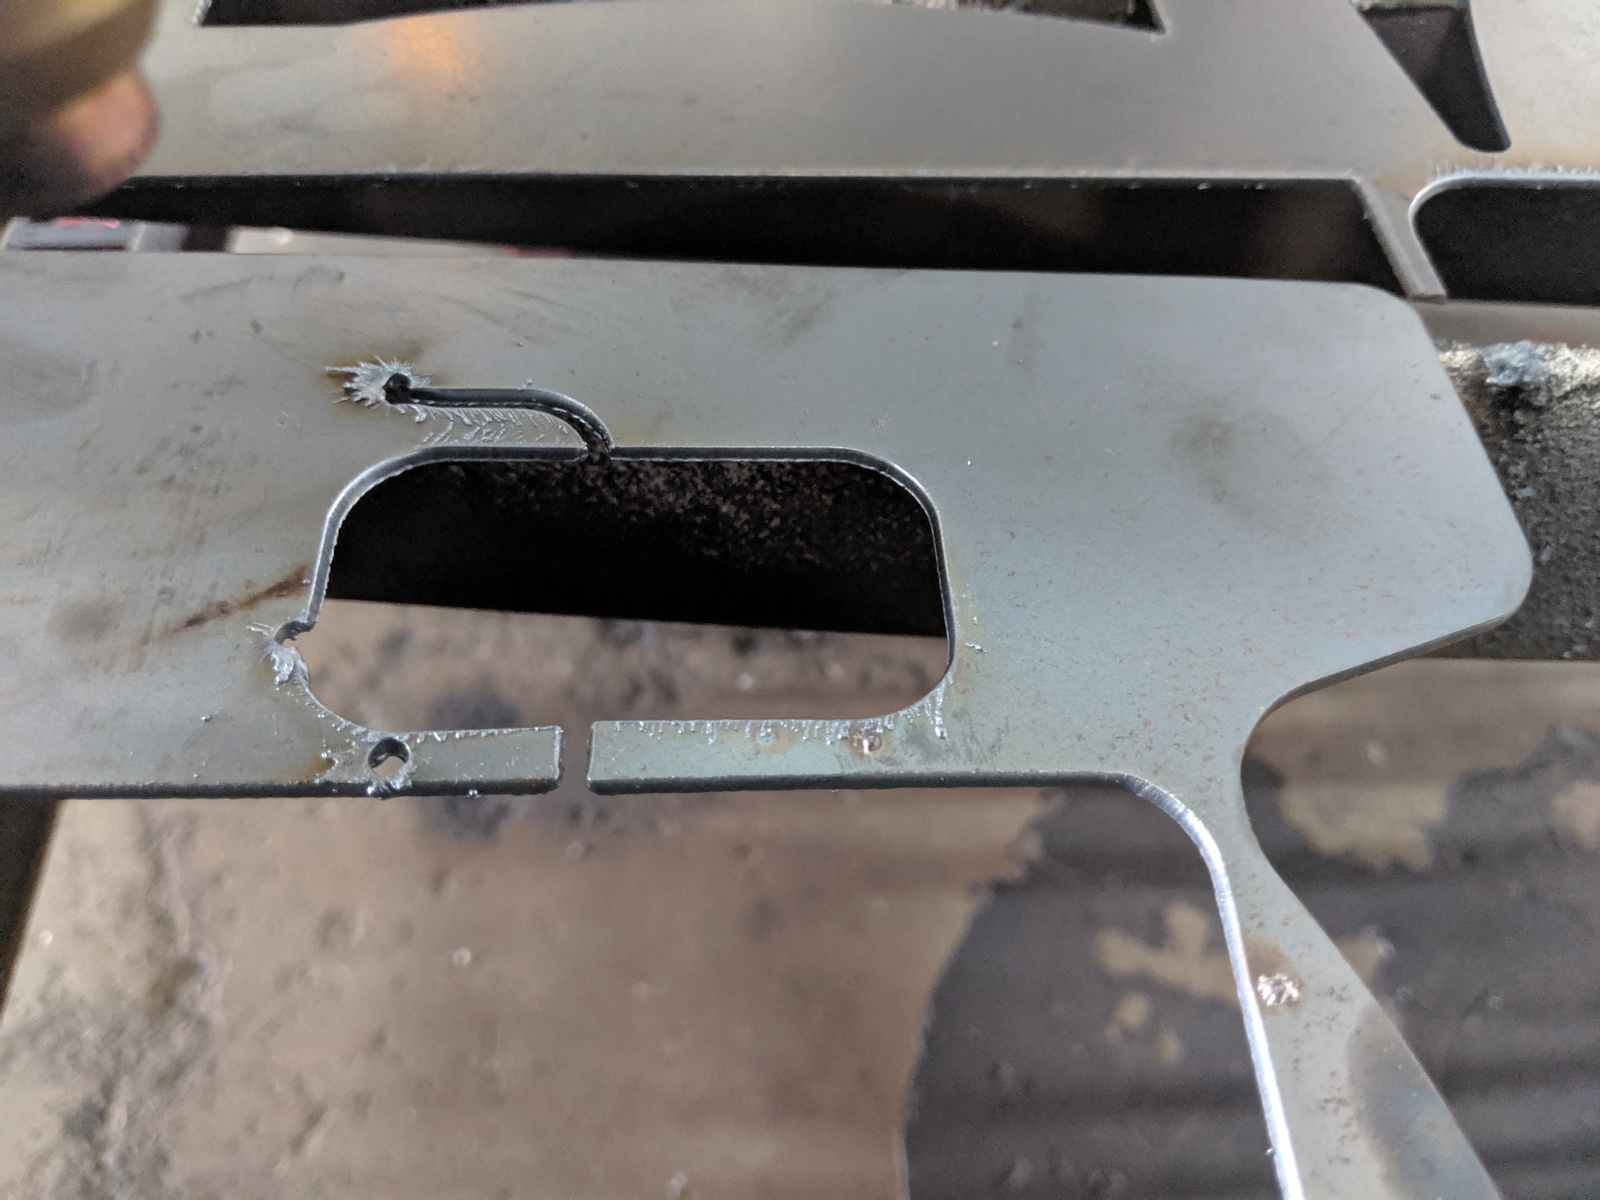
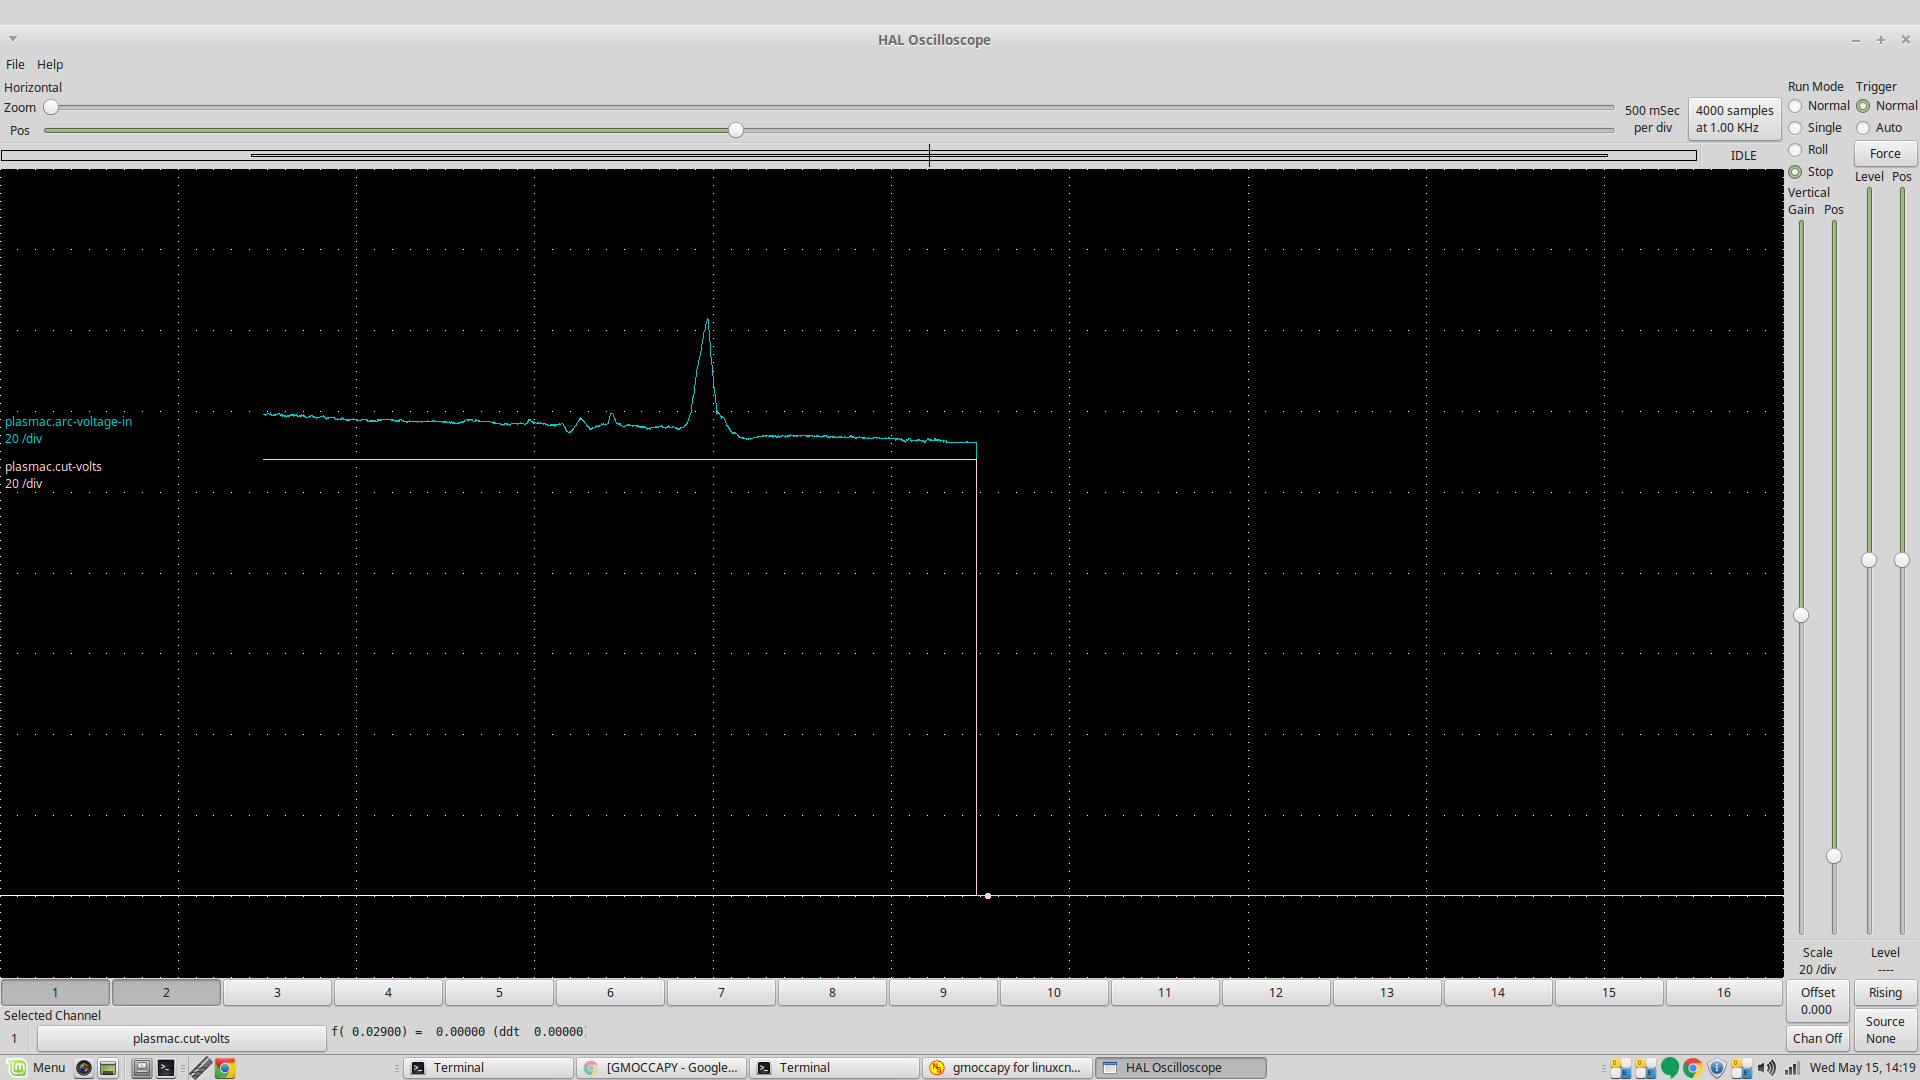
I thought this was pretty interesting and just says how much wisdom there is in this open source group that is leading to such a superior plasma controller here in the LinuxCNC Plasmac hub!
I finally got a couple of prototype parts cut today. Its taken me 2 days mucking around with post processors and the inevitable plasmac upgrades twice a day! Anyway, I took them to my neighbour next door to get folded on his brake press. He purchased a $100k table about 6 months ago with a Hypertherm Maxpro 200 inverter with HF start on it. He's been plagued by intermittent problems when cutting mild steel.
They finally worked out this week that the high frequency start is causing noise or voltage to go back through the ohmic sensing circuit while cutting and causing the electronics to fault. As soon as they removed the ohmic sensor wire, it was fine. I guess it triggers an unexpected probe signal or similar which faults the system. I told him that that is not possible on my home built system the way the plasmmac/Islander ohmic sensing circuit is designed because both sides of the ohmic sensing circuit are physically disconnected unless we are actually probing.
This has been a very expensive fault for him in terms of downtime and also quite expensive for the supplier who have replaced a torch and electronics boards that are probably damaged. Instead of fixing it the plasmac way, they are stuffing around winding the ohmic wire around a bobbin to help prevent the RFI. They are actually going to reduce the wire diameter so they can get more turns around the bobbin! Sounds like a workaround for a poor design to me!