Hi, I'm building a plasma machine and I have some questions about how to set it up.
1. I would like to control the ARC override with an encoder so that. I don't want to use a mouse. When cutting, I look at the arc and the encoder would adjust the height as needed. Using a mouse is too complicated.
2.
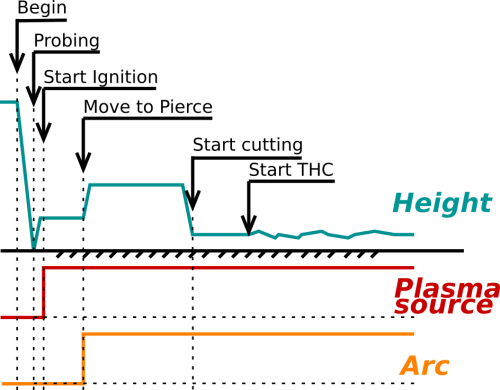
when cutting thick material, I need the torch to go up after the arc is ignited so that the blasting material does not spray on the nozzle. I am attaching a picture describing this function. This is how original software handled it.
is it possible to setup qtplasmac for this features?
Thanks Martin
1:
I would guess that it could be made to be possible, but it is not currently. The better question would be is it necessary... Have you used QtPlasmaC at all? You mentioned "this is how the original software handled it", I am wondering what you were using. At any rate, QtPlasmaC has "Auto Volts" which might negate the need for what you're describing.
linuxcnc.org/docs/devel/html/plasma/qtplasmac.html#qt_thc
2:
That looks very much like a recreation of Hypertherm's diagram from their ARC GLIDE THC manual. QtPlasmaC follows that logic, with the exception of the "transfer arc" portion you describe. Again, it's probably possible, but I believe they do this so that they get a good transfer from pilot arc to cutting arc on High Definition plasma cutters. It seems to be less about consumables and more about the ability to establish a valid arc.
An excerpt from that manual "Transfer Height: When the arc transfers to the workpiece, it can be “stretched” to the pierce height. The transfer height is lower than the pierce height because initiating arc transfer at a high pierce height may result in the arc not transferring to the workpiece at all. Enter the Transfer Height as a percentage of the cut height or as an actual transfer height distance."
All that said, it doesn't mean there's not a use case out there for someone. From a splashback standpoint, I would think it matters how thick of material you are cutting. In the air plasma scene, I'm not sure it applies, most cut charts just go to "edge start" when that become a big deal.
I'm curious what the use case is, IE, how thick of stuff are you piercing, what power source are you using, etc.