
- Posts: 164
- Thank you received: 24
Retrofitting a 1986 Maho MH400E
- J Green
- Offline
- Elite Member
-

Less
More
7 years 9 months ago #123808
by J Green
Replied by J Green on topic Retrofitting a 1986 Maho MH400E
Mark
Great - seeing the machine an slotting head being used. I wonder if a big diameter cutter on a horizontal arbour would solve the part to cutter height problem . What is the max diameter cutter that can be used with the over arm ?
The near retrofitting future---- Or, my wish list for the updated spindle-speed control comp
Would it be possible to include provisions for spindle indexing ? Maybe for both horizontal and vertical spindle .
Could there be some provision for spindle speed when using a VFD driven spindle motor , but still keeping the gear box shifting section of the code.
The distant retrofitting future----
My vote is for a ongoing update of what is happening in the Marks MAHO world !
Maybe consider a summer gathering of the MHxxxXX retrofit people
As to this site content wishes--- might ask Andy P what his off the wall thoughts are. I think it would be worthwhile if you could continue to maintain some guiding control , not as a moderator but as you have been.
Coolant
Andy P has a friend building a working model race car engine. His friend has made several You-Tube videos of which one shows the coolant system rigged up for use on his Deckel mill. I can't find that You-Tube video , maybe Andy would remember.
any way please keep on keeping on
Bob
- RotarySMP
- Offline
- Platinum Member
-

Less
More
- Posts: 1635
- Thank you received: 595
7 years 9 months ago #123816
by RotarySMP
Hi Bob, As built by Maho, the MHx00E series has no provision for a spindle angle feedback or indexing, so there is no information to built a comp on.On the 400E, the vertical and horizontal spindles turn at the same speed, so a single encoder on the horizontal or output drive shaft should be enough. John (drimaropoylos) has added an encoder to his spindle, as he is also adding a VFD.
forum.linuxcnc.org/12-milling/33035-retr...400e?start=100#99993
forum.linuxcnc.org/12-milling/33035-retr...00e?start=170#100565
He is doing his gearbox control with classic ladder rather than a comp, so anyone following us will have options of either HAL comp or ladder solutions, depending in what they are most comfortable with.
Since my machine doesn't produce the spindle angle information, and I am reliant on a friends generous volunteered time and assistance for the programming, I won't be doing the spindle indexing routines. At least not until Sergey has the need to tap a thousand holes and decides we need syncronised spindle motion The source code for our comp is published on github though, so it should be easy enough to modify it.
github.com/jin-eld/mh400e-linuxcnc
The later MHx00E2 models also had a simplified gearbox (Just the back gear?) and a VFD so they may already have spindle angle feedback encoders. I get the impression that they are pretty rare though.
Mark
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
Oh Bob, that is just evil! I never knew a corner milling attachment was made for the MAHO, but now I NEED one!Saw this in a 1982 product range brochure . Hope it doesn't cause undue lust for old Maho attachments.
The near retrofitting future---- Or, my wish list for the updated spindle-speed control comp
Would it be possible to include provisions for spindle indexing ? Maybe for both horizontal and vertical spindle .
Could there be some provision for spindle speed when using a VFD driven spindle motor , but still keeping the gear box shifting section of the code.
Hi Bob, As built by Maho, the MHx00E series has no provision for a spindle angle feedback or indexing, so there is no information to built a comp on.On the 400E, the vertical and horizontal spindles turn at the same speed, so a single encoder on the horizontal or output drive shaft should be enough. John (drimaropoylos) has added an encoder to his spindle, as he is also adding a VFD.
forum.linuxcnc.org/12-milling/33035-retr...400e?start=100#99993
forum.linuxcnc.org/12-milling/33035-retr...00e?start=170#100565
He is doing his gearbox control with classic ladder rather than a comp, so anyone following us will have options of either HAL comp or ladder solutions, depending in what they are most comfortable with.
Since my machine doesn't produce the spindle angle information, and I am reliant on a friends generous volunteered time and assistance for the programming, I won't be doing the spindle indexing routines. At least not until Sergey has the need to tap a thousand holes and decides we need syncronised spindle motion
The source code for our comp is published on github though, so it should be easy enough to modify it.github.com/jin-eld/mh400e-linuxcnc
The later MHx00E2 models also had a simplified gearbox (Just the back gear?) and a VFD so they may already have spindle angle feedback encoders. I get the impression that they are pretty rare though.
Mark
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
7 years 9 months ago - 7 years 9 months ago #123818
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
To anyone just considering/planning a user interface module, here are some thoughts on mine.
I see all the hype around that new guis which look prettier. Once you use gmoccapy, you really appreciate how well thought out Norberts interface is. The way the soft keys adapt to the task at hand (jogging/touching off, loading/editing/running a program etc ) is extremely intuitive. You end up with a pretty simple looking screen, which always shows you what is relevant for what you are doing, never looks cluttered with a million settings, and doesn't leave you head scratching "where do I find xx function" The adaptive bezel keys, combined with duplicate hard bezel keys covers a lot of what you would normally add buttons for.
I stumbled back over John's advice not to use a vertical screen.
forum.linuxcnc.org/12-milling/33035-retr...00e?start=130#100132
I don't mind the vertical alignment, but mine is mounted too low to be comfortable. I used a pretty old ELU touch screen, and the viewing angle is crap. I find I end up with a stool in front of the user module, and sit down to use the MDI, or edit a few lines.
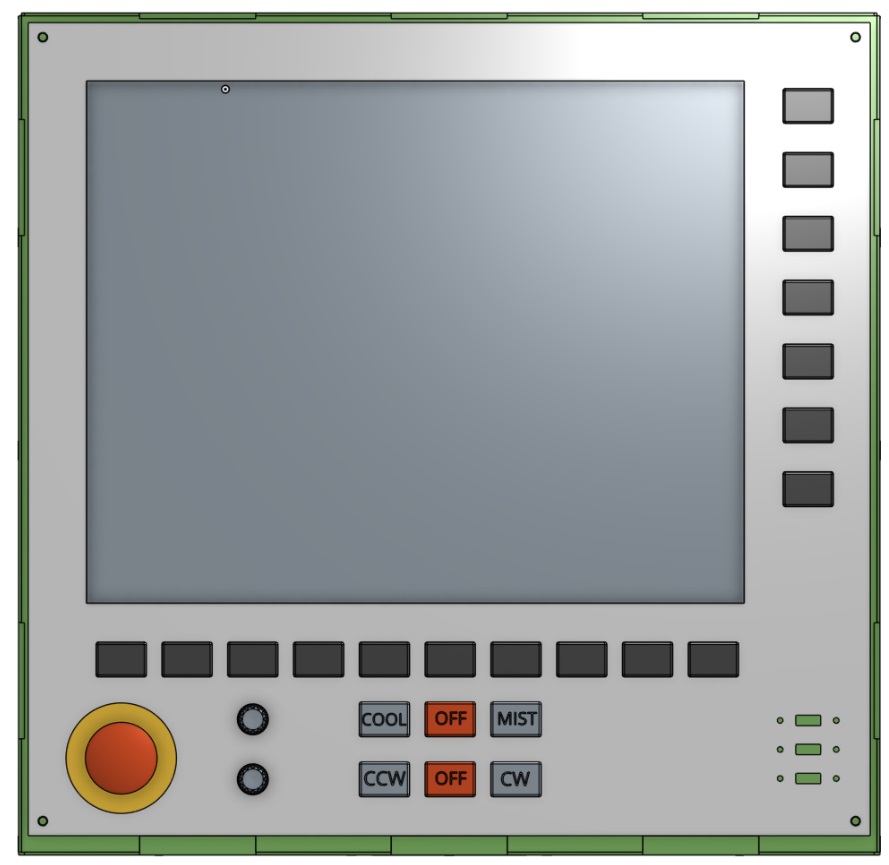
When I planned my physical buttons and encoders on the control panel, I had no experience with a CNC mill, so my decision process was pretty lame. I figured you don't need physical run/stop/pause cycle buttons with gmoccapy, as these are covered by the bezel edge keys. That still seems like a good decision. I piggybacked a hard wired controller start onto the top bezel key, so the controller start is similar to a Phillips two button press.
My decision process what to add on the six hard keys was pretty lame. Along the lines of, buttons look cool, heidenhain has them, what could I put on buttons. Coolant and spindle start stop are available on the gmoccapy touch screen, but not the bezel soft keys, so I made physical buttons for them. Not a terrible idea, but I do notice I often hit the touch screen rather than use the button.
Mark
I see all the hype around that new guis which look prettier. Once you use gmoccapy, you really appreciate how well thought out Norberts interface is. The way the soft keys adapt to the task at hand (jogging/touching off, loading/editing/running a program etc ) is extremely intuitive. You end up with a pretty simple looking screen, which always shows you what is relevant for what you are doing, never looks cluttered with a million settings, and doesn't leave you head scratching "where do I find xx function" The adaptive bezel keys, combined with duplicate hard bezel keys covers a lot of what you would normally add buttons for.
I stumbled back over John's advice not to use a vertical screen.
forum.linuxcnc.org/12-milling/33035-retr...00e?start=130#100132
I don't mind the vertical alignment, but mine is mounted too low to be comfortable. I used a pretty old ELU touch screen, and the viewing angle is crap. I find I end up with a stool in front of the user module, and sit down to use the MDI, or edit a few lines.
When I planned my physical buttons and encoders on the control panel, I had no experience with a CNC mill, so my decision process was pretty lame. I figured you don't need physical run/stop/pause cycle buttons with gmoccapy, as these are covered by the bezel edge keys. That still seems like a good decision. I piggybacked a hard wired controller start onto the top bezel key, so the controller start is similar to a Phillips two button press.
My decision process what to add on the six hard keys was pretty lame. Along the lines of, buttons look cool, heidenhain has them, what could I put on buttons. Coolant and spindle start stop are available on the gmoccapy touch screen, but not the bezel soft keys, so I made physical buttons for them. Not a terrible idea, but I do notice I often hit the touch screen rather than use the button.
Mark
Last edit: 7 years 9 months ago by RotarySMP.
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
7 years 9 months ago #123819
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
A couple of questions:
- Is AND2 normally autoinstalled in the basic linuxCNC set up? I tried to add it to my HAL but it is unknown on my controller. Where can I get that component from?
- I have my two user interface encoders connected to the MESA 7i77 as encoder 4, and 5. The axis encoders are 0,1,2. There is nothing connected to encoder 3. I only see the HAL command below, and if I change it num_encoders=5 can that work?
Can he HM2 driver deal with that, or will I have to move the addition two encoders to position 3 and 4 to be sequential?
I had to give up on shaping that anvil with the slotting head. There is a hard area which just ground the edge straight off the HSS tool bit.
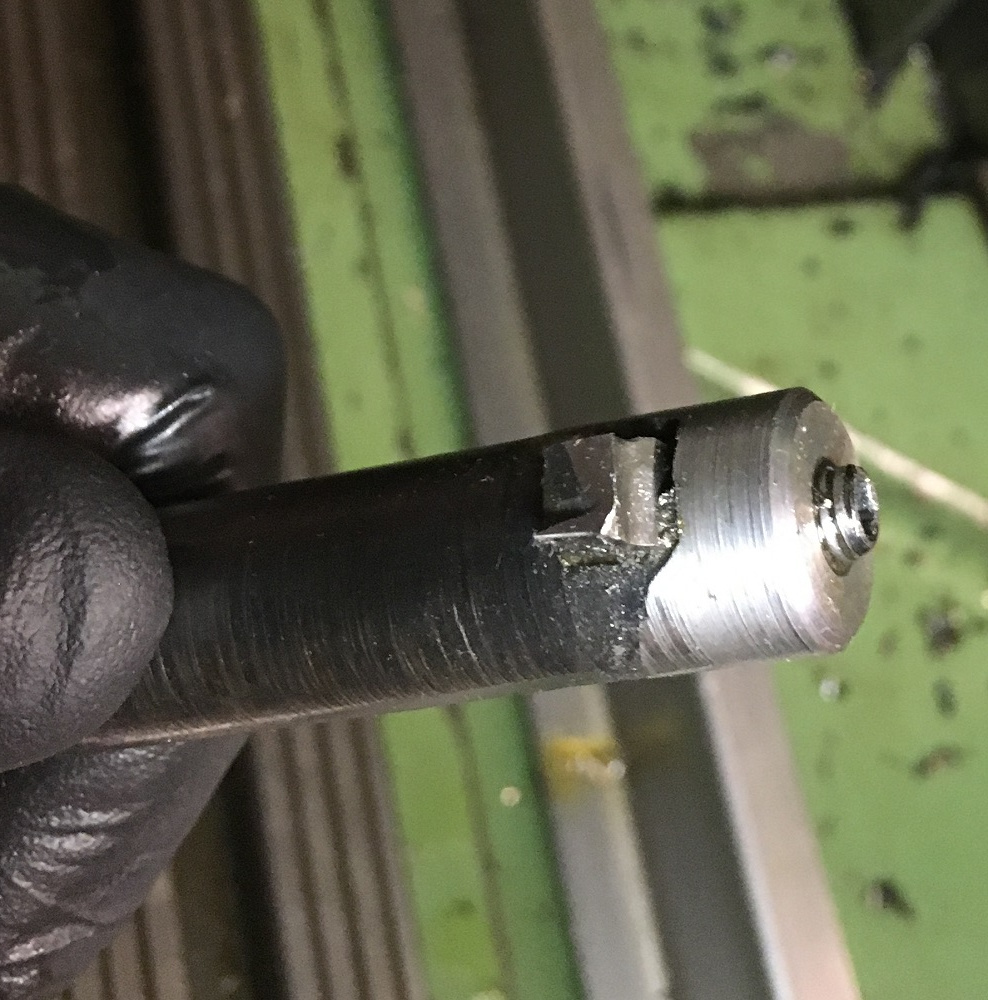
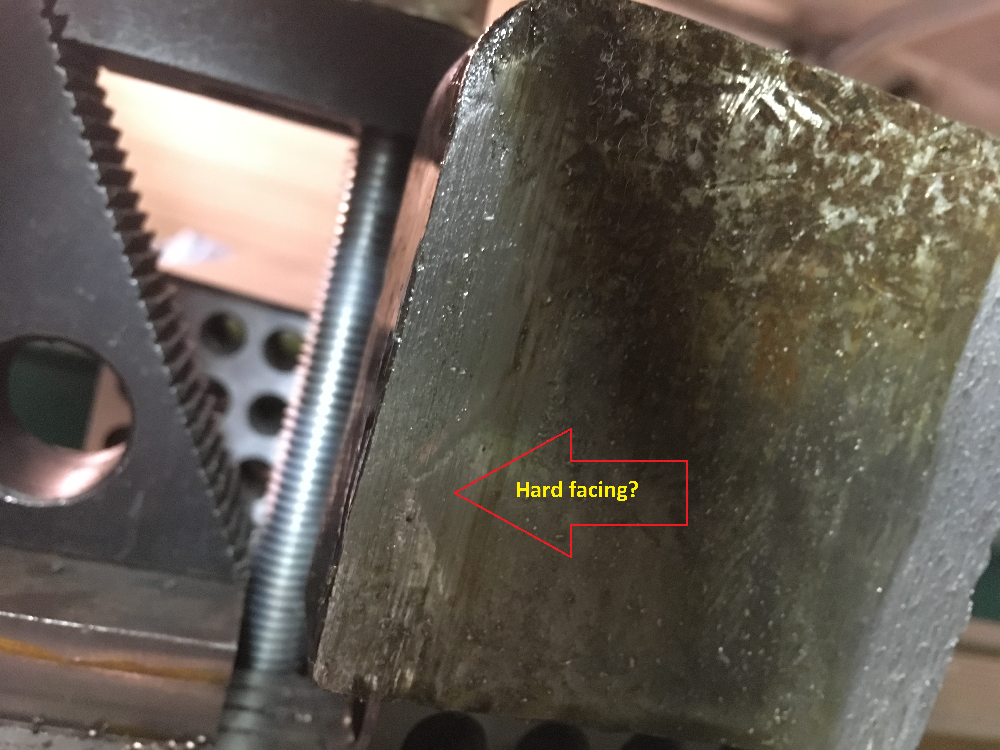
Next attempt will be the 100mm carbide insert face mill in the horizontal spindle.
Mark
- Is AND2 normally autoinstalled in the basic linuxCNC set up? I tried to add it to my HAL but it is unknown on my controller. Where can I get that component from?
- I have my two user interface encoders connected to the MESA 7i77 as encoder 4, and 5. The axis encoders are 0,1,2. There is nothing connected to encoder 3. I only see the HAL command below, and if I change it num_encoders=5 can that work?
Can he HM2 driver deal with that, or will I have to move the addition two encoders to position 3 and 4 to be sequential?
Code:
loadrt hm2_pci config=" num_encoders=3 num_pwmgens=0 num_stepgens=0 sserial_port_0=300xxx"
I had to give up on shaping that anvil with the slotting head. There is a hard area which just ground the edge straight off the HSS tool bit.
Next attempt will be the 100mm carbide insert face mill in the horizontal spindle.
Mark
- snoozer77
- Offline
- Premium Member
-

Less
More
- Posts: 97
- Thank you received: 12
7 years 9 months ago #123828
by snoozer77
Replied by snoozer77 on topic Retrofitting a 1986 Maho MH400E
Just an opinion on physical run, pause and stop buttons. I use machines with both types of controls. One large vertical borer with retrofitted touch screen only, and another reftrofitted mill with normal screen and physical buttons. I believe having physical buttons is safer (on the machines i use) as you can always have your finger on the physical button, while you watch the machine, waiting for something unexpected to happen......... 
In the end, it comes down to personal preference. Whatever your comfortable with.
Cheers
Matt
In the end, it comes down to personal preference. Whatever your comfortable with.
Cheers
Matt
- andypugh
- Offline
- Moderator
-

Less
More
- Posts: 19899
- Thank you received: 4655
7 years 9 months ago #123839
by andypugh
it's one of the most basic components. it really should be there.
HAL names are case-sensitive, though. it should be
for example
Replied by andypugh on topic Retrofitting a 1986 Maho MH400E
RotarySMP wrote: - Is AND2 normally autoinstalled in the basic linuxCNC set up? I tried to add it to my HAL but it is unknown on my controller.
it's one of the most basic components. it really should be there.
HAL names are case-sensitive, though. it should be
Code:
loadrt and2 count=3
The following user(s) said Thank You: RotarySMP
Moderators: piasdom
Time to create page: 0.241 seconds