Hurco KMB-IS CNC update

More
6 years 2 months ago #177278 by CORBETT
Replied by CORBETT on topic Hurco KMB-IS CNC update
True, there should not be any way to mess up the servo amp unless wiring for the power was messed up somewhere. Especially if you detach the analog inputs to avoid anything else coming in. Be aware that most likely one or all 3 of the axis will start to try and move when you power the amps. If you do not have the limit switches (proximity switches) working, then you can crash an axis. So be careful to just power up the servo amp with out first having a way of killing power really quick. If it were me WITH POWER OFF TO MACHINE, I would reach down into the machine and turn the Y ball screw until the table was in the very middle, X is not reachable unless you take off the cover to the servo motor and turn at the motor coupling (may have to do this elsewhere, been awhile), but do the same and put the table in the middle. Do the same for Z, but keep in mind you have very little run out in Z, only 6" travel in Z, 3" each way. That way if you fire up the amps and they start moving the motors you will not crash. They usually move with a slow drift, but you do not know what the previous person did to the machine, so you have to be careful that one of the axis doesn't just suddenly take off, hence why you need a way to kill power to amps really quick.

One thing is that if you keep the wiring as is and do not bypass the contactor you will need to power other items to get the servo amps to work. Back when I was speaking of safety blocks in a previous post, they are in this part also. The K5 relays are what control the ACC contactor that powers the amps, but I know you sent a pic with just a little different setup. Yours does not appear to have the ACC contactor in the same place. I will go back later tonight and try and take a look and see how it was done (this is a bad work week for me, so not much time). If you were going to fire up the amps, the air pressure switch needs air pressure at the back and the emergency stop chain will need to be working also. They would have had some type of contactor to break power to the amps for an emergency condition. But since you may have an upgrade from MIdwest, this could be wired totally different. They are not going to bypass safety themselves either as they are a company that would be facing liability and lawsuits f that was the case.

But once you get power to the transformer and it passes to the amps, whether through a relay or contactor, then you should be ready to see what the servos are going to do. You can do a quick and dirty movement of the X using a AAA battery (NOT 9V BATTERY) but this is dangerous and you would need to understand several things before attempting this. But this is the way to check if everything is fine with the servos and can move the table around to check.


Moving down hills are not fun at all, definitely tie off well as better overkill than underkill and have the machine on its side. Yeah for what you described, I would plan all day and very slow methodical way of doing it. We are riggers also as we install fire pumps and have to be careful with trying to keep the assembly from flexing to avoid re-aligning the driver to the pump Measure everything before going with machine to make sure height isn't a problem, but head can come off for more room getting in. We took the entire spindle assembly off to move one of them.


Will be back later,
Robert

Please Log in or Create an account to join the conversation.

More
6 years 2 months ago #177281 by Teknic_Servo
Hi _big_,

I'm an engineer with Teknic and I recently came across this post; I thought it might be helpful to quickly clarify a few questions/comments about the ClearPath motors.

tommylight is correct - LinuxCNC is compatible with the ClearPath SD motors ( www.teknic.com/products/clearpath-brushl...stepper-replacement/ ) as long as you provide 5-24VDC Step and Direction signals. If you’re planning on reusing your existing servo drives though, then ClearPath is not an appropriate option. ClearPath is an integrated servo motor, servo drive, and encoder; so to use it on your machine you would need to replace your existing motors and drives.

Speaking to the output power of ClearPath, there are options ranging from 100 W, NEMA 23 and 34 motors to higher-powered, NEMA 56 and 143 models, which output up to 5.8 kW. The optimal ClearPath motors depend on your application's peak and continuous torque requirements, target speed(s), and a number of other factors.

Without more information about your application, I can't say whether or not Teknic motors could be a good fit, but I'd be happy to discuss it further if you are interested.

If you have any questions about sizing or using ClearPath, please feel free to give us a call at 585-784-7454, or use our "Contact Us" form online. ( www.teknic.com/contact/ ).

Best,
Nick S. - Teknic Servo Systems Engineer

Please Log in or Create an account to join the conversation.

More
6 years 2 months ago #177289 by CORBETT
Replied by CORBETT on topic Hurco KMB-IS CNC update
I forgot to add earlier that you have the same identical pendant that I had.

Man I could fly on that thing. I could be watching the spindle and reach over punching what ever I needed as I had the whole thing memorized. May sound crazy, but I still do miss using it as I was so verse with it....

Please Log in or Create an account to join the conversation.

More
6 years 2 months ago - 6 years 2 months ago #177291 by CORBETT
Replied by CORBETT on topic Hurco KMB-IS CNC update

Leith,

Ok here is a basic drawing from Hurco for the transformers. This is not the drawing that came with the Schematics, but is practically the same. I will try to find the other transformer schematic. Once again, during this time period Hurco tried to keep everything built and looking the same through out all machines. I looked at several big VMC's that had almost the same cabinet layout as mine, just larger contactors for the spindle motor and other added items.

Anyway, this may help you, but like I said before you should be able to trace the wiring back to the left cabinet and to the step down transformer and then to the disconnect.

Will be back later,
Robert


Here is the PDF schematic

Your browser does not support embedded PDFs. Please download the file here: Download PDF.

Last edit: 6 years 2 months ago by CORBETT.

Please Log in or Create an account to join the conversation.

More
6 years 2 months ago - 6 years 2 months ago #177333 by CORBETT
Replied by CORBETT on topic Hurco KMB-IS CNC update

Leith,

Ok, I went back and looked at the left cabinet where you thought the VFD was located.

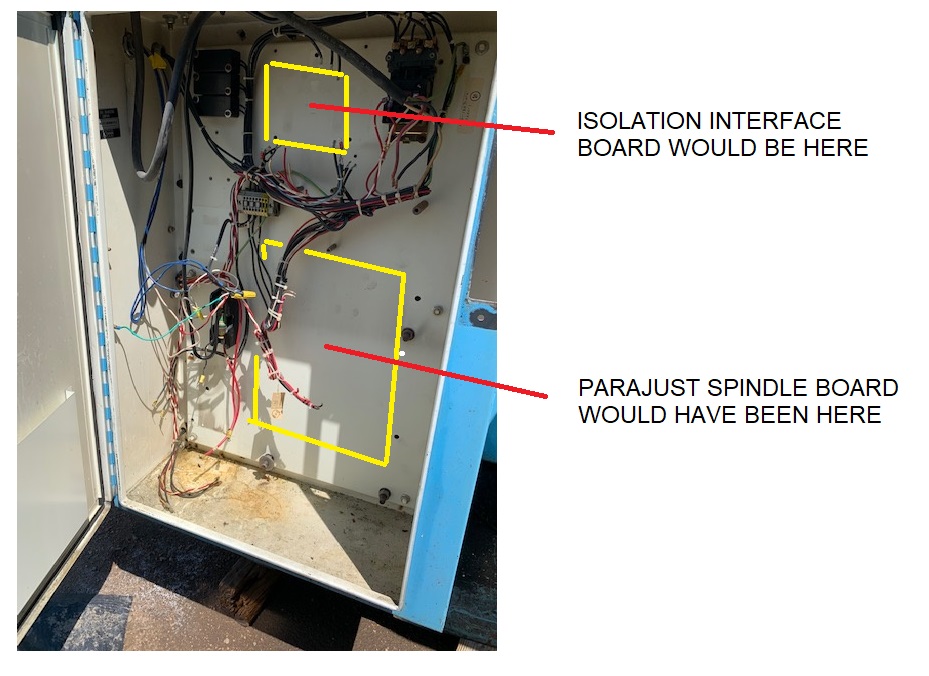
Ok my opinion is this.... after going back and looking, what I think is that the machine was totally working and still had the parajust board. I believe the parajust went out and they pulled it to get repaired and that did not pan out because of cost when they got the price from whoever that they sent it to. The reason I say this is from what the wiring looks like in it's present condition. It literally looks like they unwired and then unbolted the 2 boards. The parajust board is pretty big, and the other board above it is smaller and I can see where it was located originally. The smaller board is just a interface/isolation board, and the parajust is the spindle speed board.

It does not appear that there ever was a VFD installed. If there was, then someone sucked at their wiring and left a lot of hot wires siting open.

I fully believe the parajust went out, they pulled both boards thinking it was either of the two as the spindle control was giving them problems and the rest of the machine is fully operational. I would isolate the wiring in that left cabinet, check the step down transformer input to see if wired 220 or 440, and put power to the cabinet and see if it fires up. i really am starting to believe the everything else is fine. This would make sense as what would happen is some shop was tight on money. They pulled the board, or a service guy pulled it and they had the intention to fix the board. When they got the price, they balked at fixing it as it would probably have cost a couple of thousand for the total repair. And they had no clue how to wire in and implement a traditional VFD as the parajust wiring would have stumped them, so the final outcome was it sat until they got rid of it. In other words from a business standpoint, in their eyes the machine was not worth fixing as it was good money thrown after bad in a old machine when they could invest that money in a new or newer machine. I think it has been sitting in that condition for awhile, but if you isolate the parajust board wiring that you could possibly get it fired up pretty easy to check the servos.

Here is your picture where the boards would have been. Will find some pics of real thing.


I will be back in a bit, wanted to get that on to you so you could be thinking about it. Still have a lot to get done in order to send you more pics and info, but working on it.

Robert
Last edit: 6 years 2 months ago by CORBETT. Reason: spelling

Please Log in or Create an account to join the conversation.

More
6 years 2 months ago #177335 by CORBETT
Replied by CORBETT on topic Hurco KMB-IS CNC update

Leith

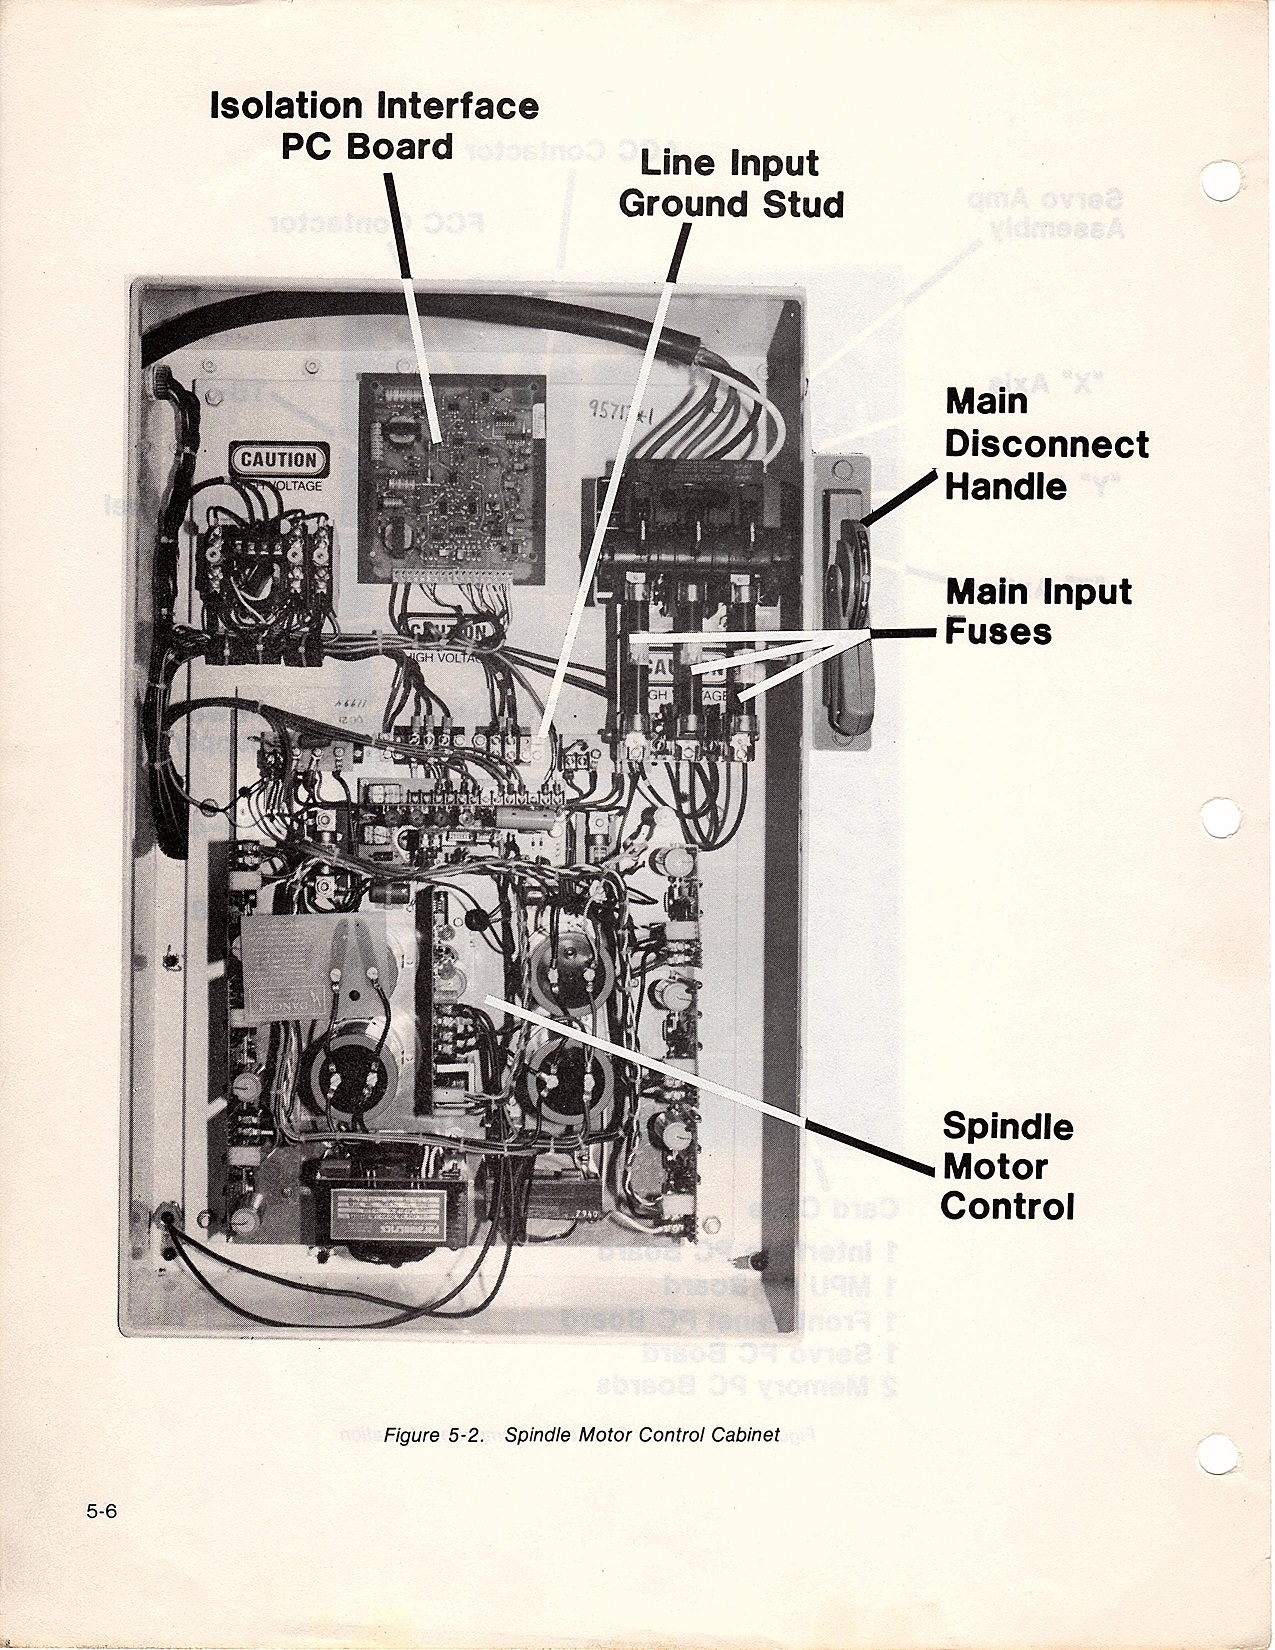
Ok here is one page out of my 1981 manual.

It looks a tiny bit different, but you get the idea. I will try to find one of your machine.


Please Log in or Create an account to join the conversation.

Time to create page: 0.448 seconds
Powered by Kunena Forum