Optimum Optimill MH50V CNC conversion

More
2 years 8 months ago #293696 by Unlogic
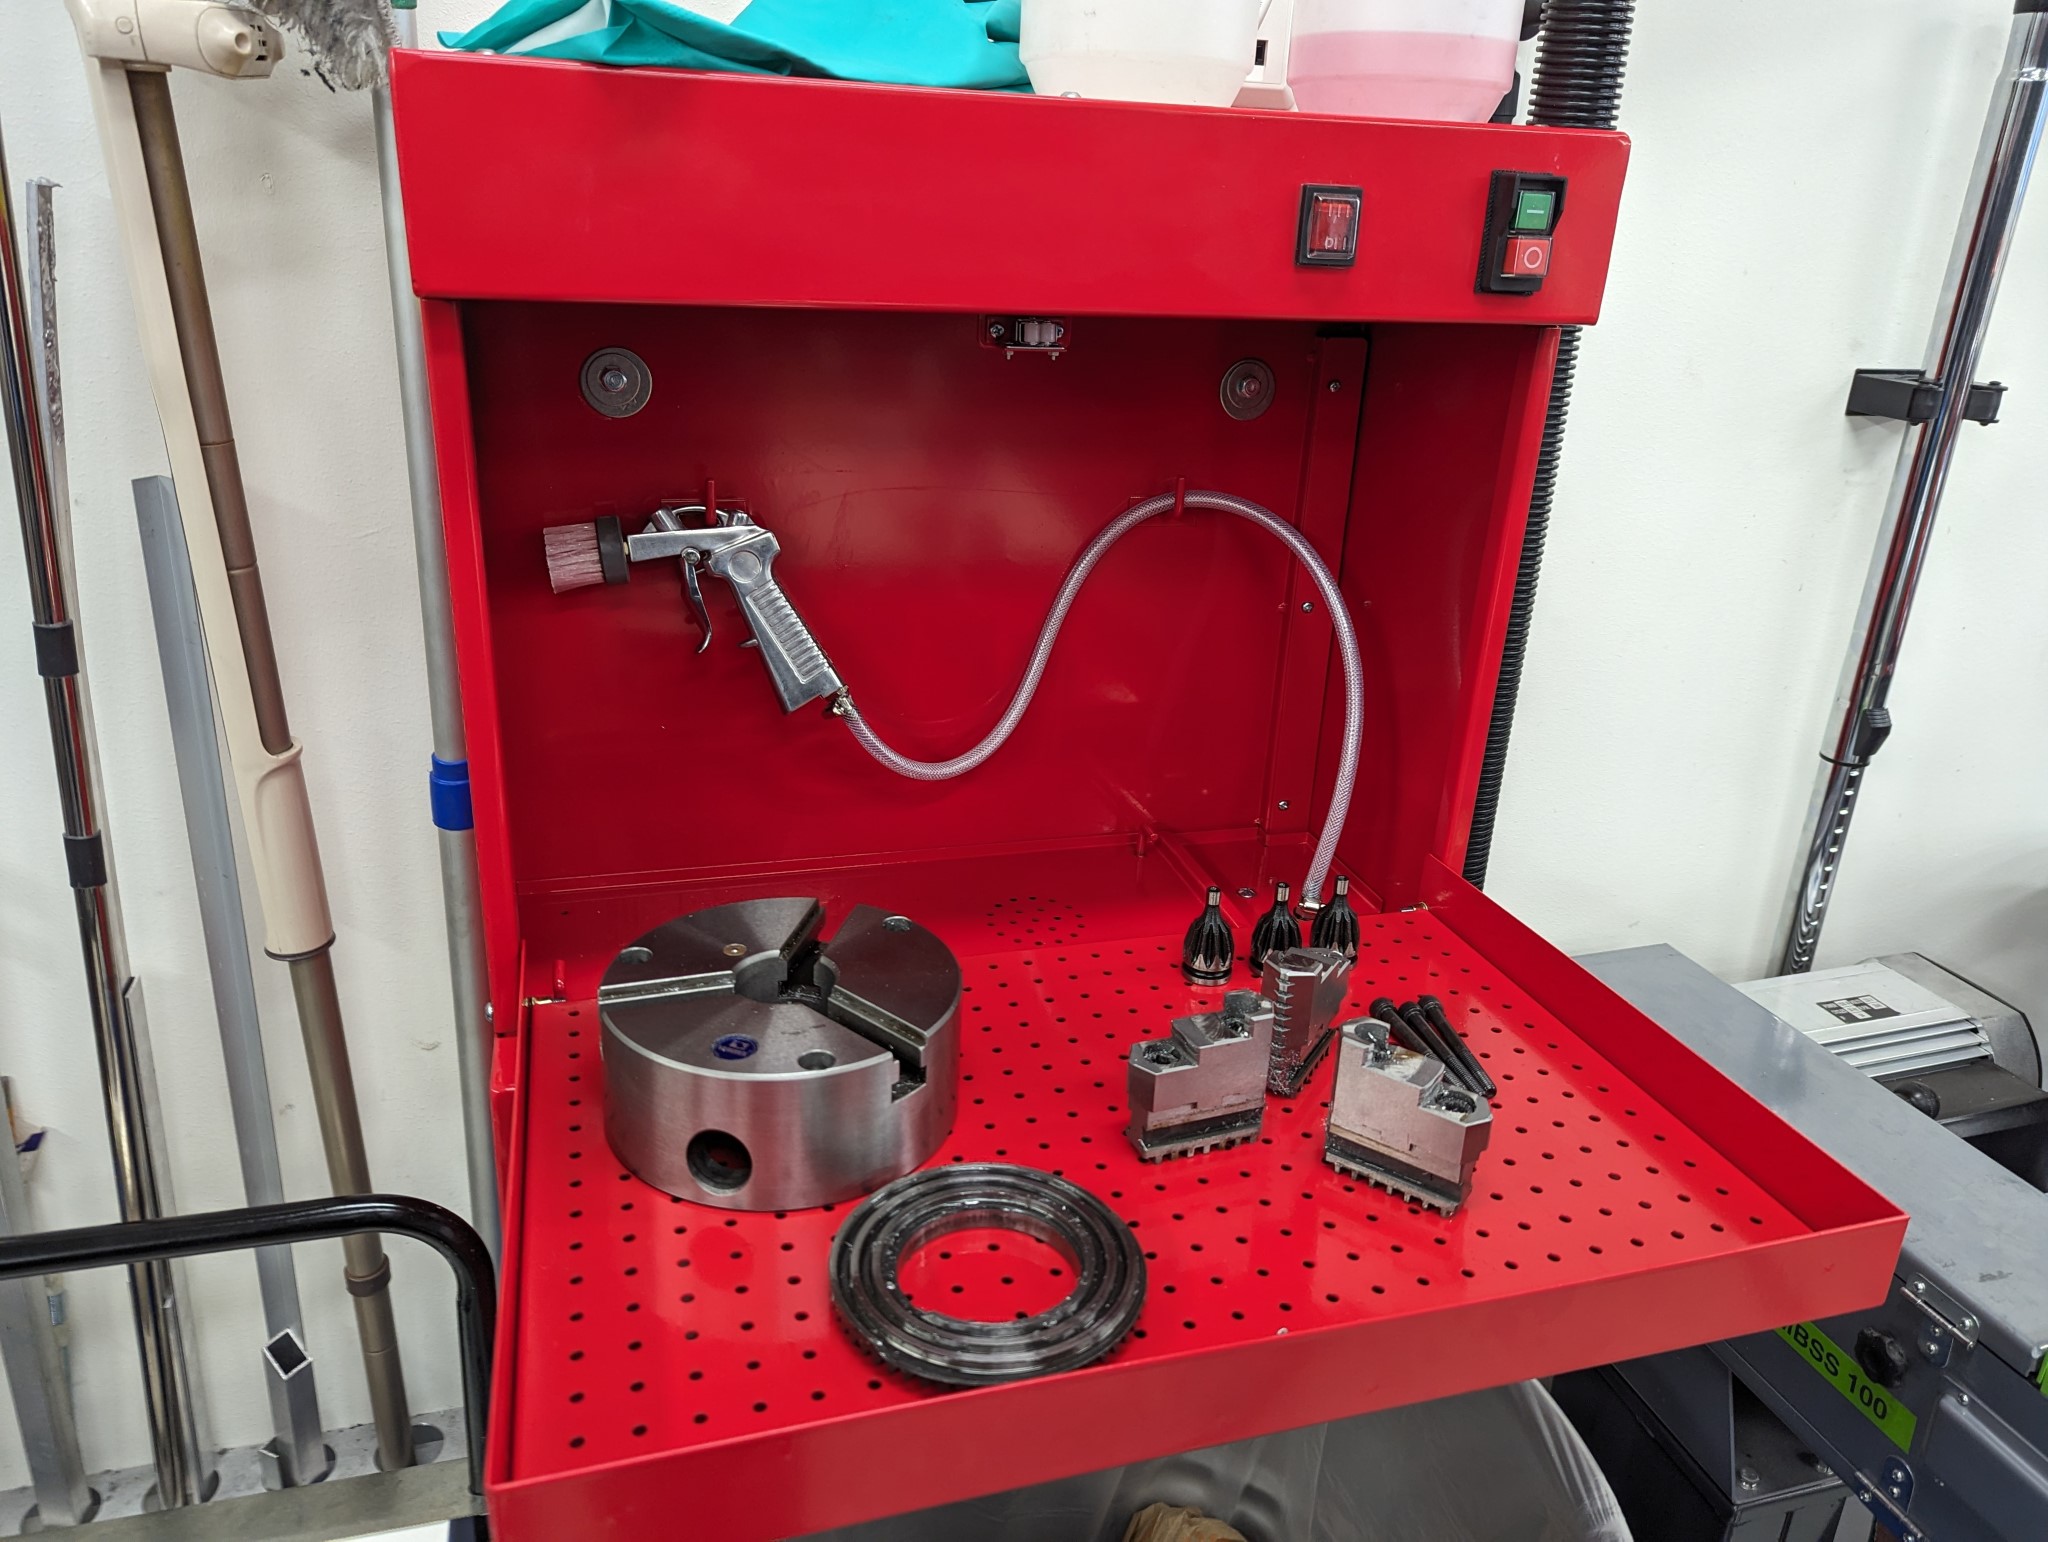
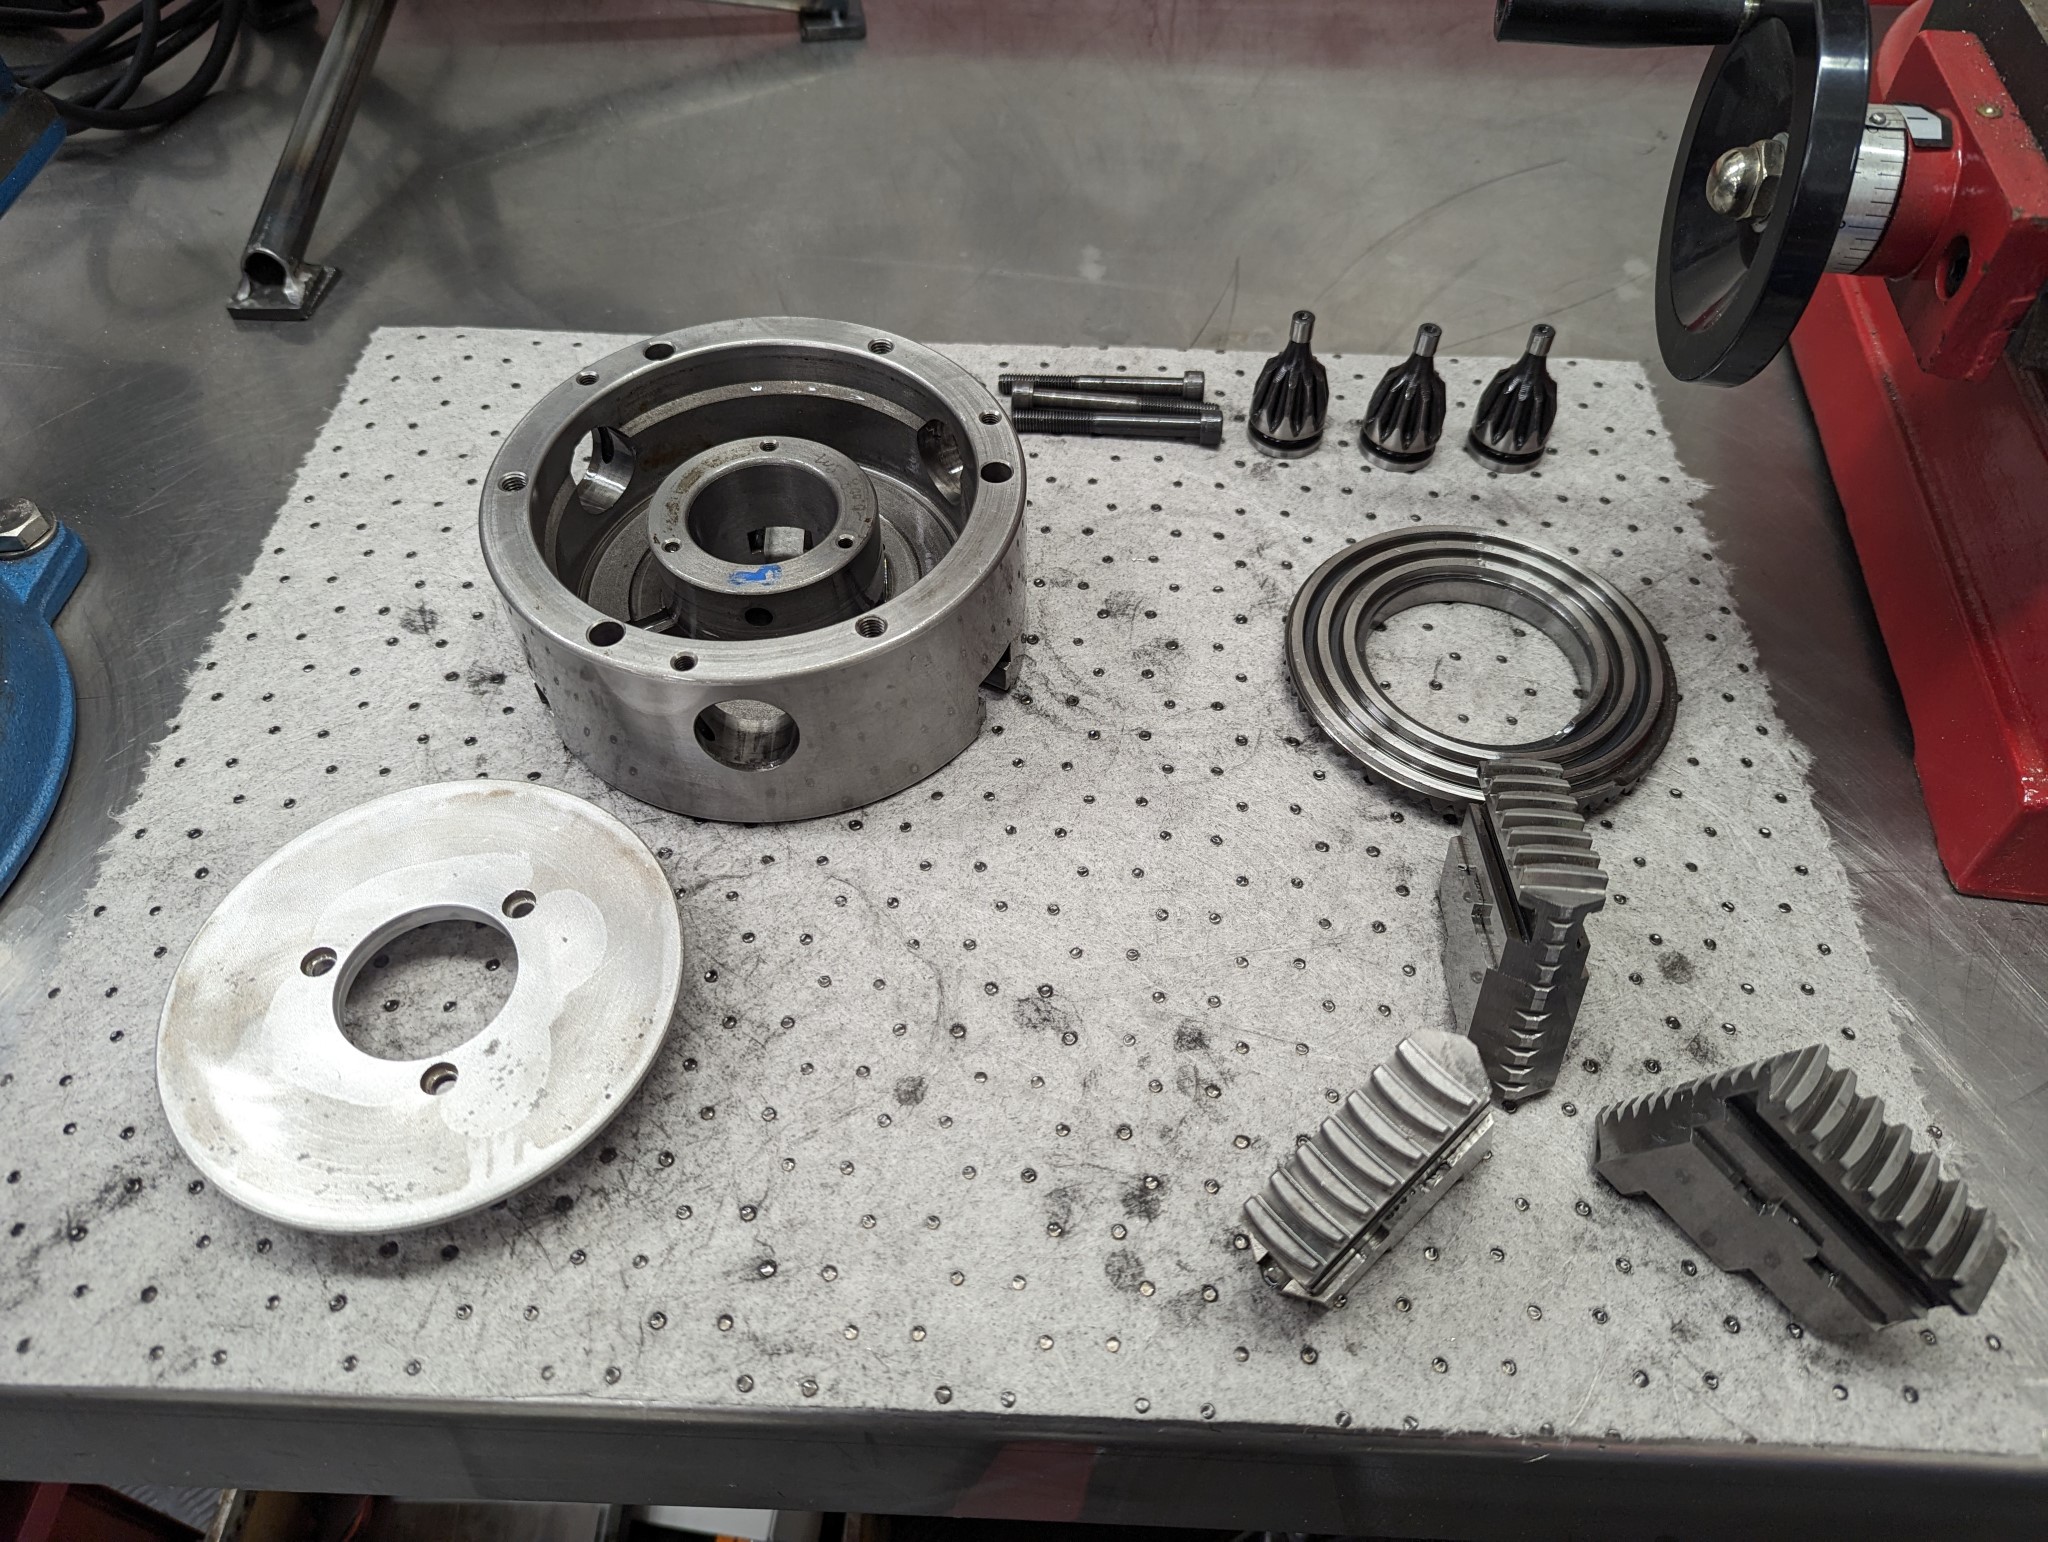
I had to use a very small depth of cut when making the center holes in the pulleys which caused very nasty dust like chips to form. The FogBuster blew those chips into the internals of the chuck on my rotary table. So when I was done with the pulleys I had to take the chuck apart and give it a through clean in the parts cleaner...


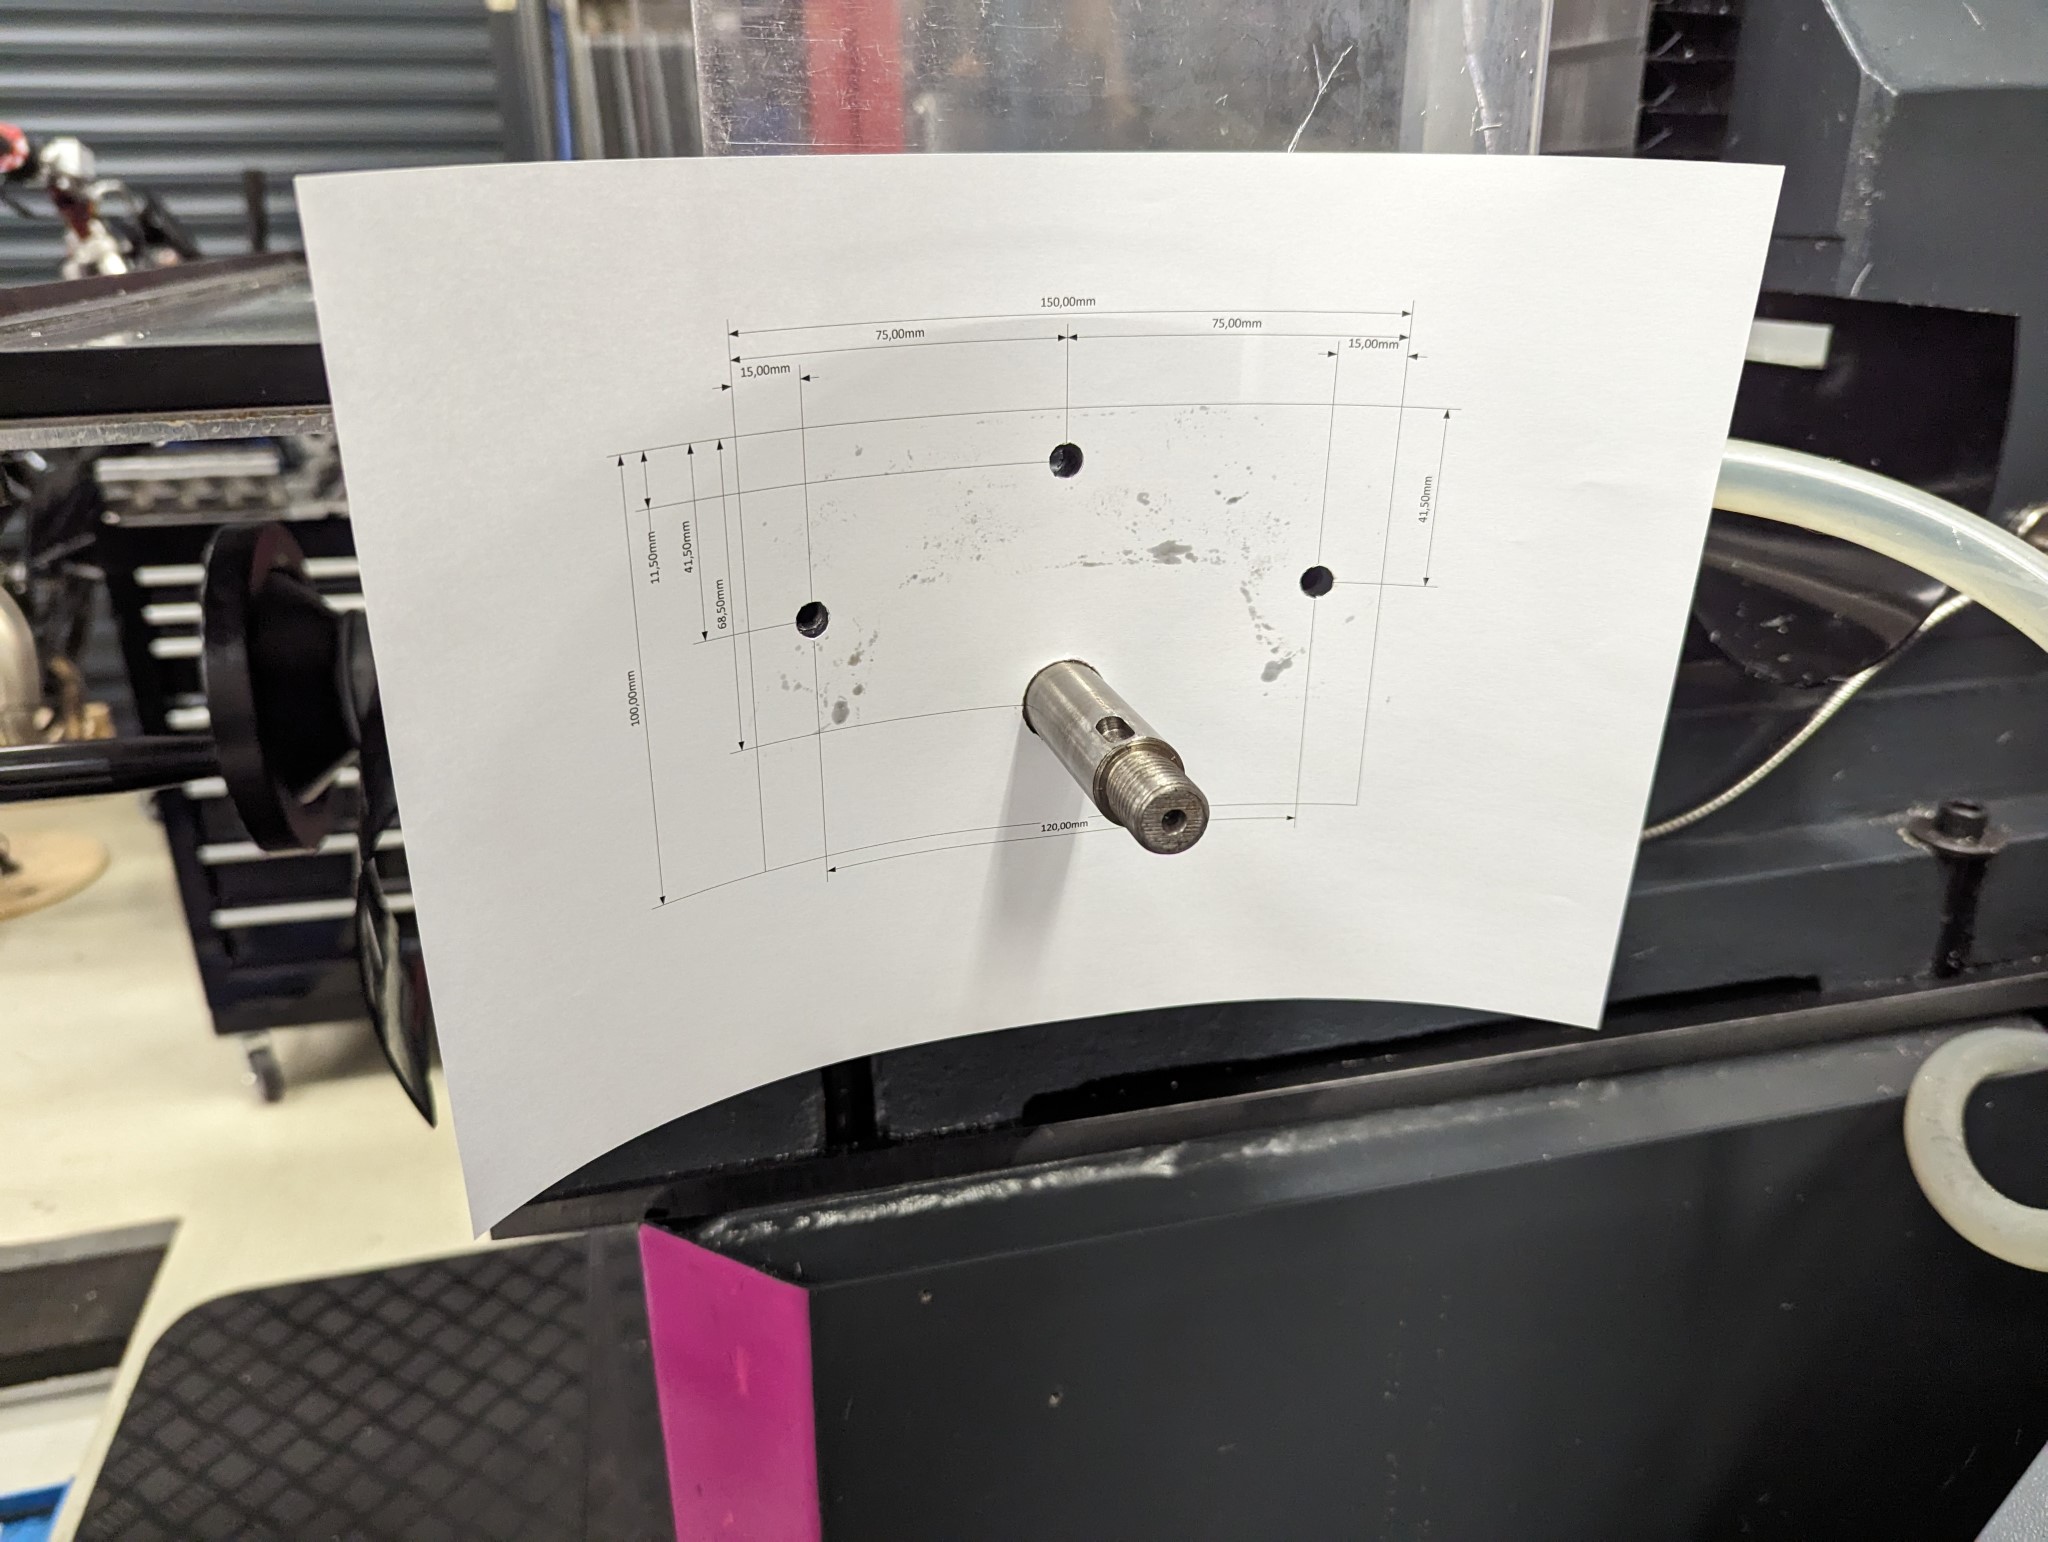
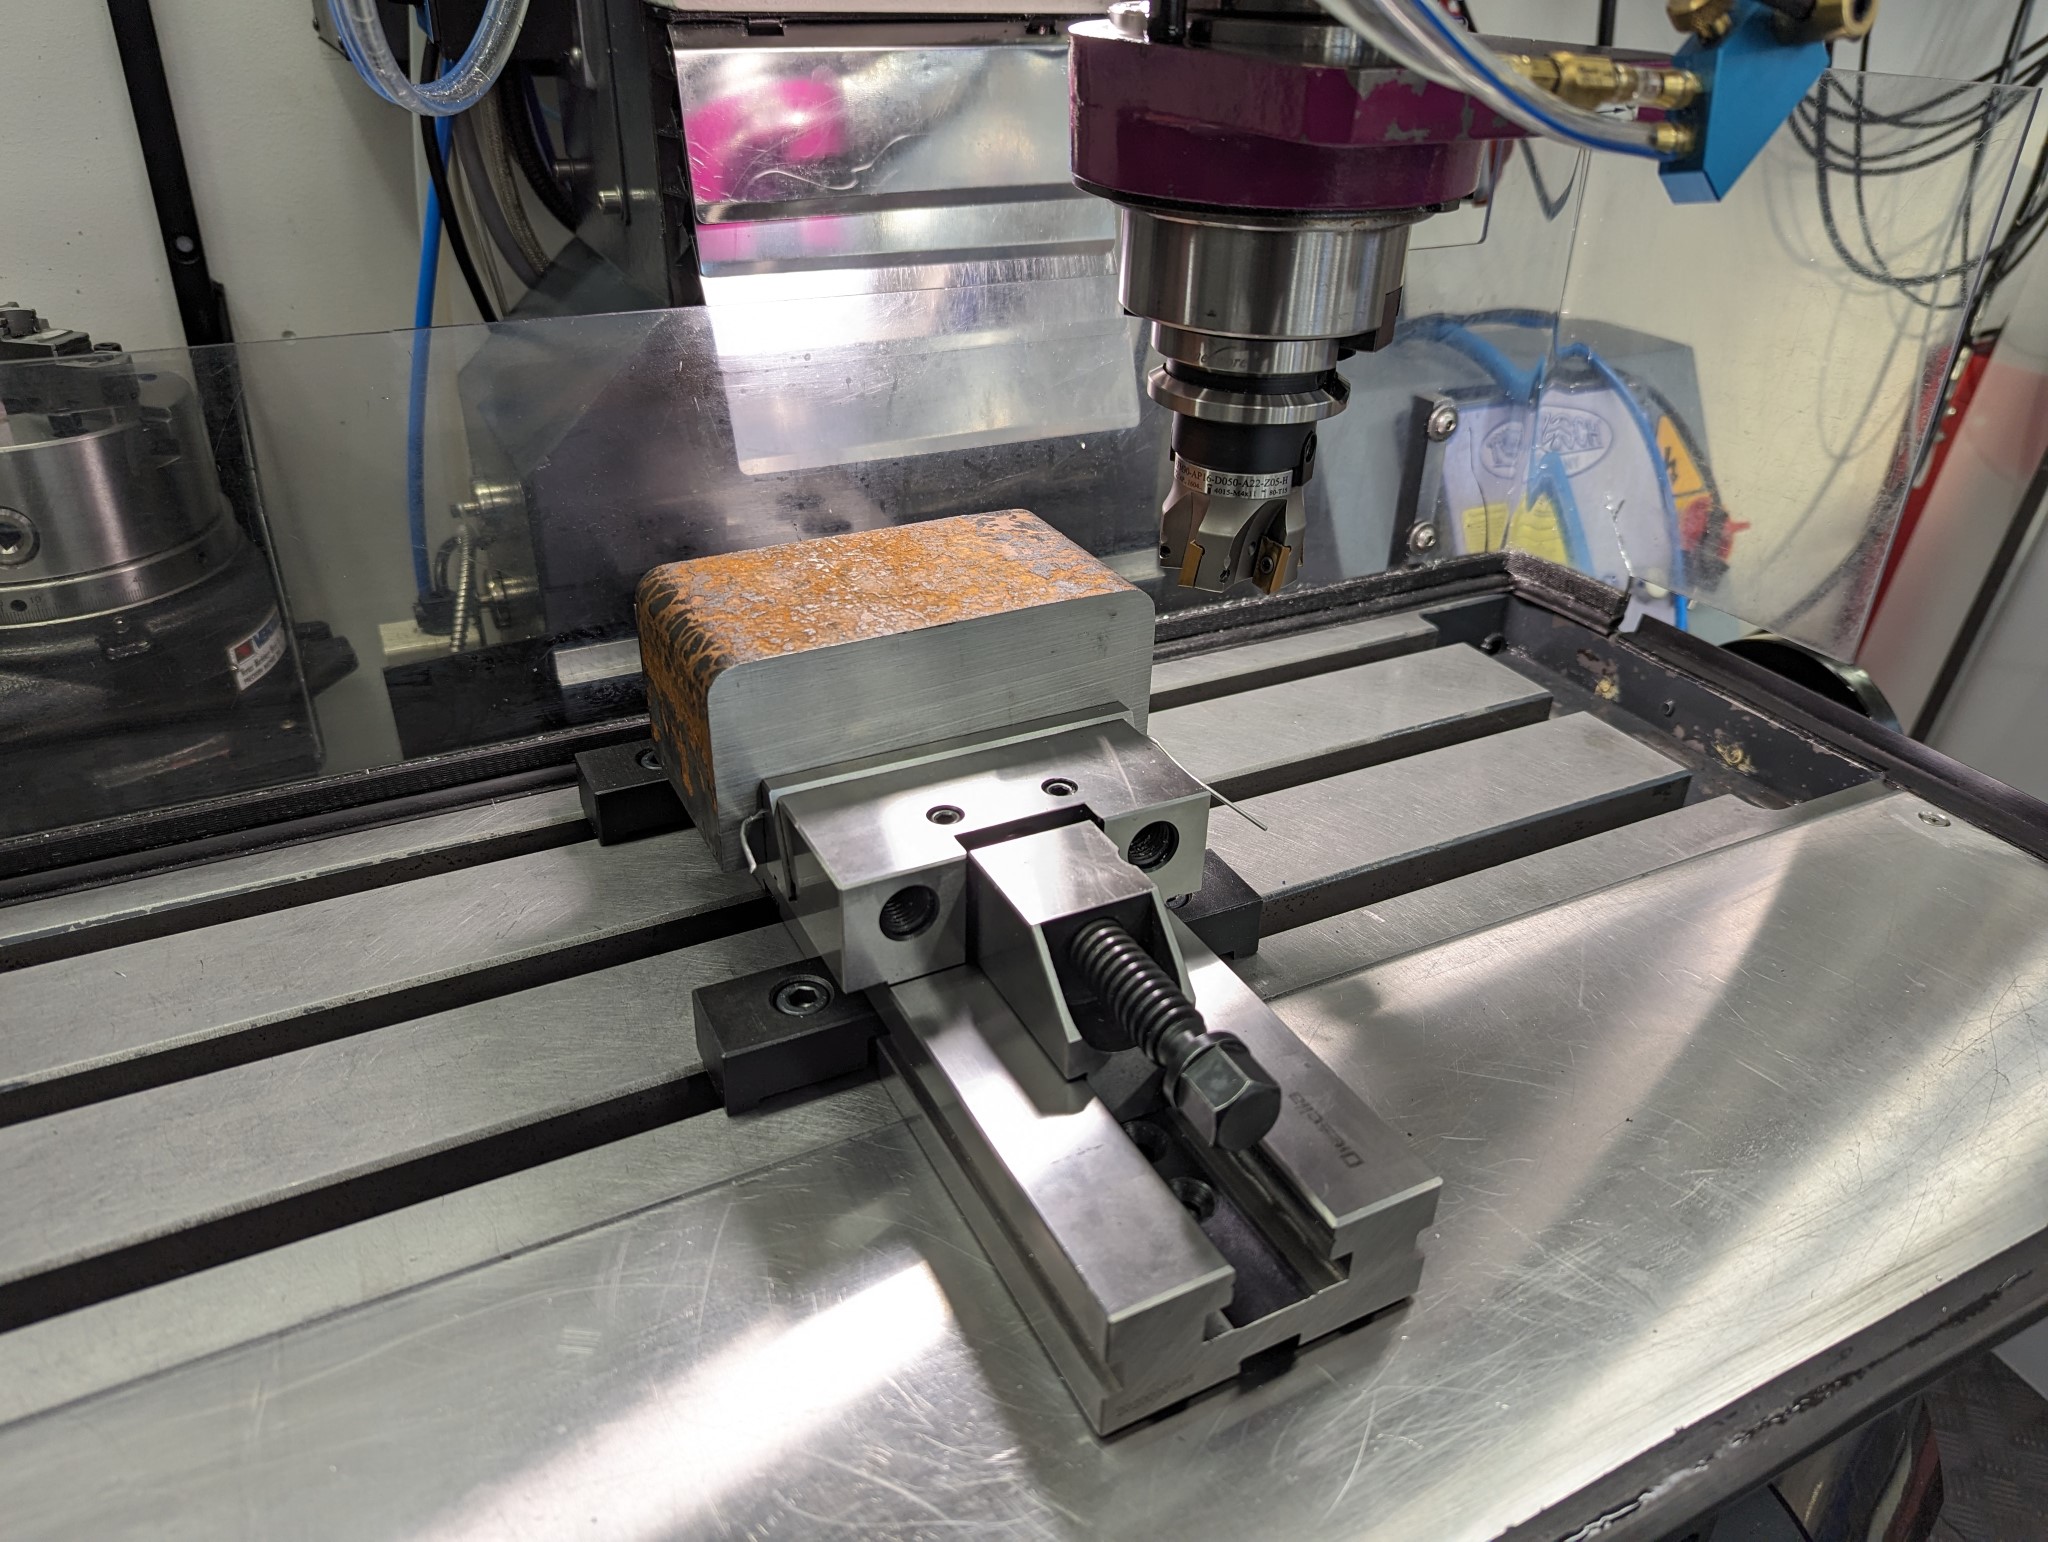
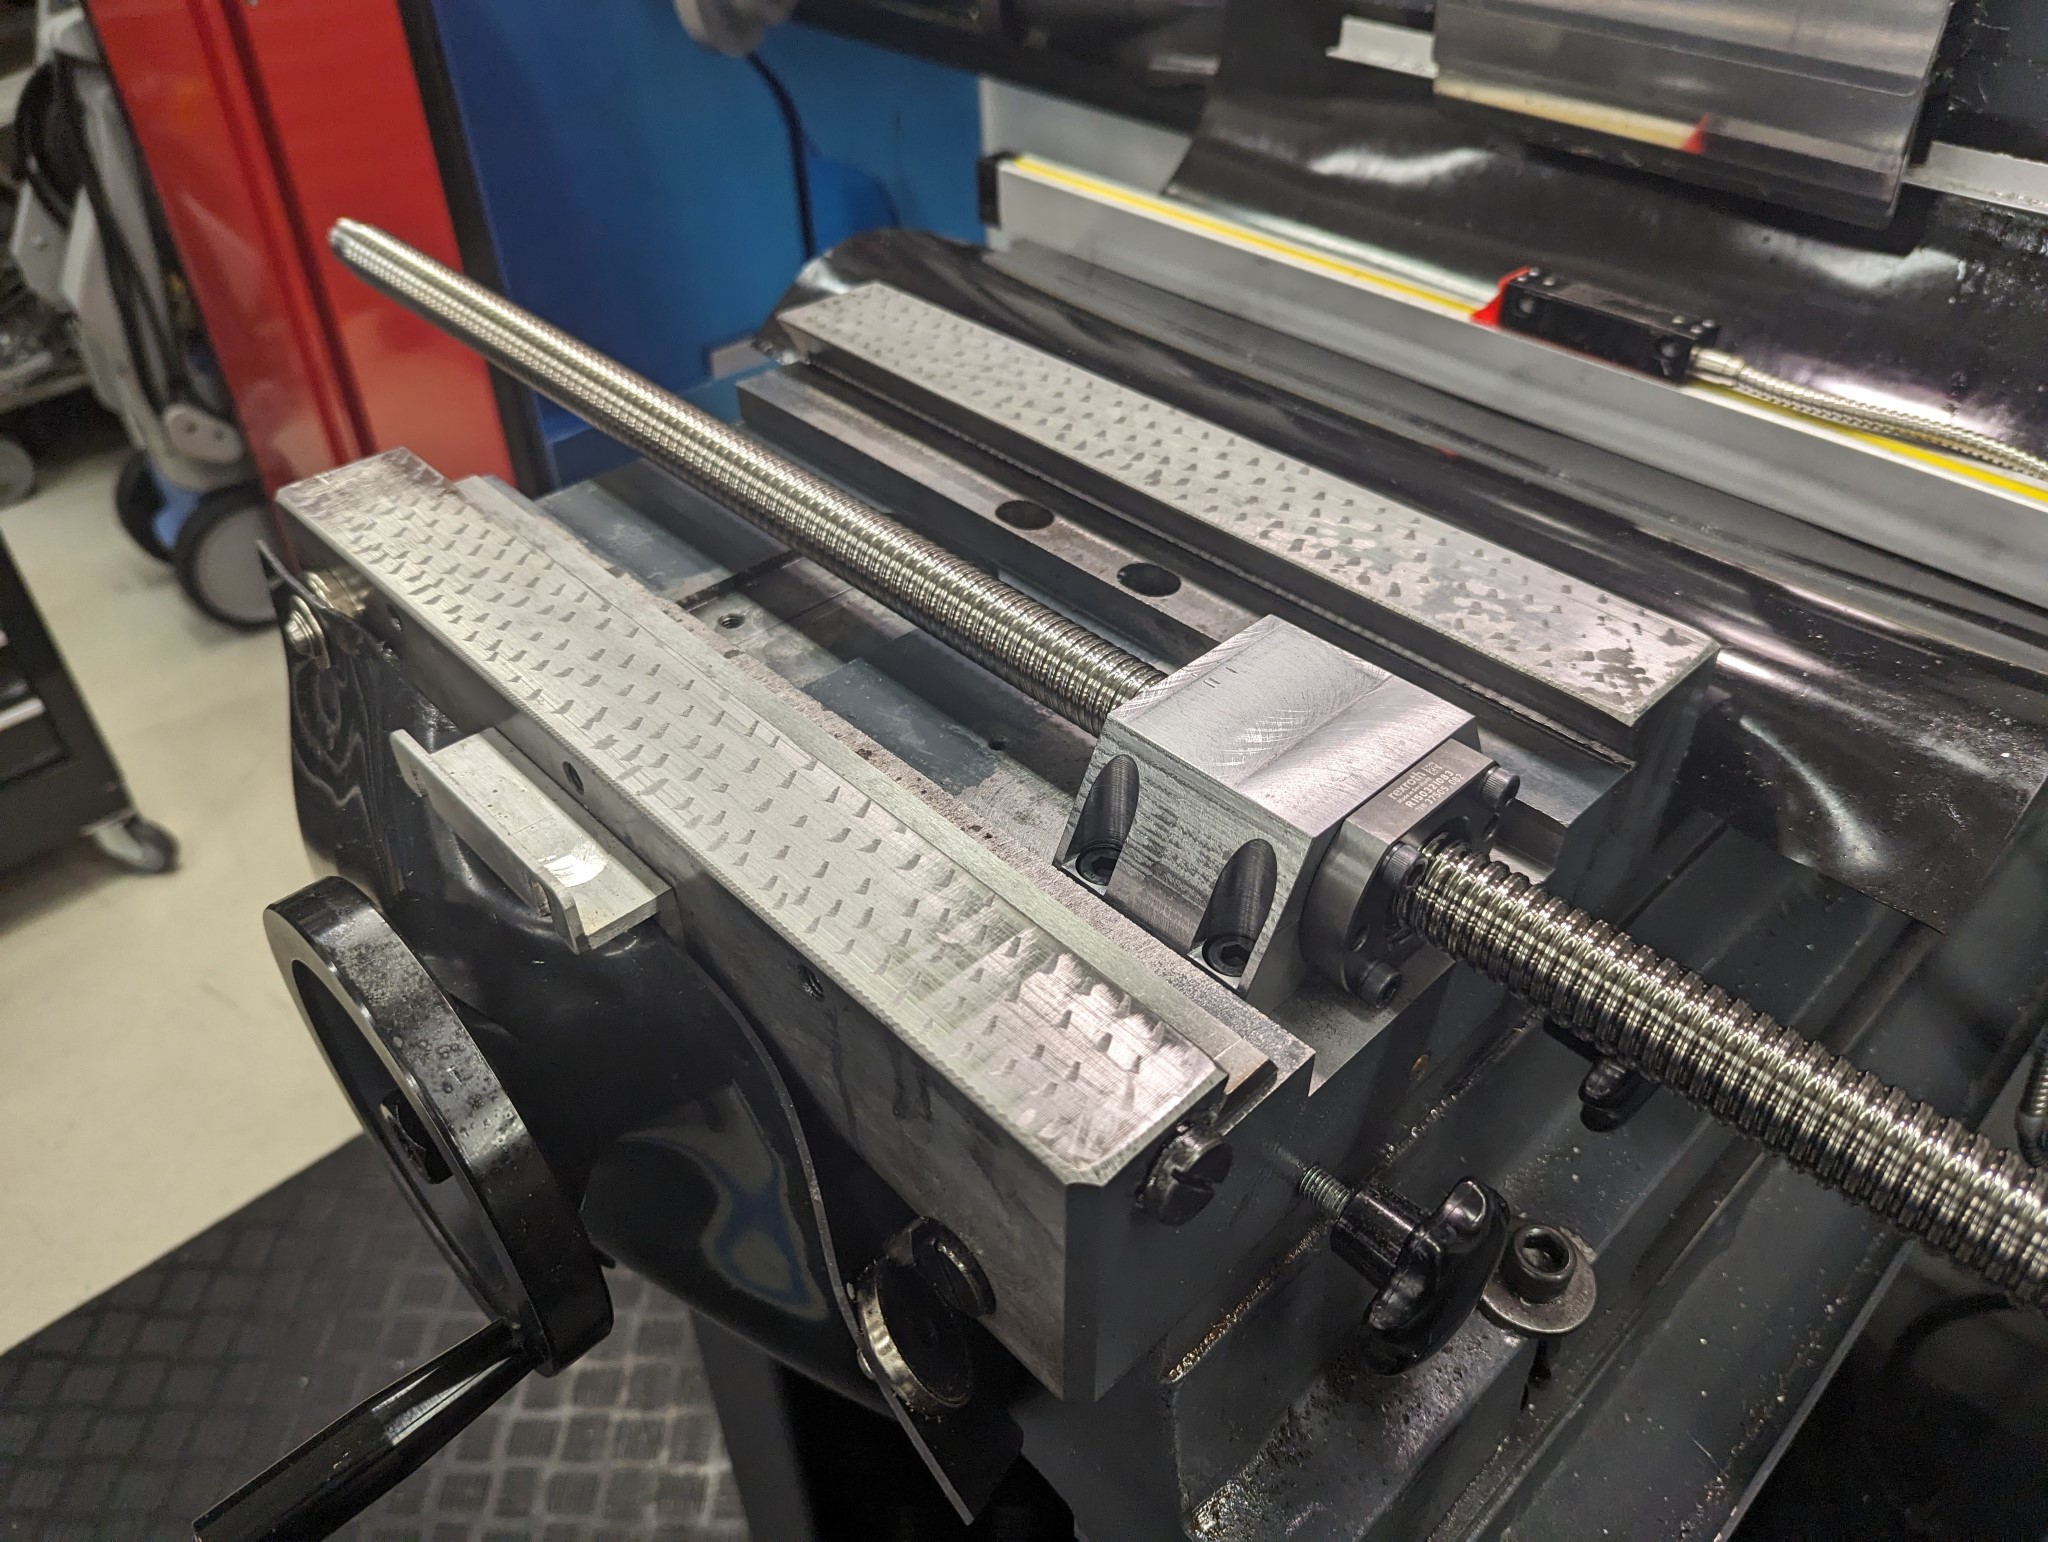
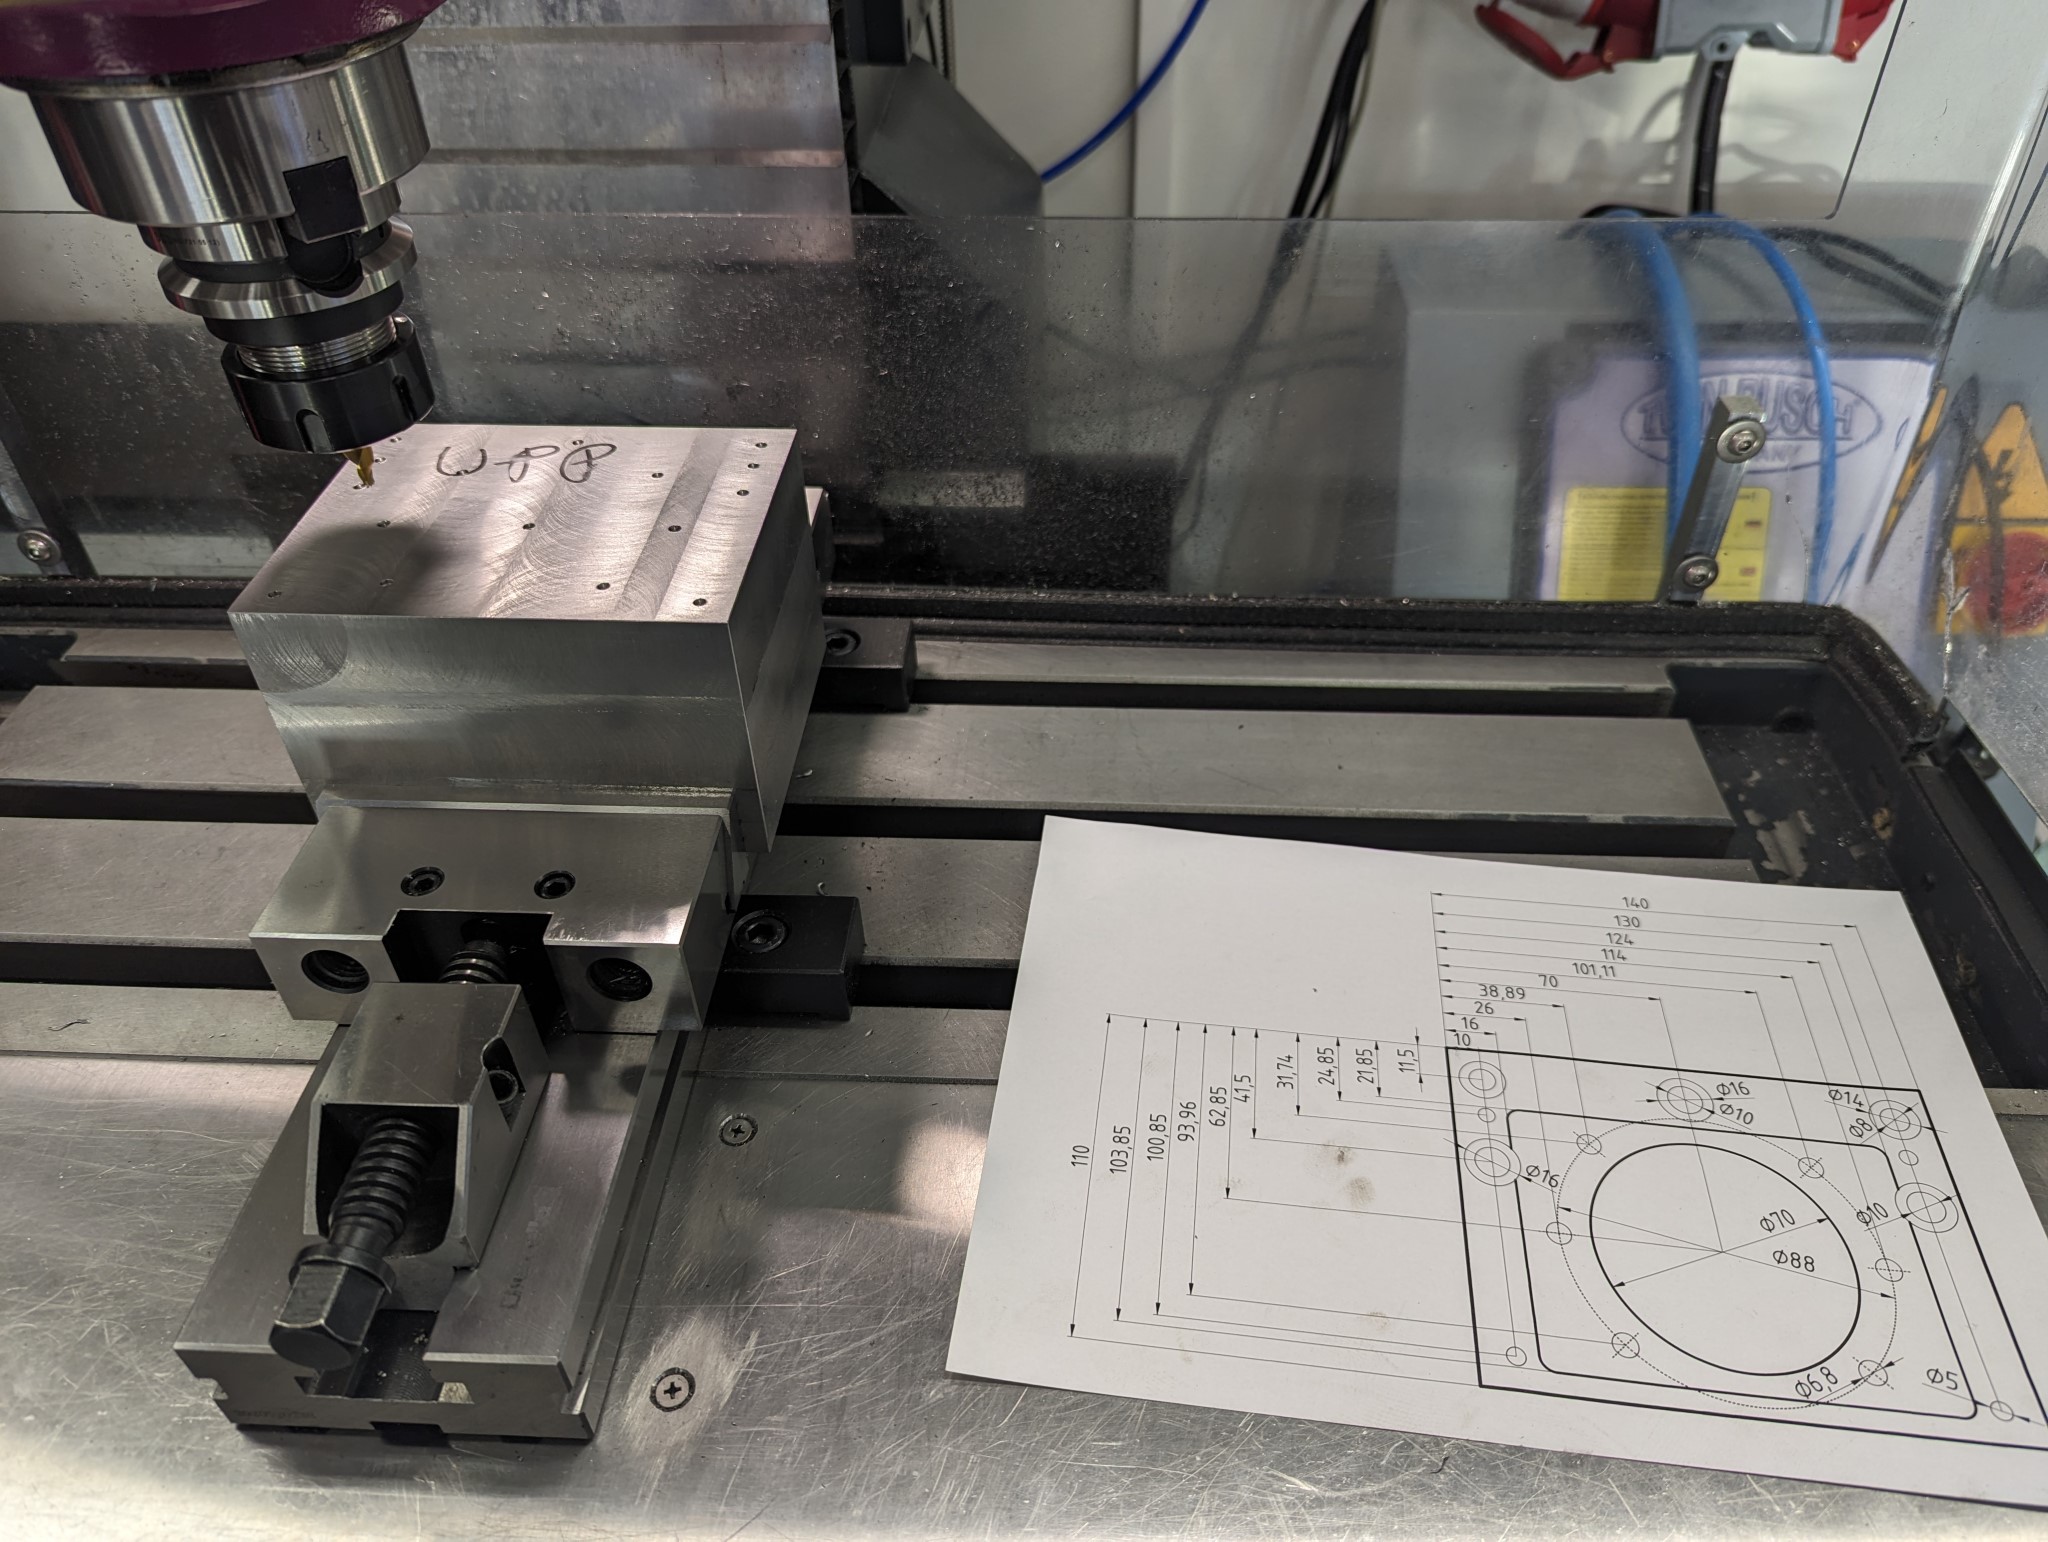
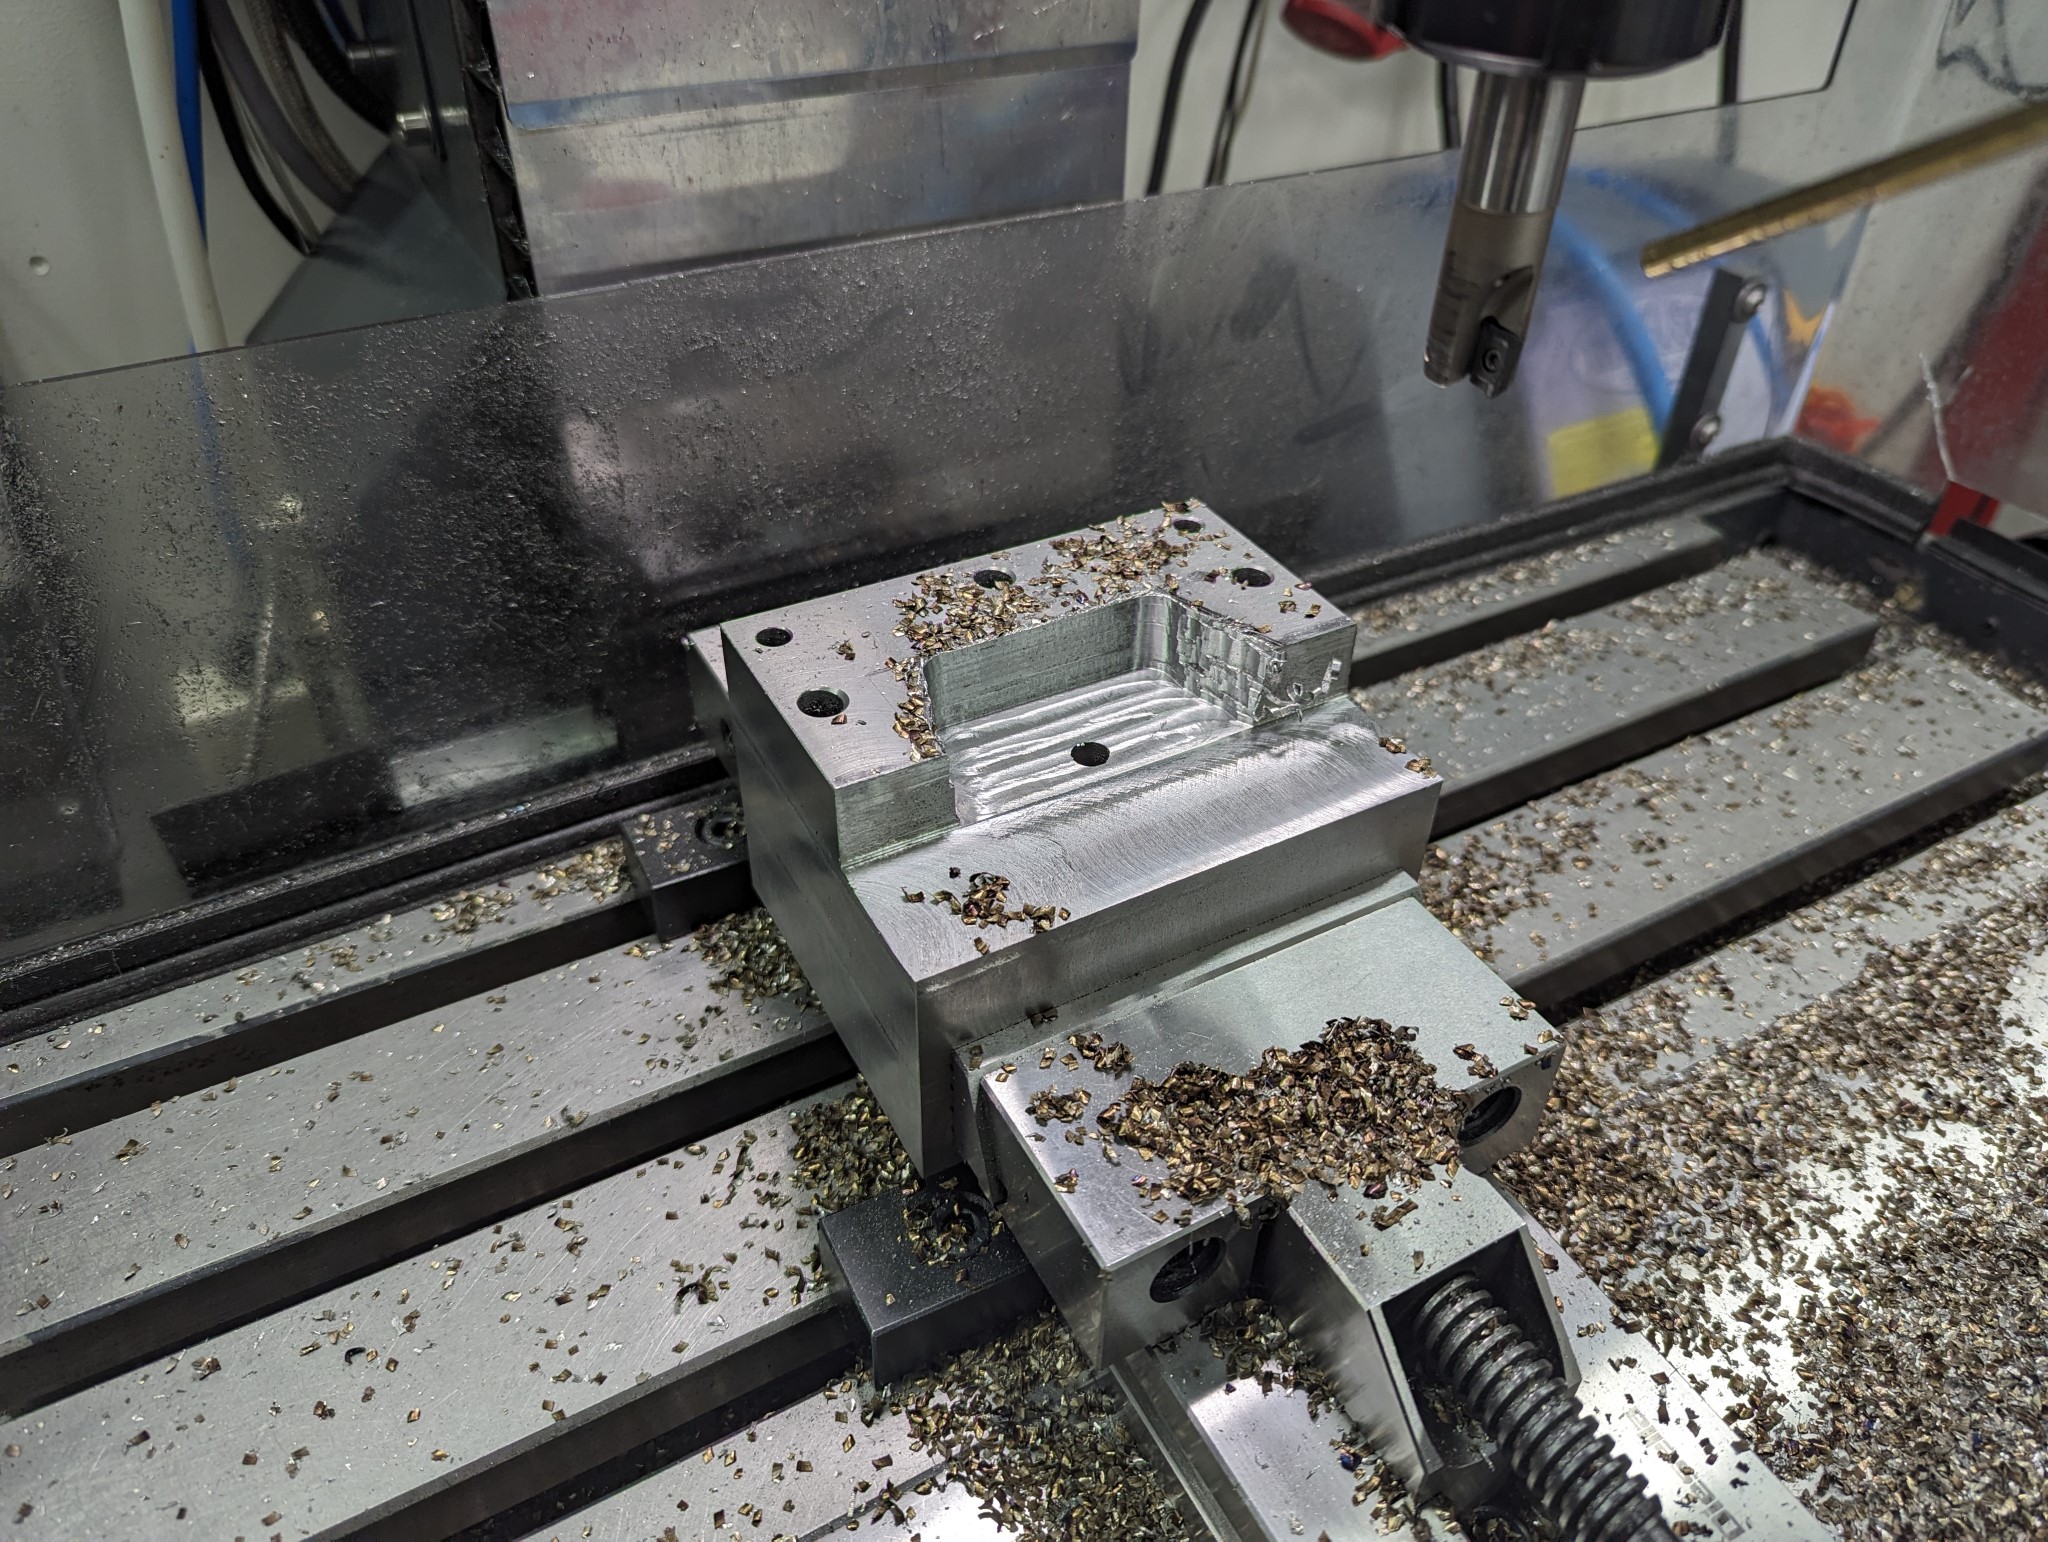
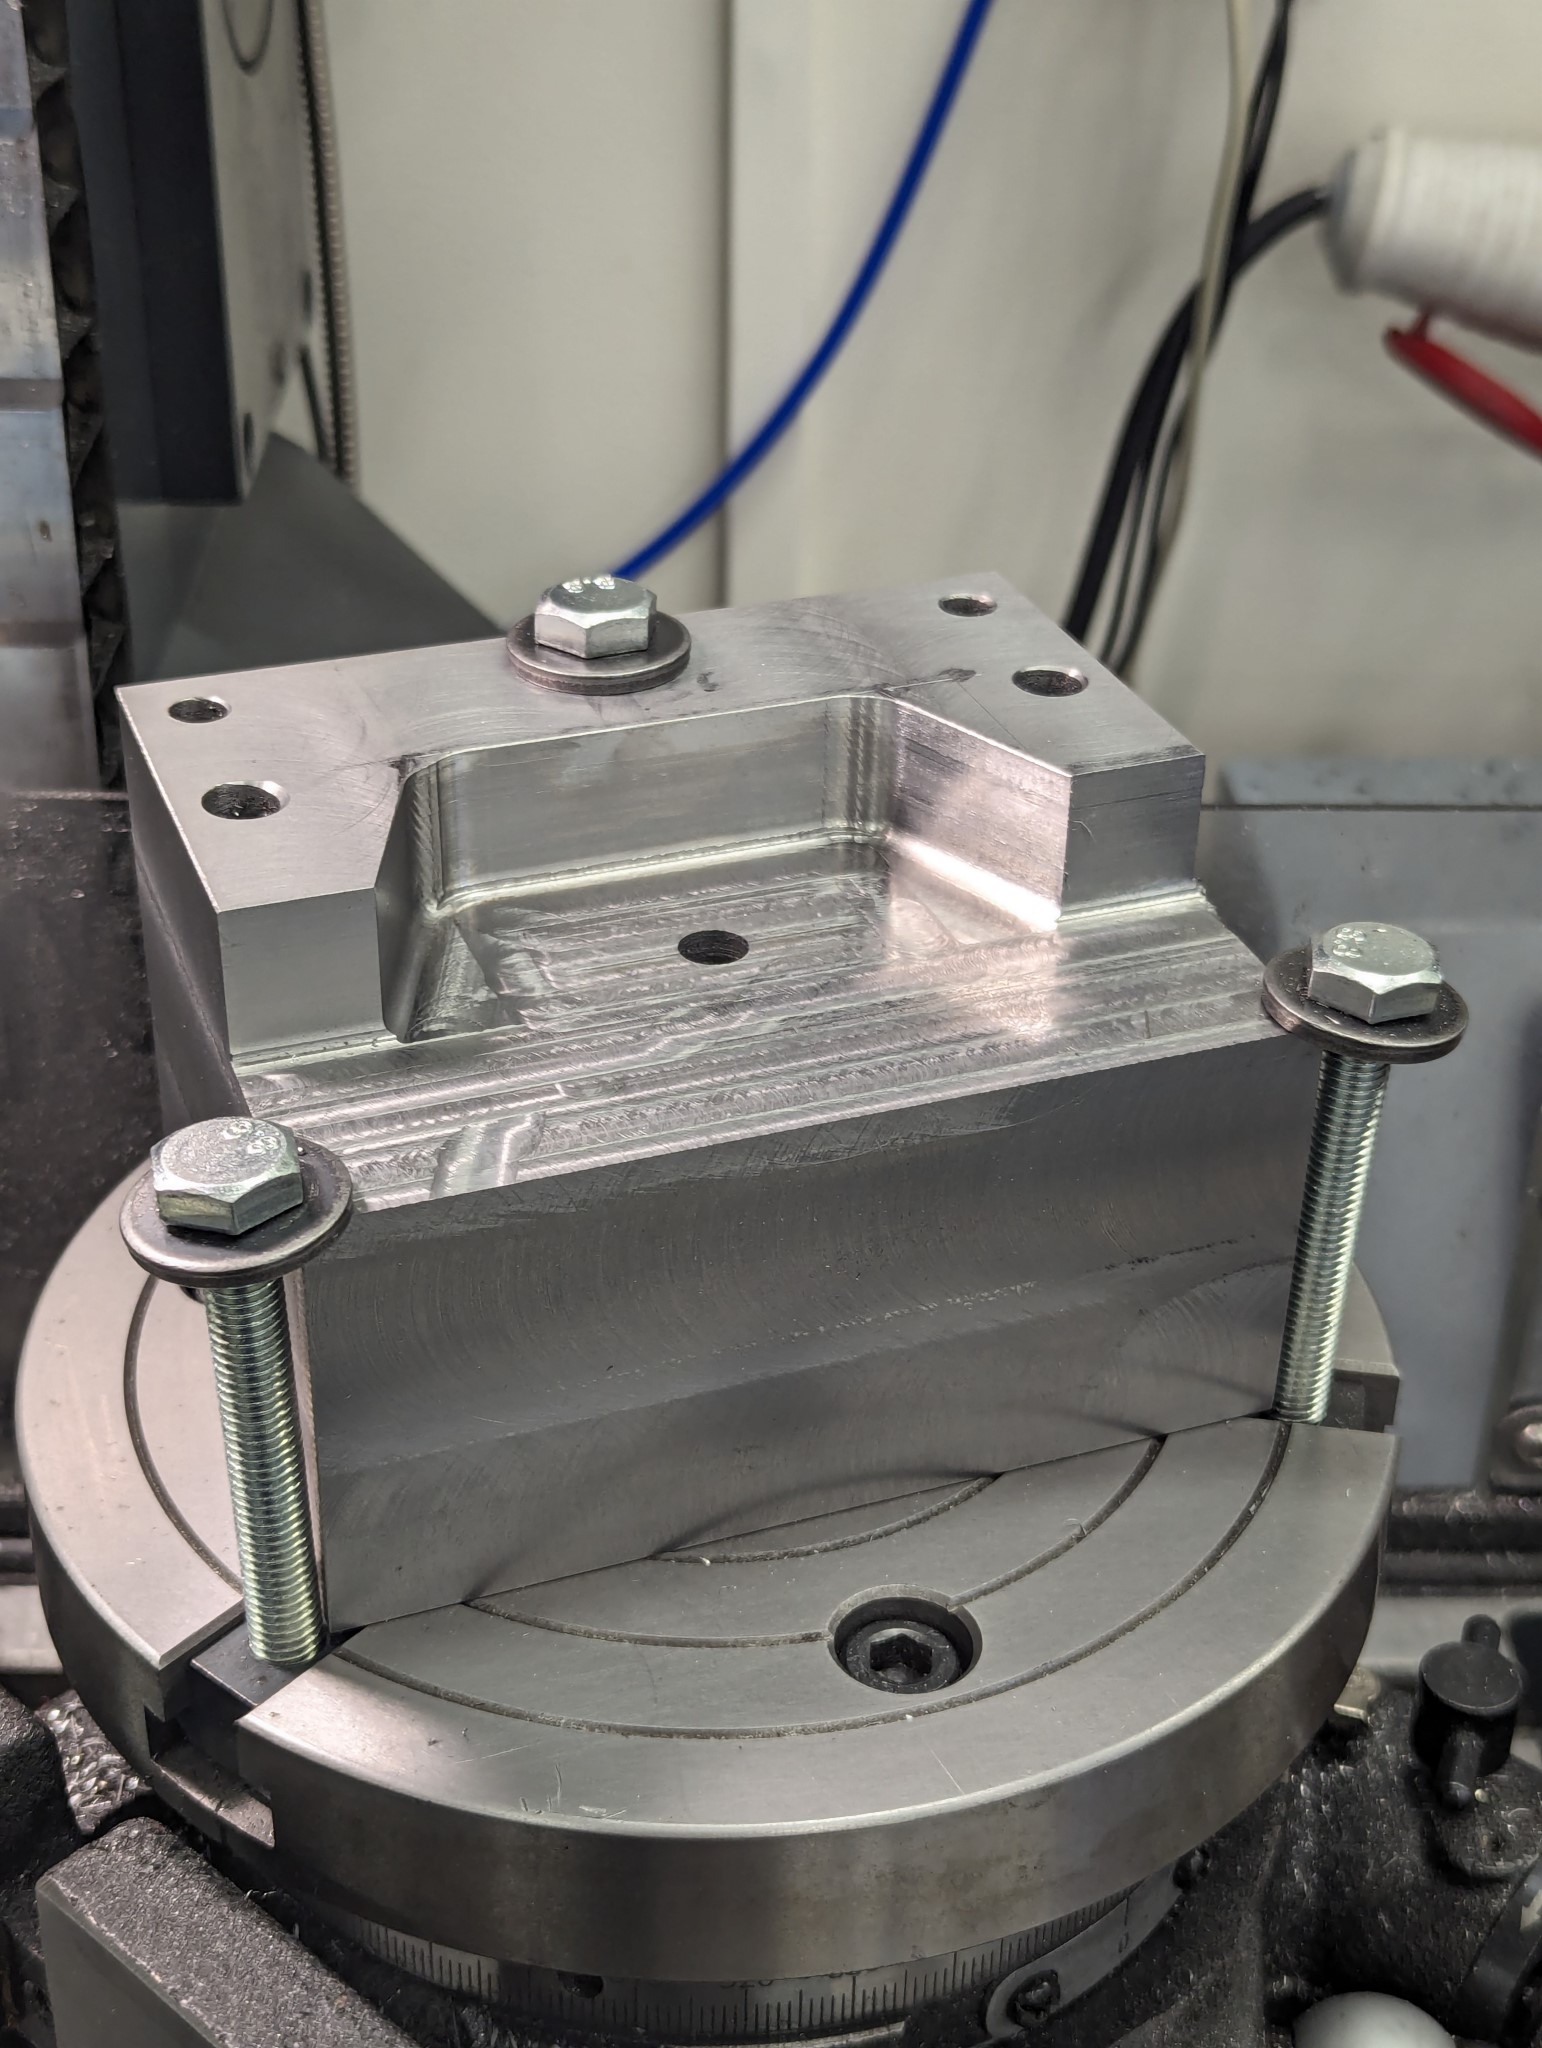
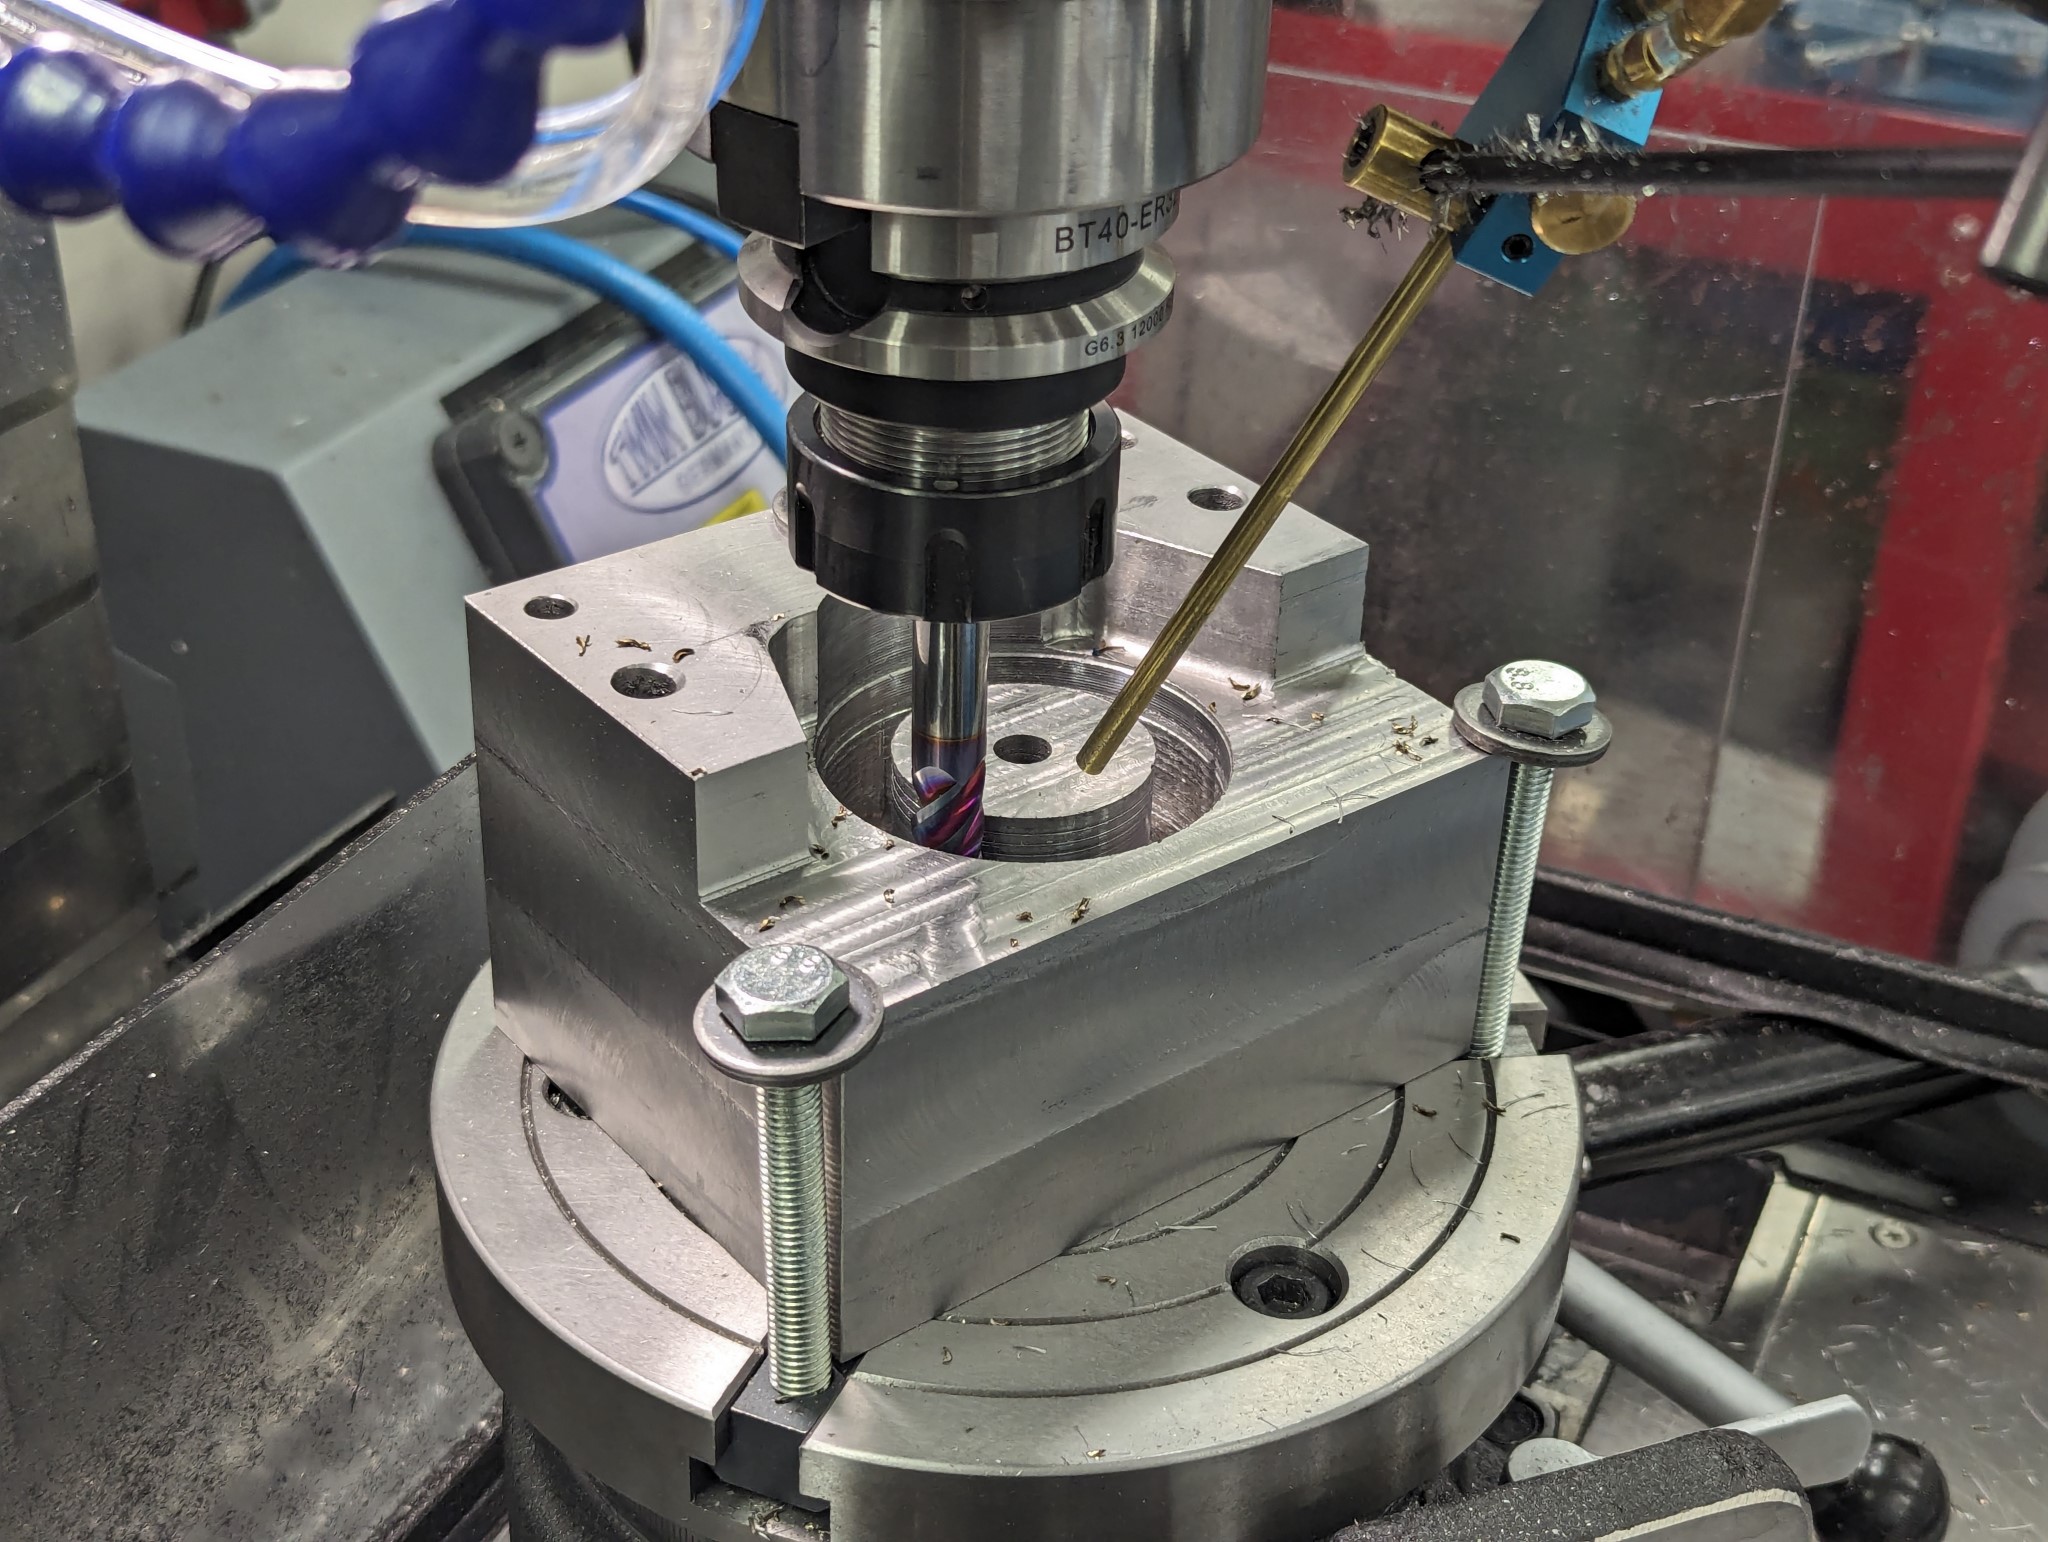
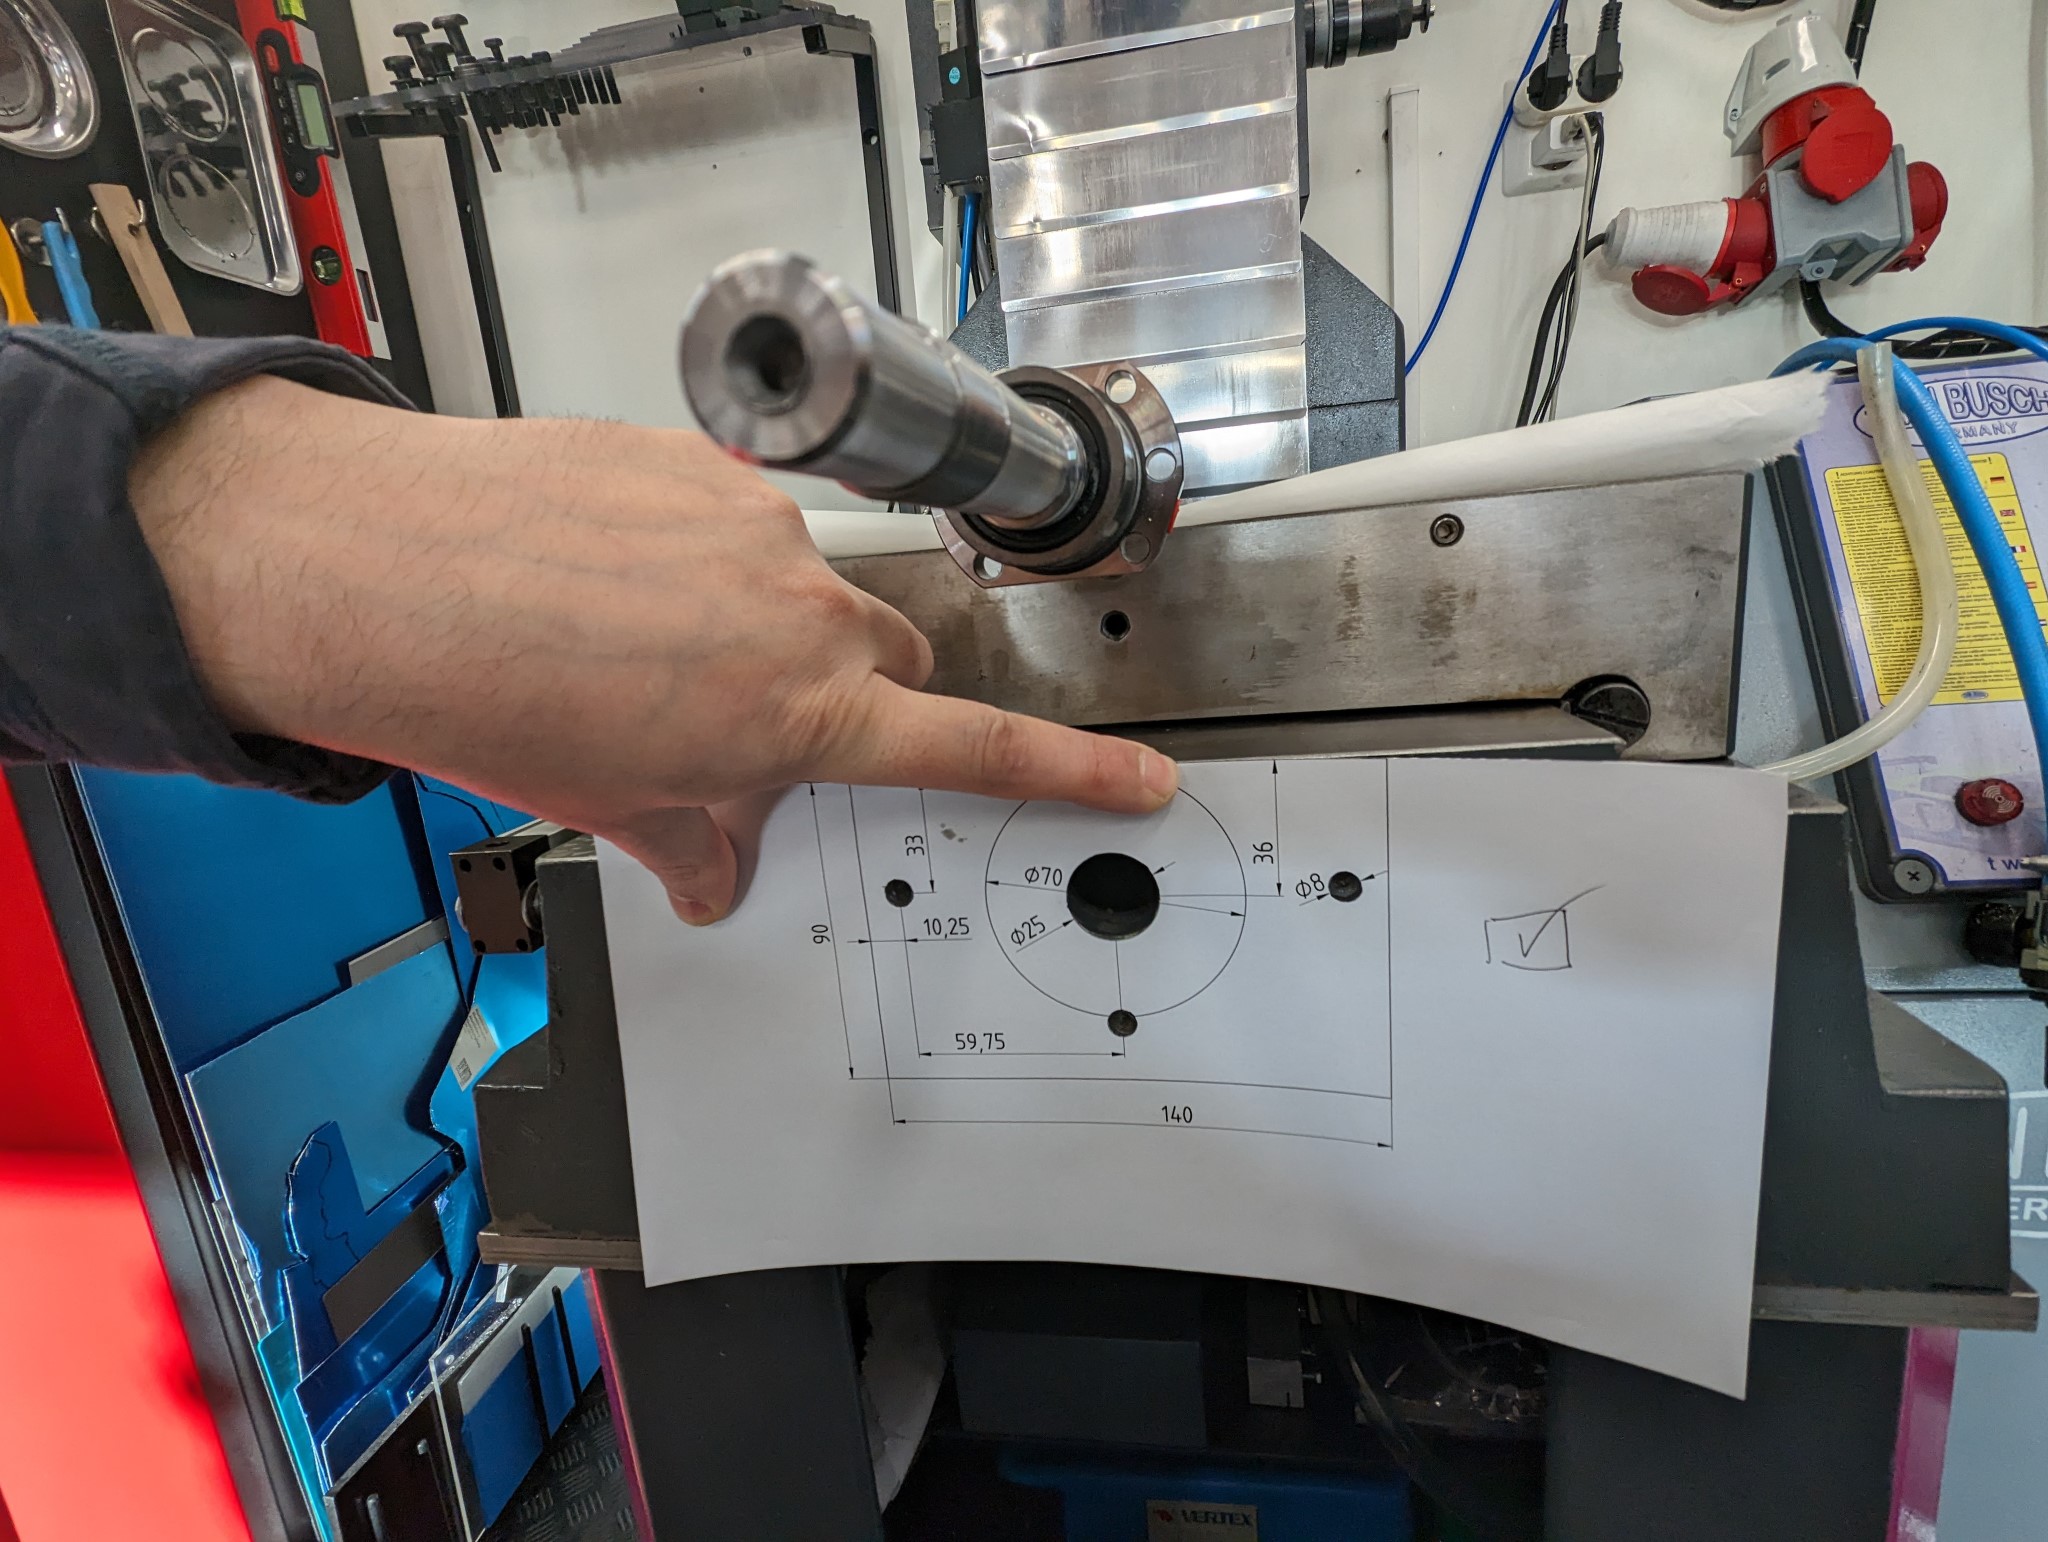
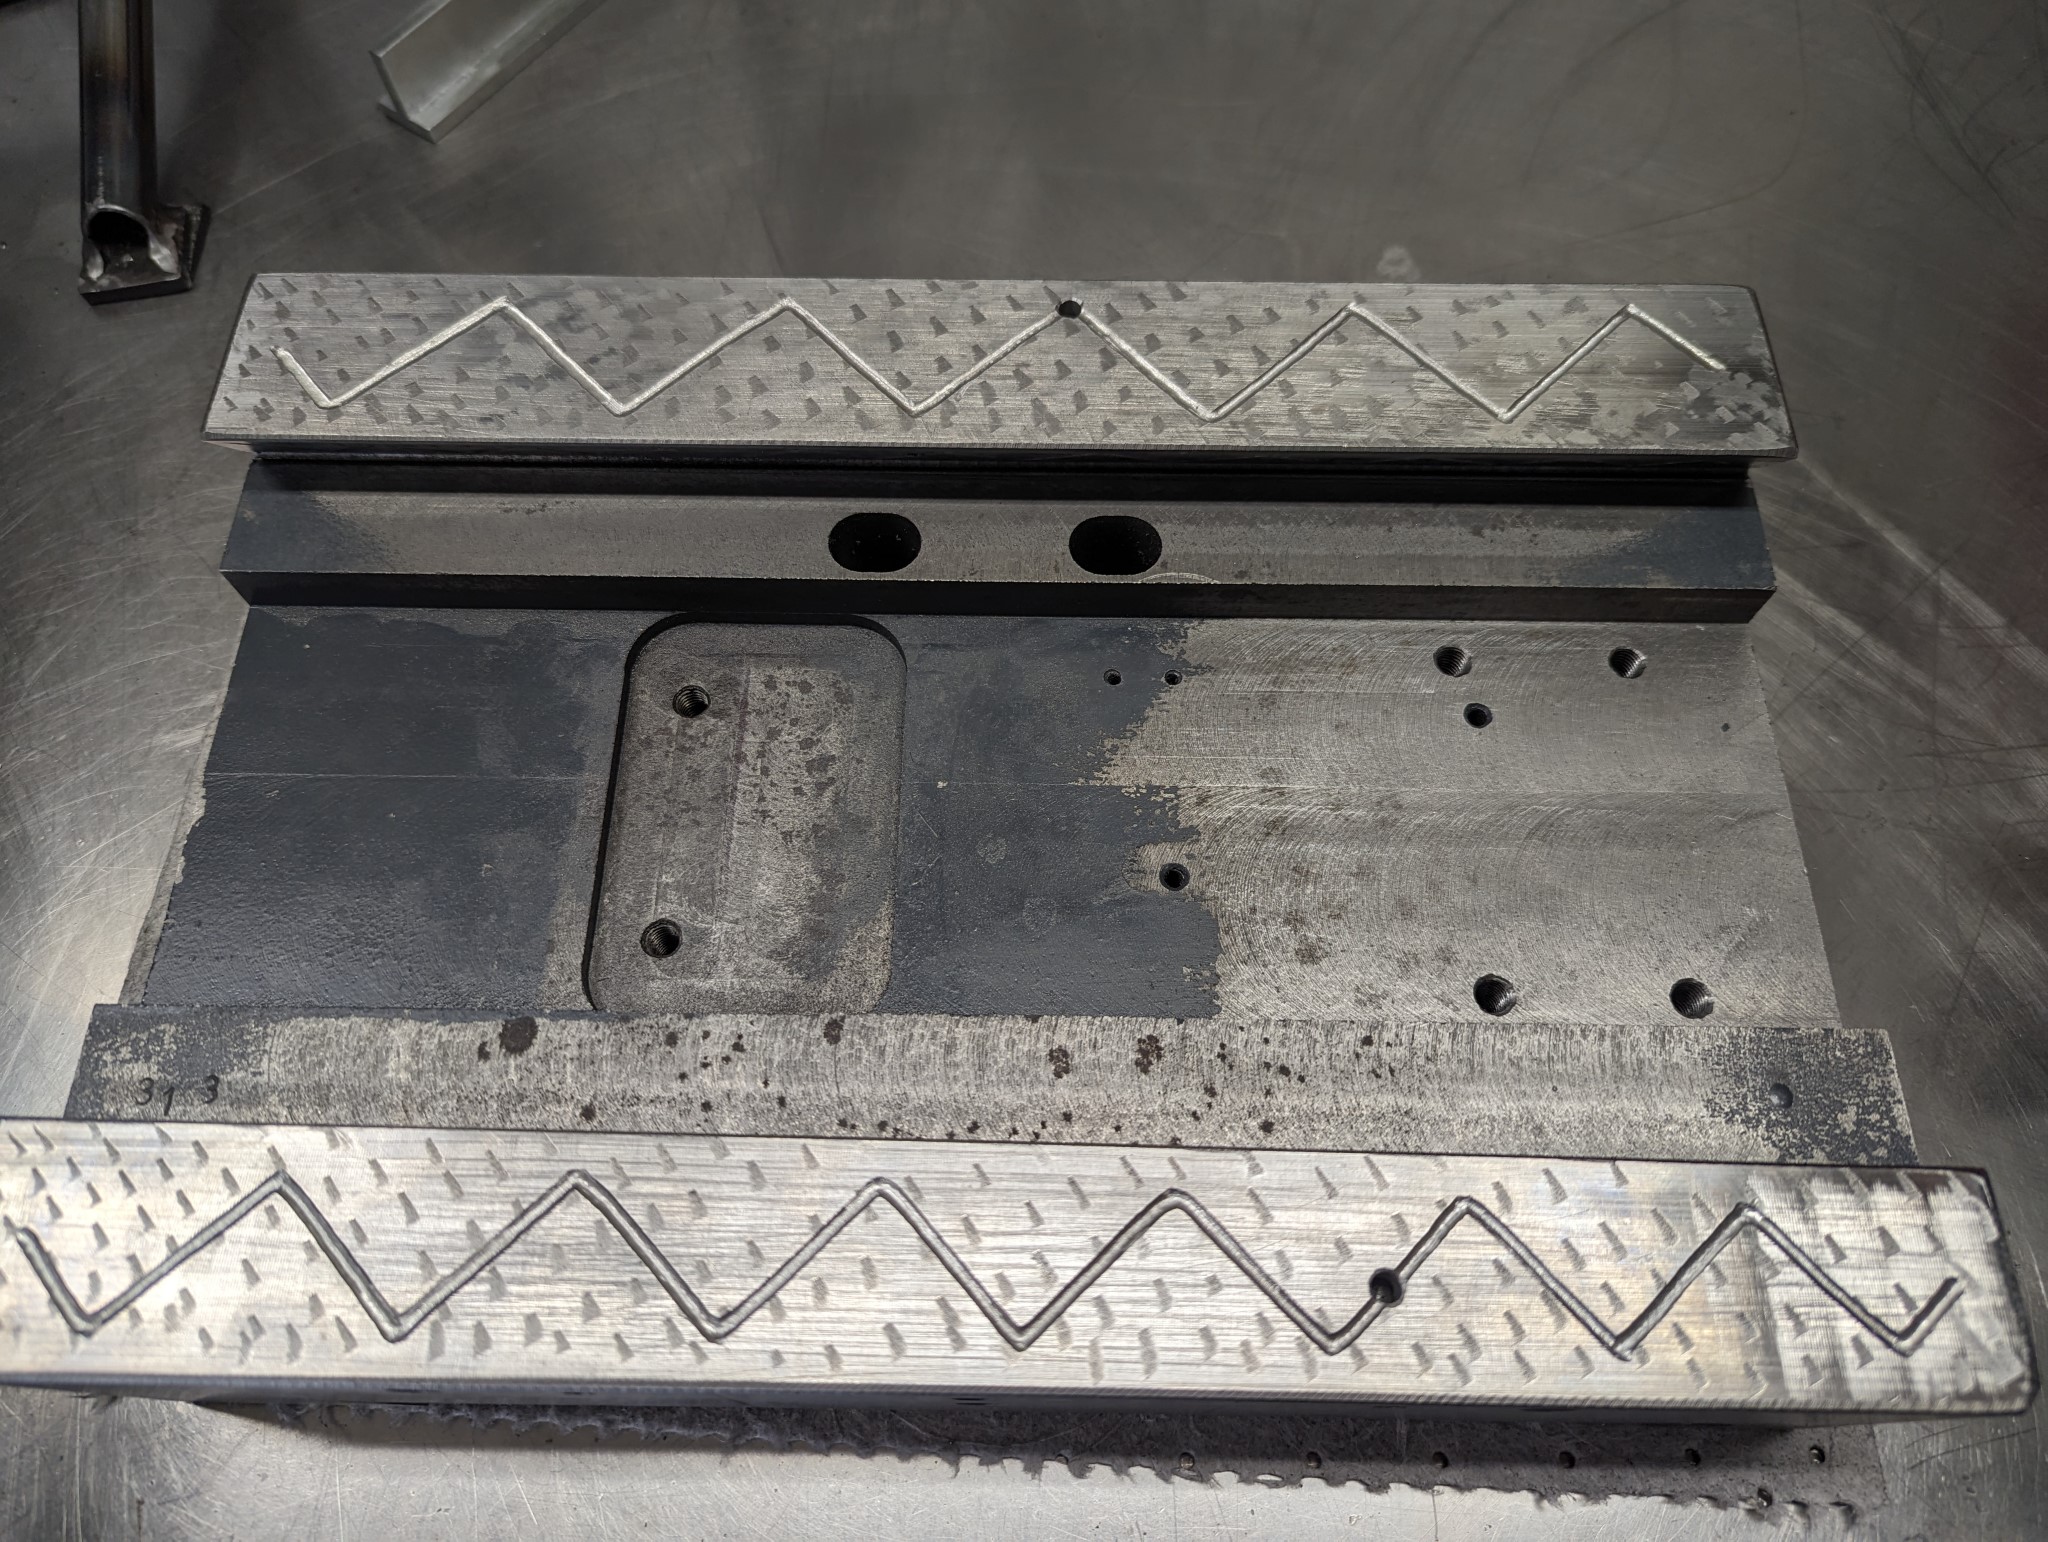
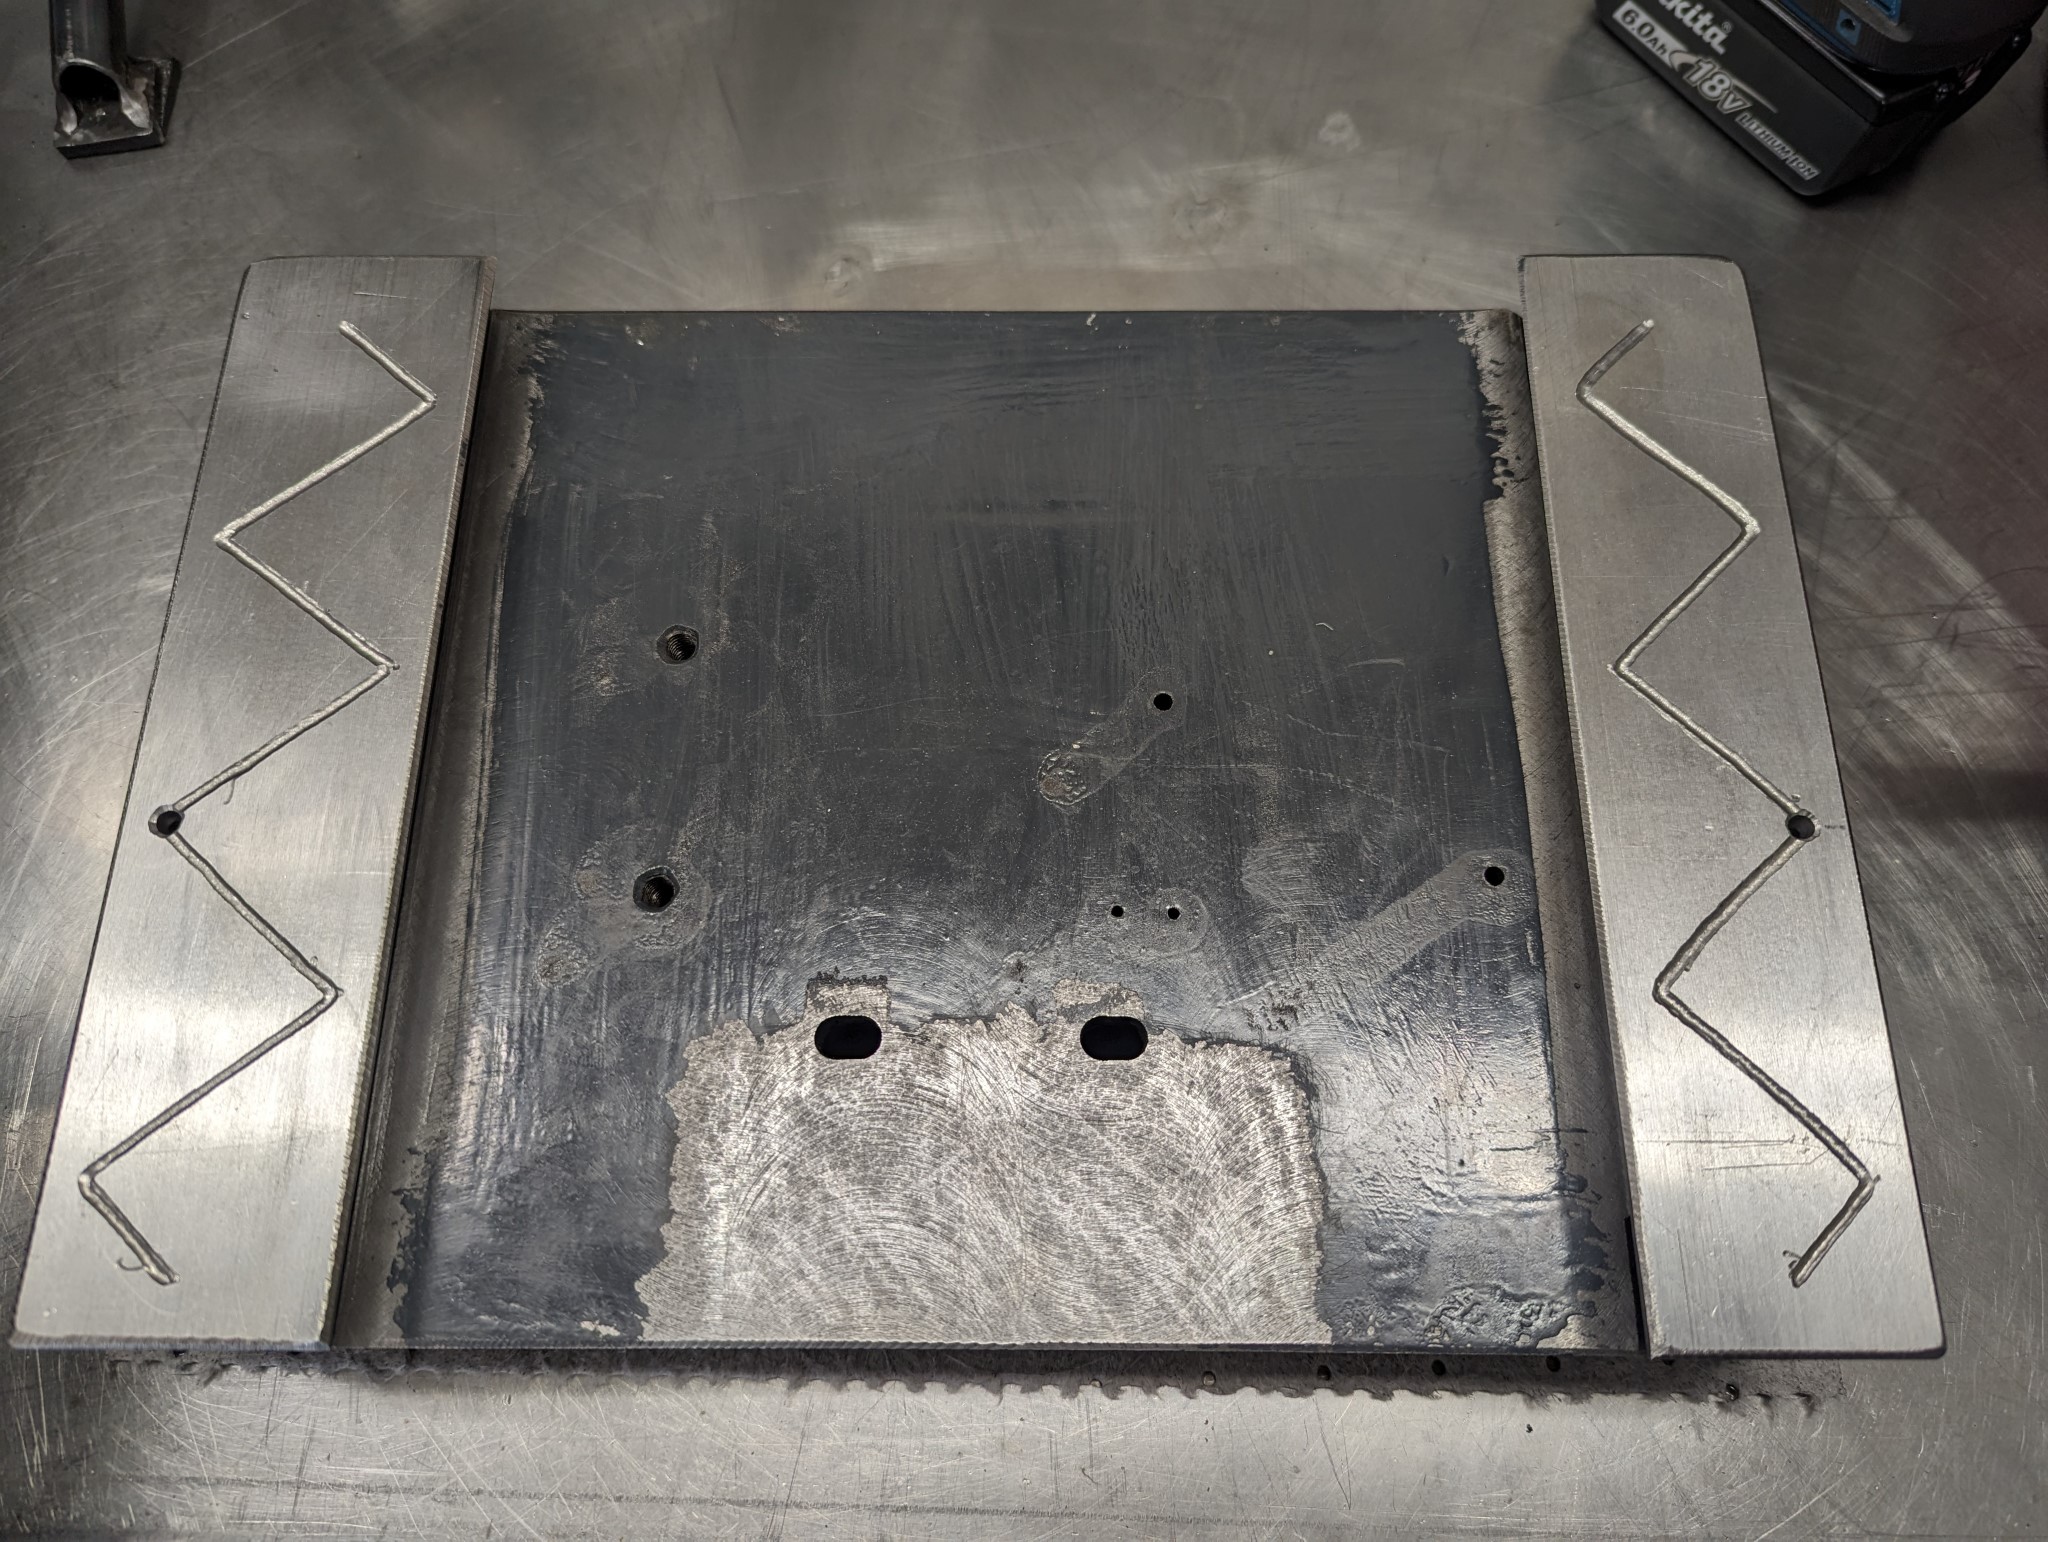
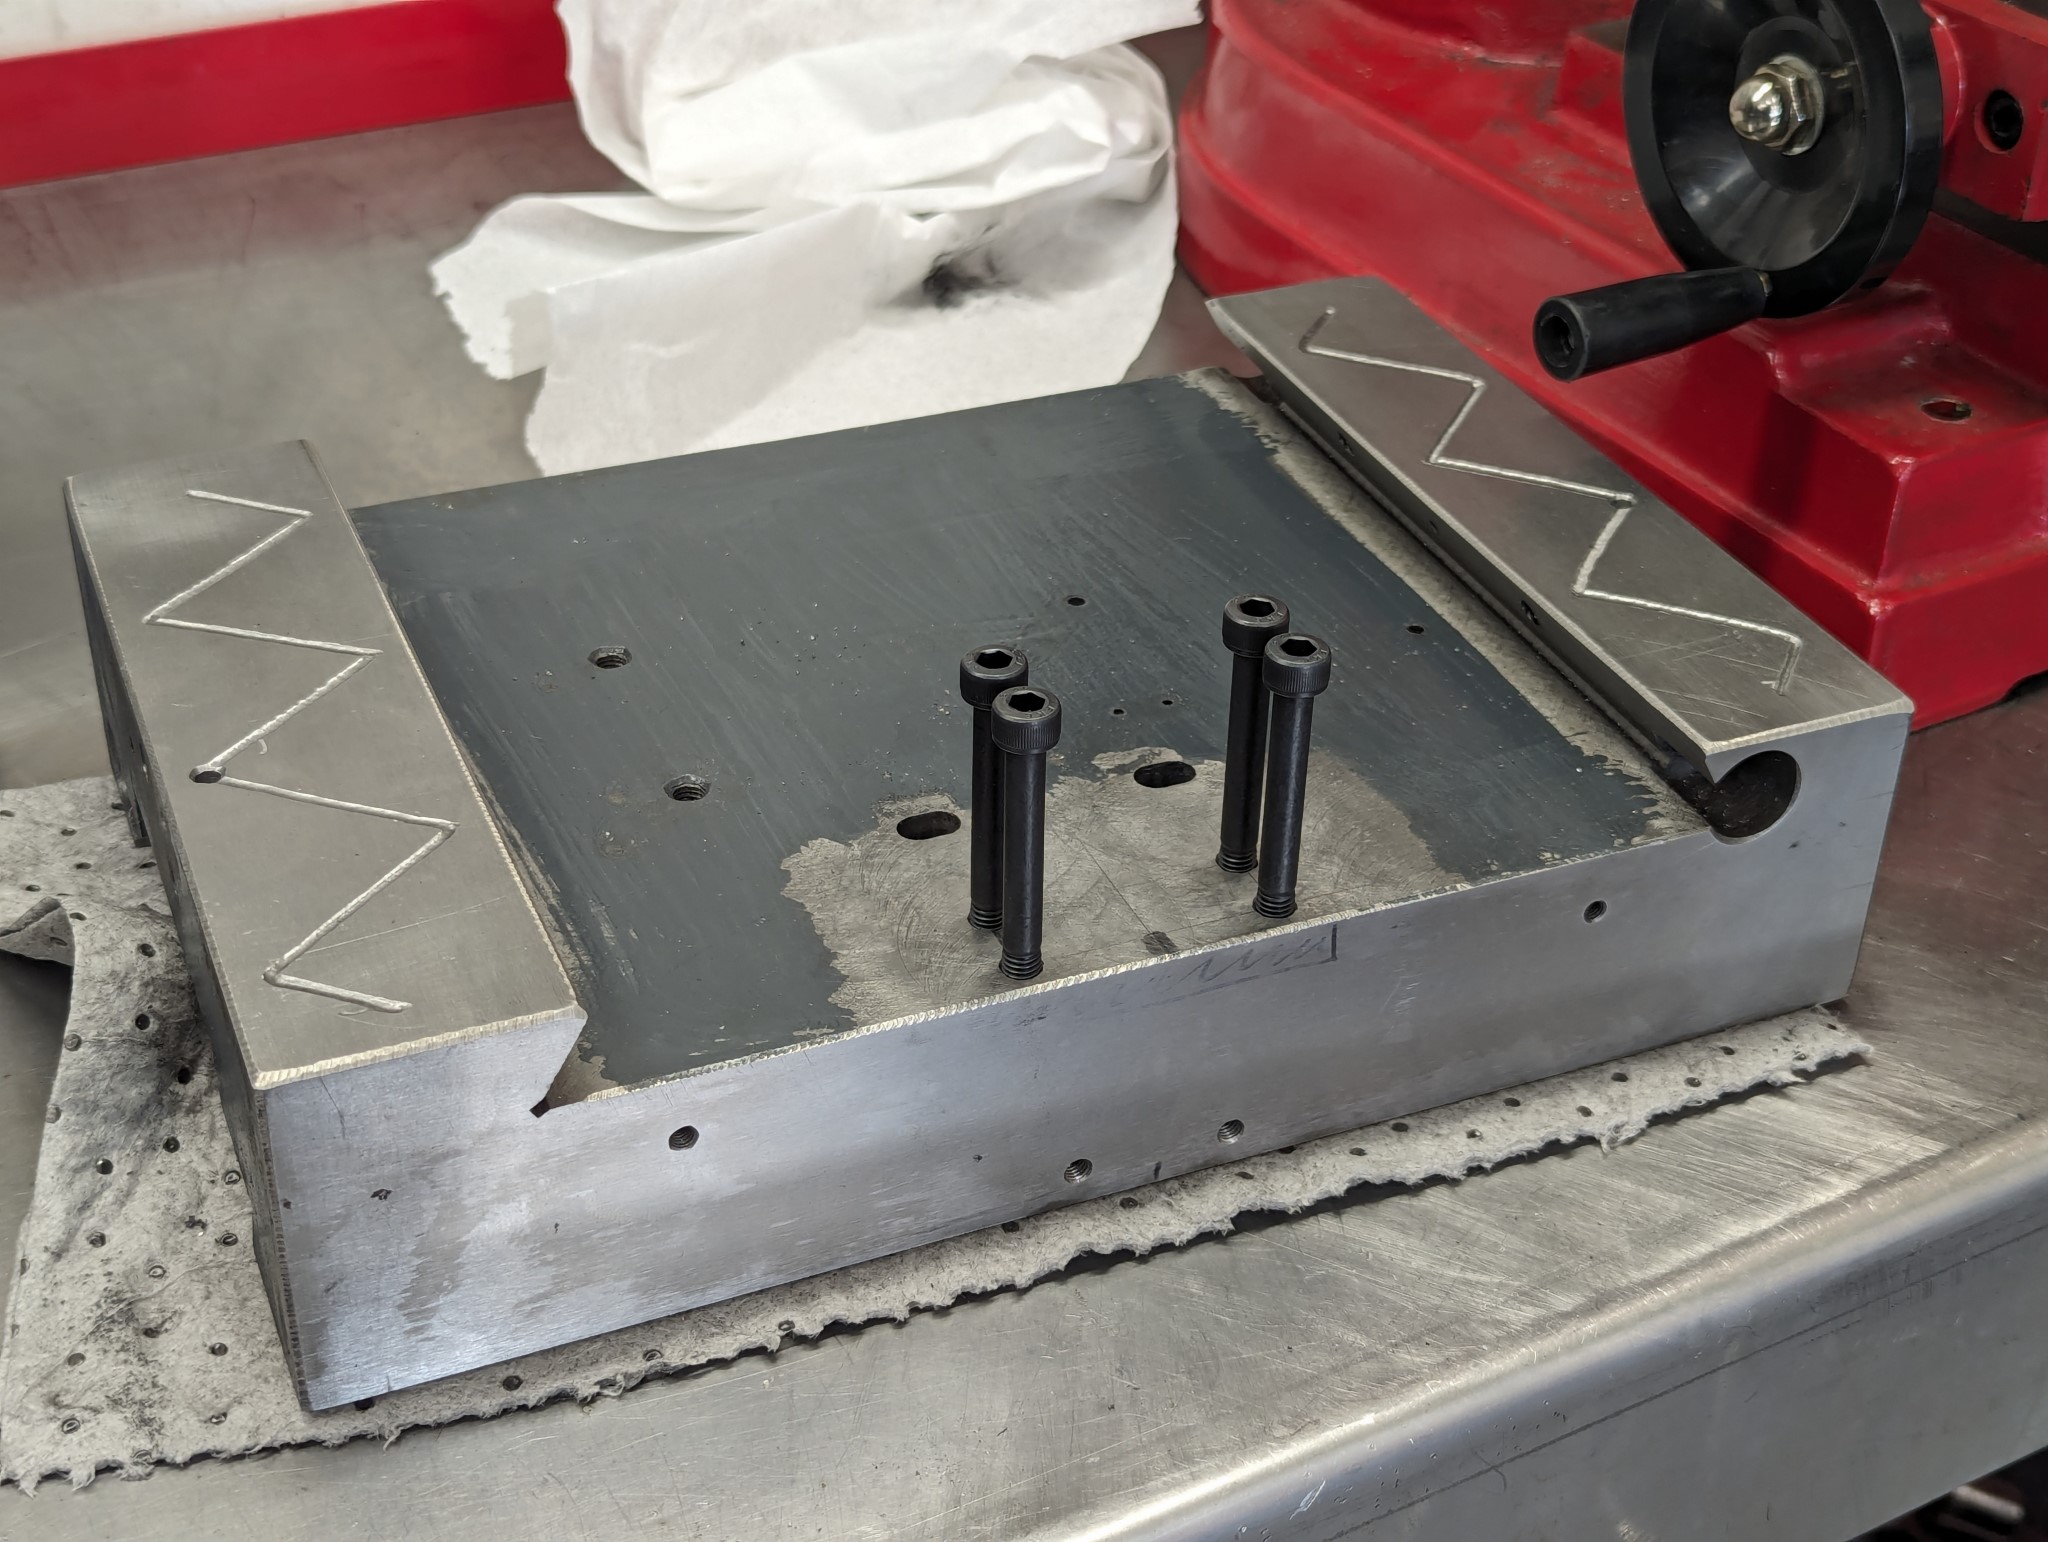
Next up it was time to start making the mount for the ball screws and bearing blocks. I did some rough measurements and then made drawings using in Visio which I then printed and tweaked until they fit on the machine.


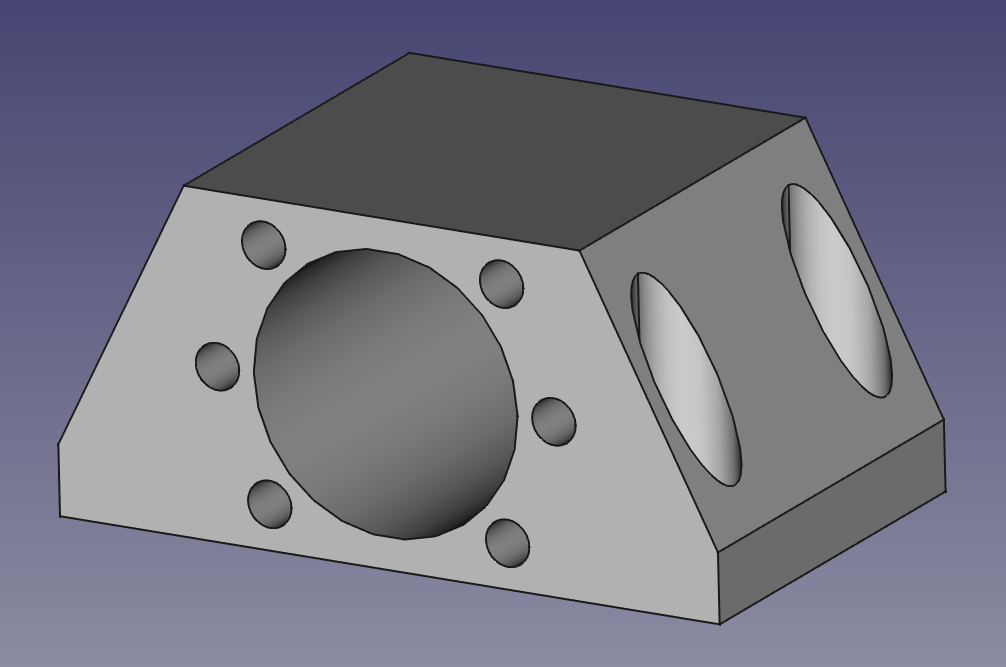
Halfway through this process I realized that Visio wasn't the right tool for this job and I decided to learn how to use FreeCAD.

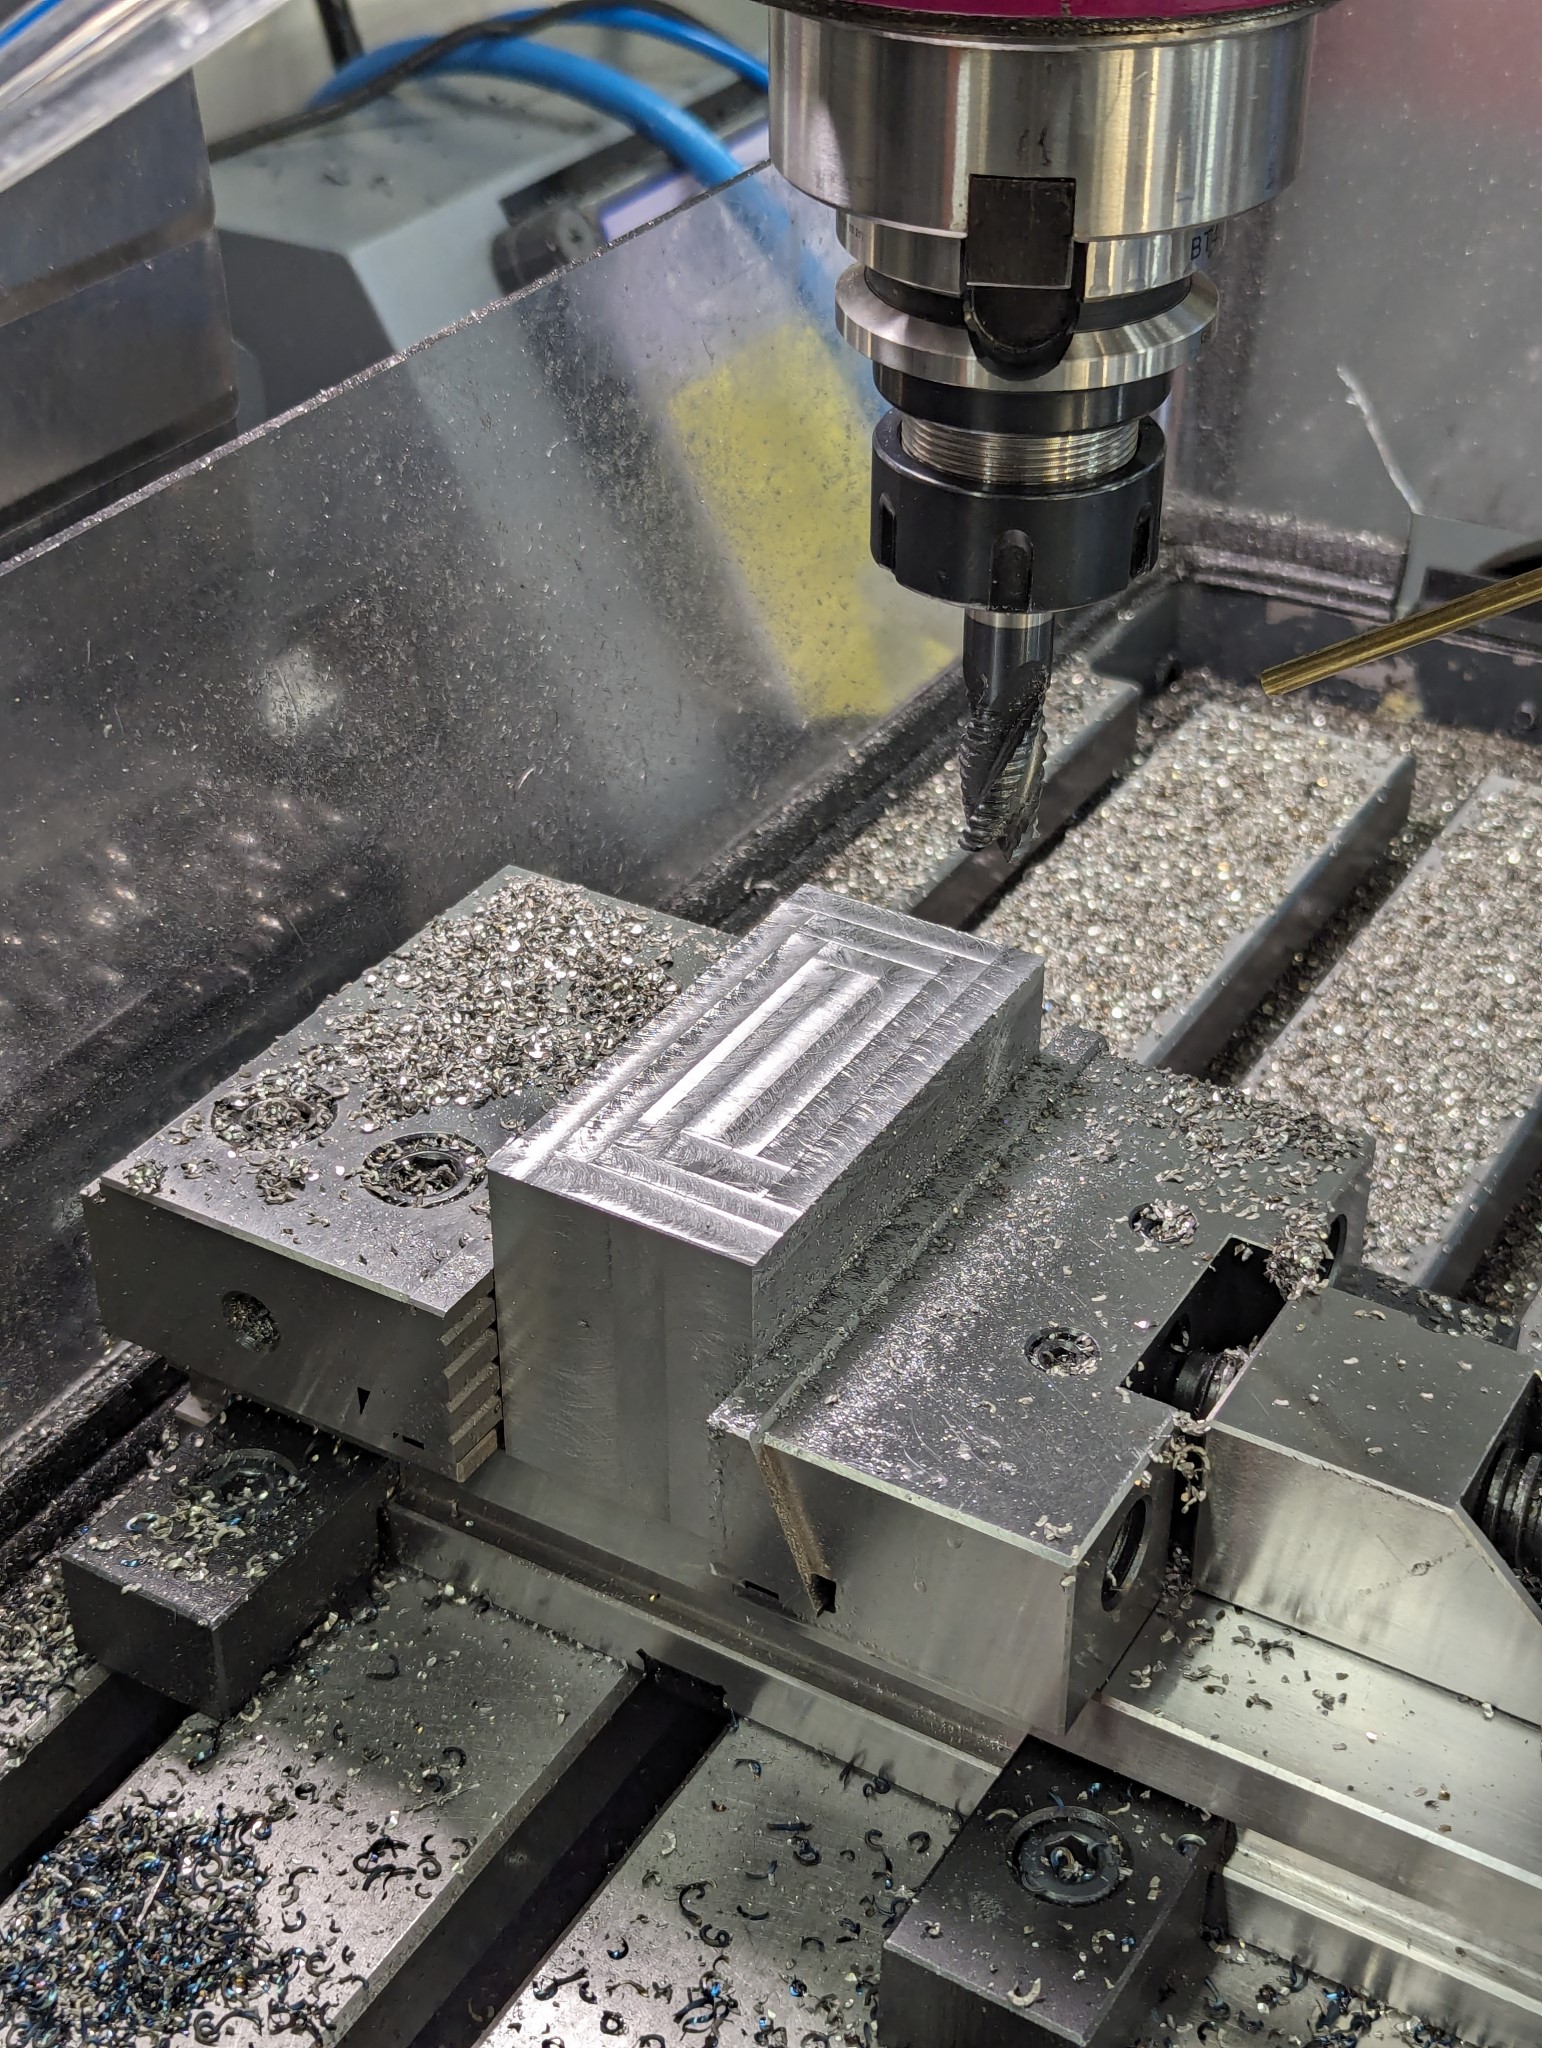
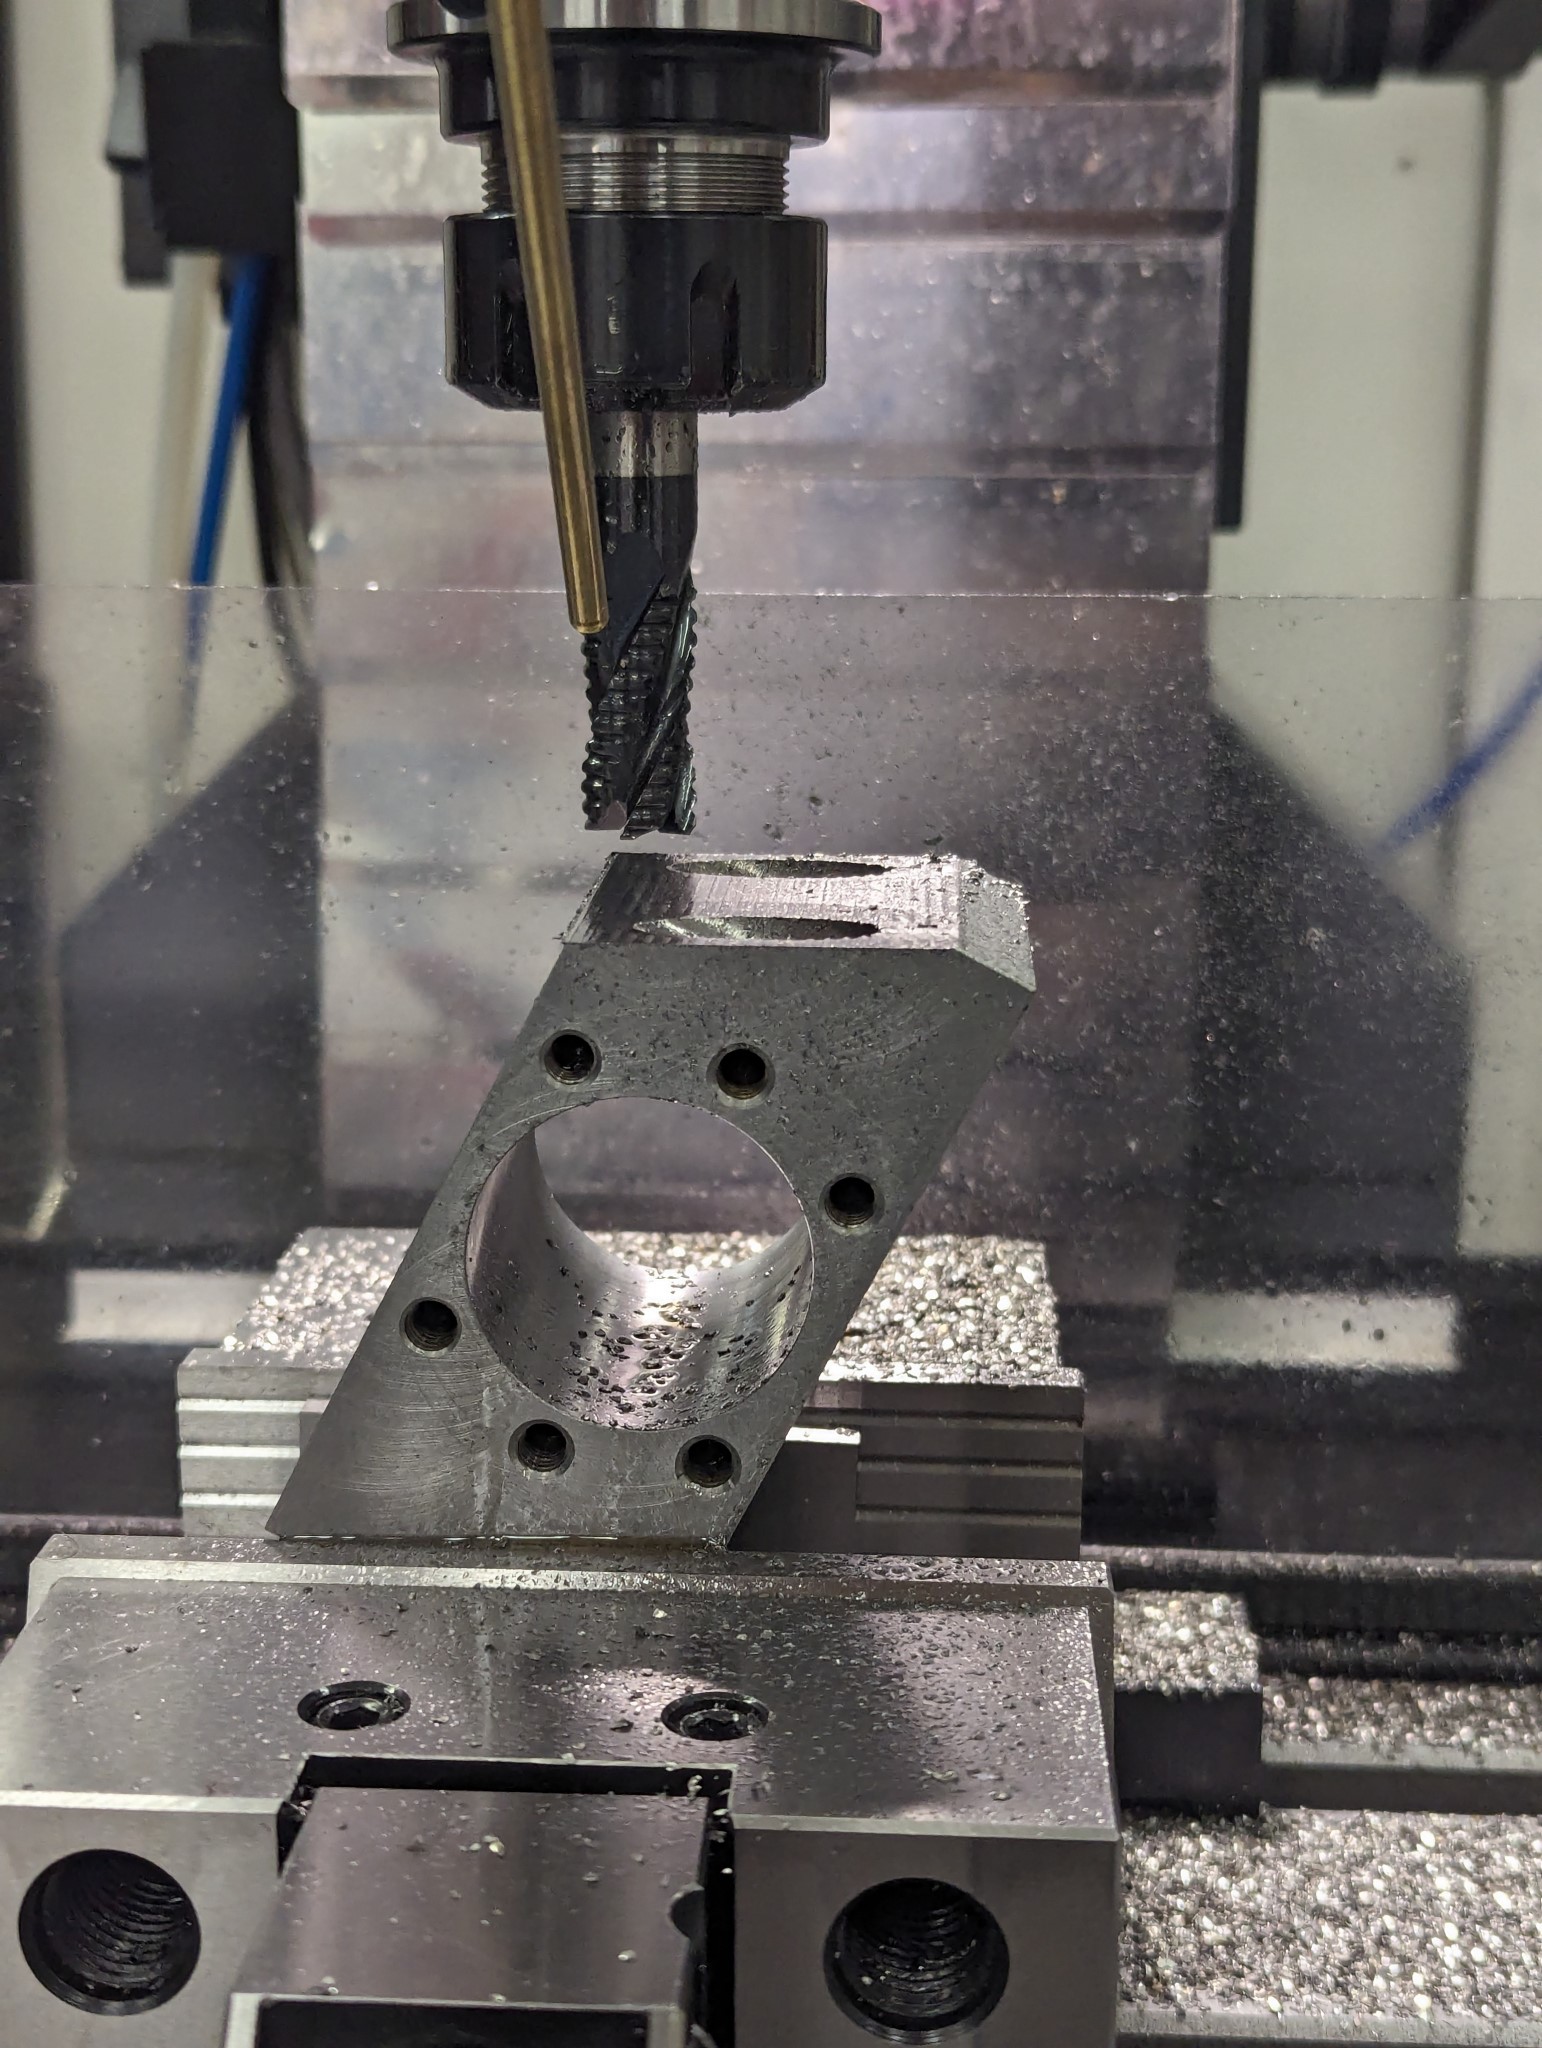
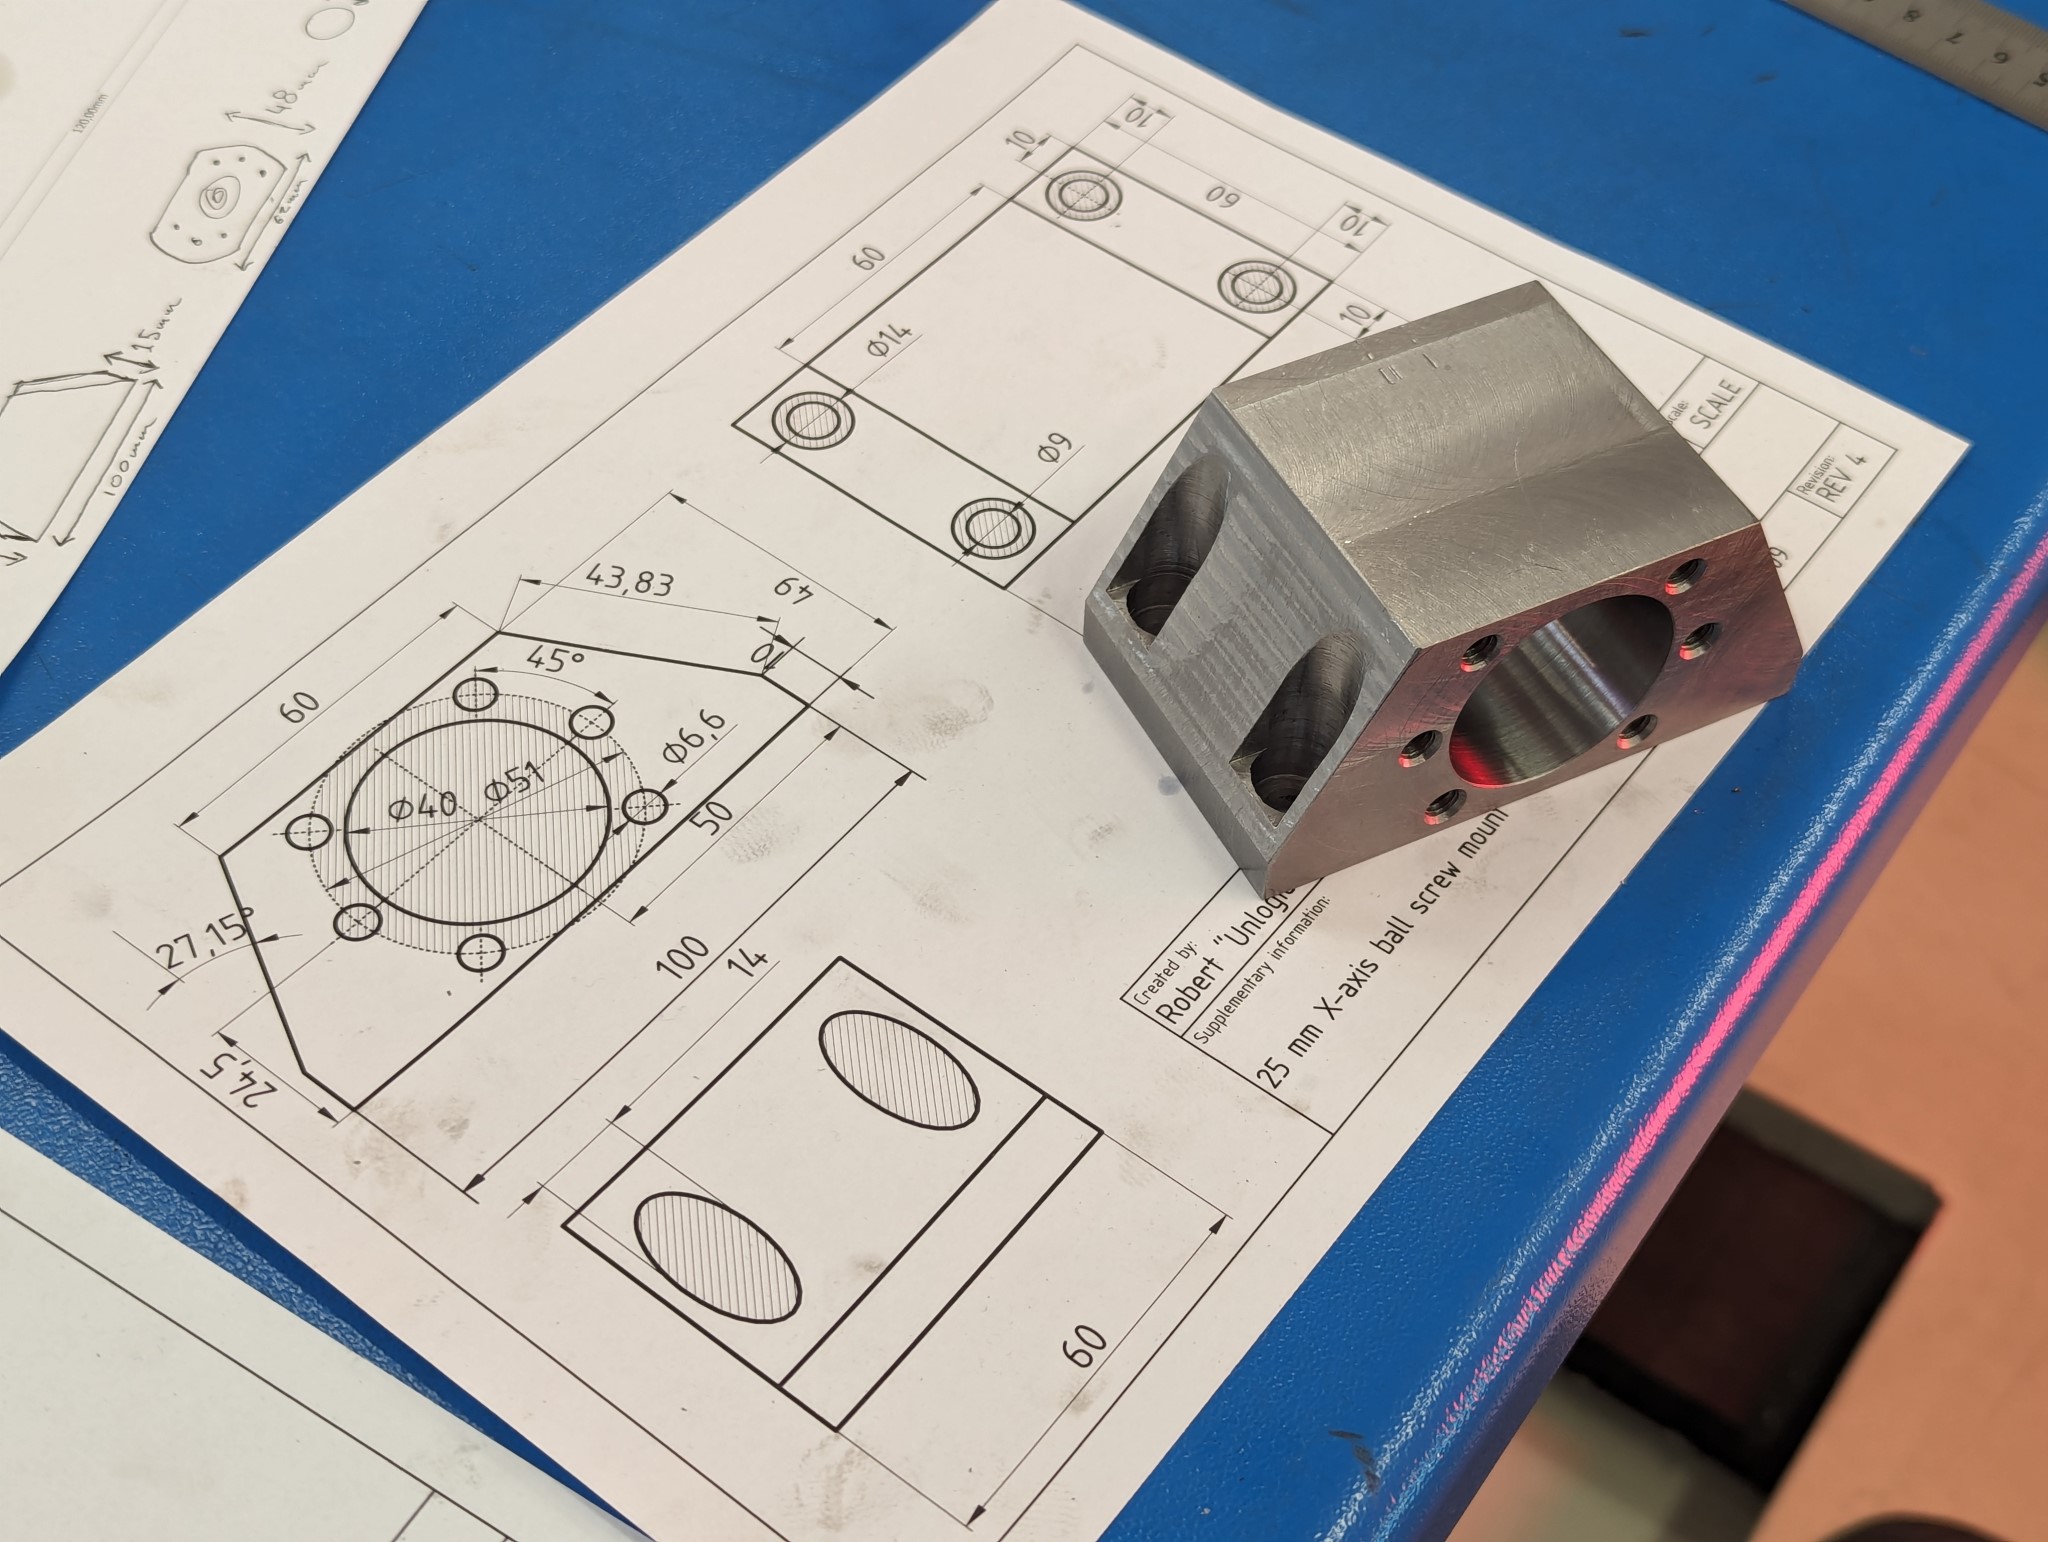
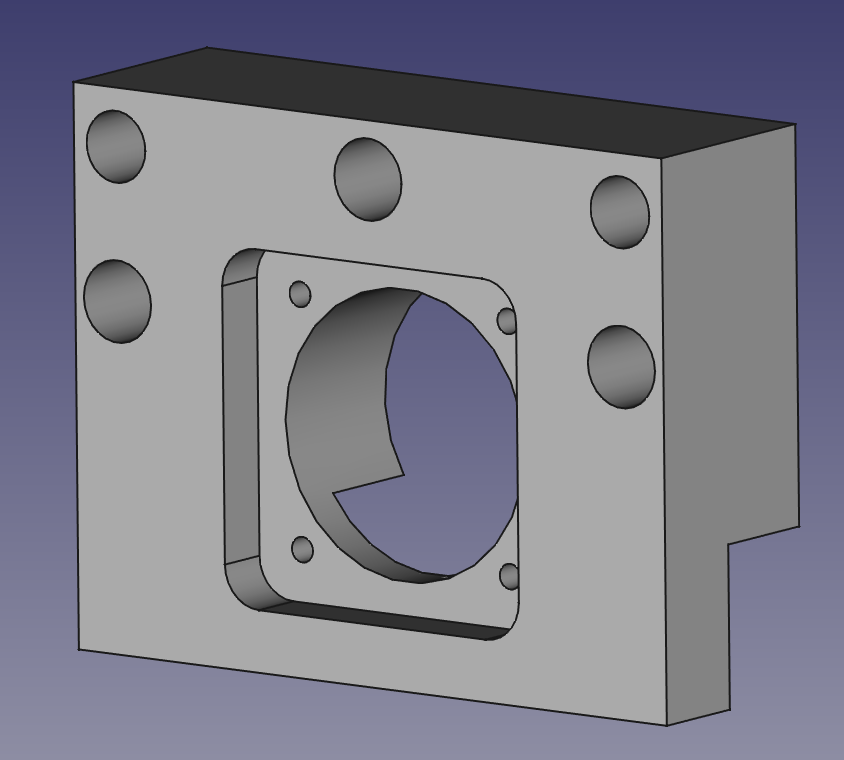
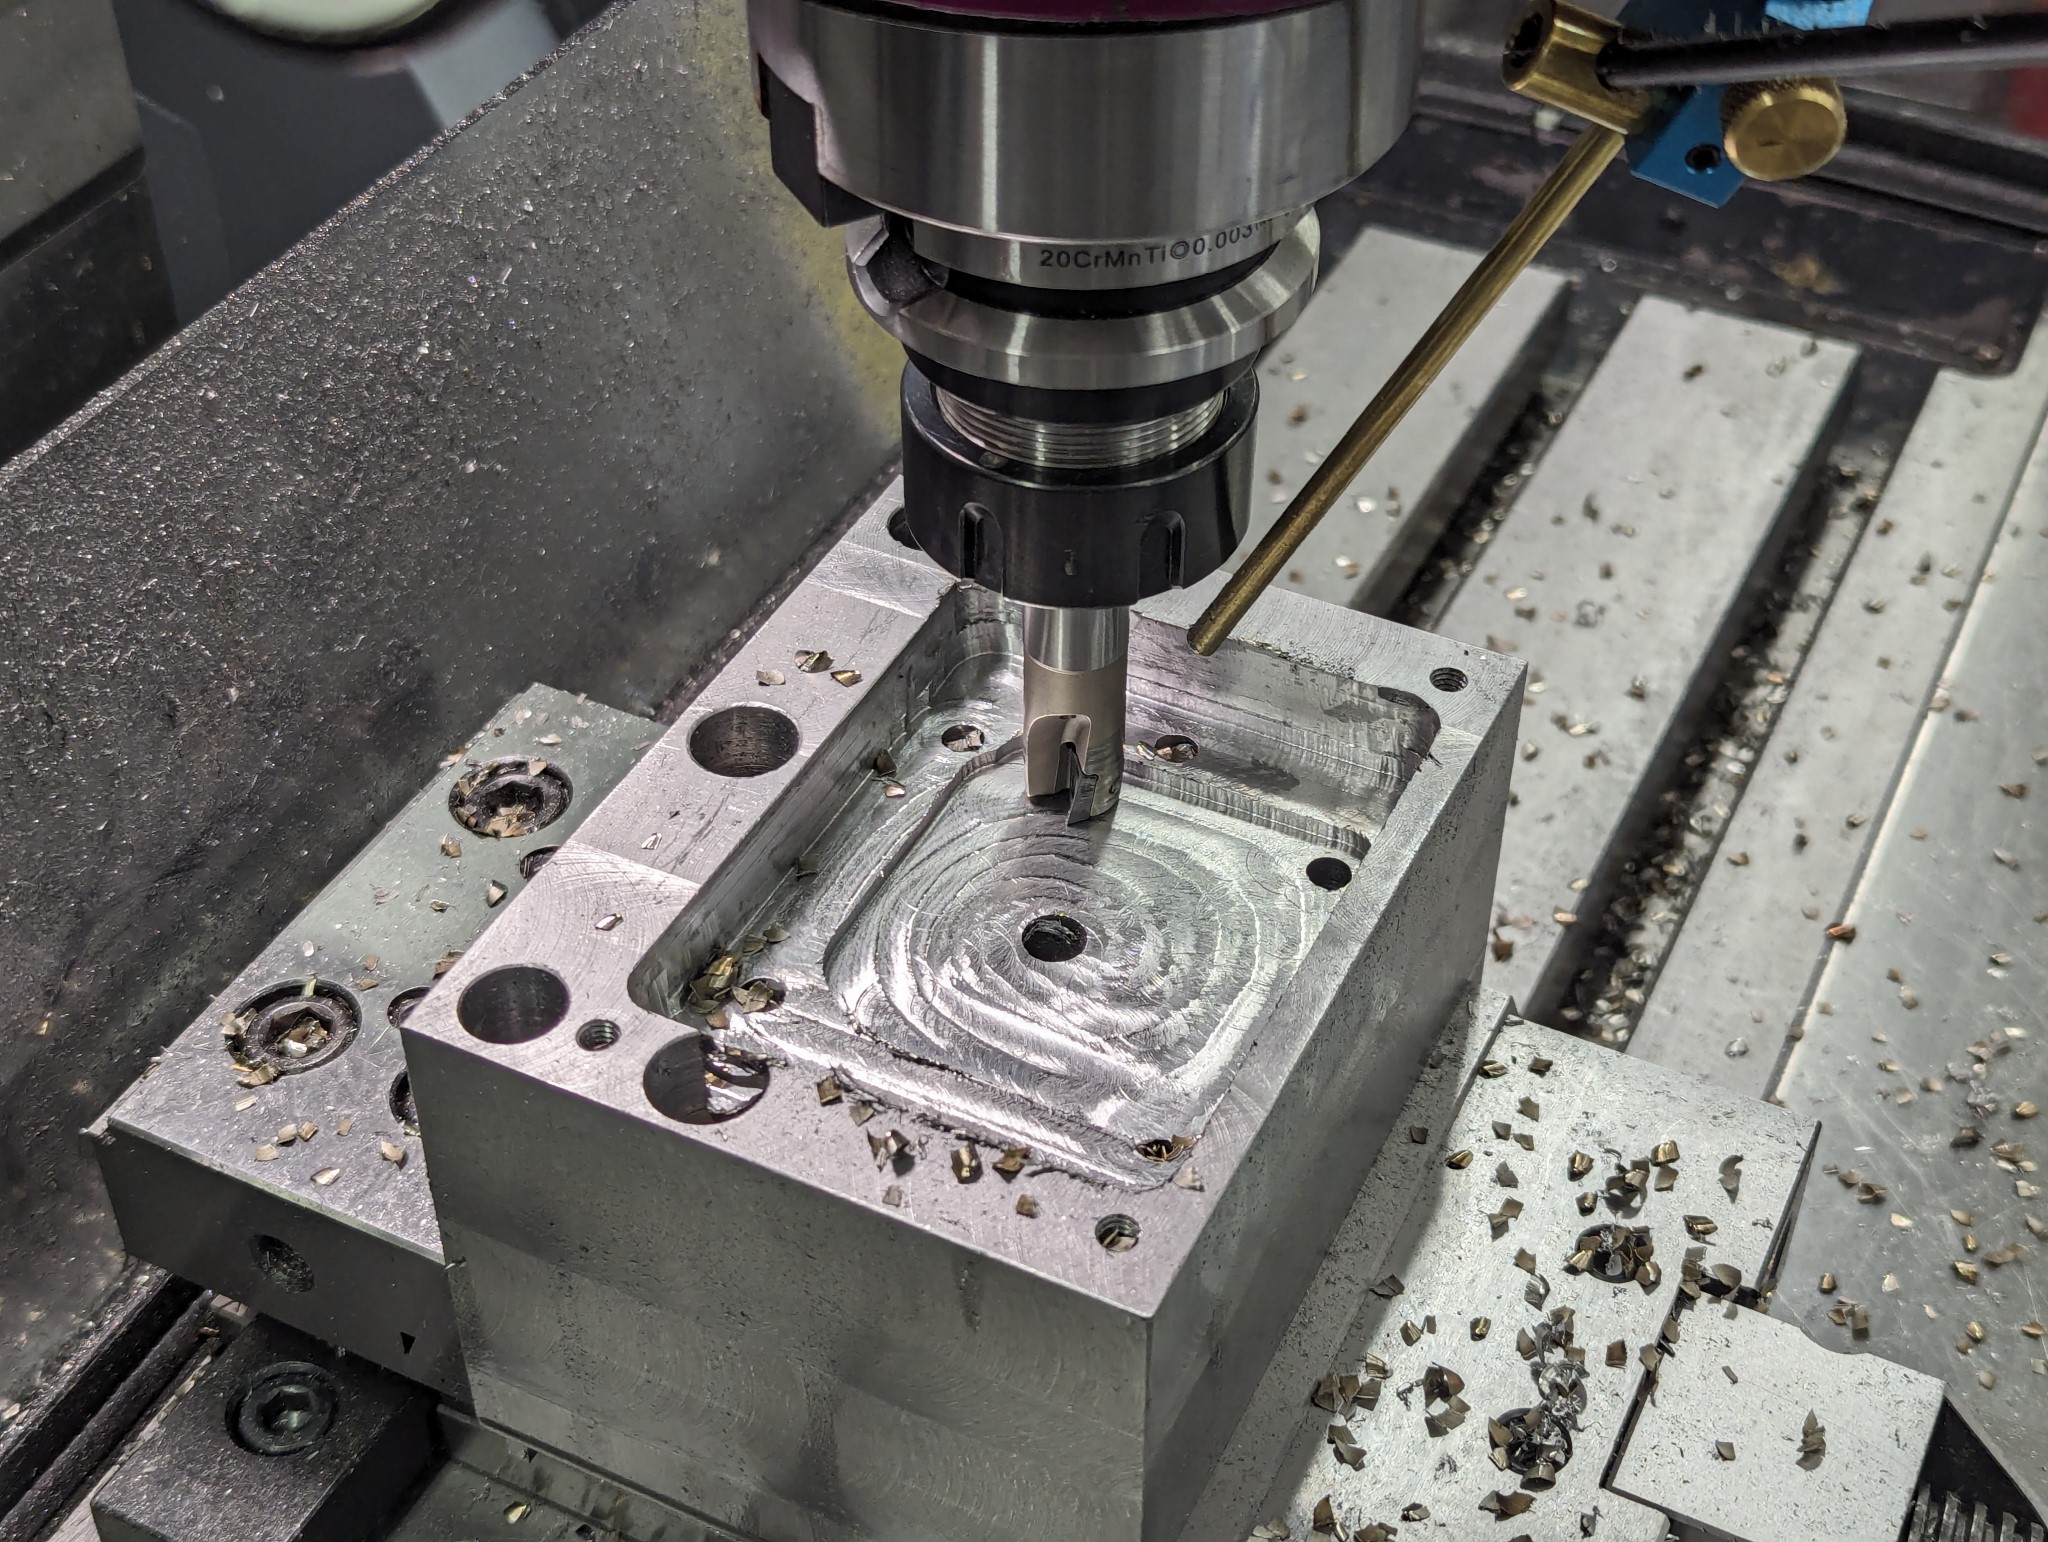
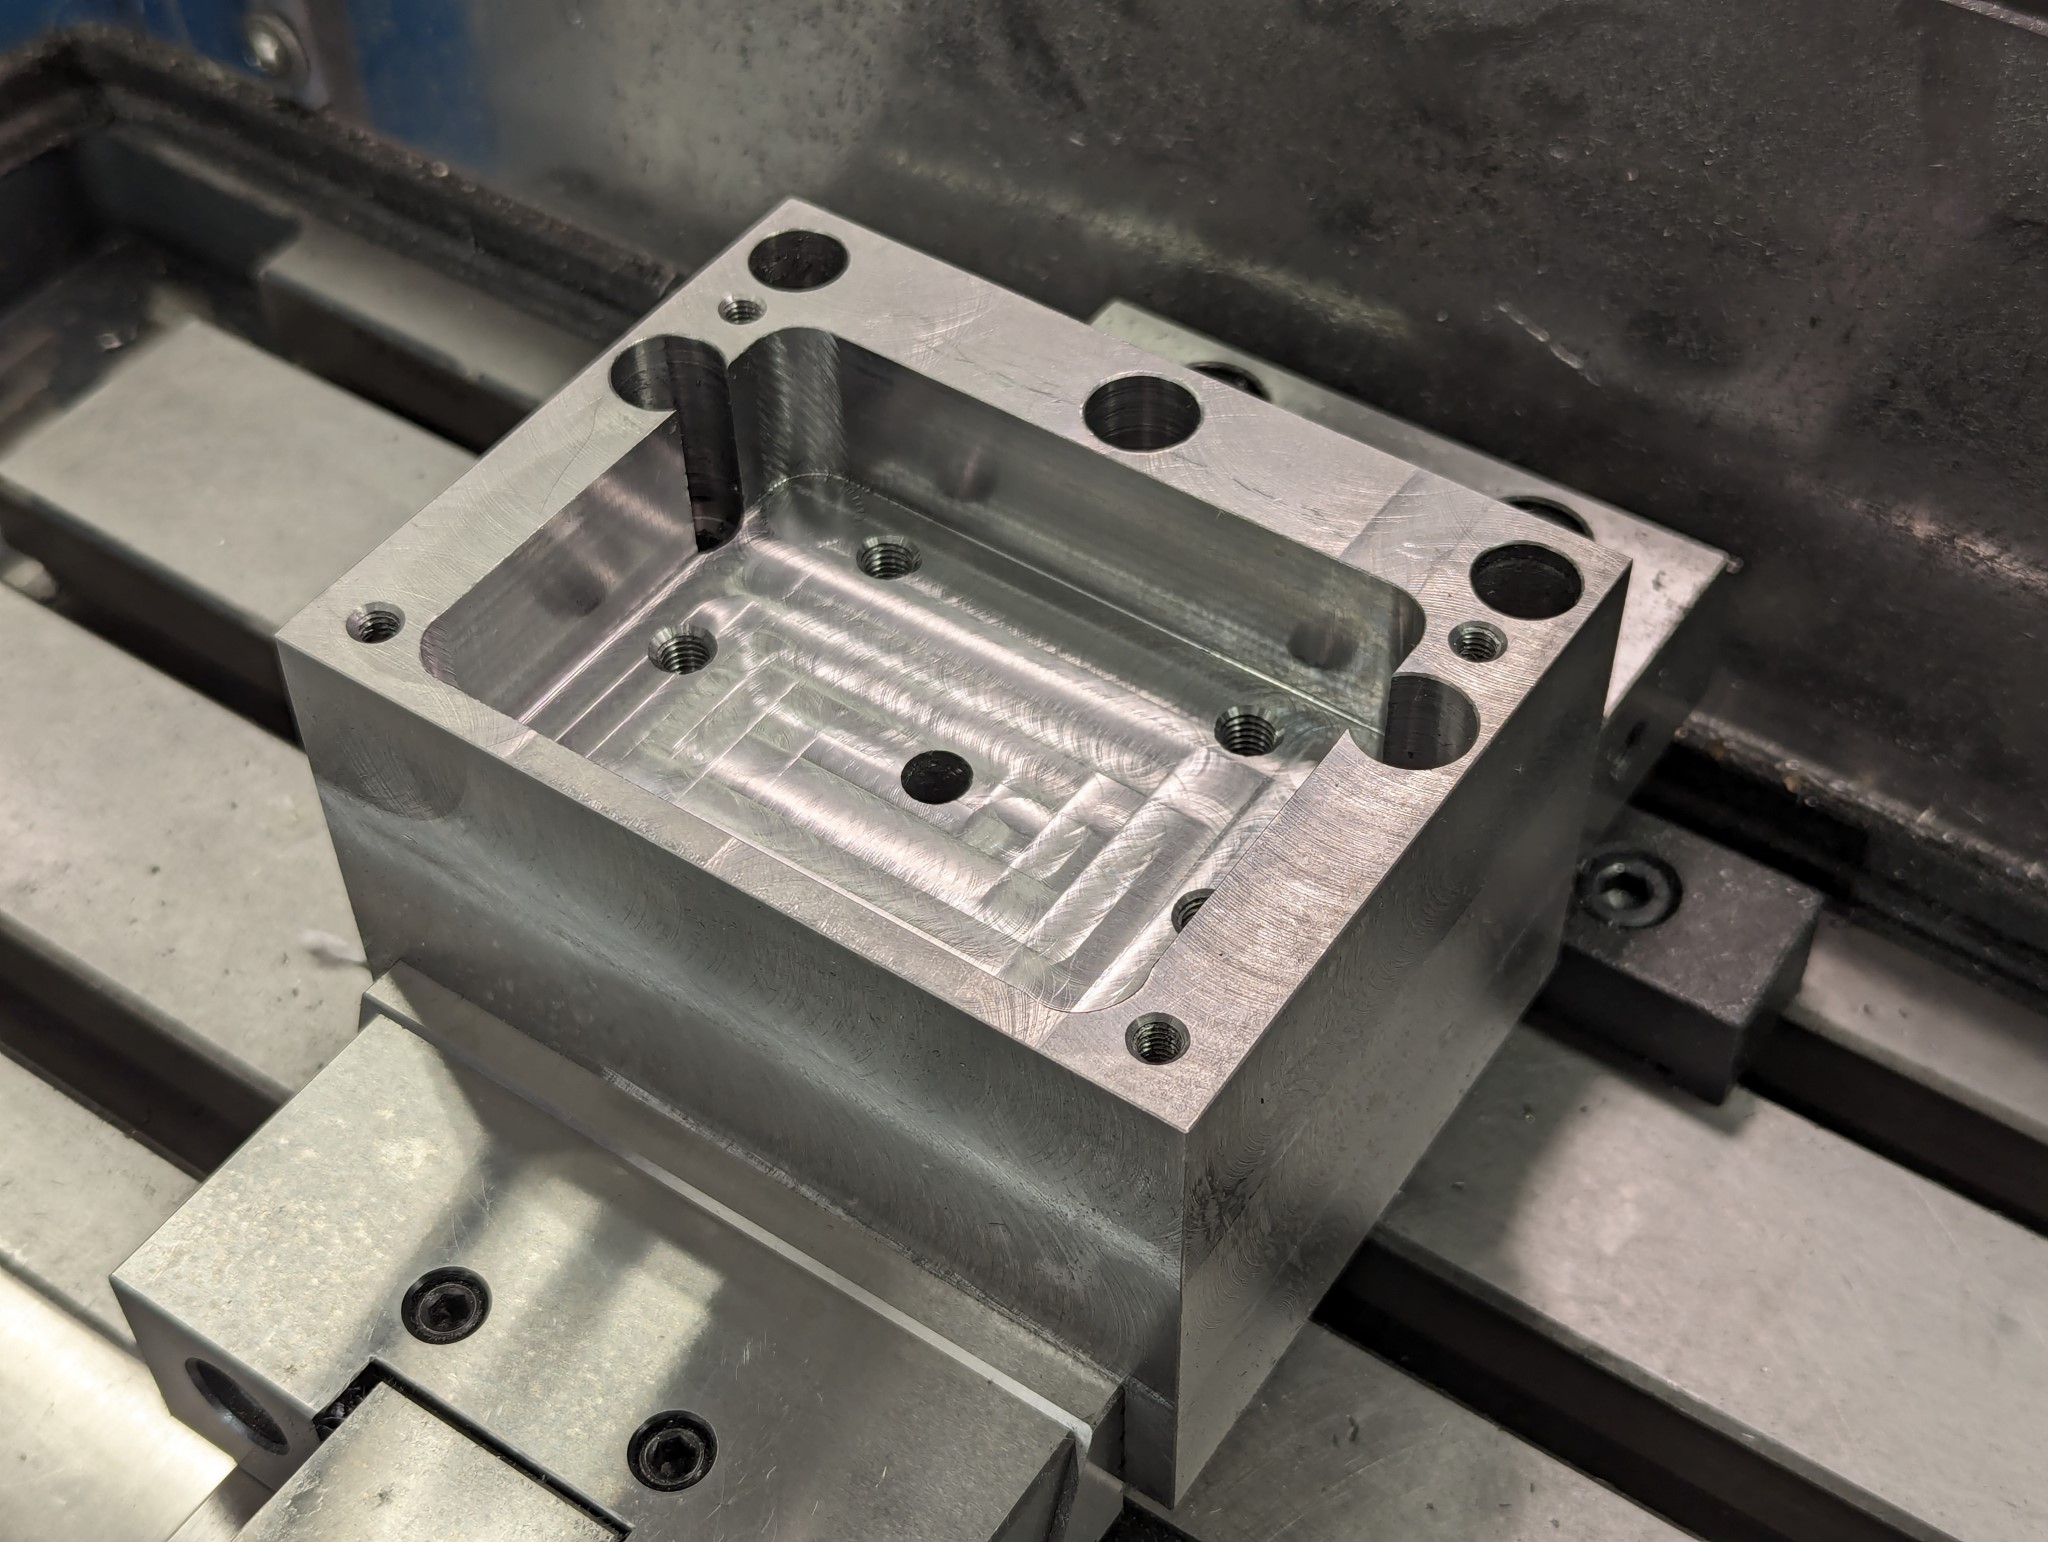
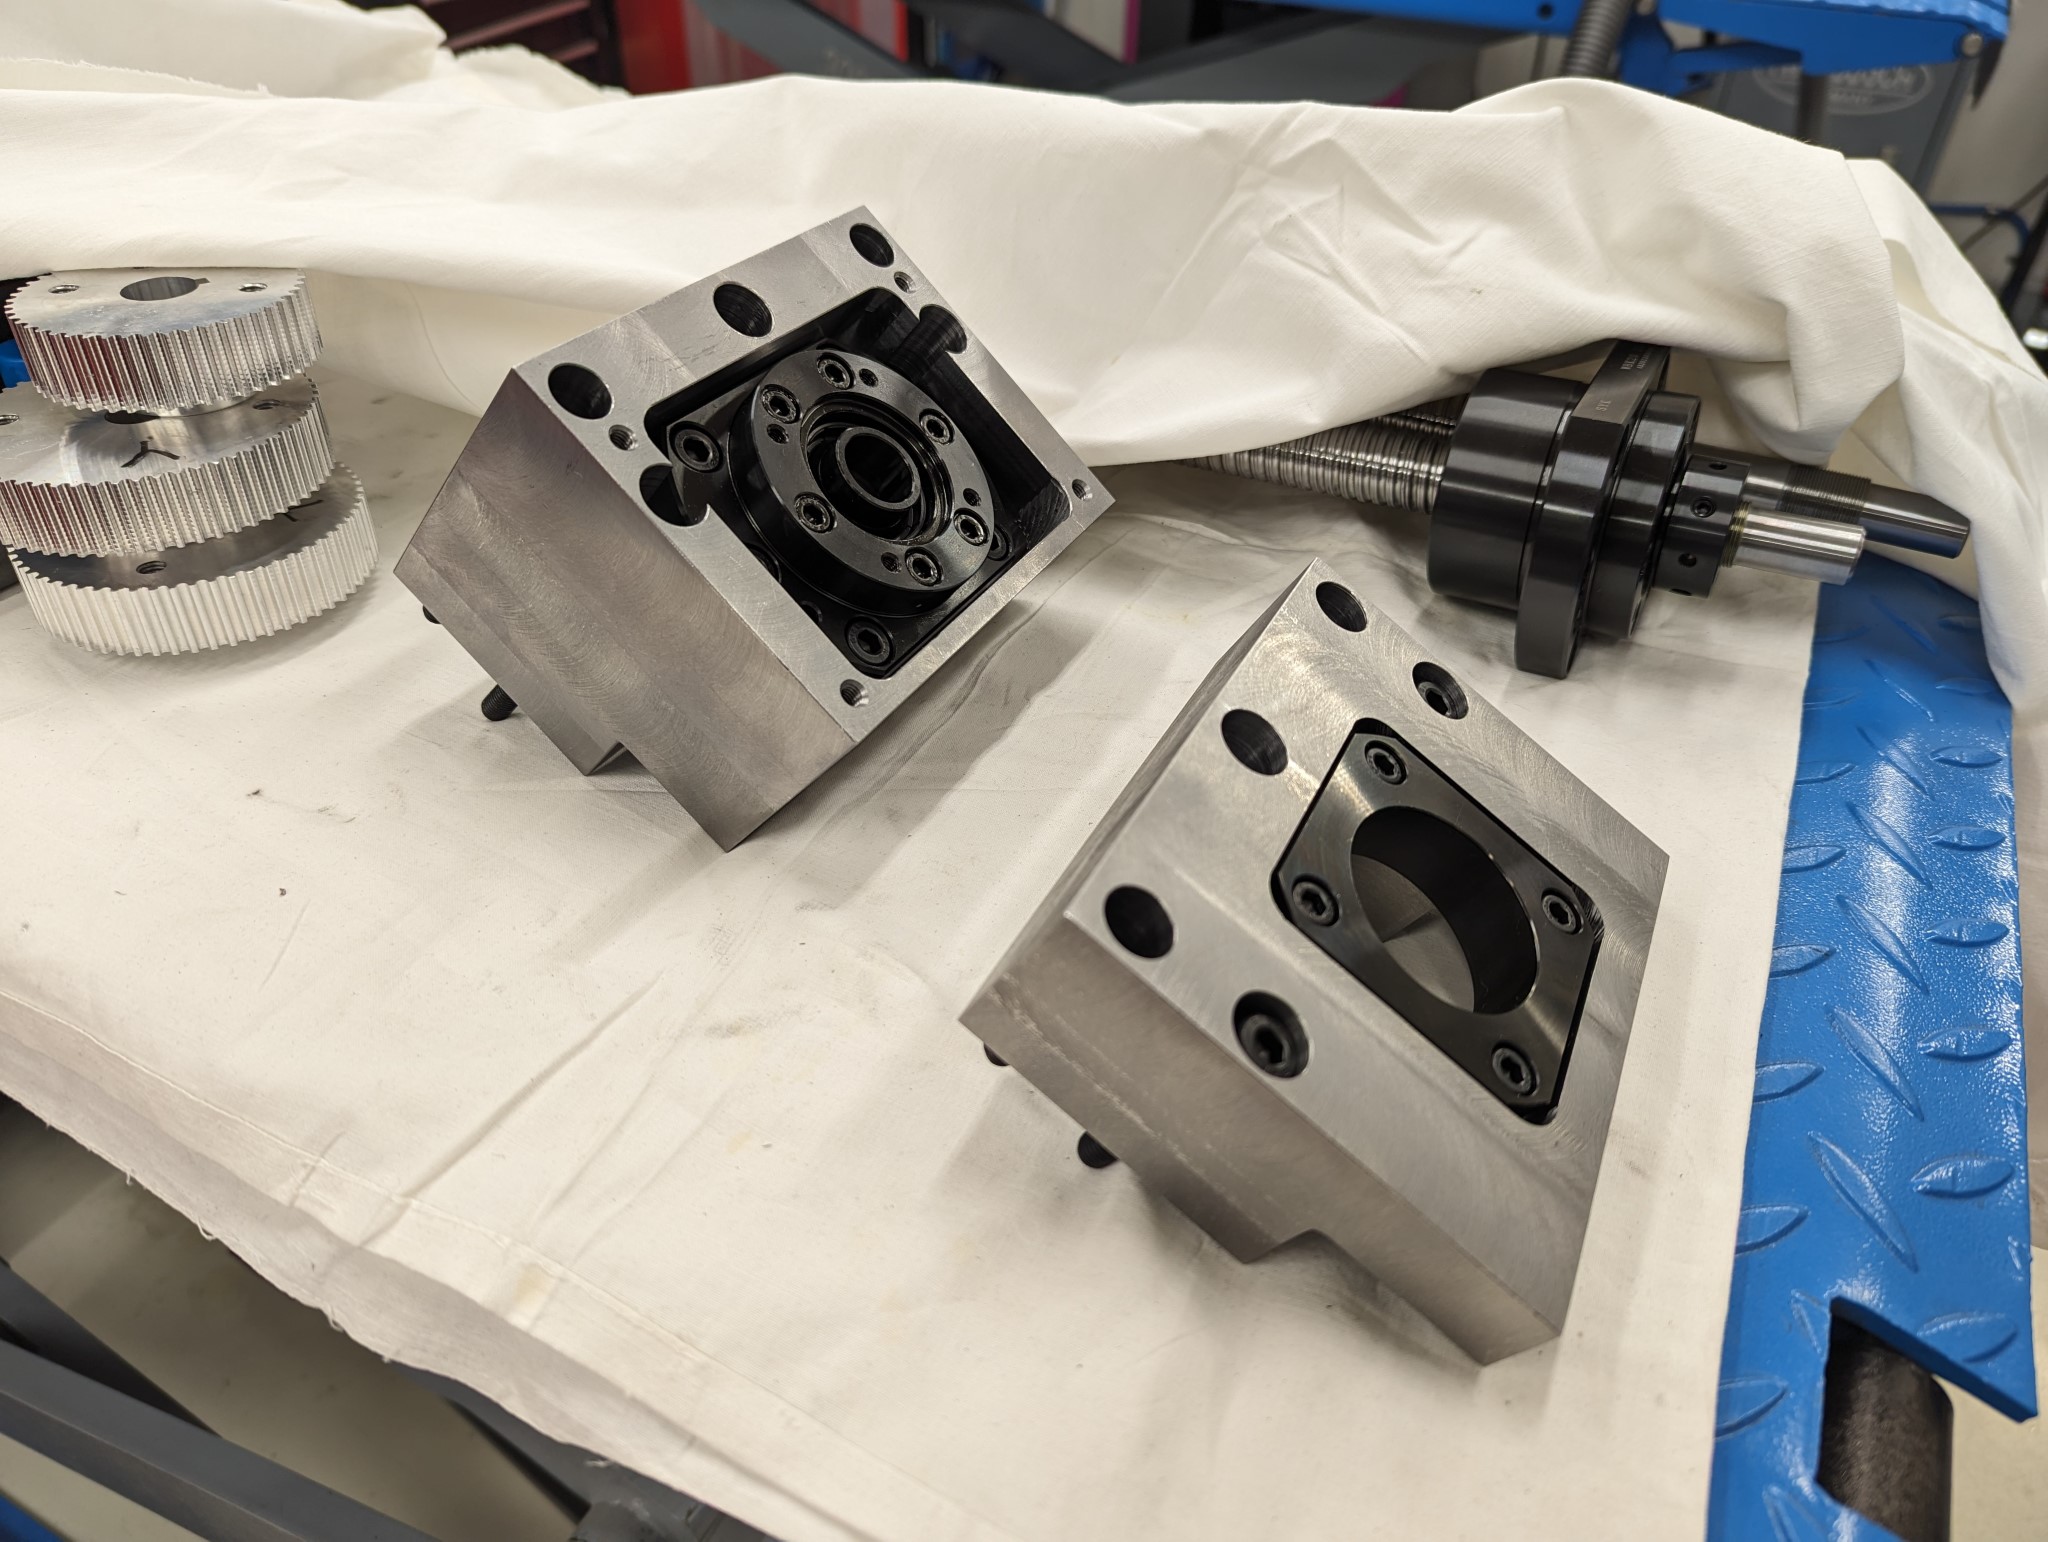
The first thing I designed in FreeCAD was the mount for the ball screw nut for the X axis which I then machined out of steel.


FreeCAD was really surprisingly easy and intuitive to get started with, much thanks to the great YouTube tutorials from MangoJelly Solutions (https://www.youtube.com/@MangoJellySolutions). 


Please Log in or Create an account to join the conversation.

More
2 years 8 months ago #293697 by Unlogic
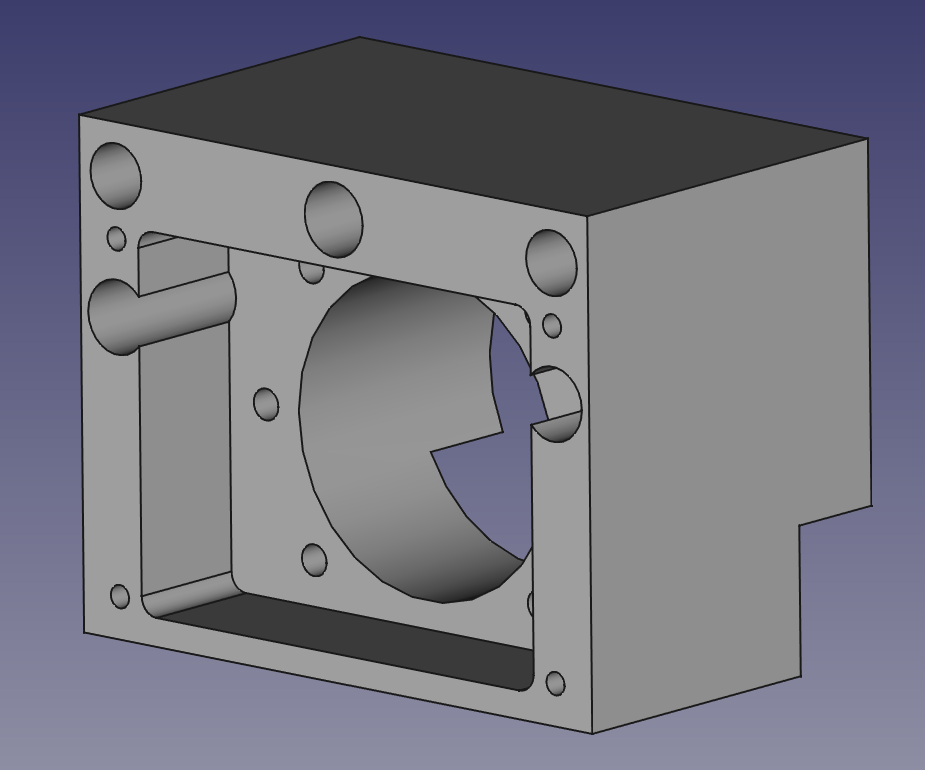
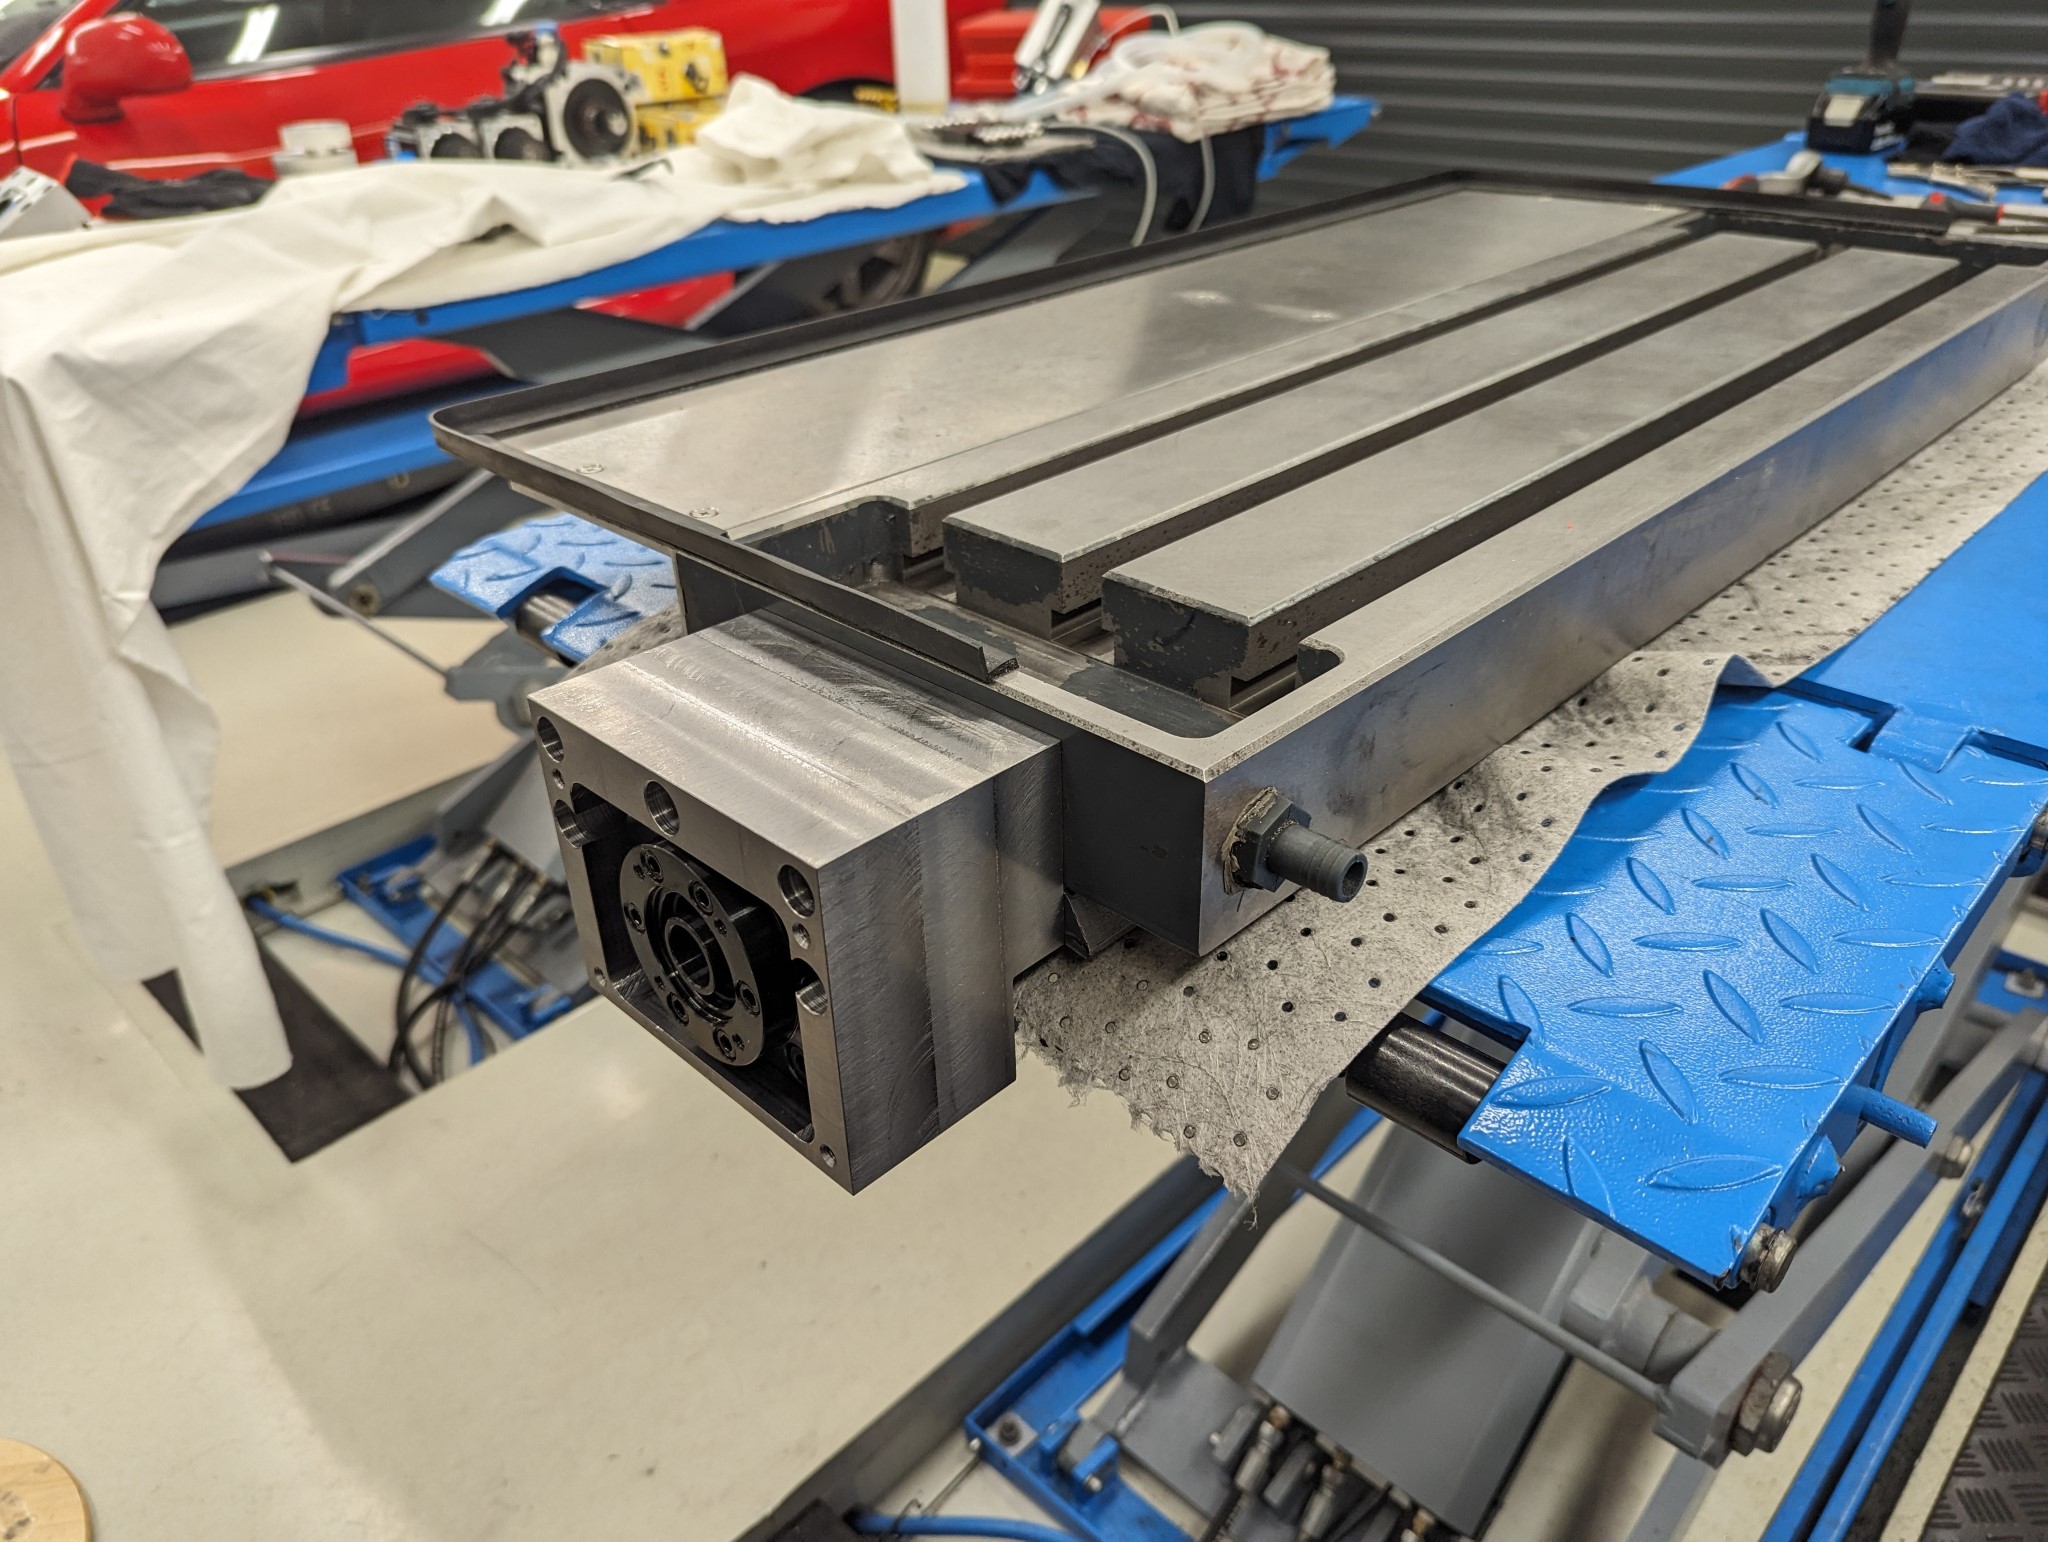
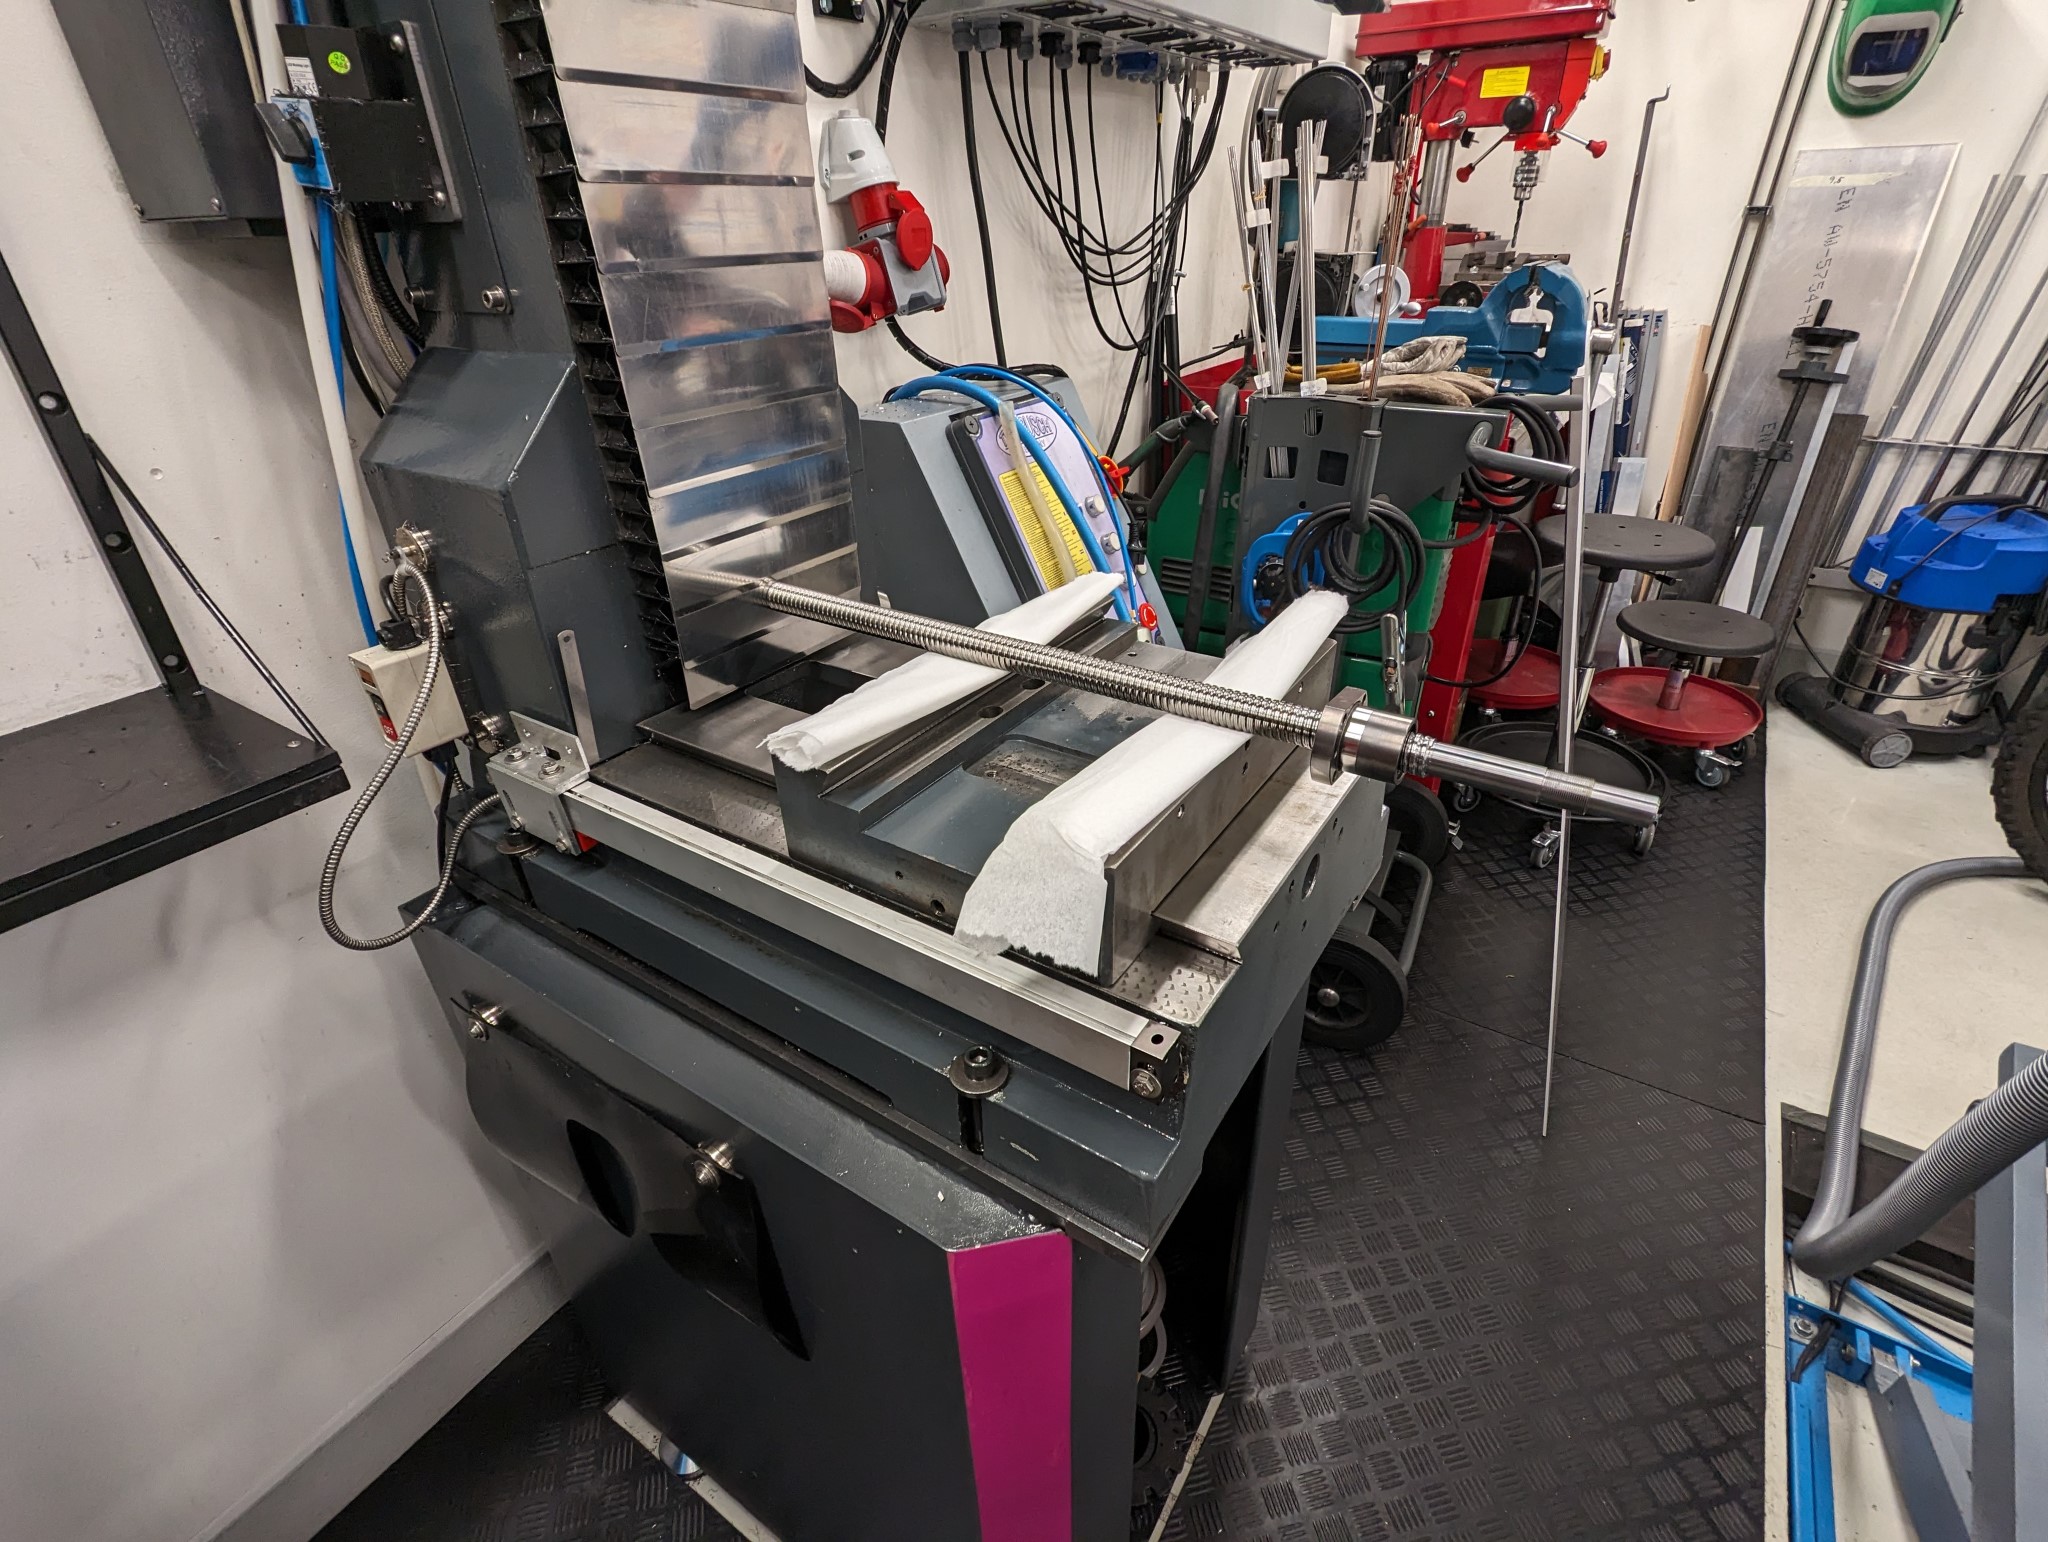
With the mount for the ball screw nut for the X axis done I could temporarily mount the ball screw and take some measurements for the bearing blocks and then design them in FreeCAD.


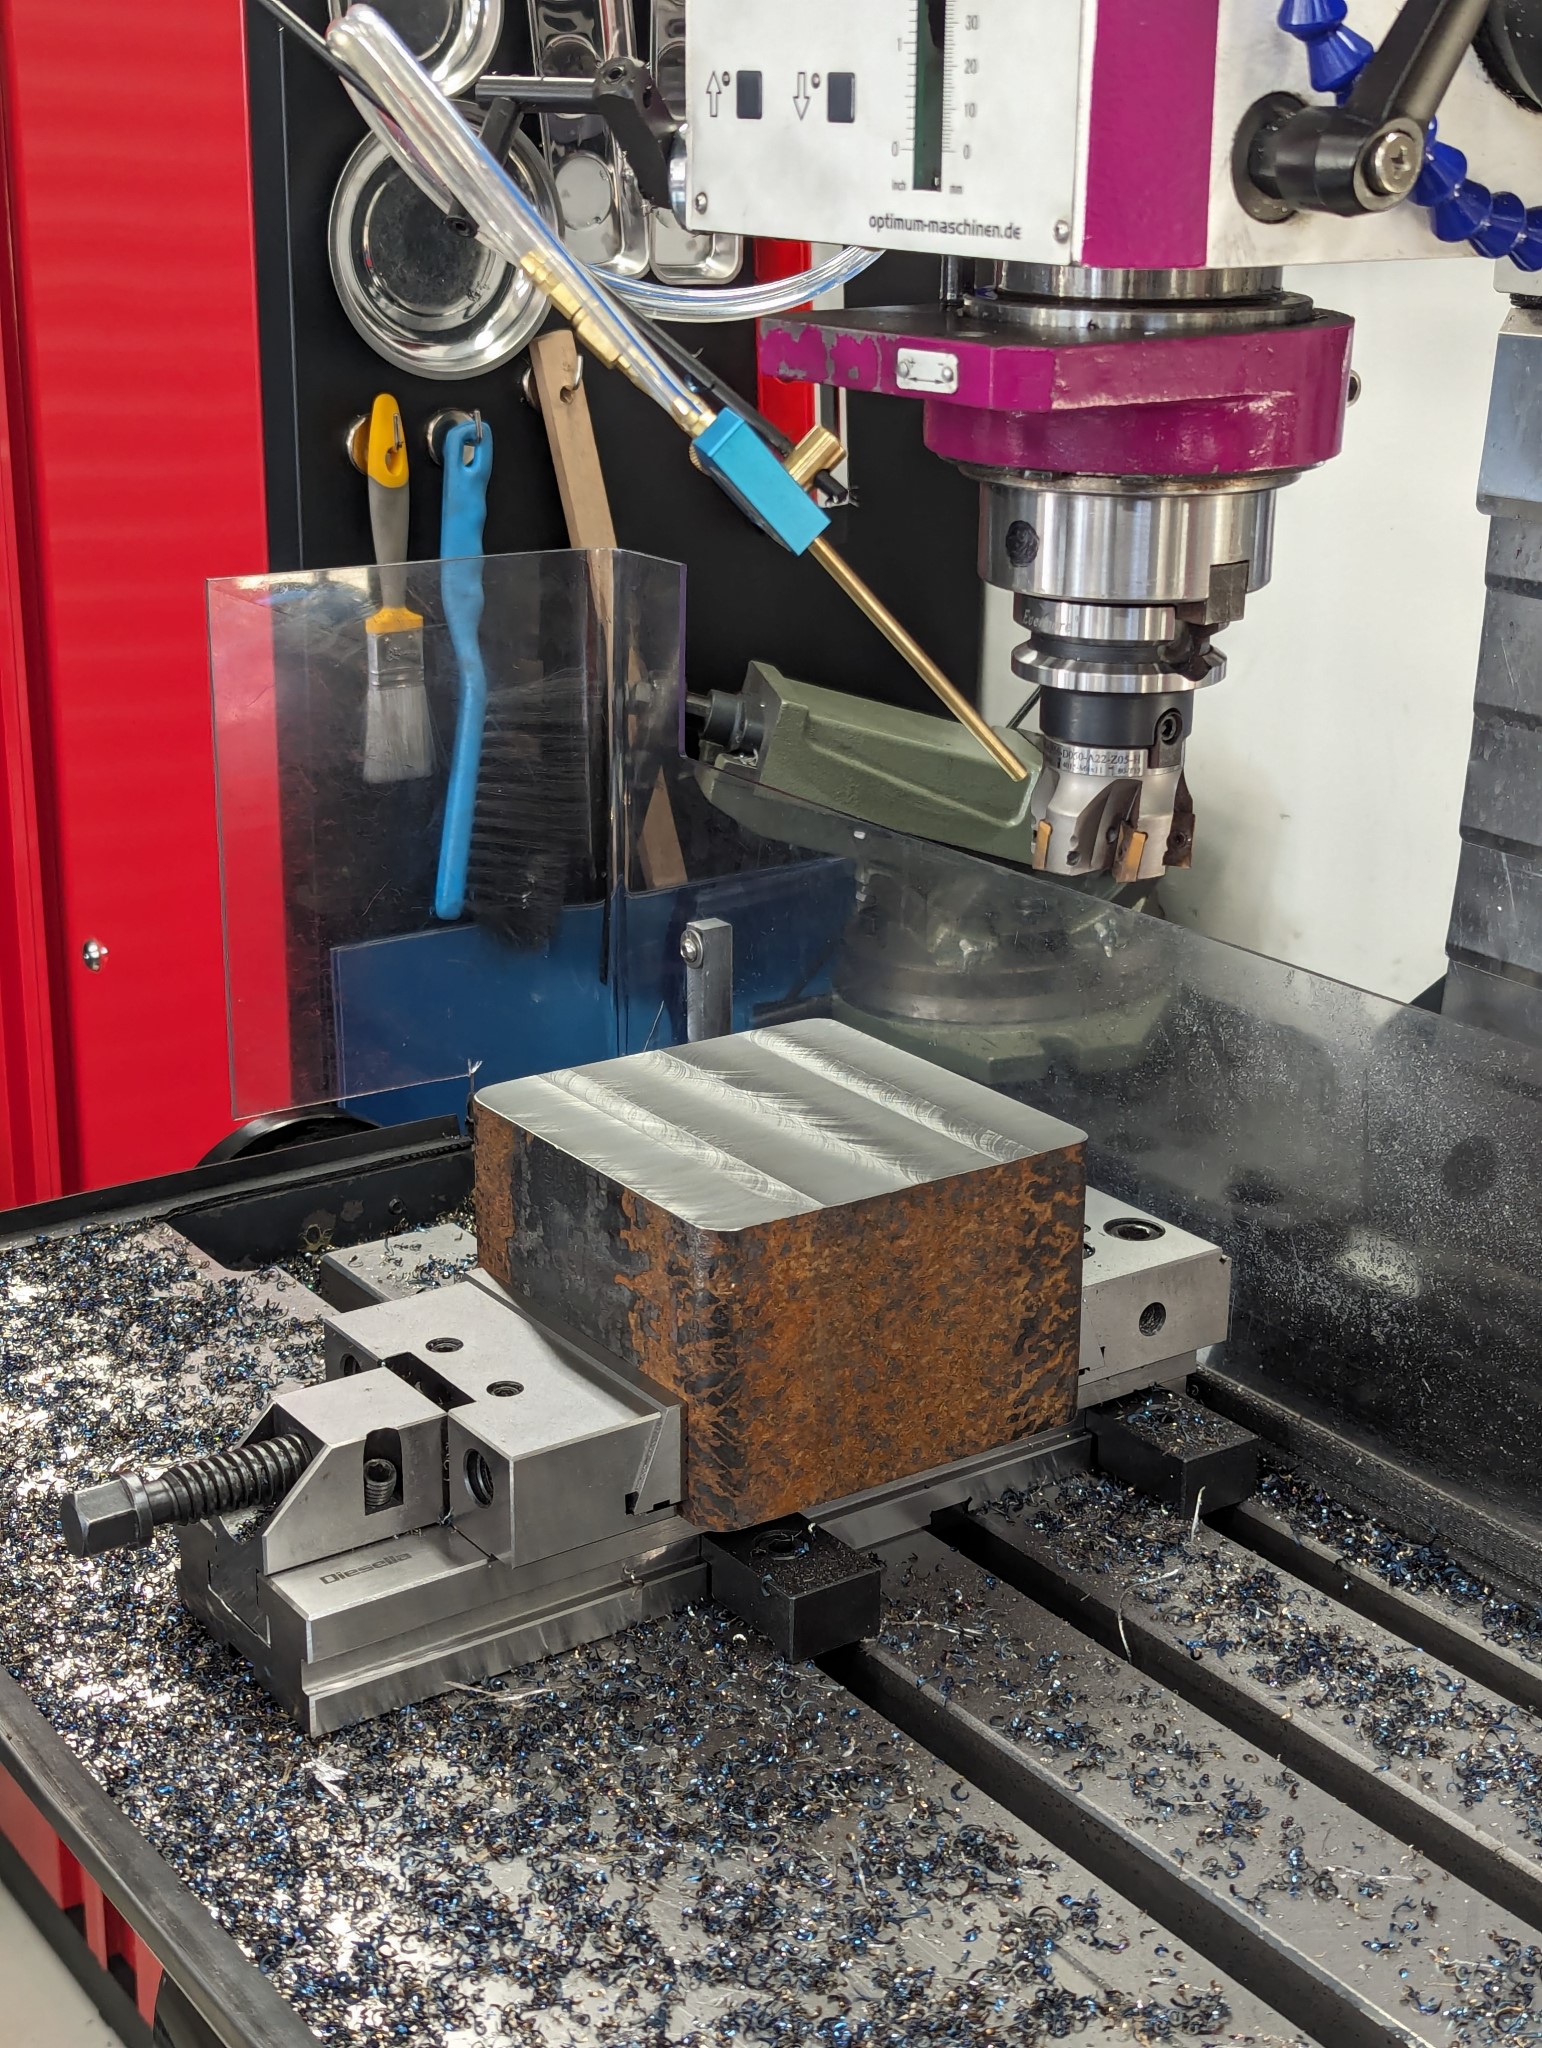
Then followed a lot more milling in steel...


Please Log in or Create an account to join the conversation.

More
2 years 8 months ago #293698 by Unlogic


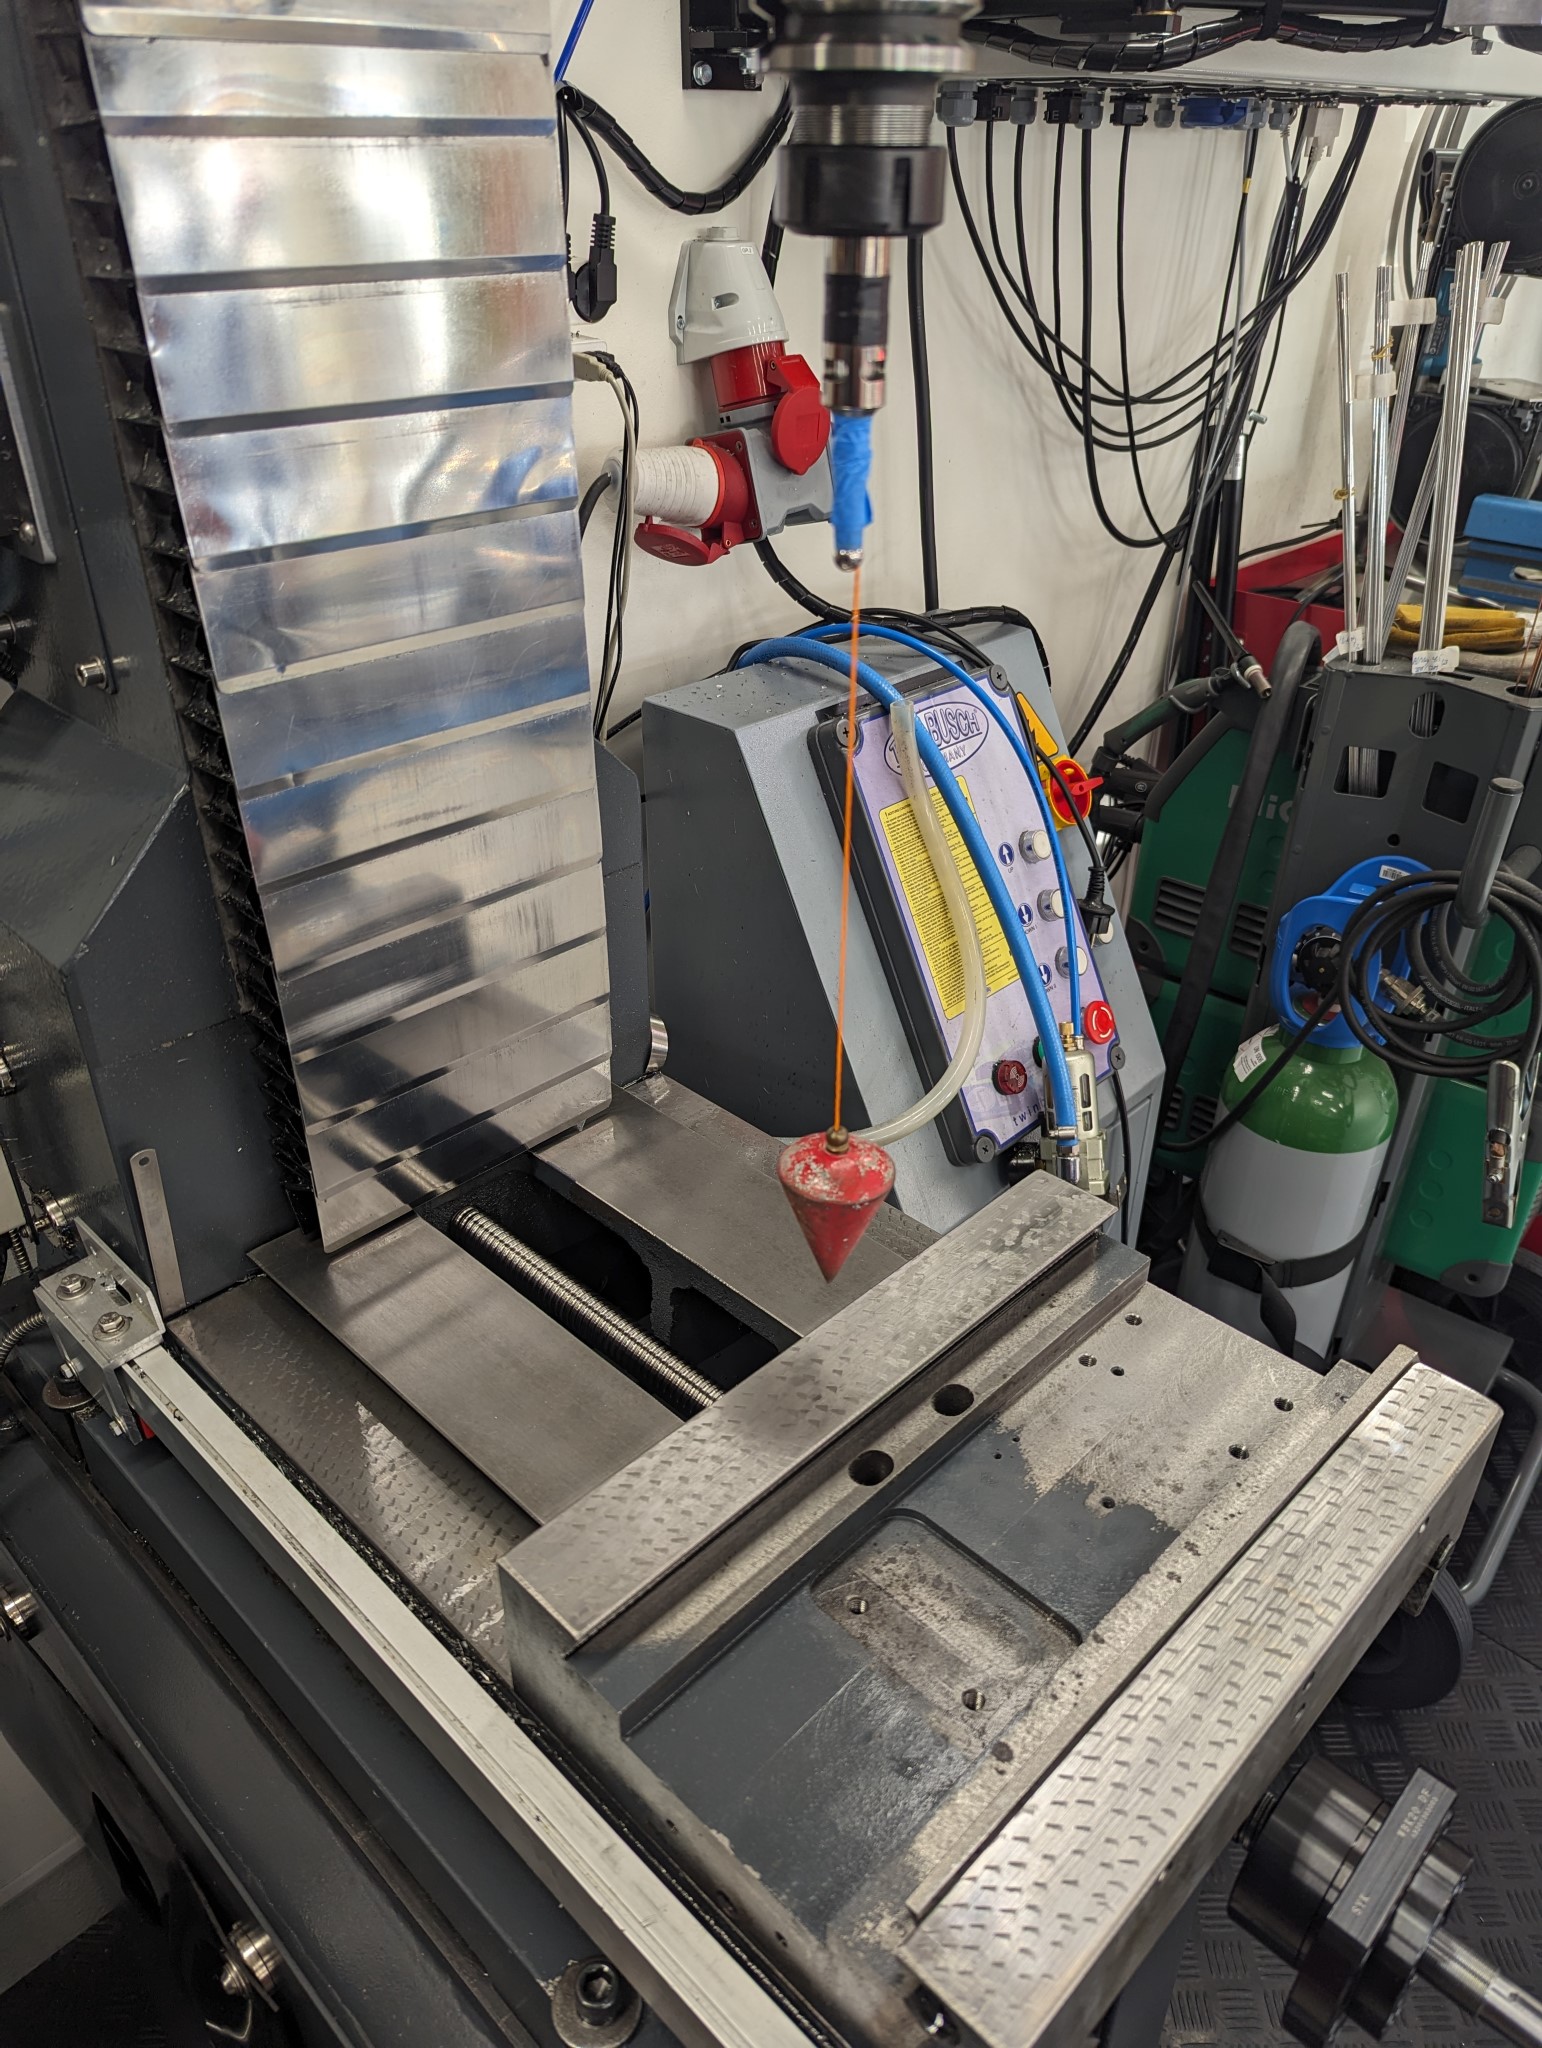
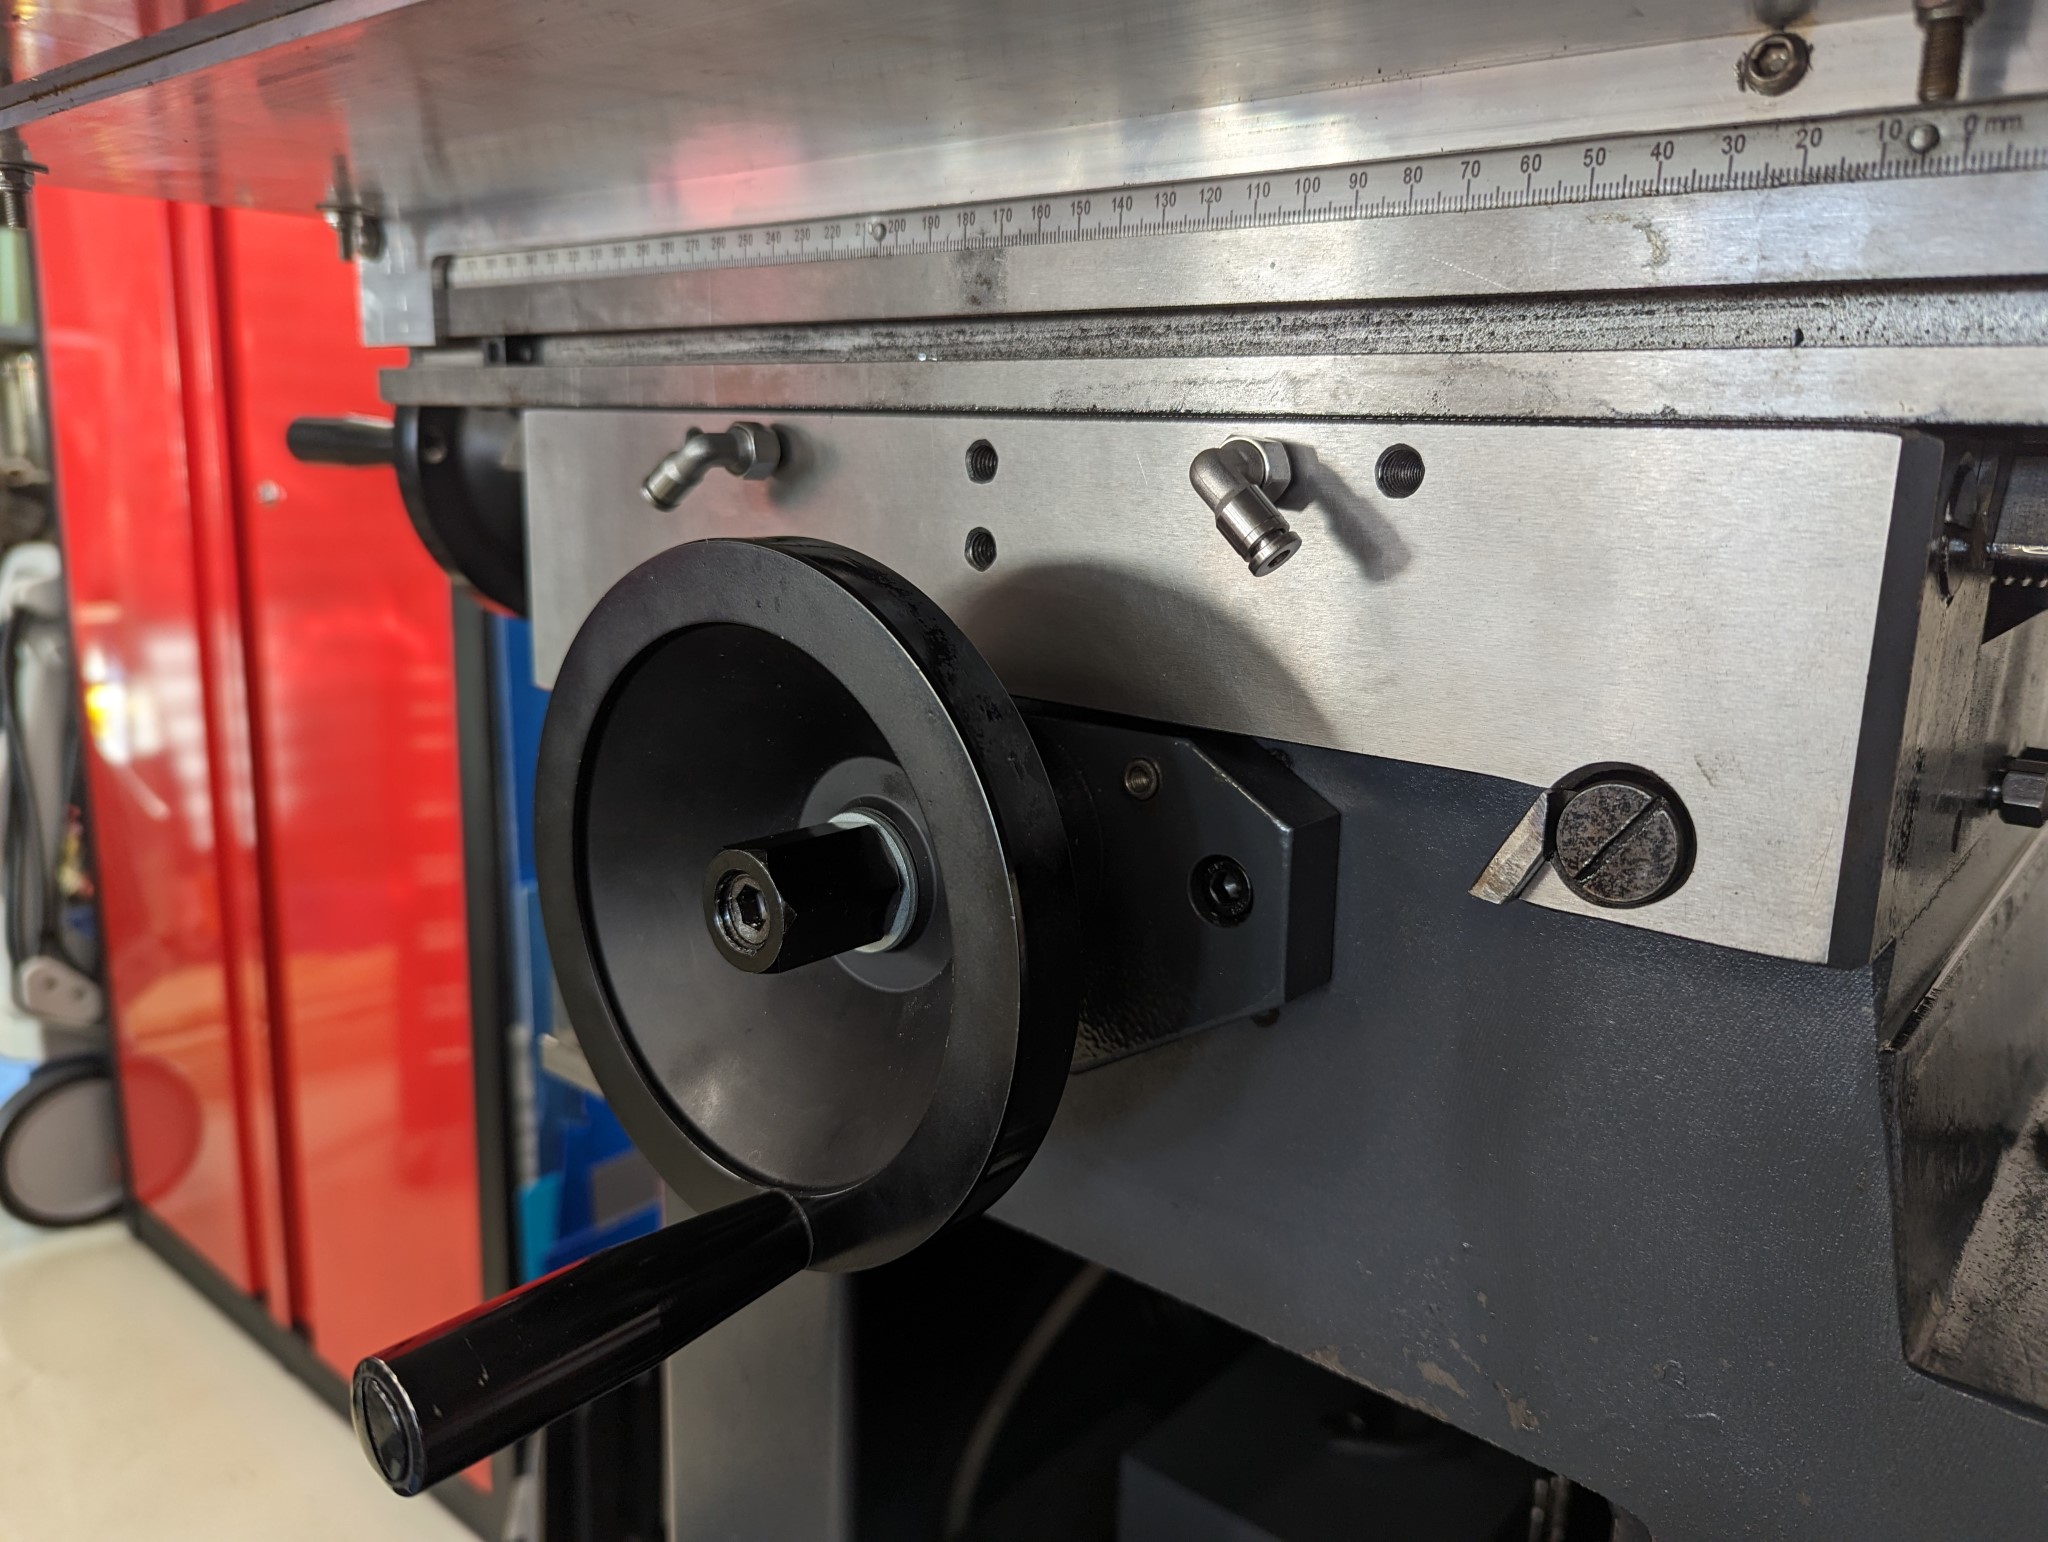
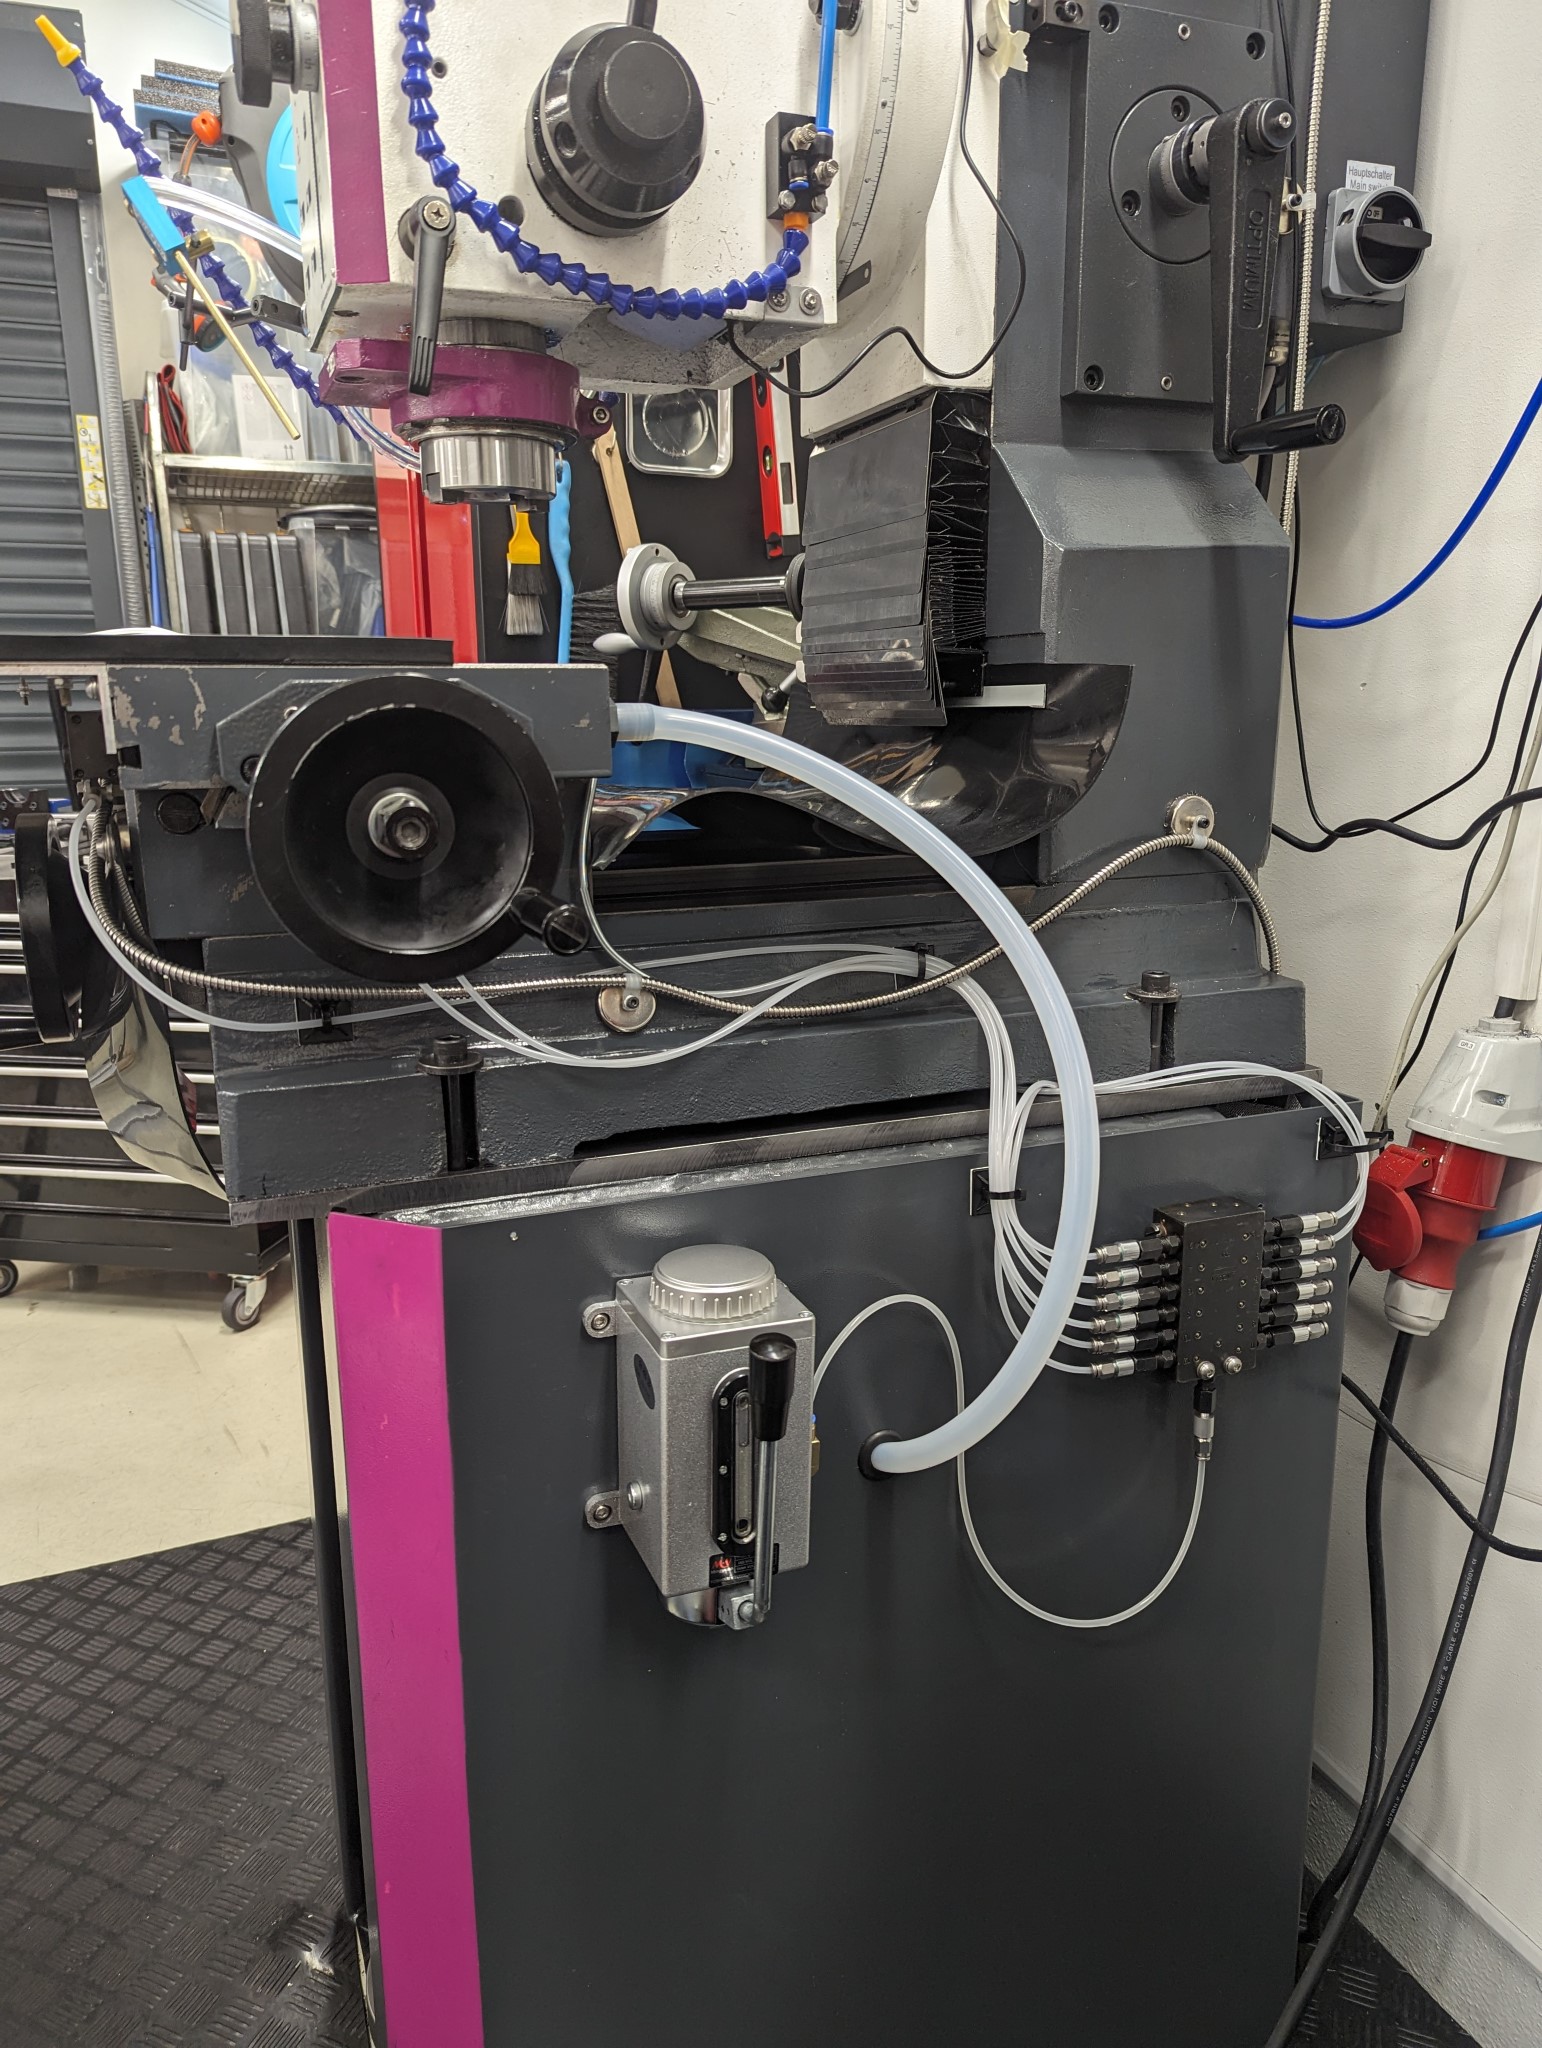
With the bearing block mounts done for the X-axis I could proceed to tear down the machine even further and actually install the central lubrication system and measure the parts needed for the Y-axis.


Please Log in or Create an account to join the conversation.

More
2 years 8 months ago #293700 by Unlogic
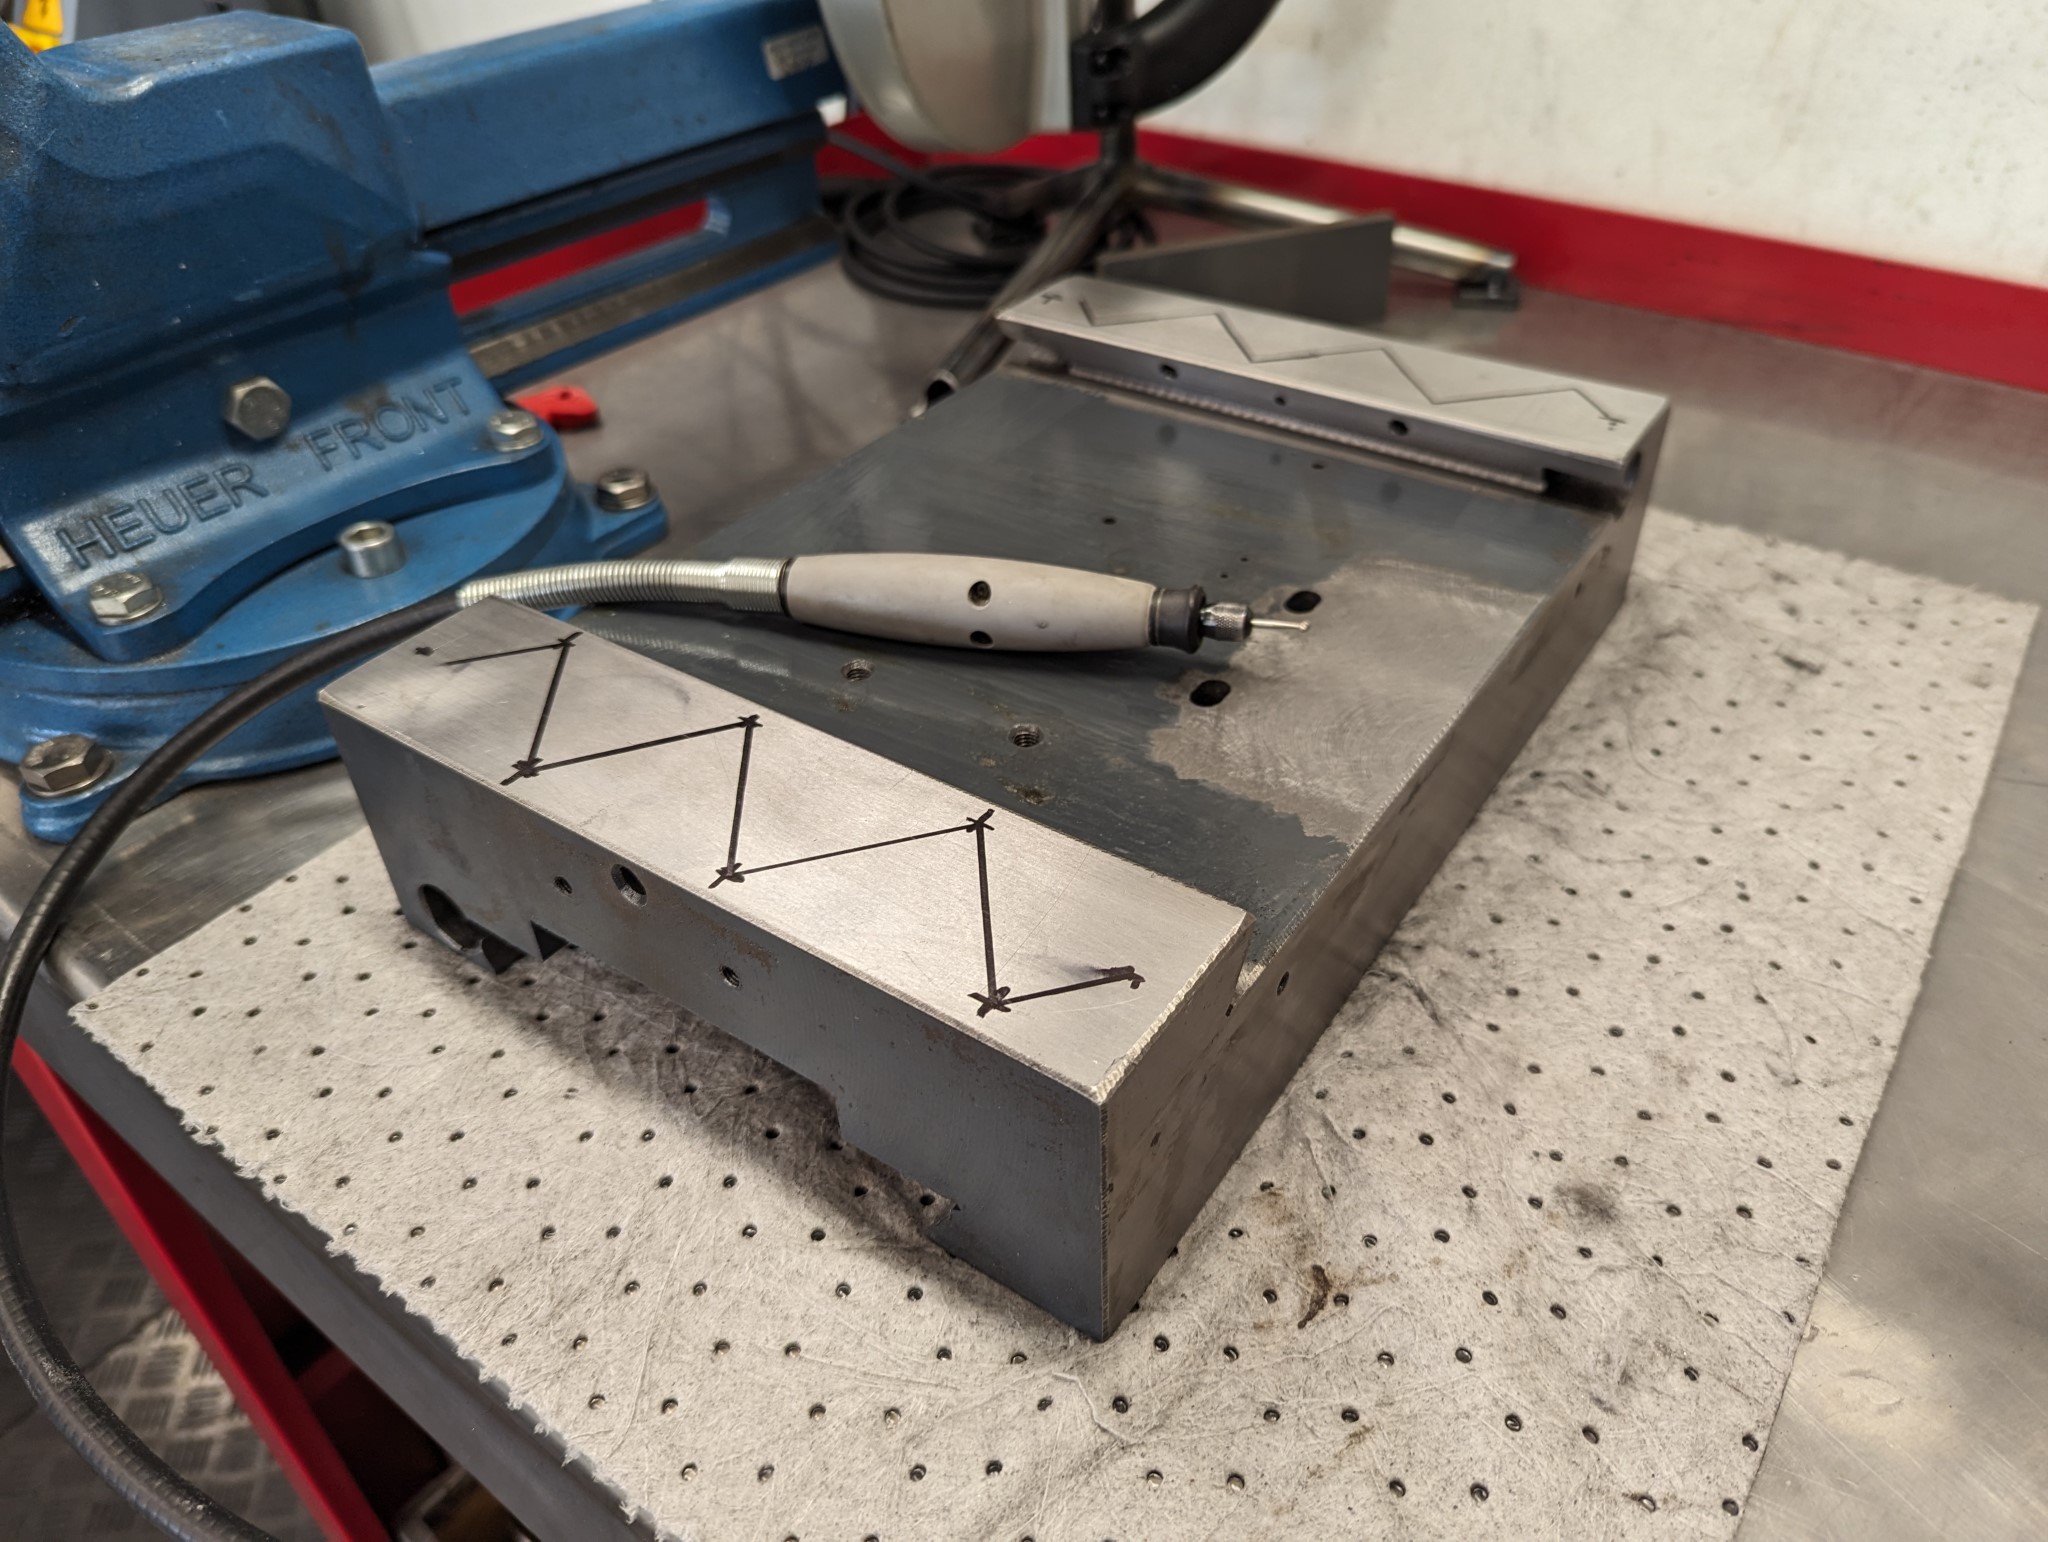
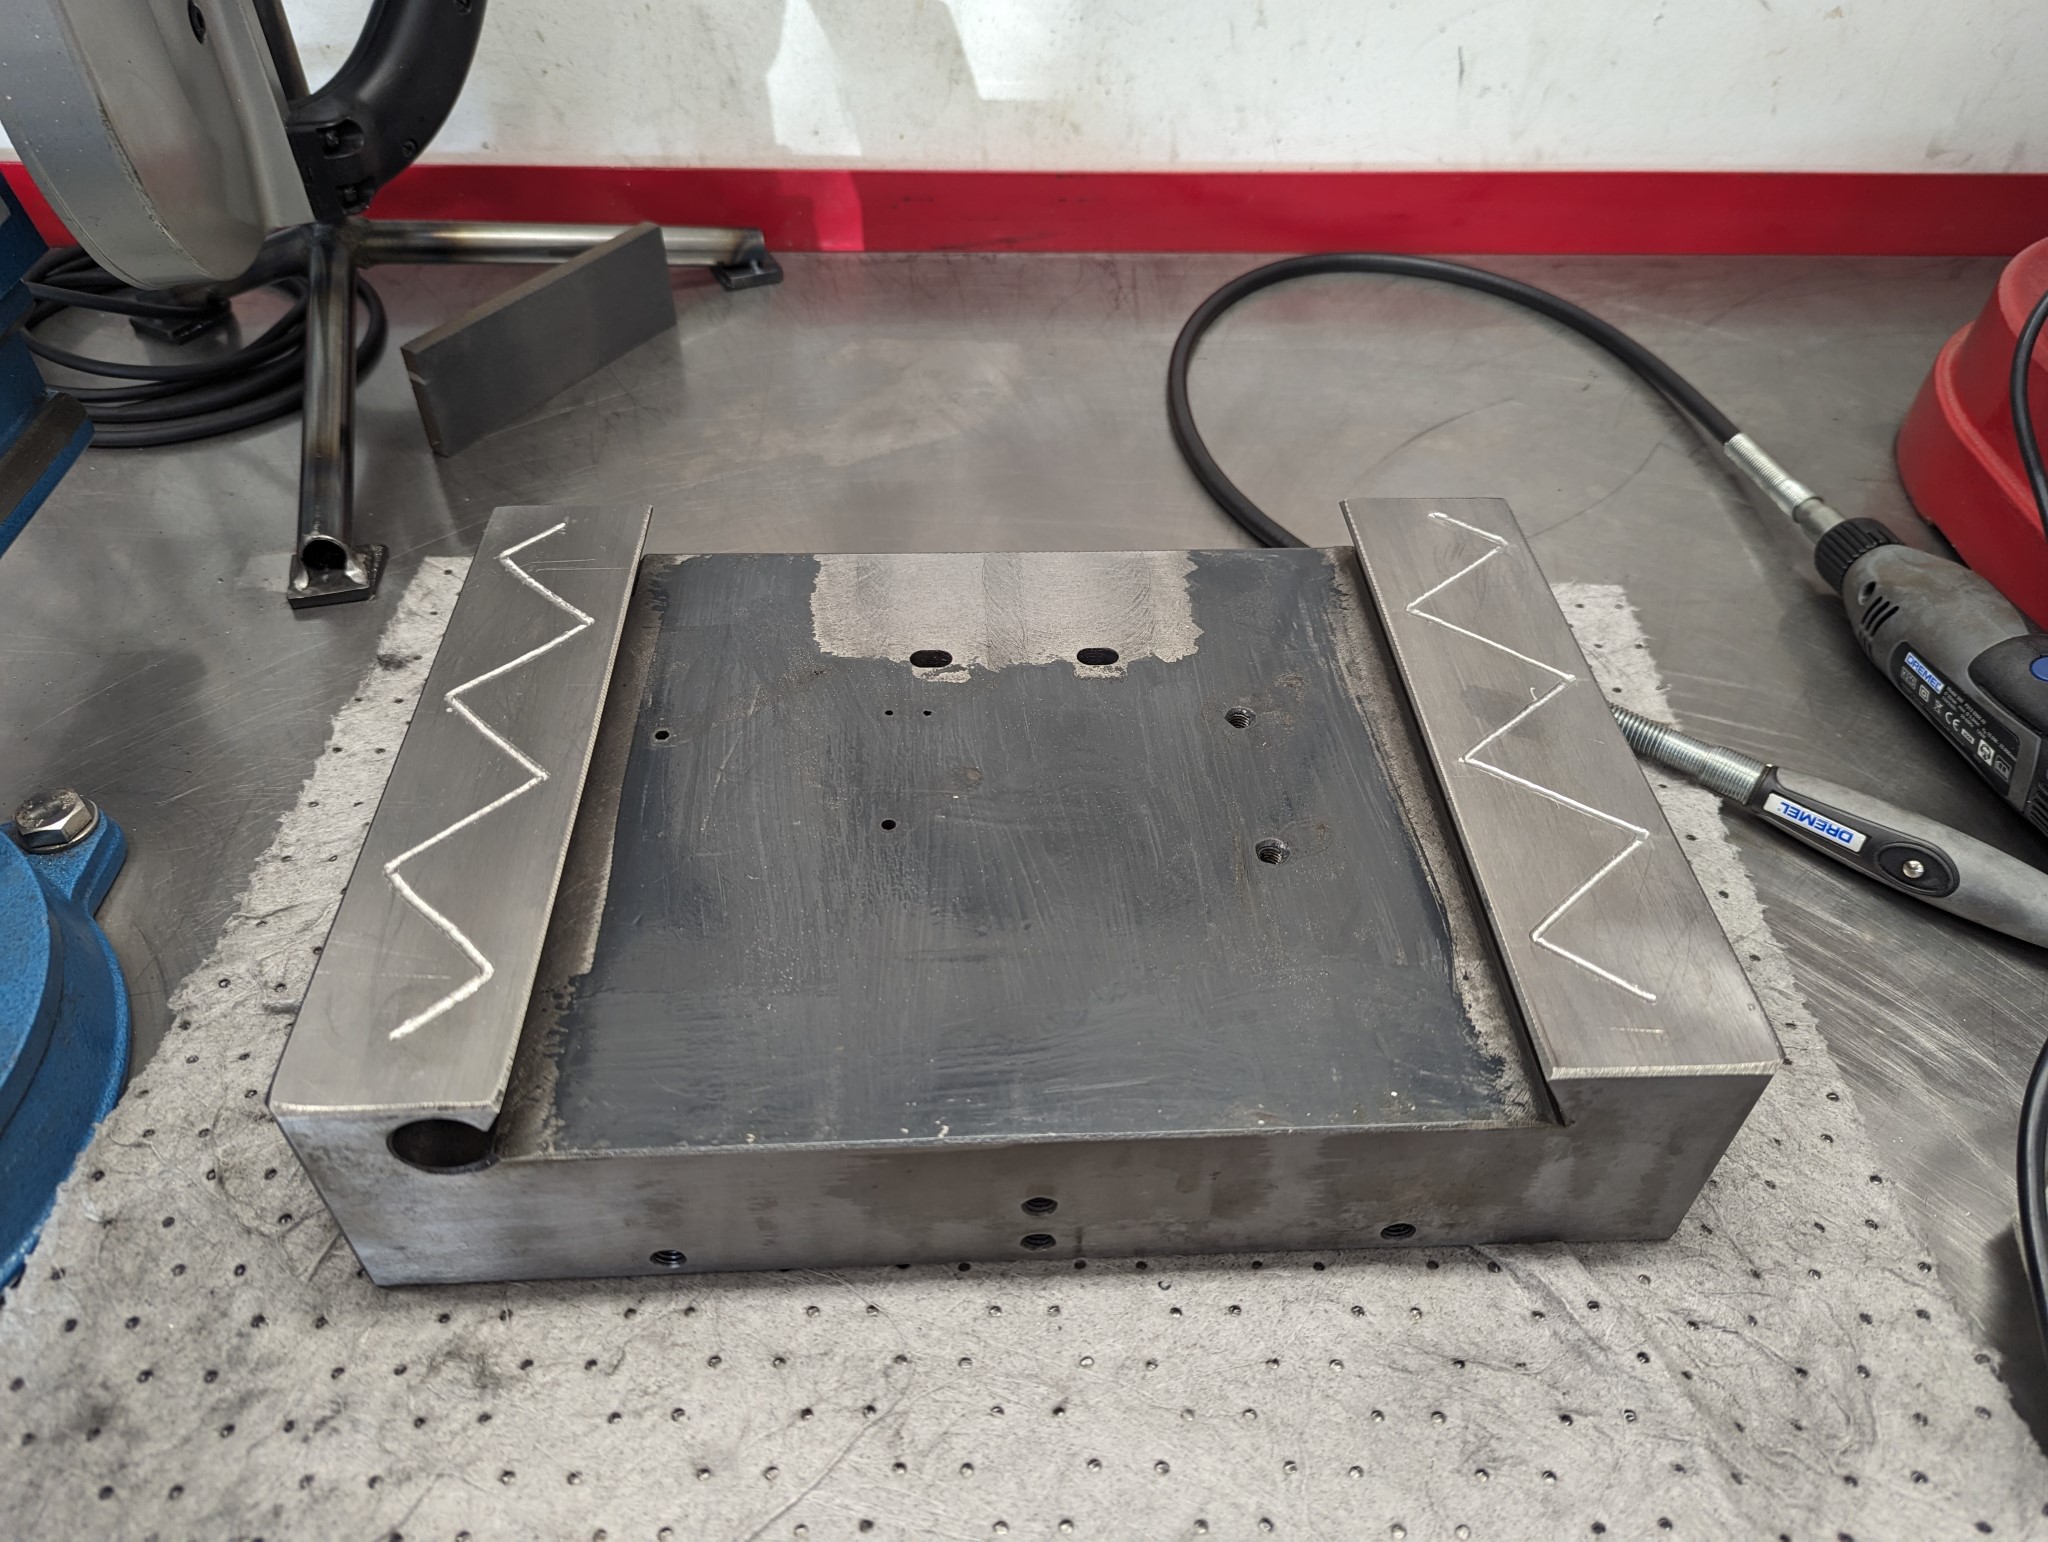
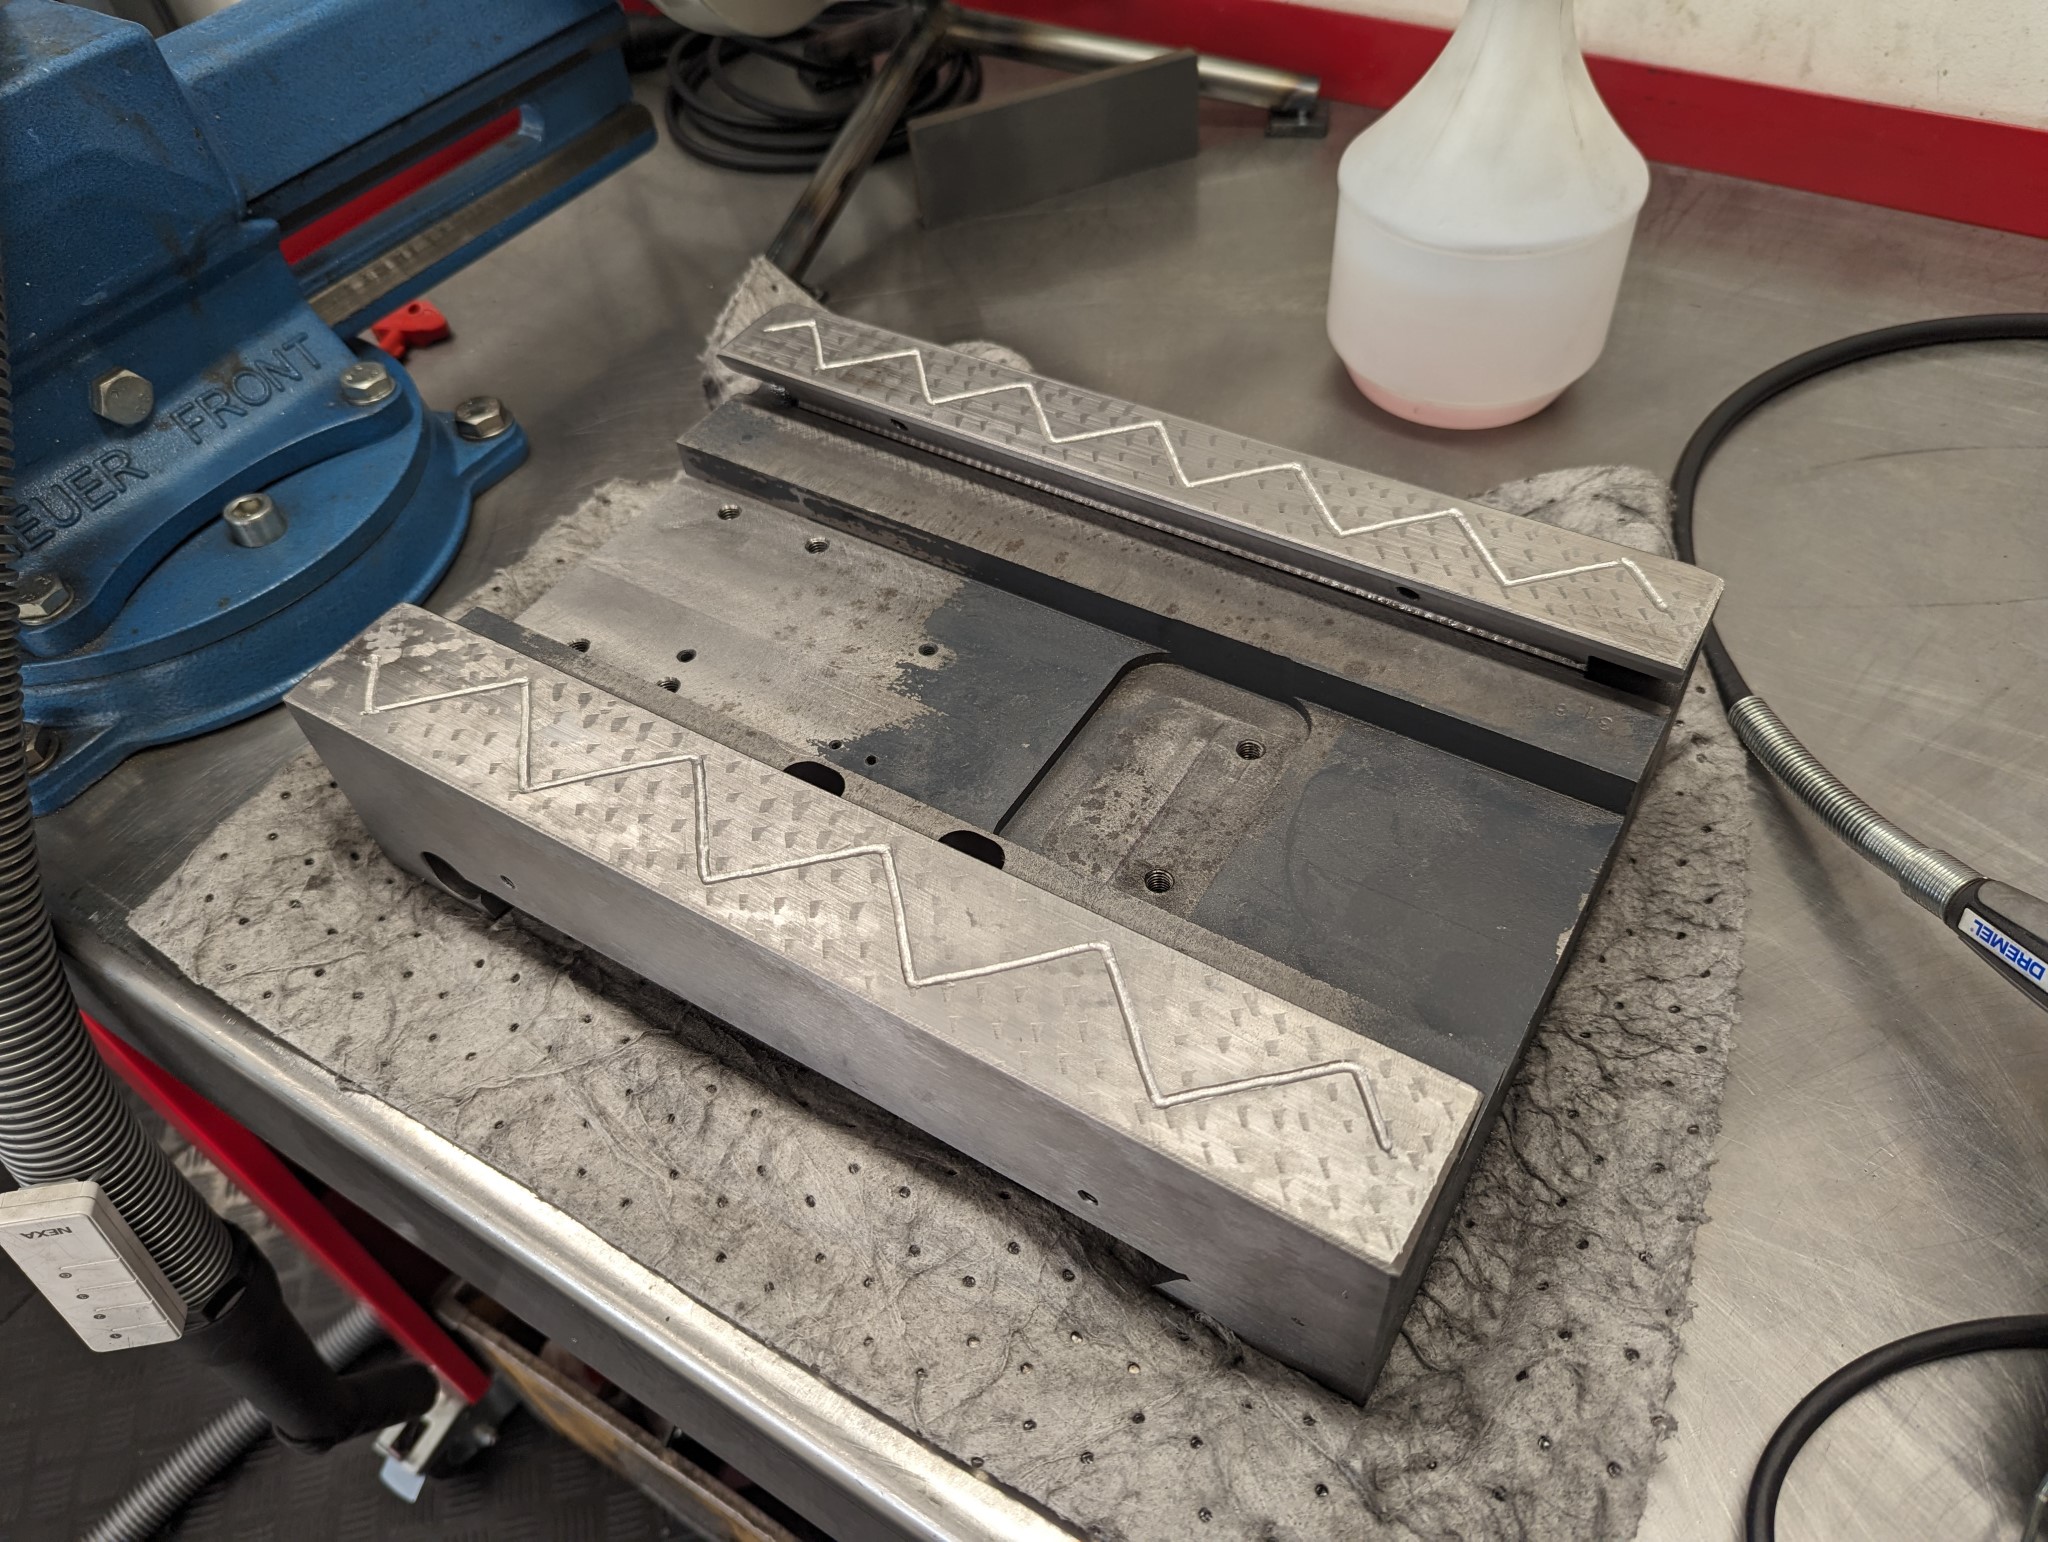
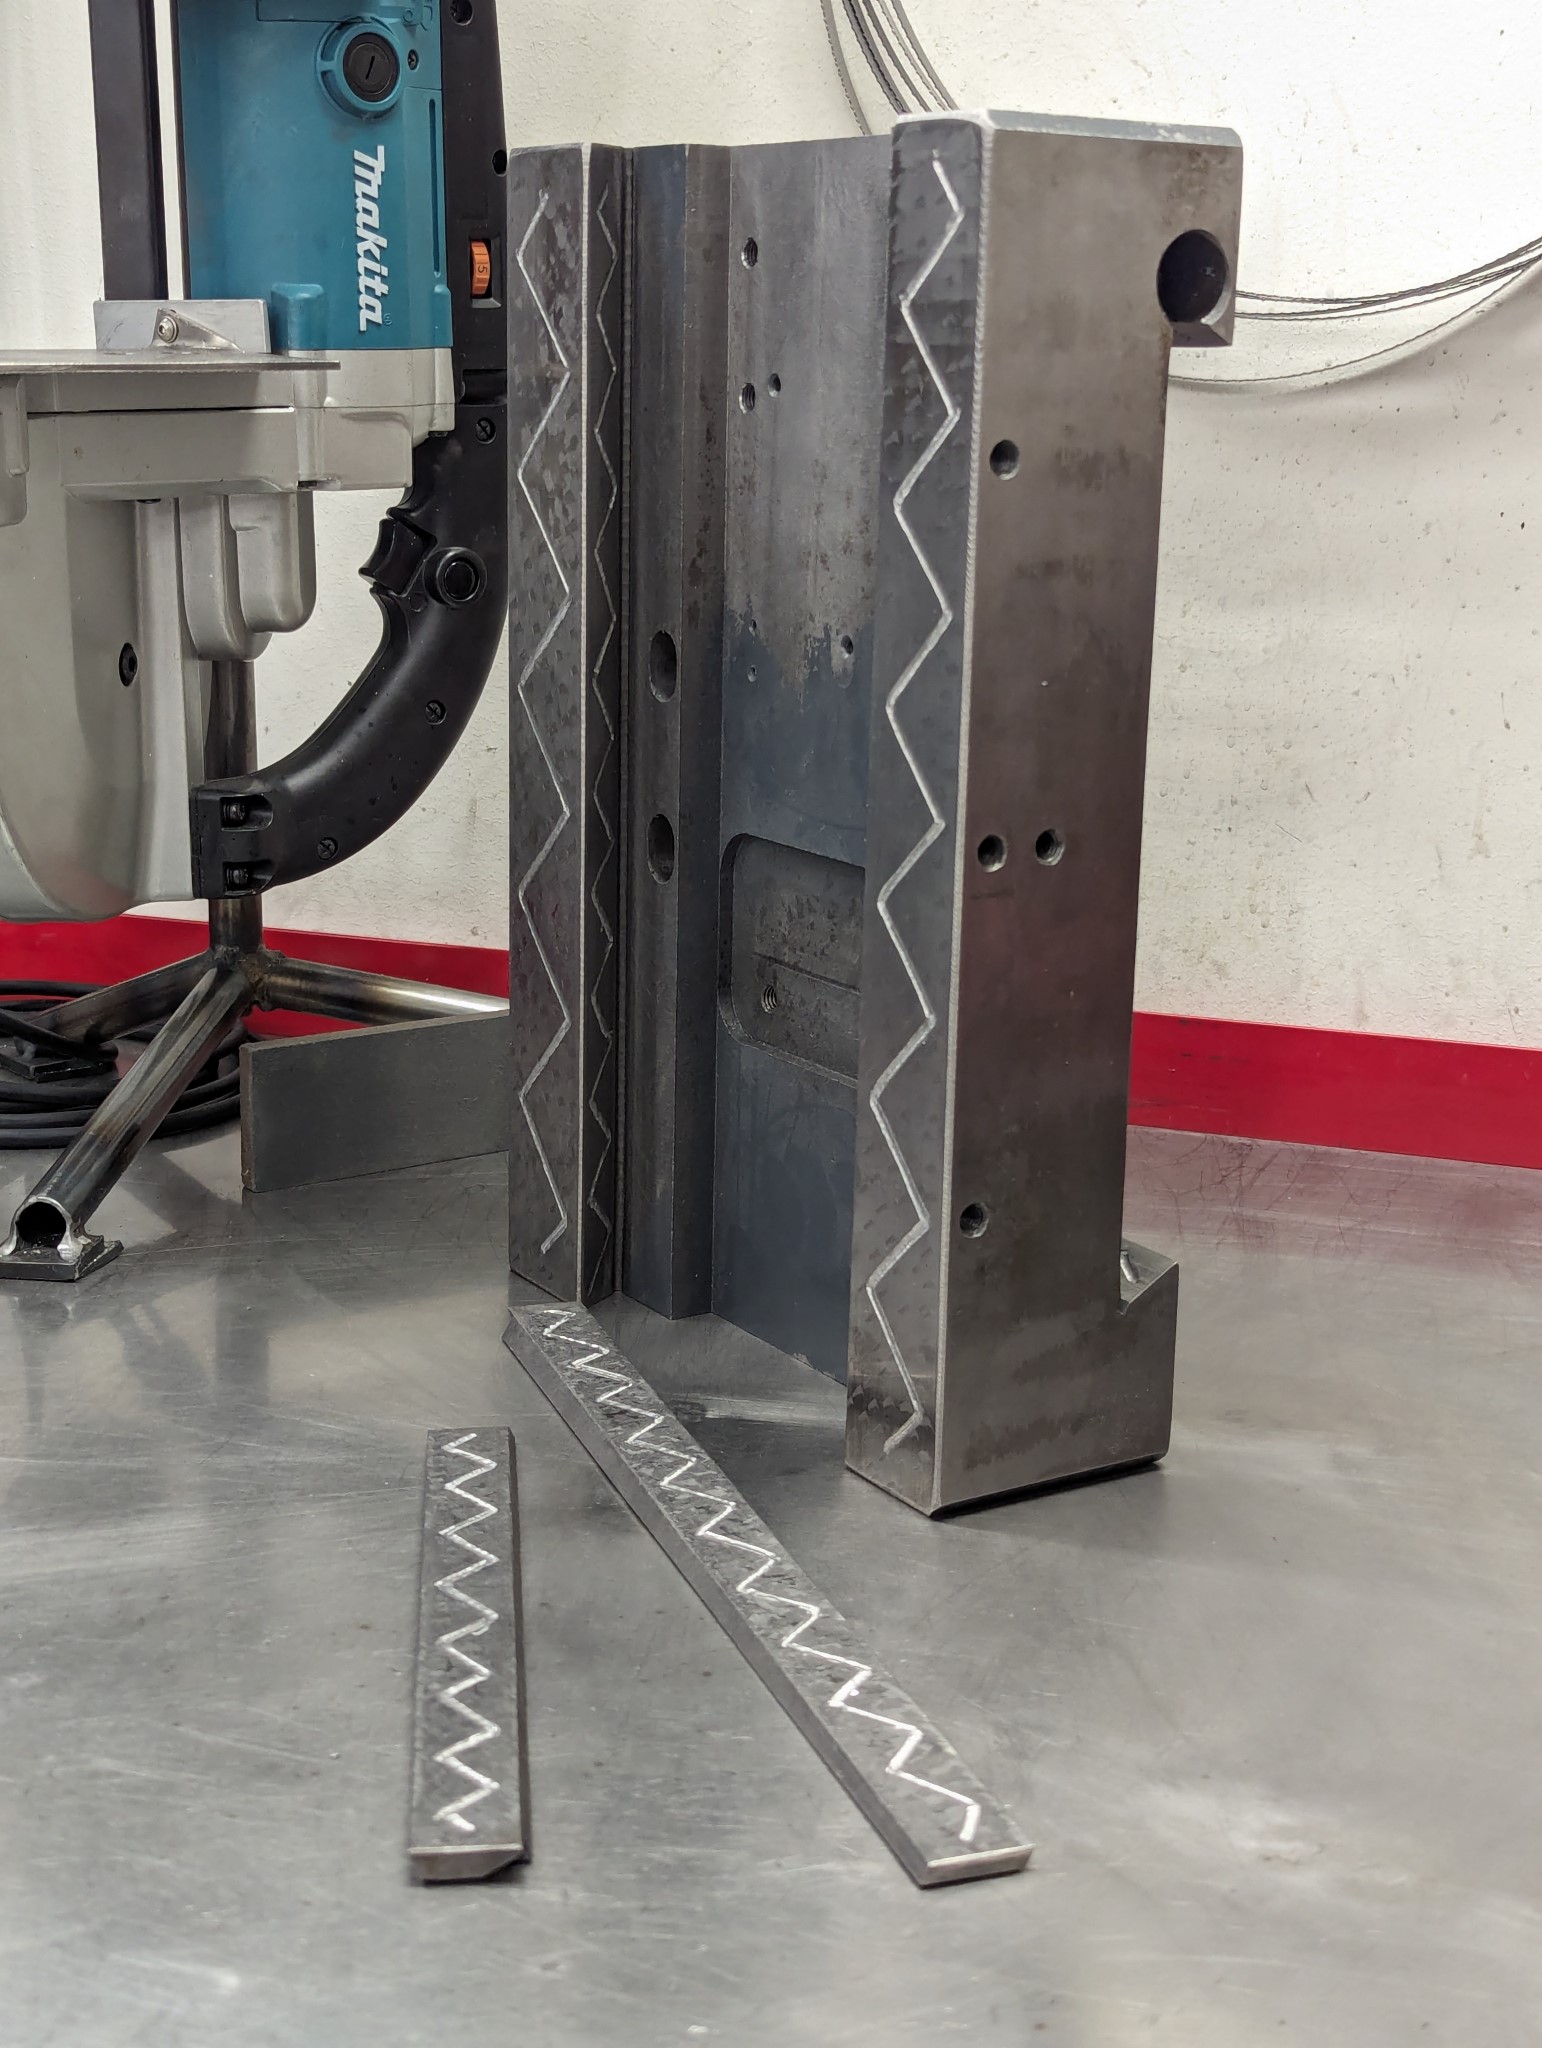
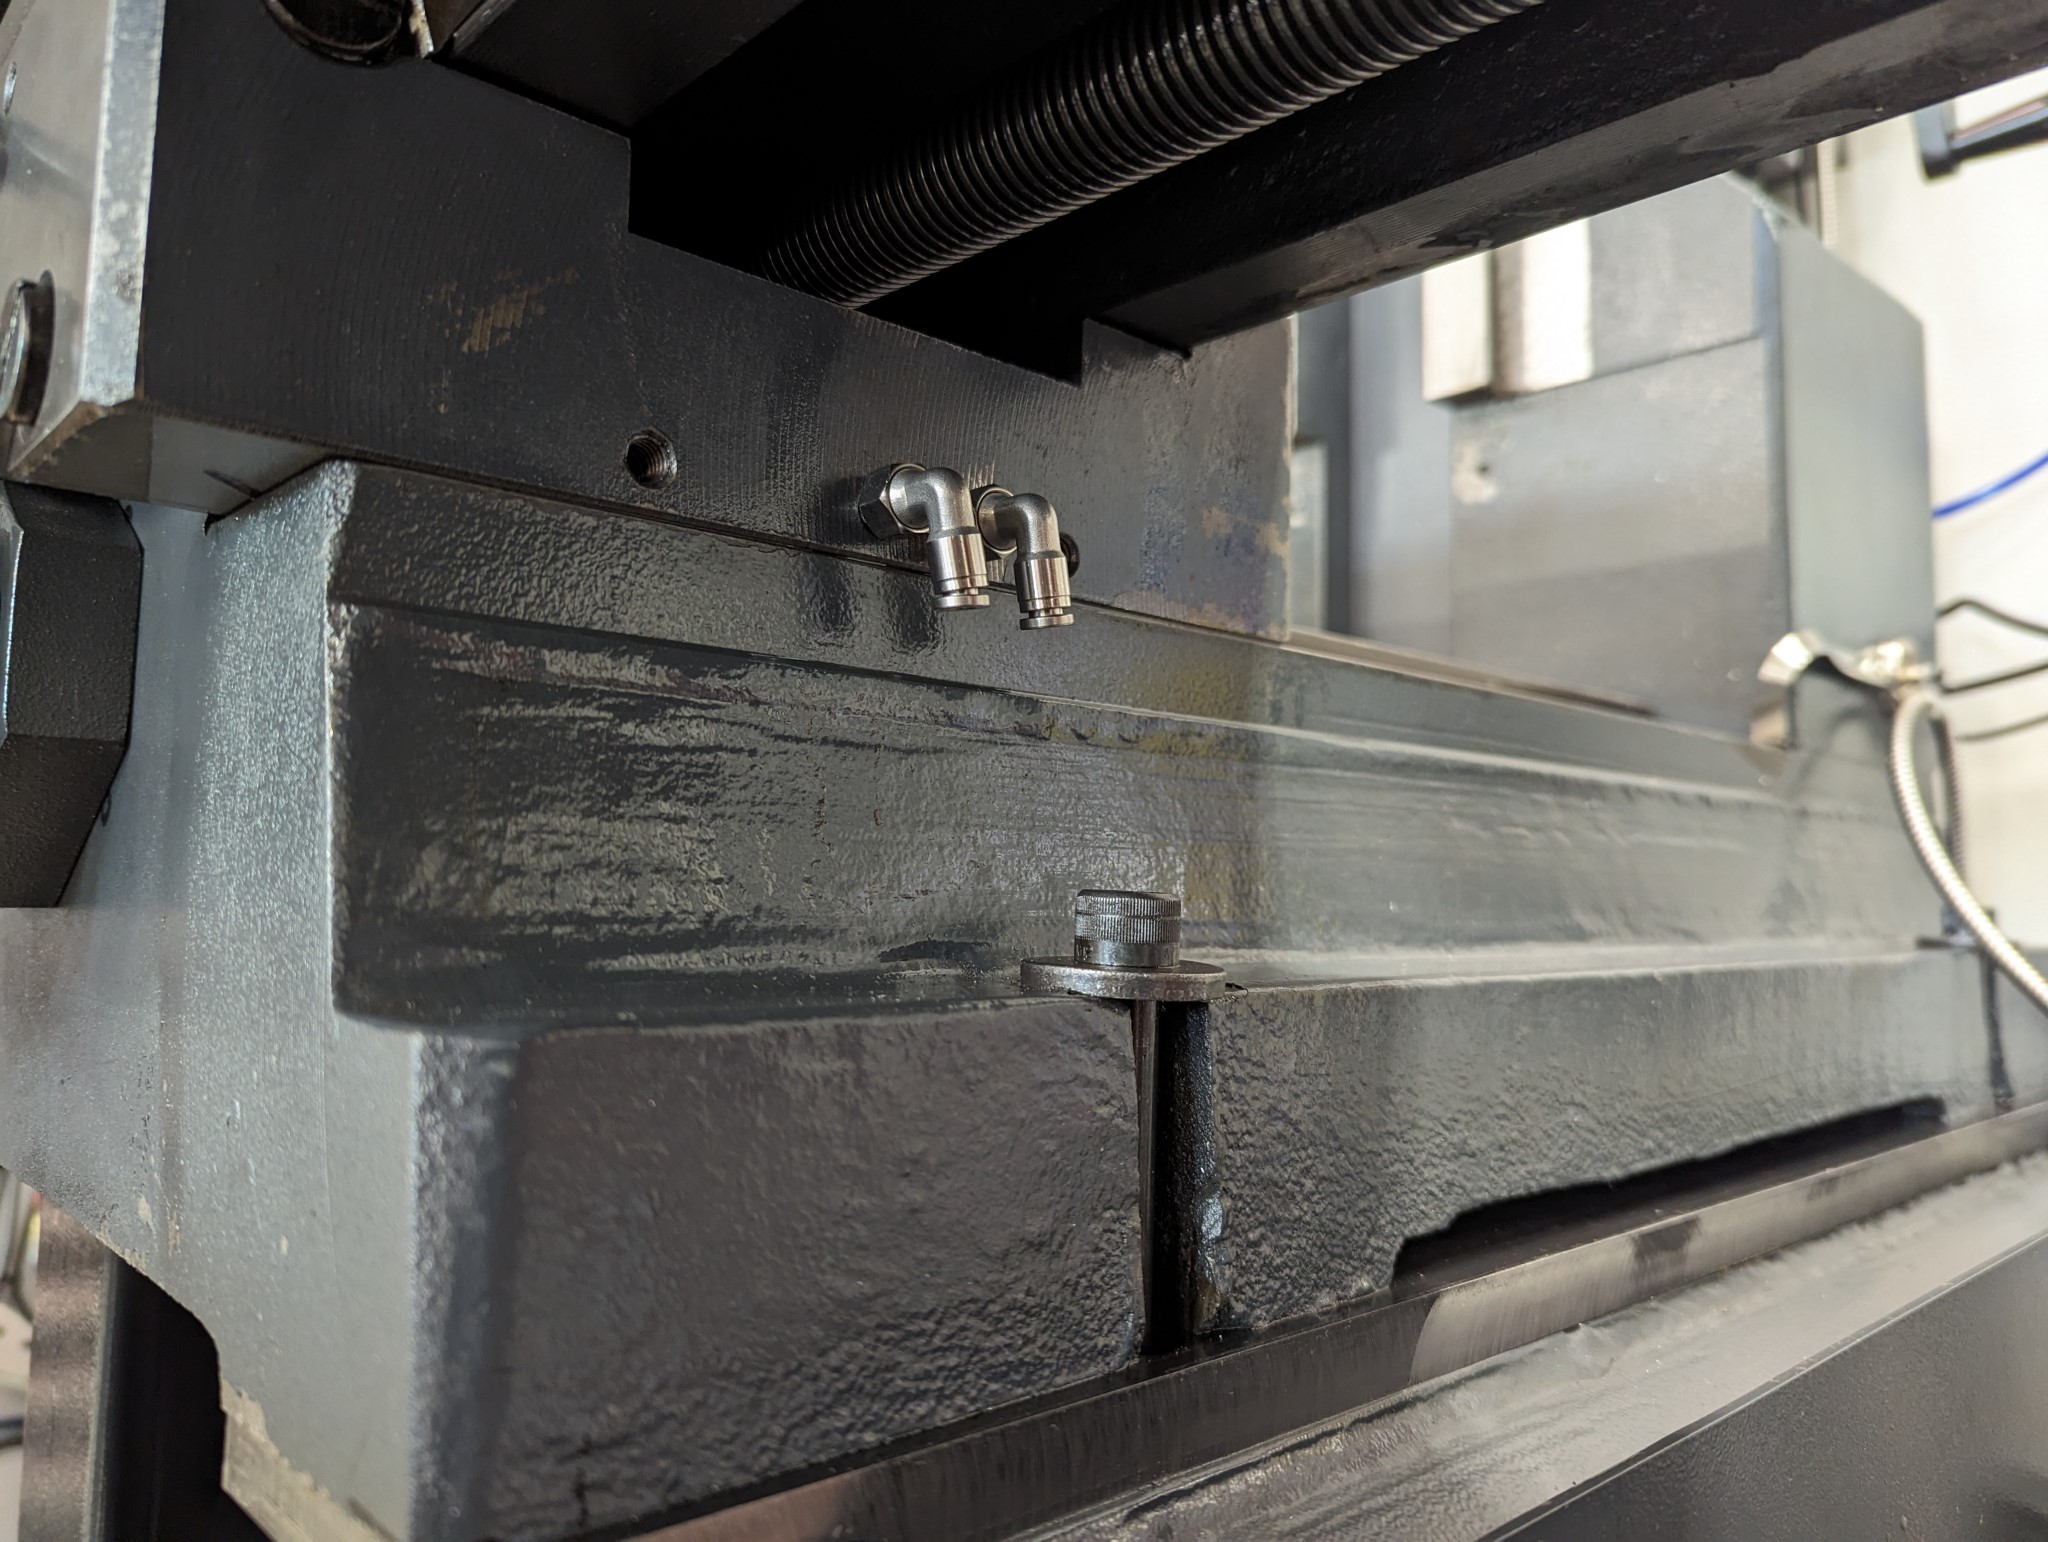
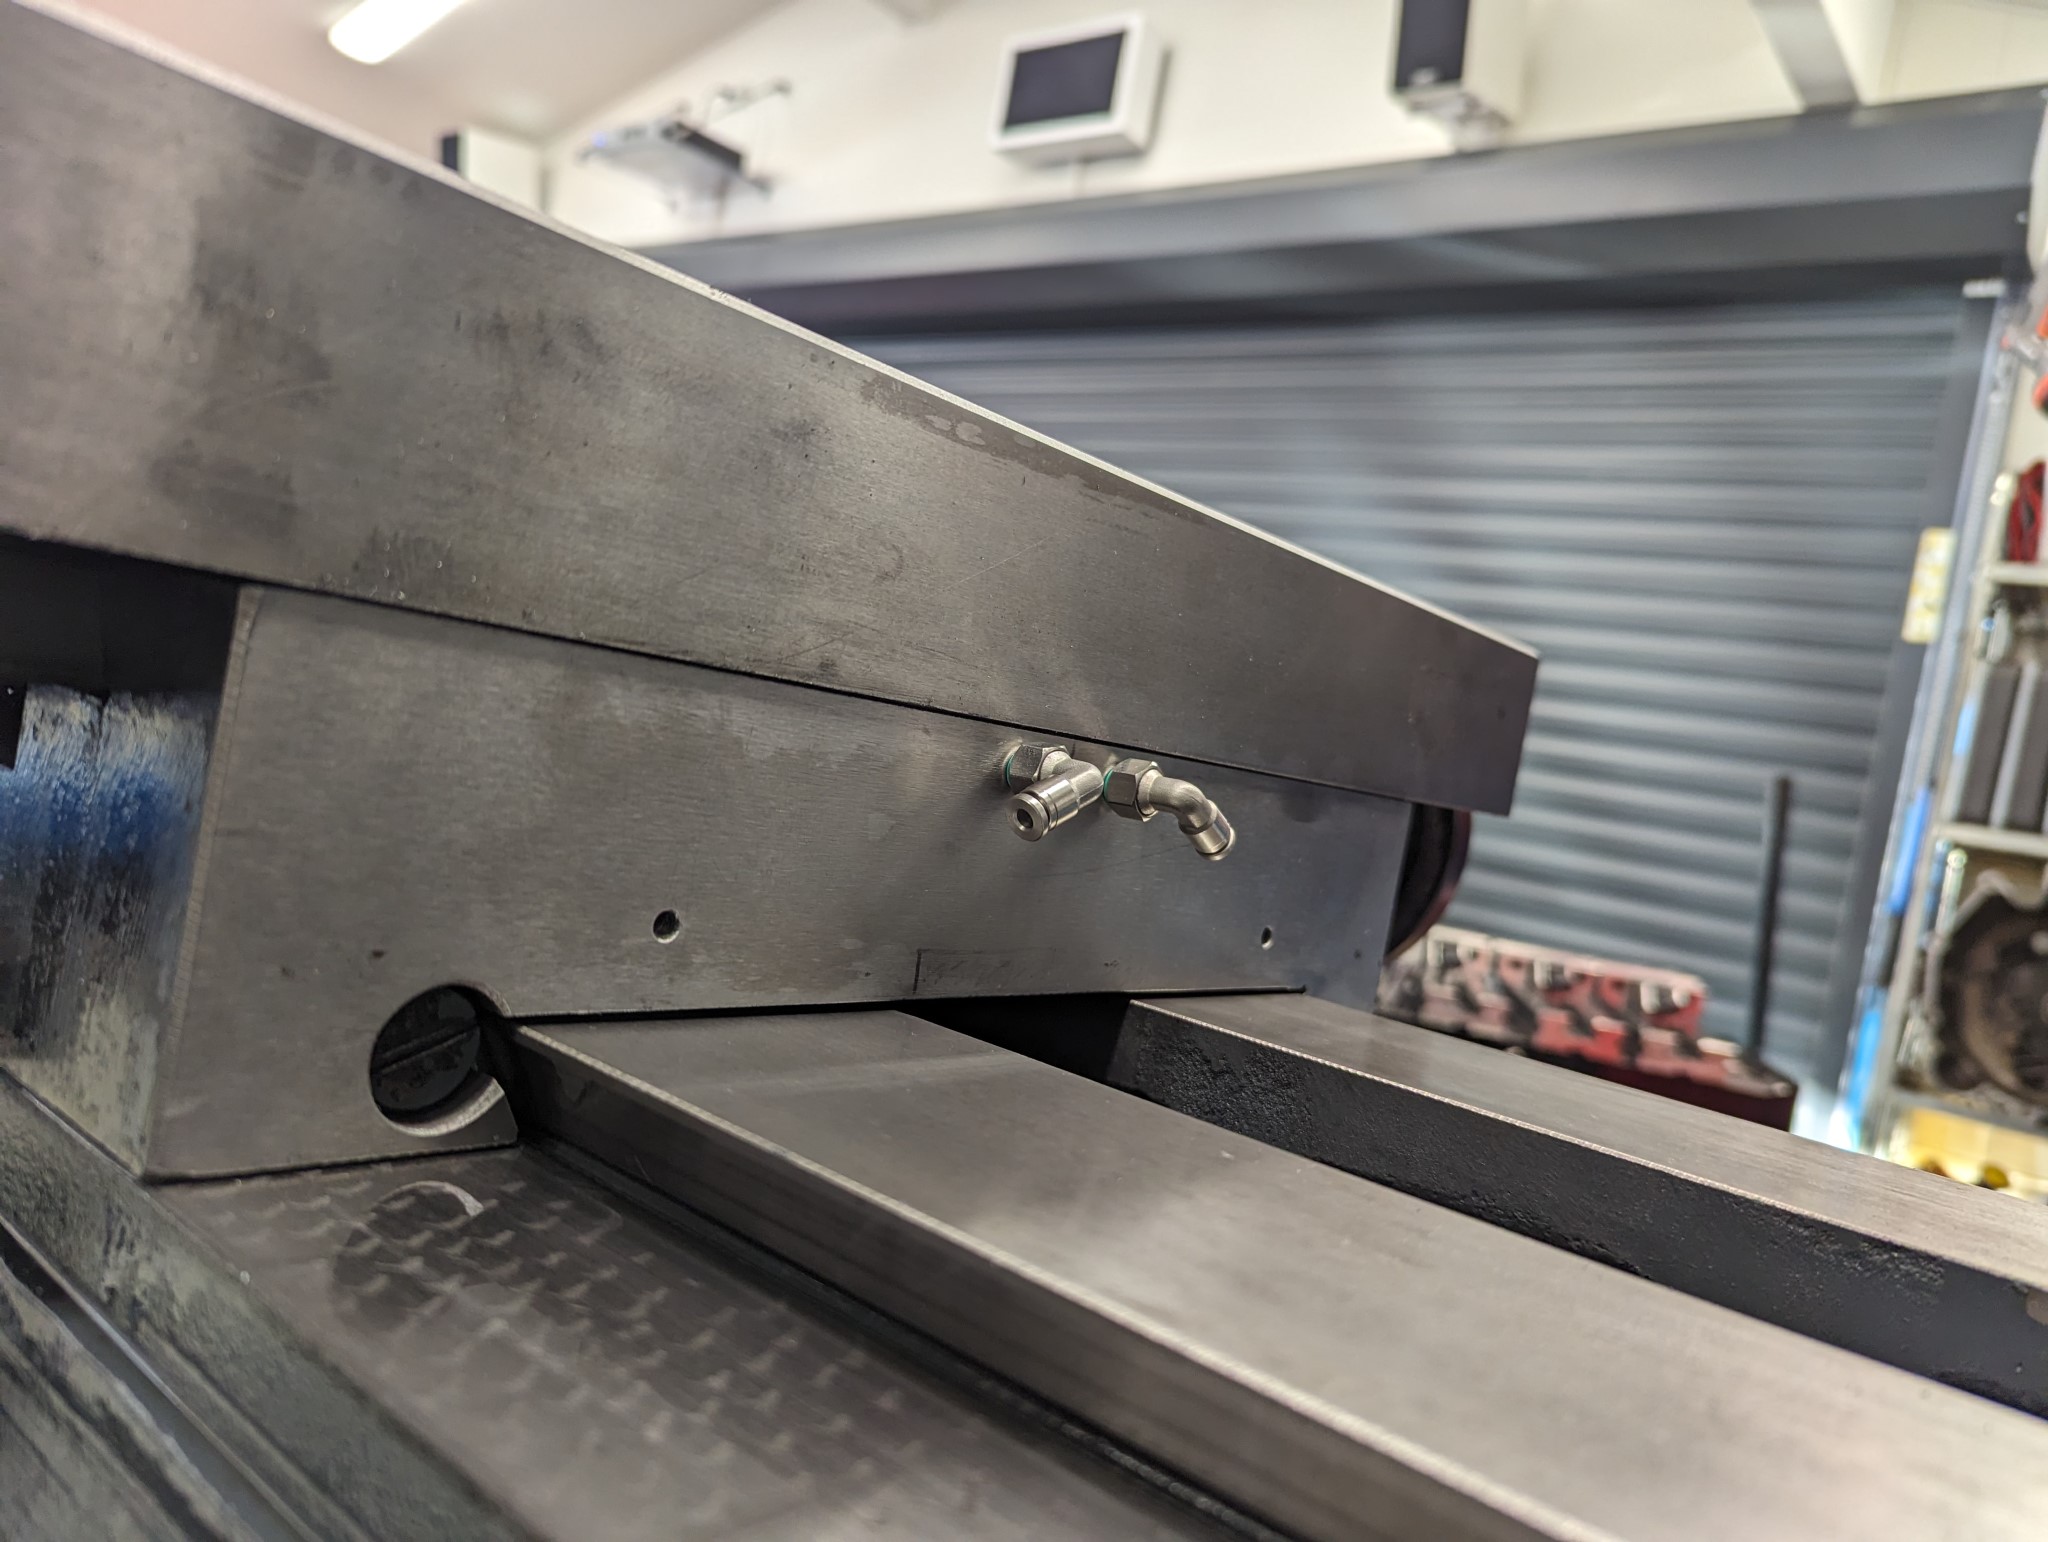
Since I have only one milling machine I had to make the grooves for the oil in the saddle using a Dremel which took a while but gave an acceptable result in the end.


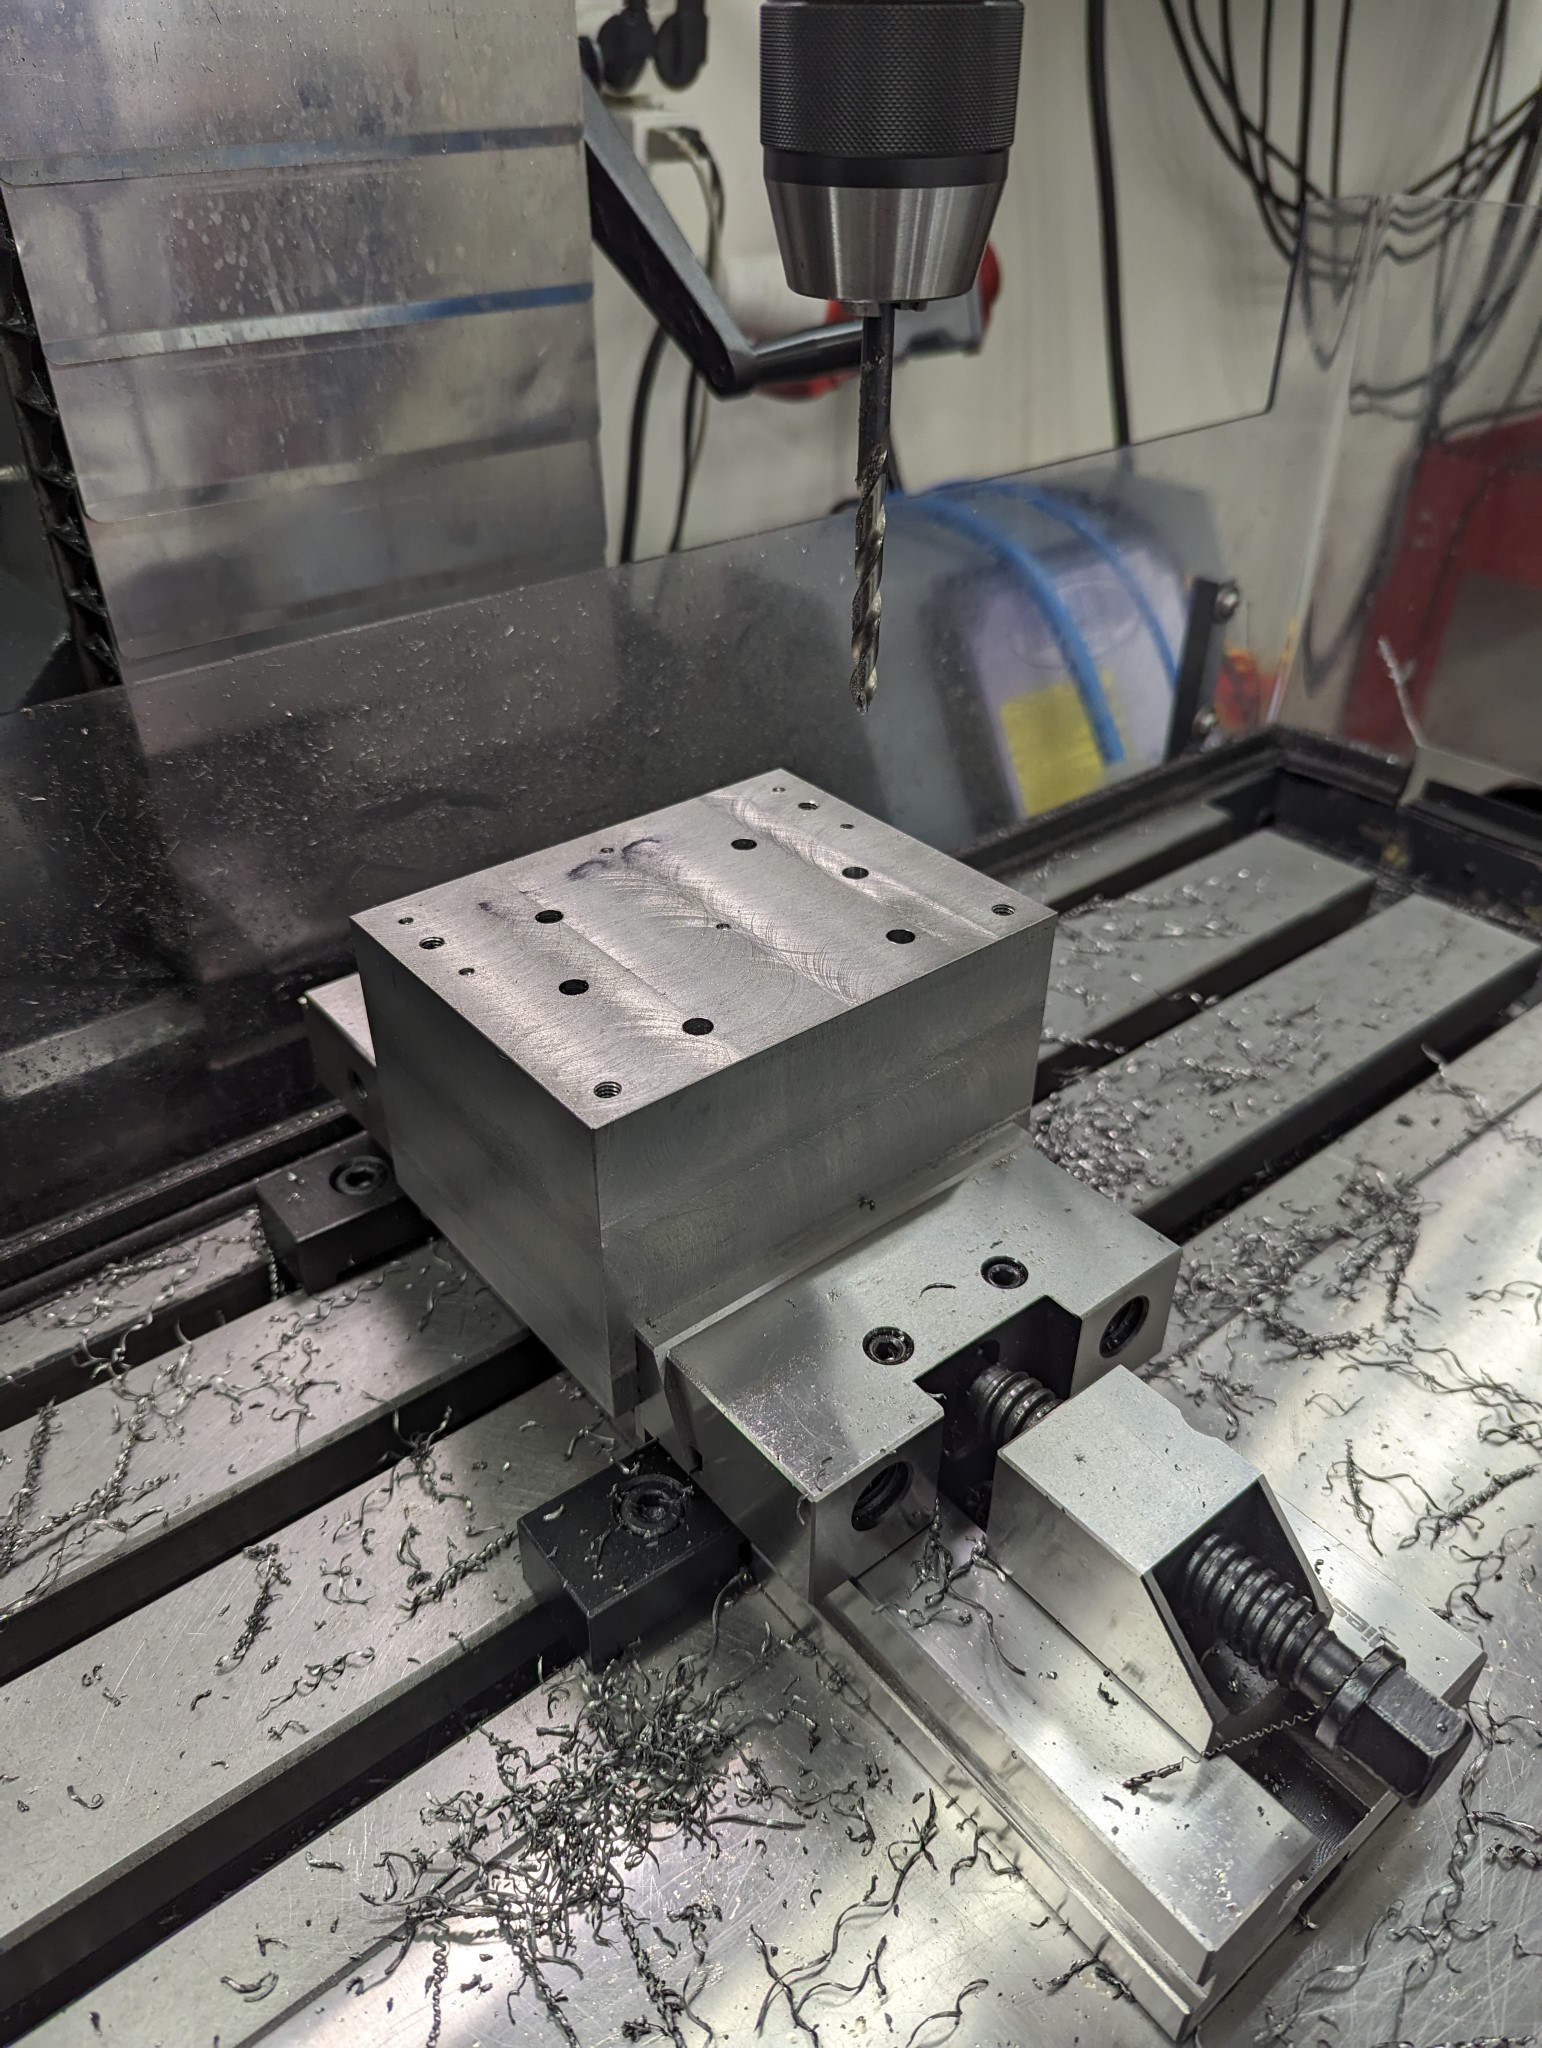
I used this very flimsy Chinese drill press to drill the new holes for the central lubrication oil fittings.


While I was at it I also drilled the holes for the bolts that will hold the mount for the Y axis ball screw nut.


I also removed a tiny bit of material from the saddle in order to extend the travel of the table a bit. The travel will actually be extended a few  centimeters because the new ball screw nut mount will sit closer to the column compared to the stock mount for the trapezoidal screw.


Please Log in or Create an account to join the conversation.

More
2 years 8 months ago #293701 by Unlogic
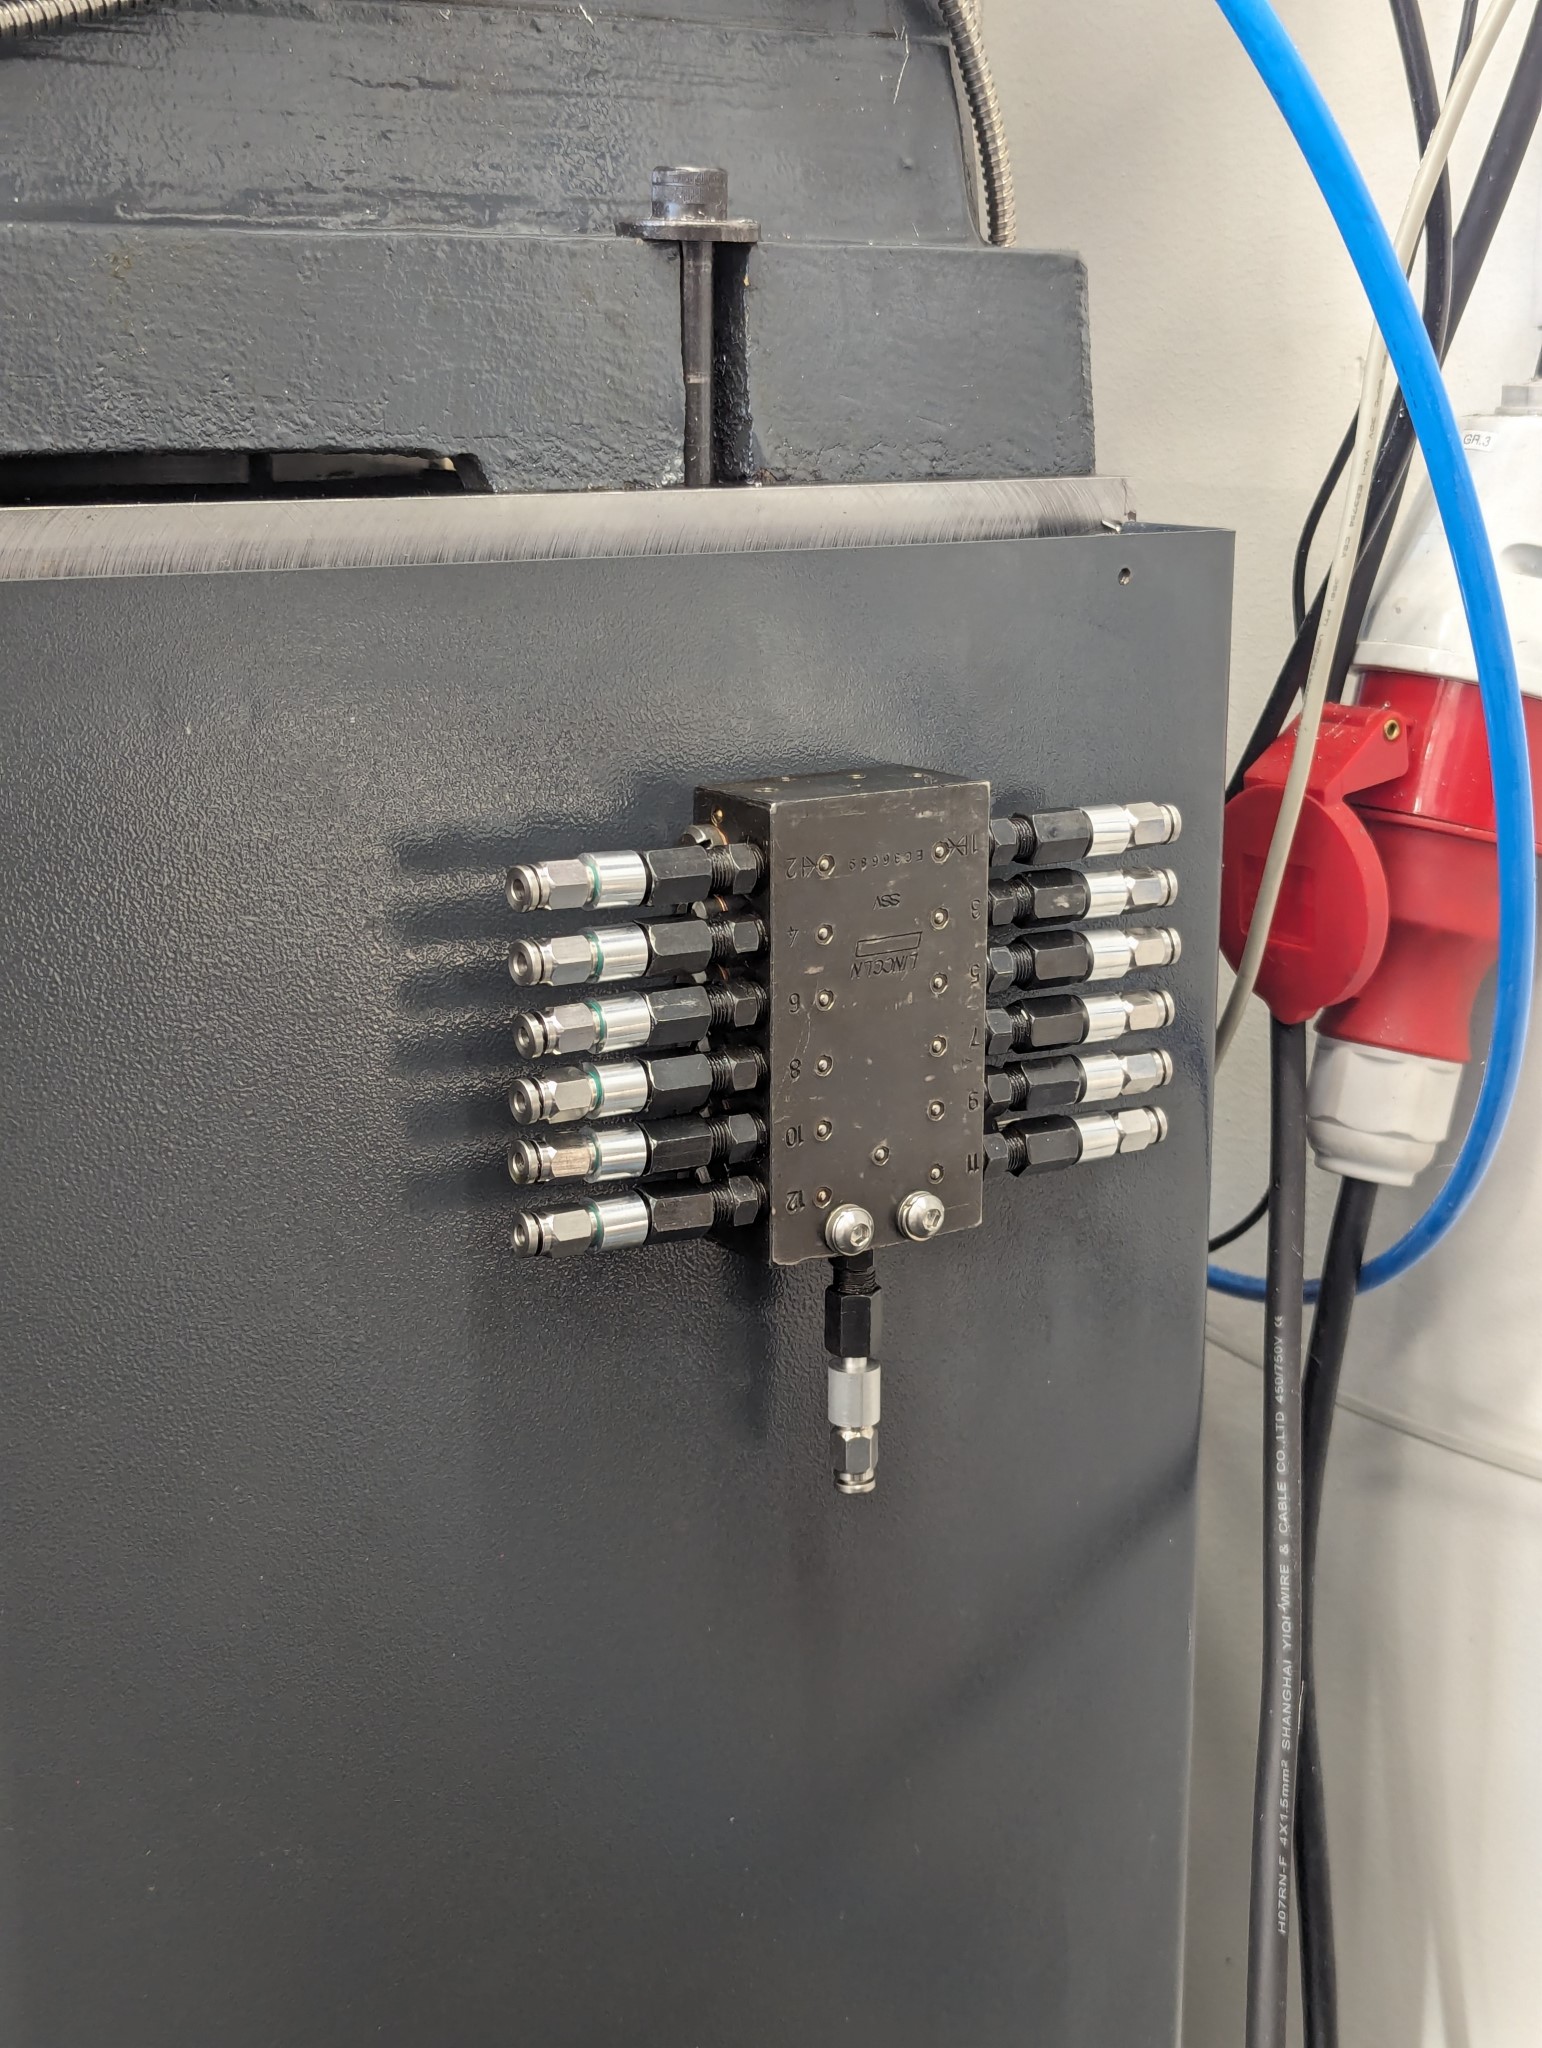
With that done I stoned the gibs a bit and then assembled everything along with the central lubrication system.


The central lubrication and the work on the gibs did wounder for how a smooth the machine travels. This machine really should have come with central lubrication from the factory.

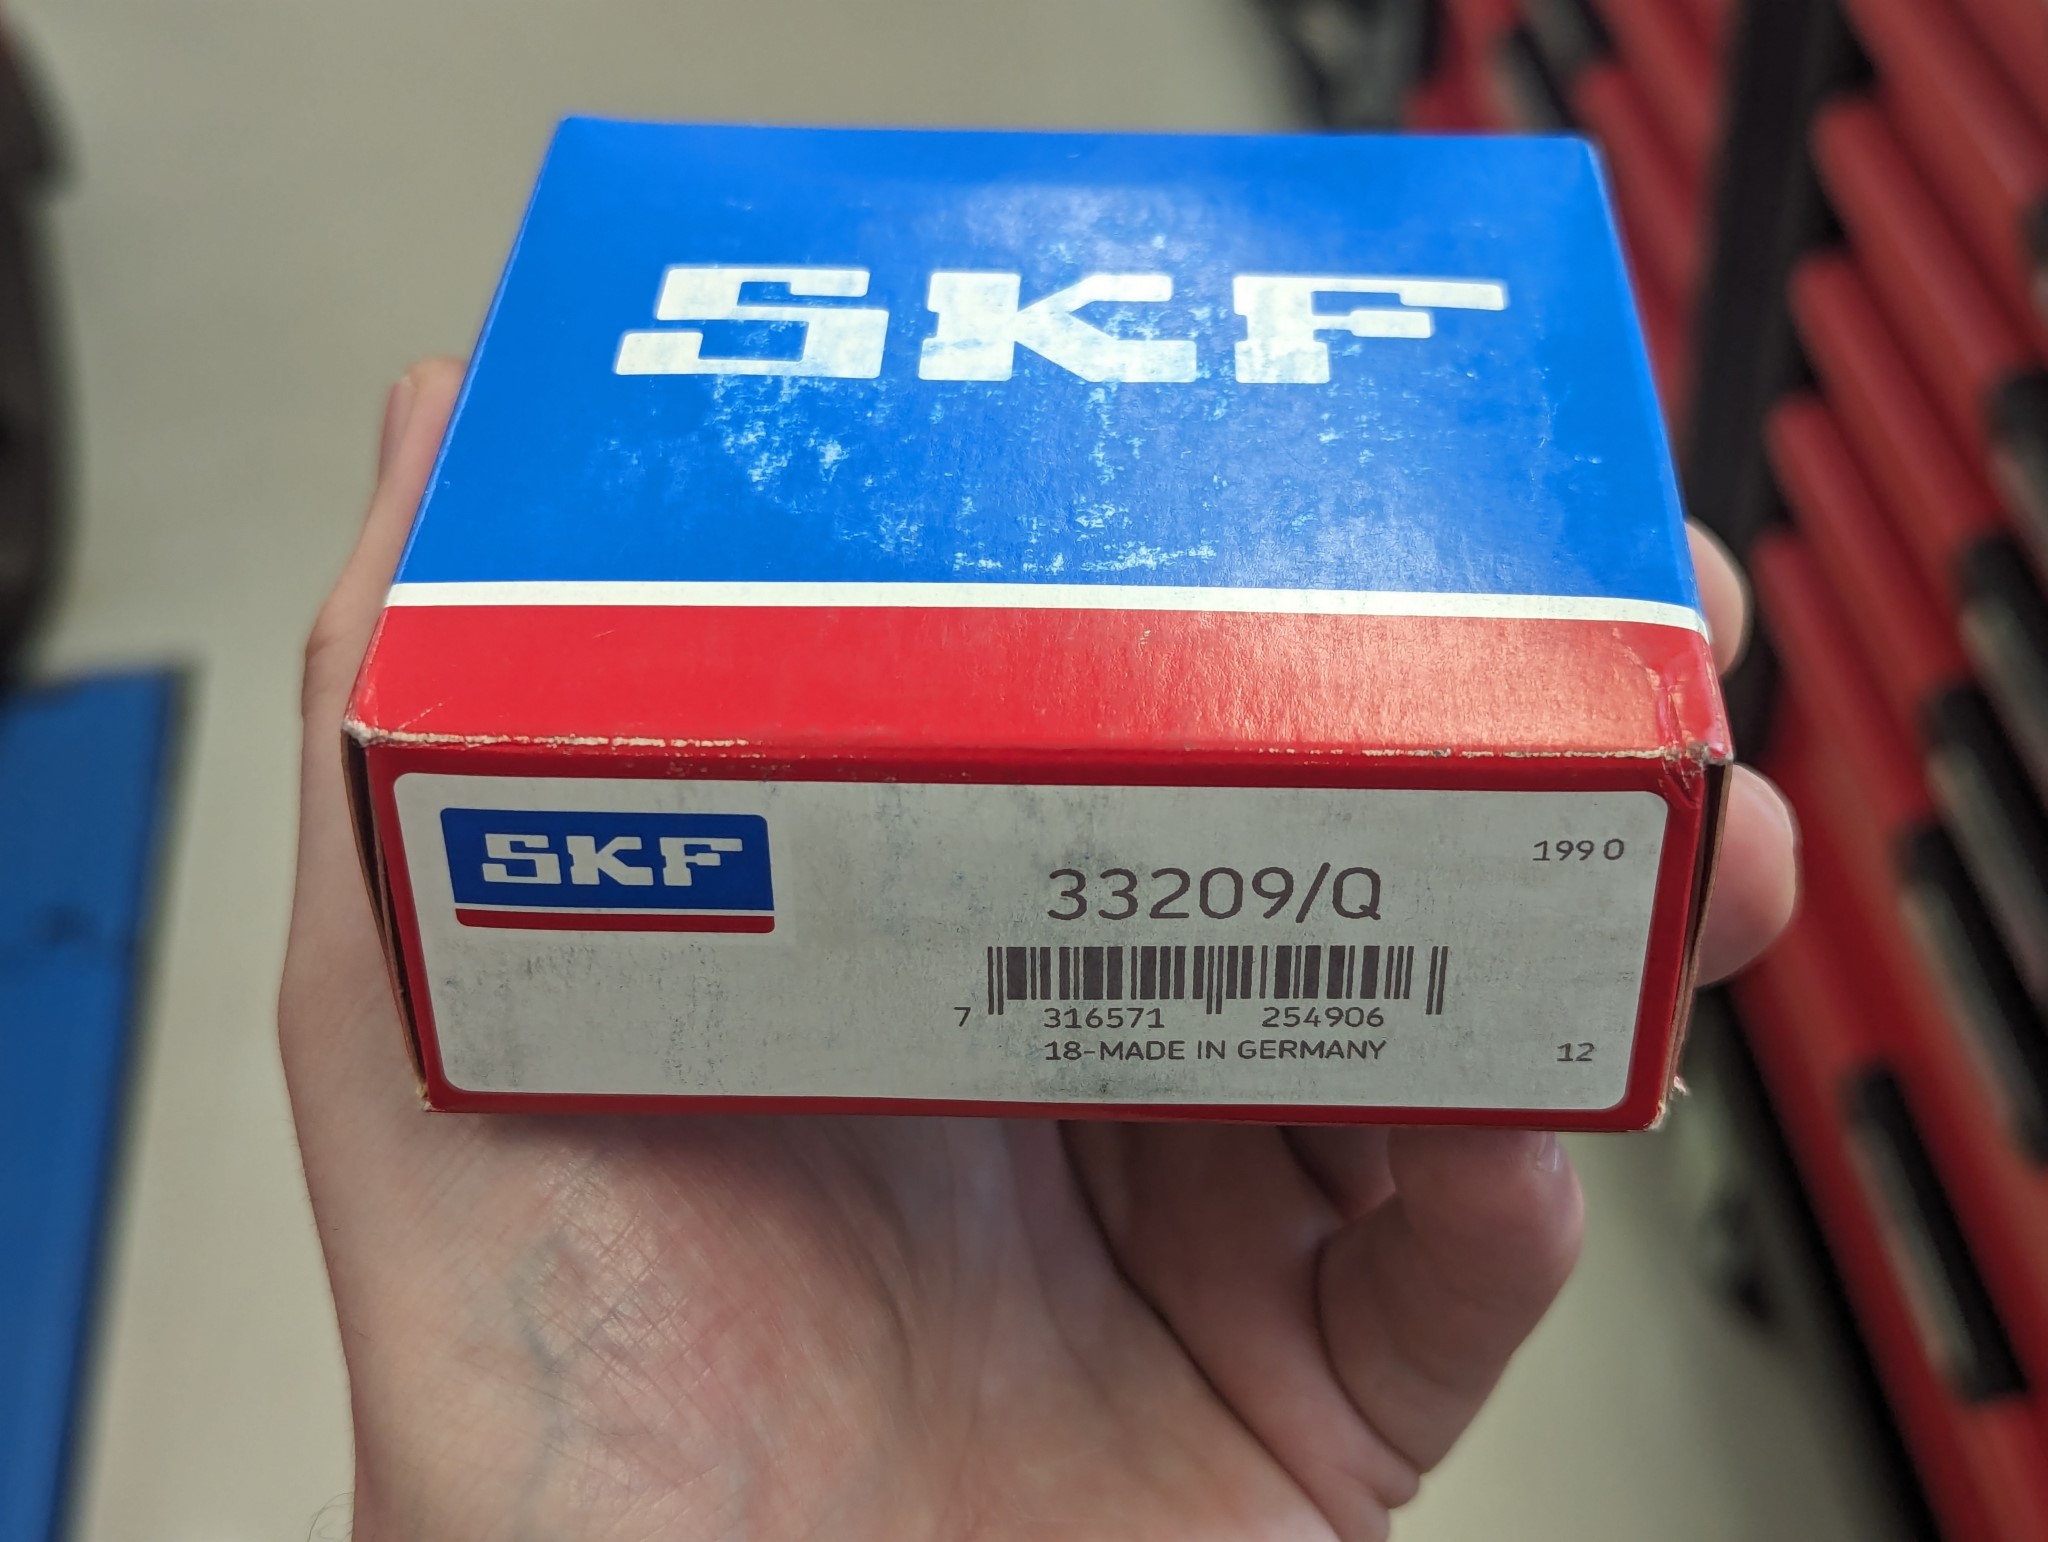
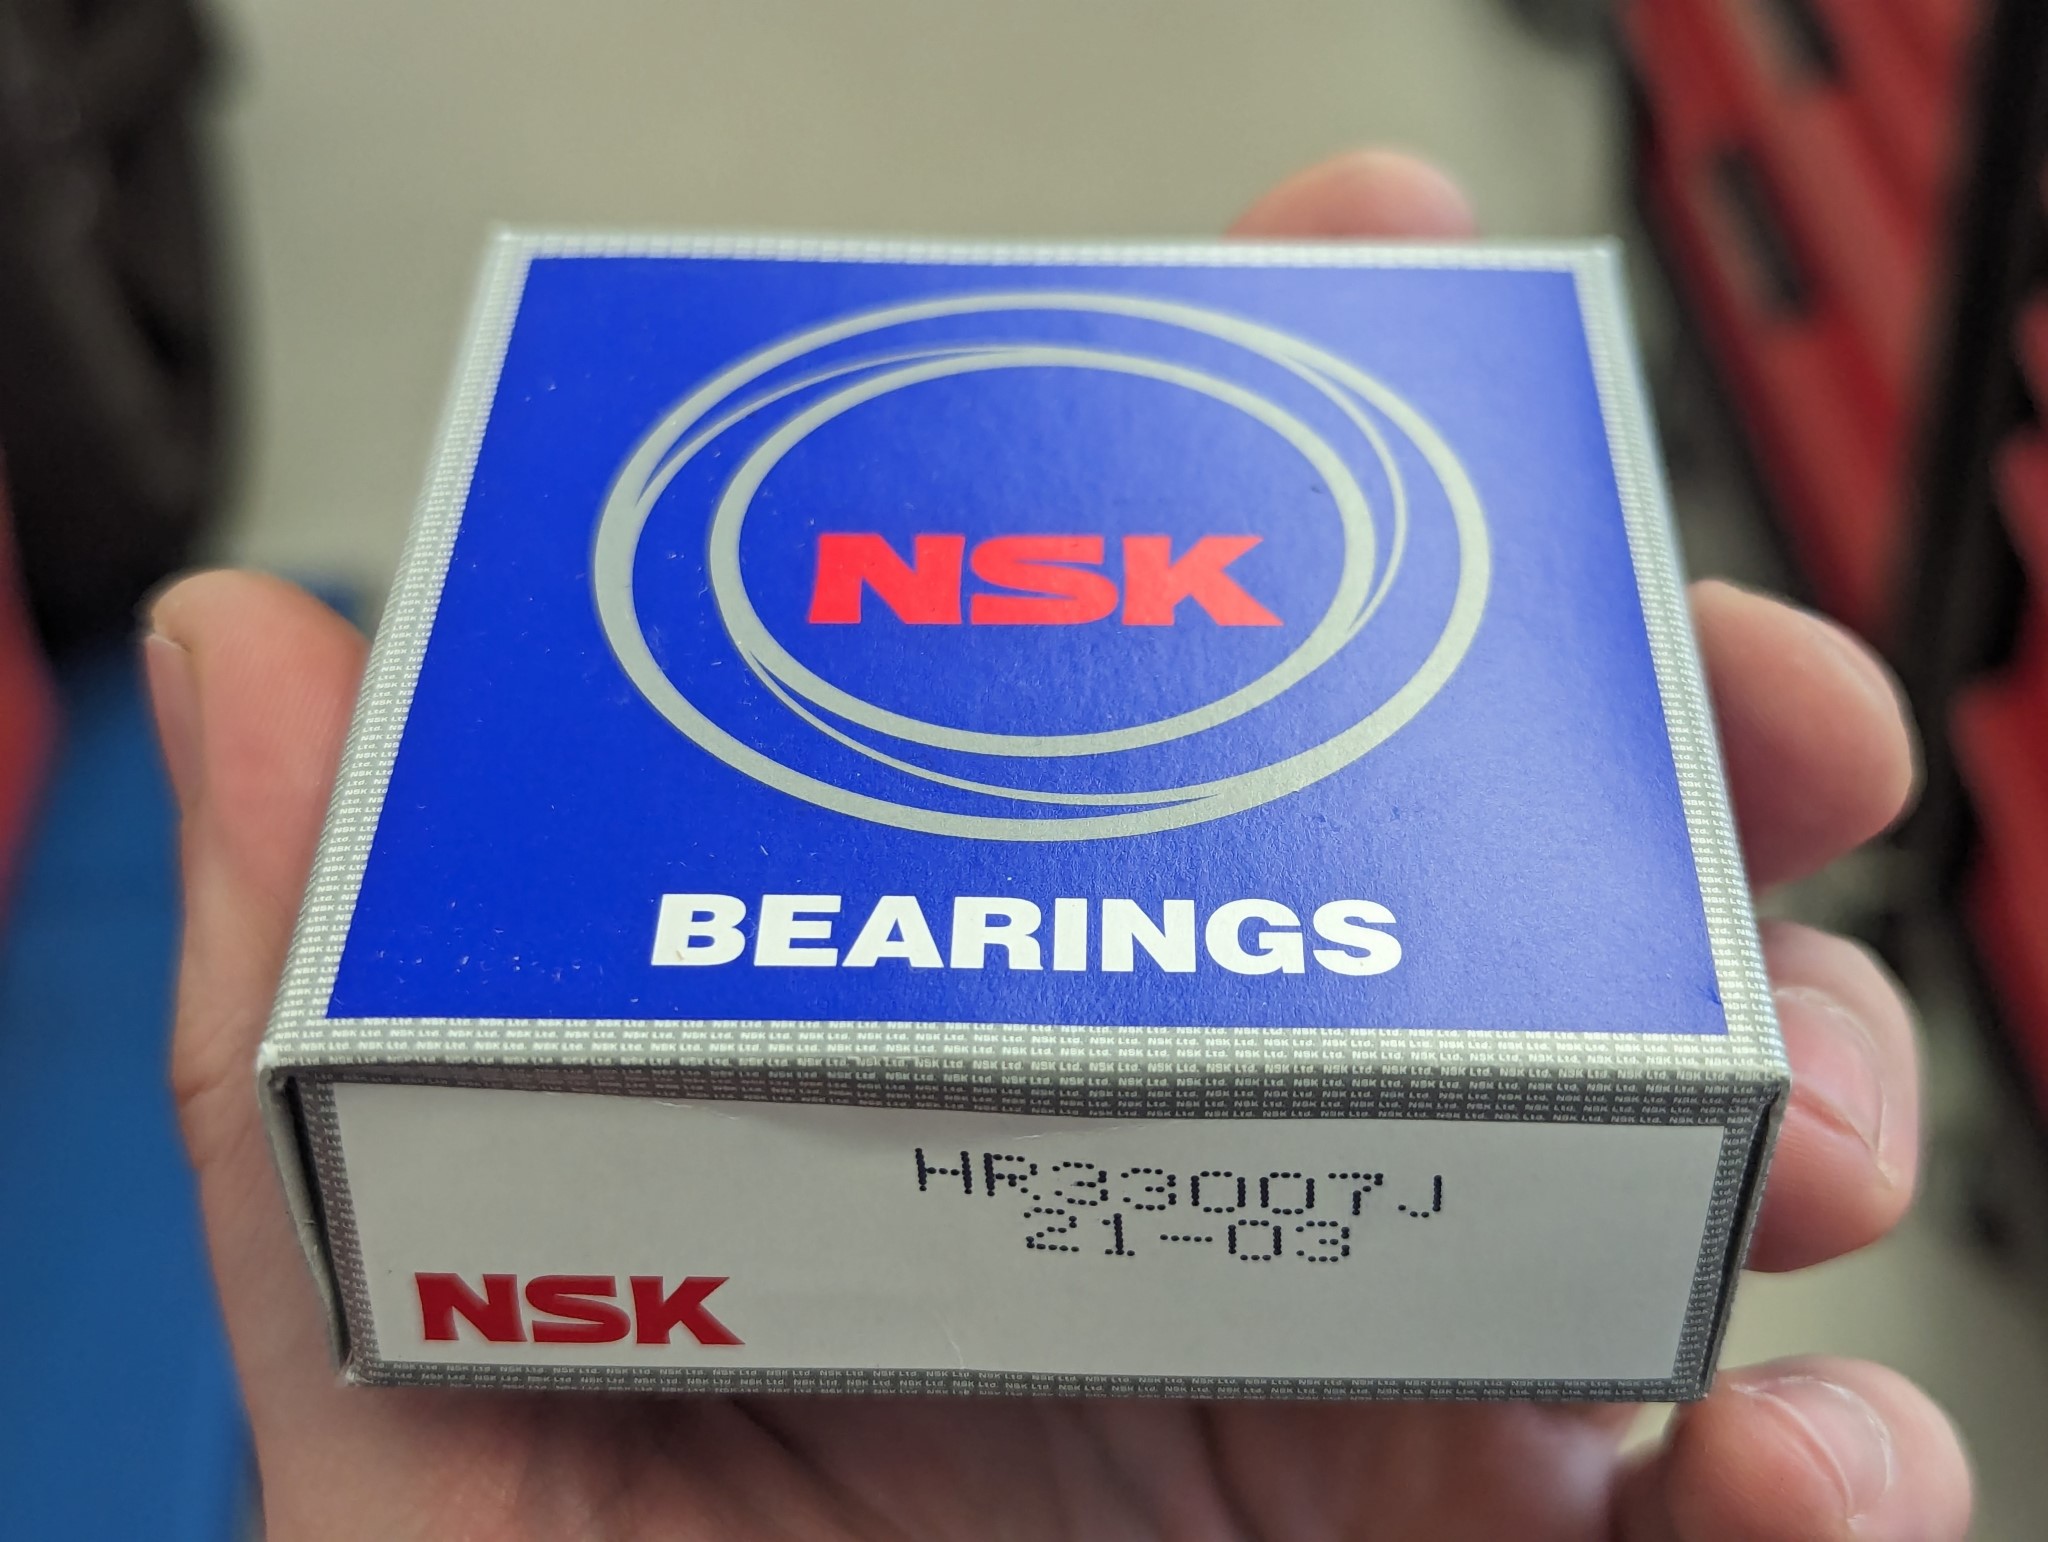
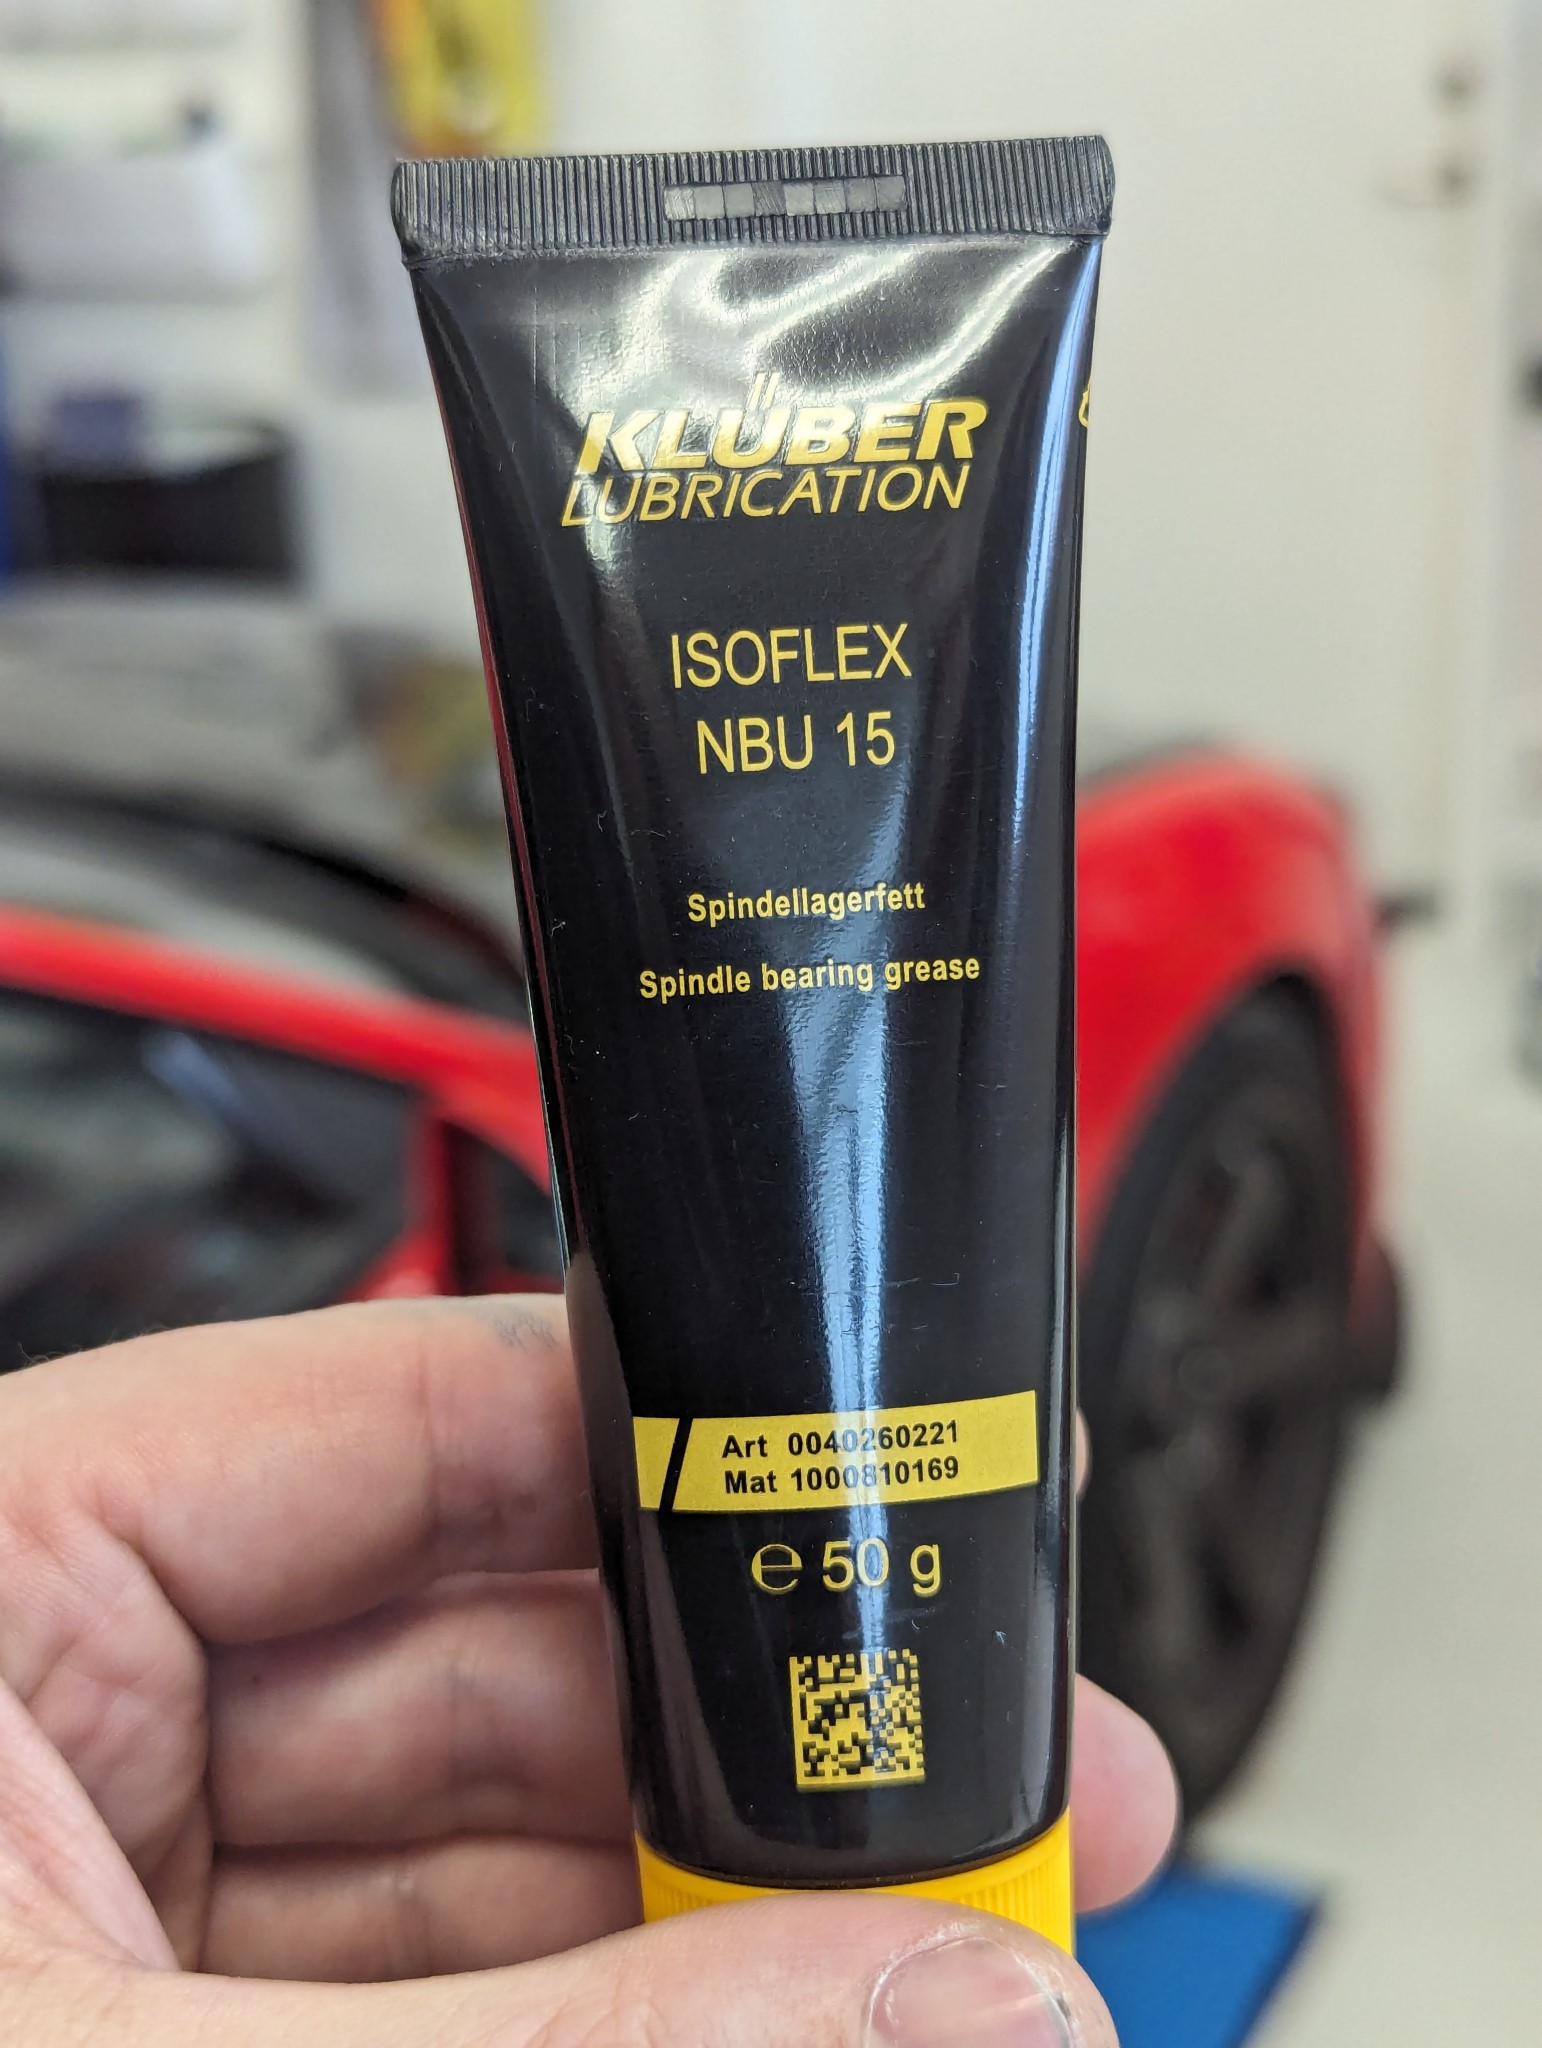
My spindle bearings have been making a slight noise for some time and all the milling in steel haven't exactly improved things. So when the CNC conversion is done and I've regained some bench space in the garage then my plan is the remove the spindle and replace the bearings.

SKF doesn't make the type of roller bearing used for the upper bearing in the spindle so I'm gonna use a mix of SKF and NSK bearings along with Klüber Isoflex NBU 15 grease.


The following user(s) said Thank You: tommylight, anders

Please Log in or Create an account to join the conversation.

More
2 years 7 months ago #296946 by Unlogic
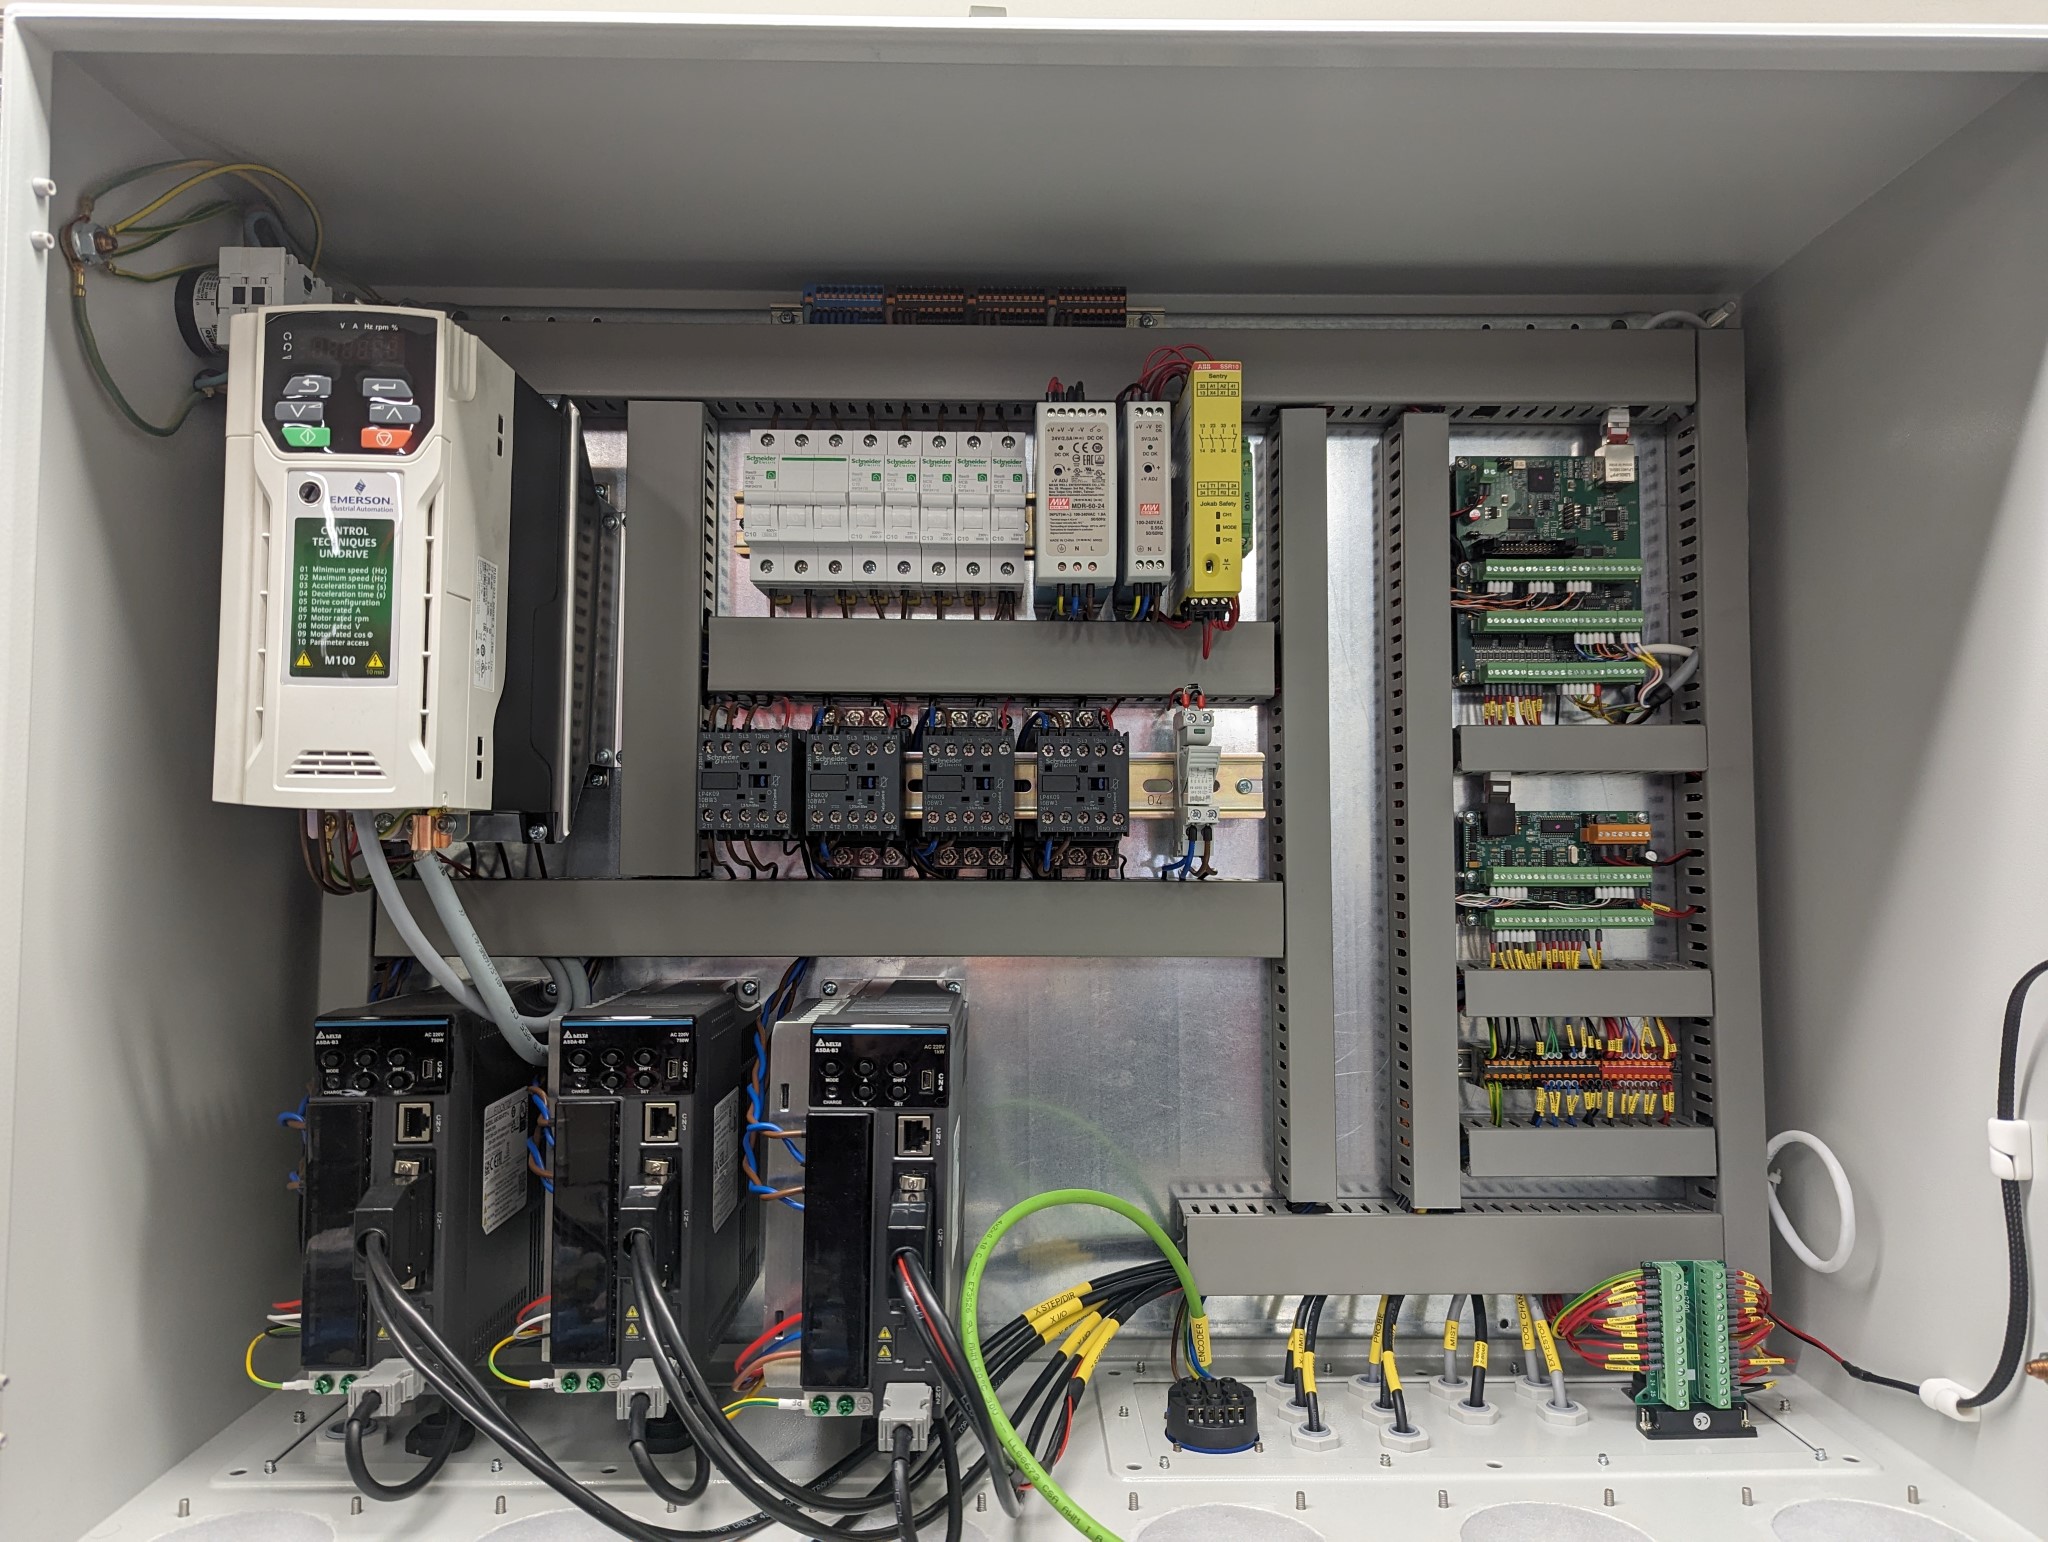
I've finished all the mechanical parts of this conversion now and the electrical cabinet that came with the machine has been removed along with all the stock electronics.

Here is how the control cabinet ended up looking on the inside with everything installed.


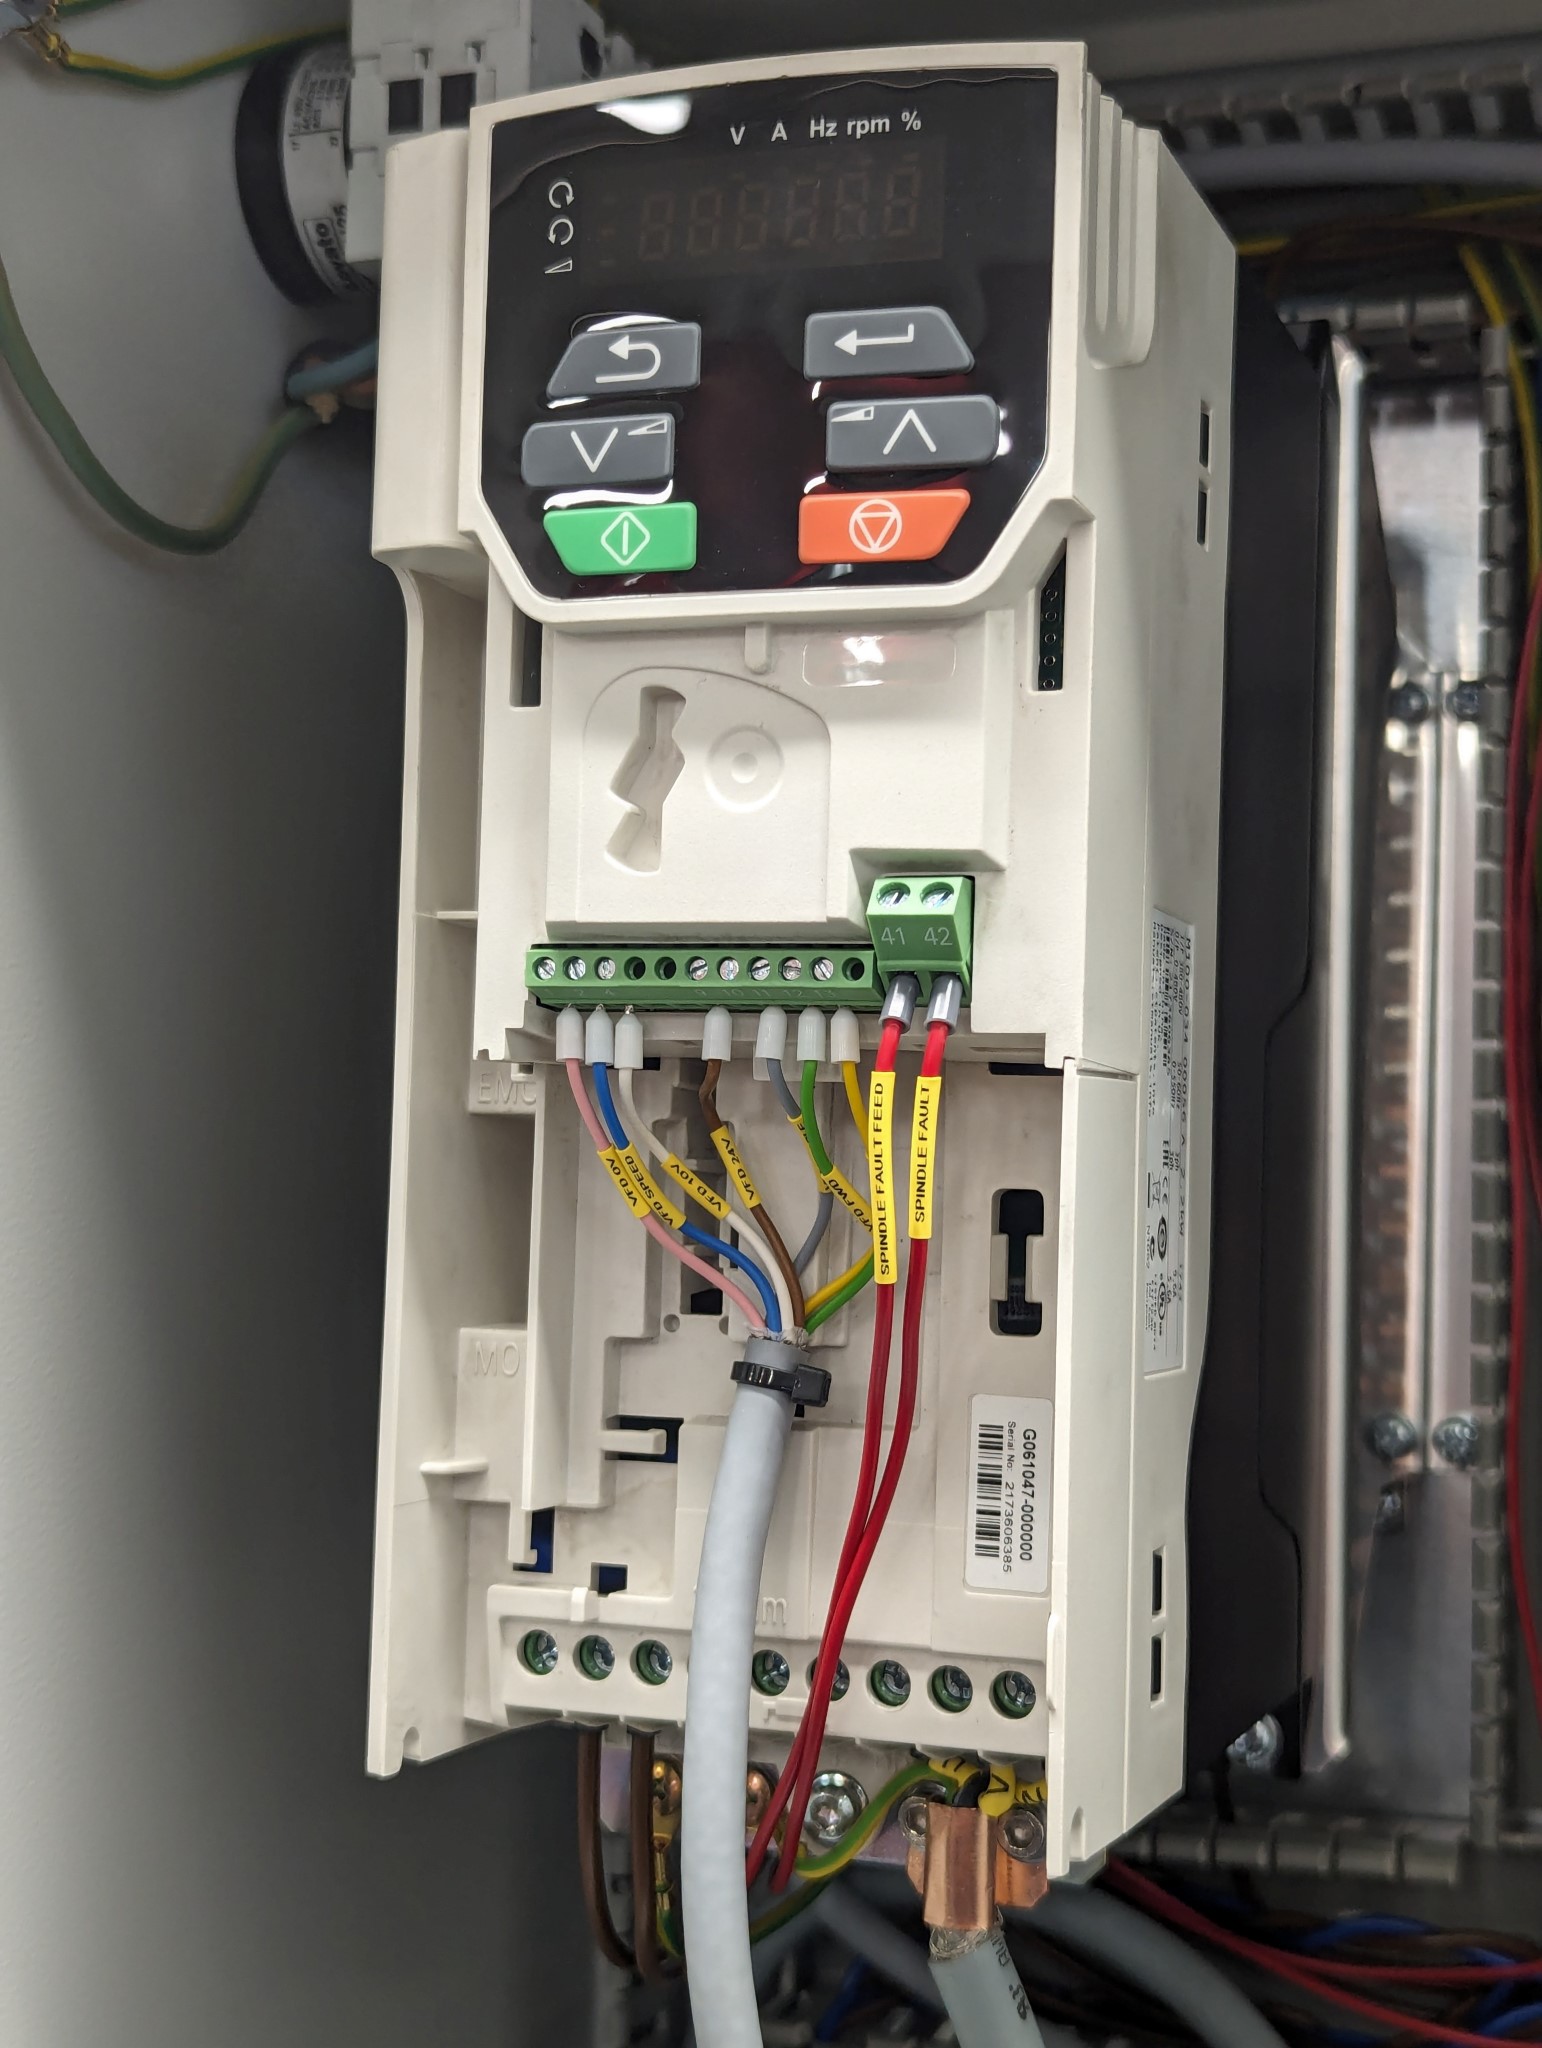
The only thing I reused from the electronics that came with the machine was the VFD and the estop button.

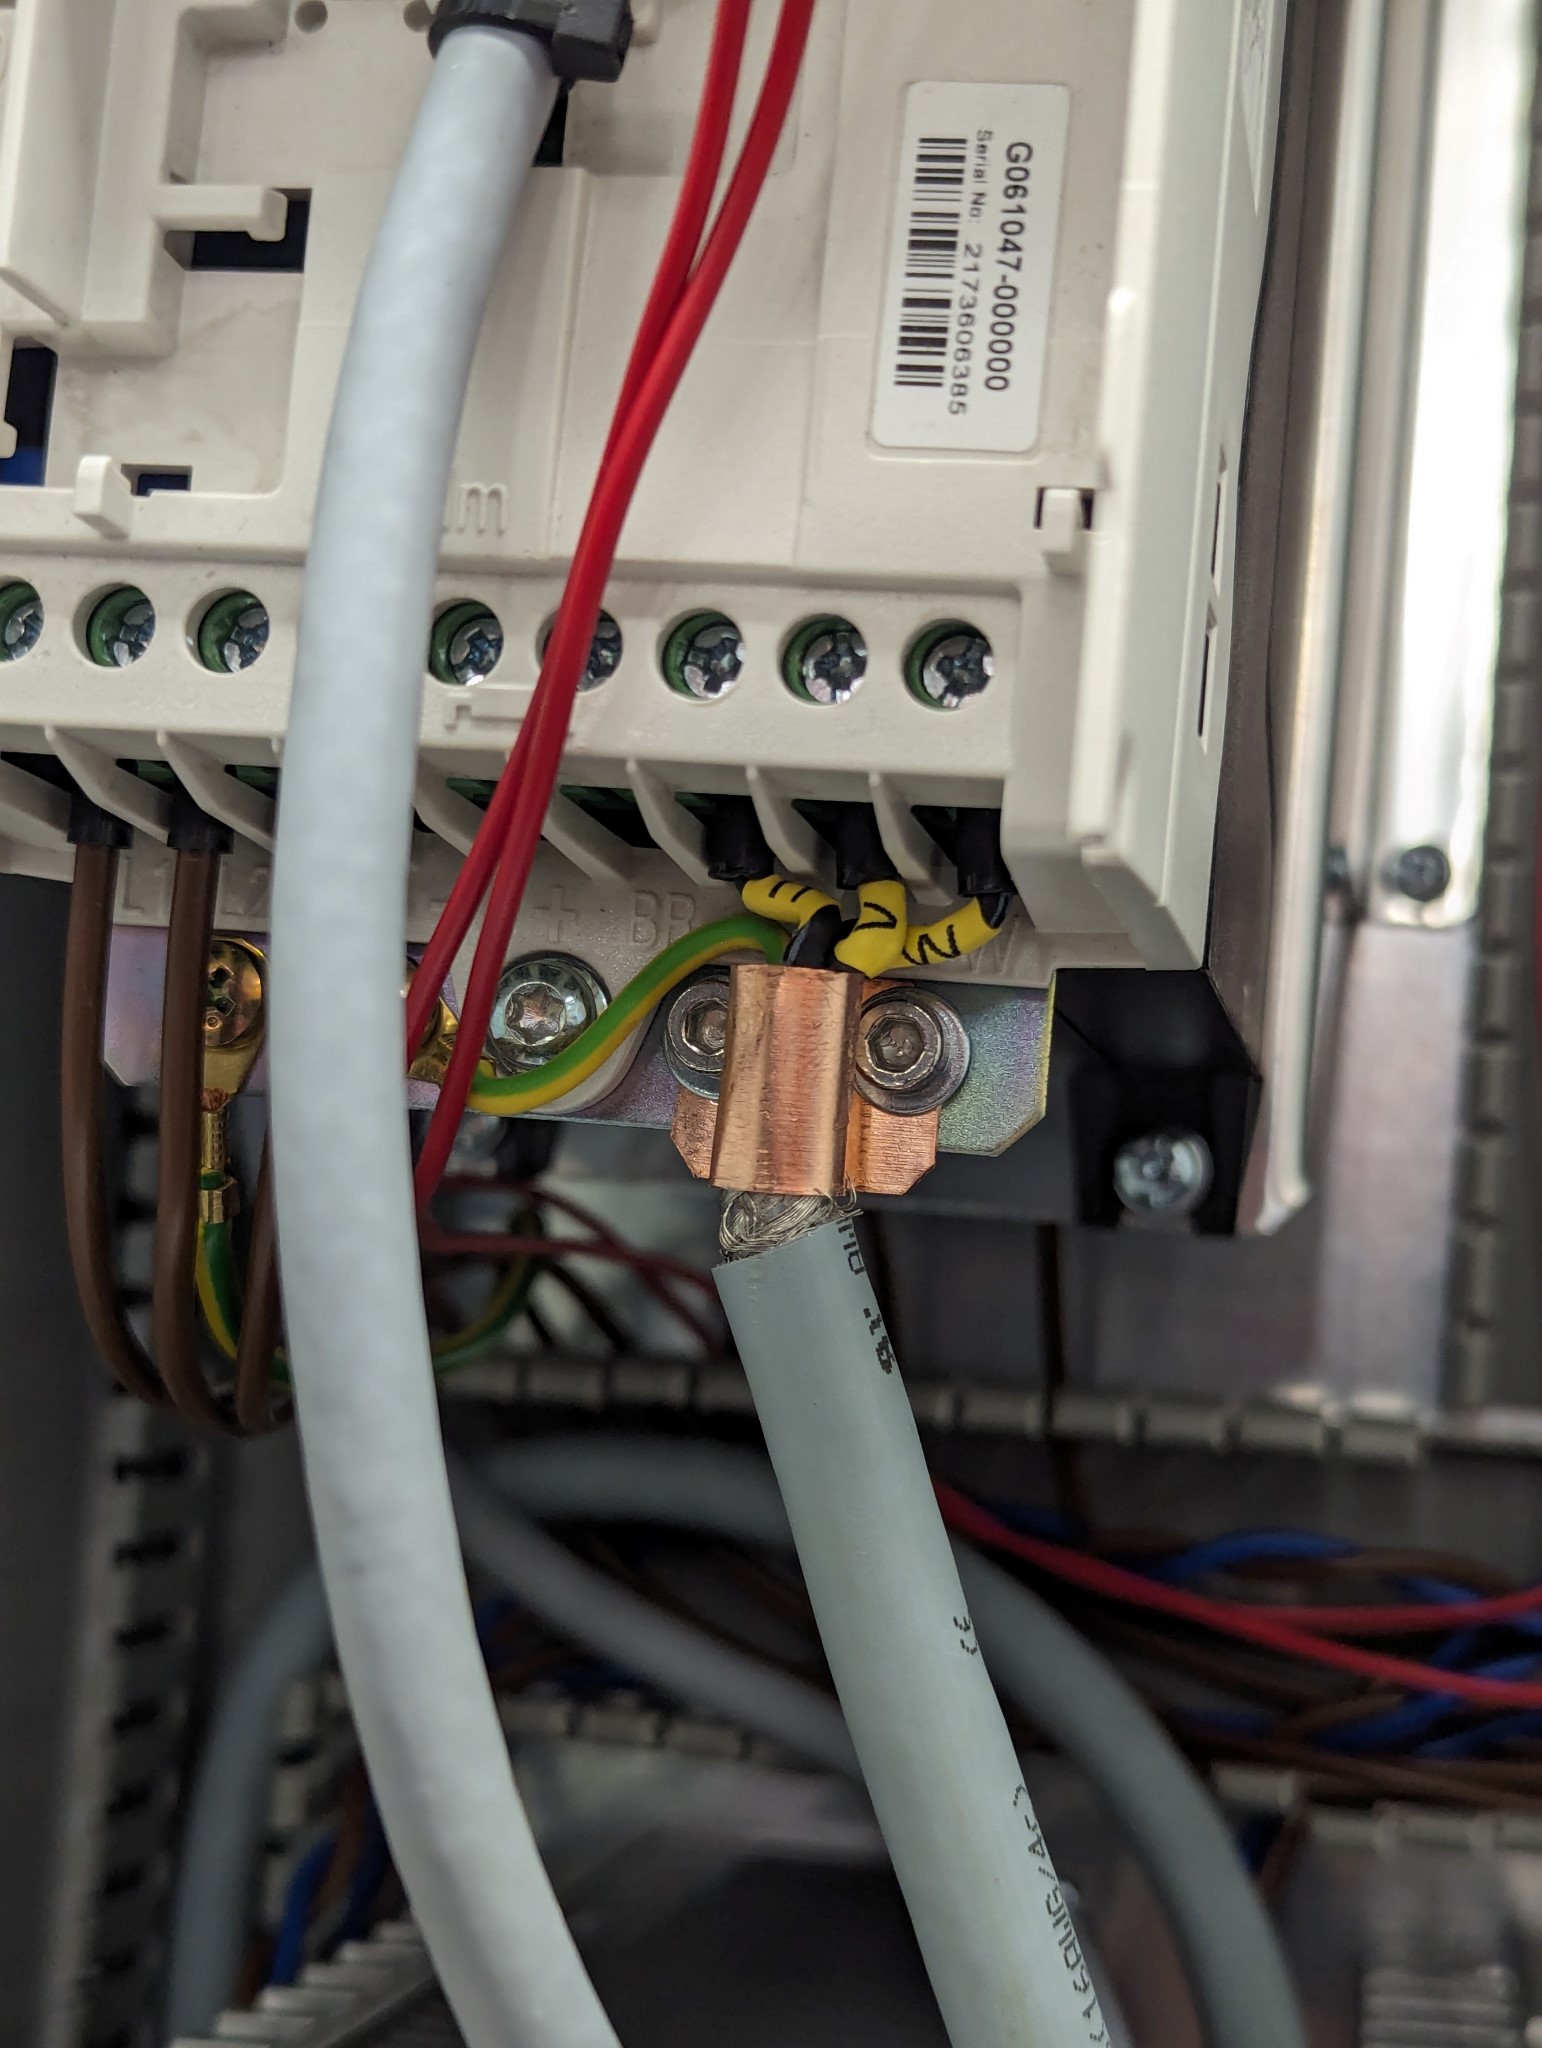
As I know VFD's can generate quite a bit of electrical noise I took no chances and terminated the shielded spindle motor cable right at the VFD using a copper bracket that contacts the shield around the whole circumference of the cable.


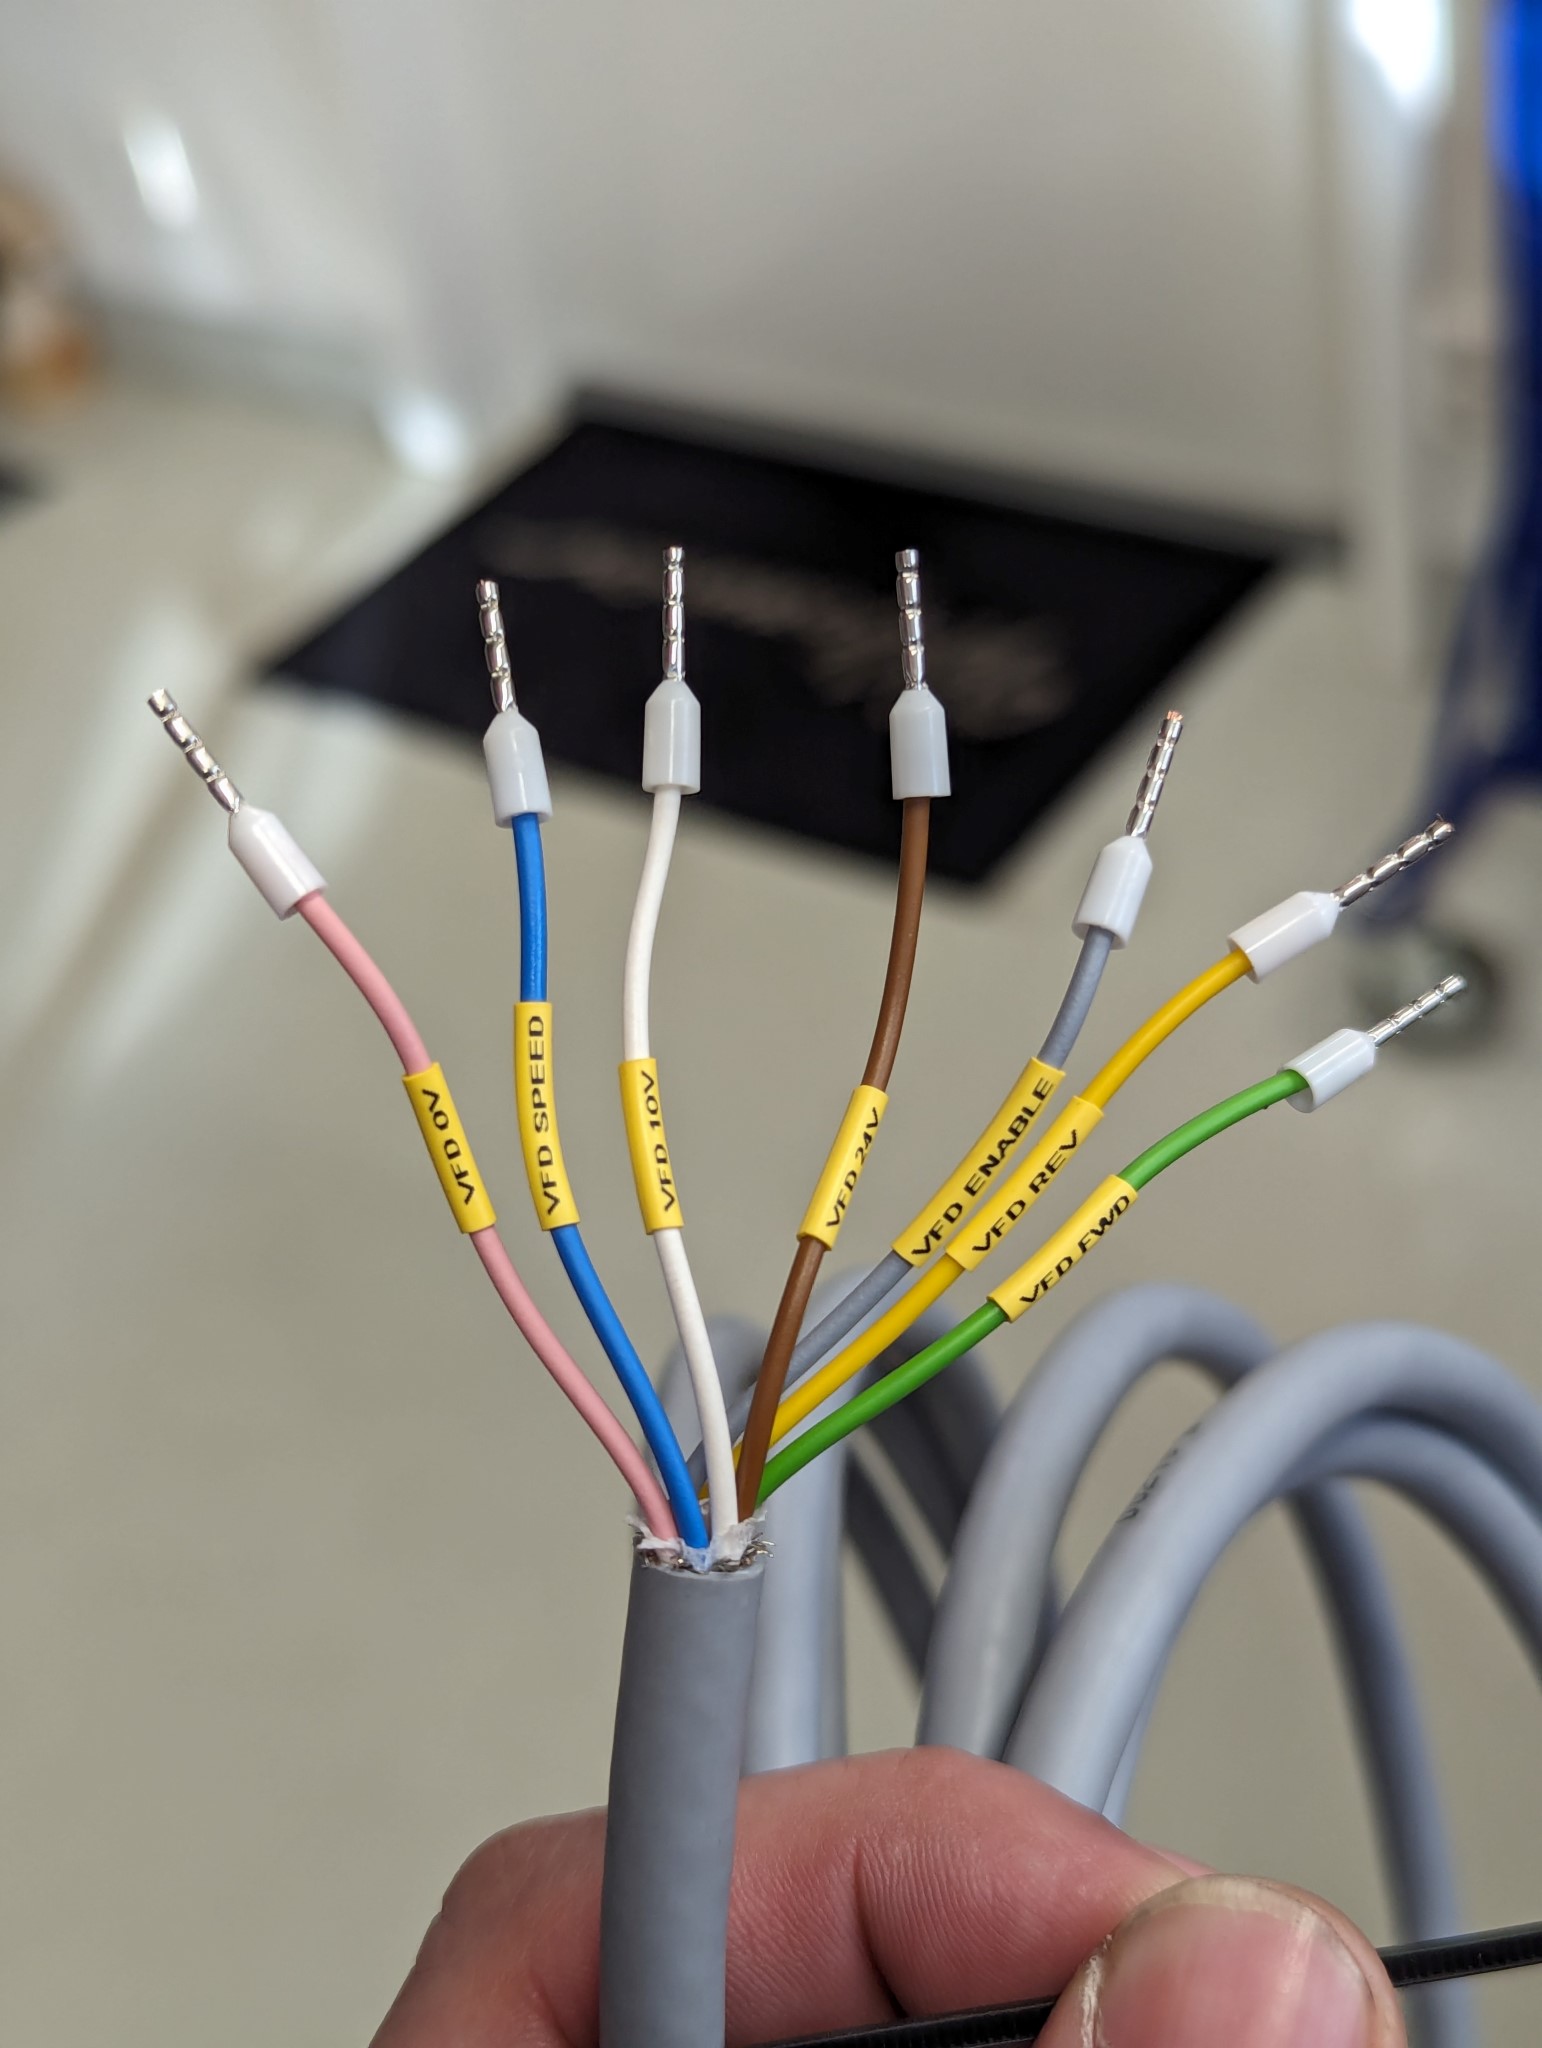
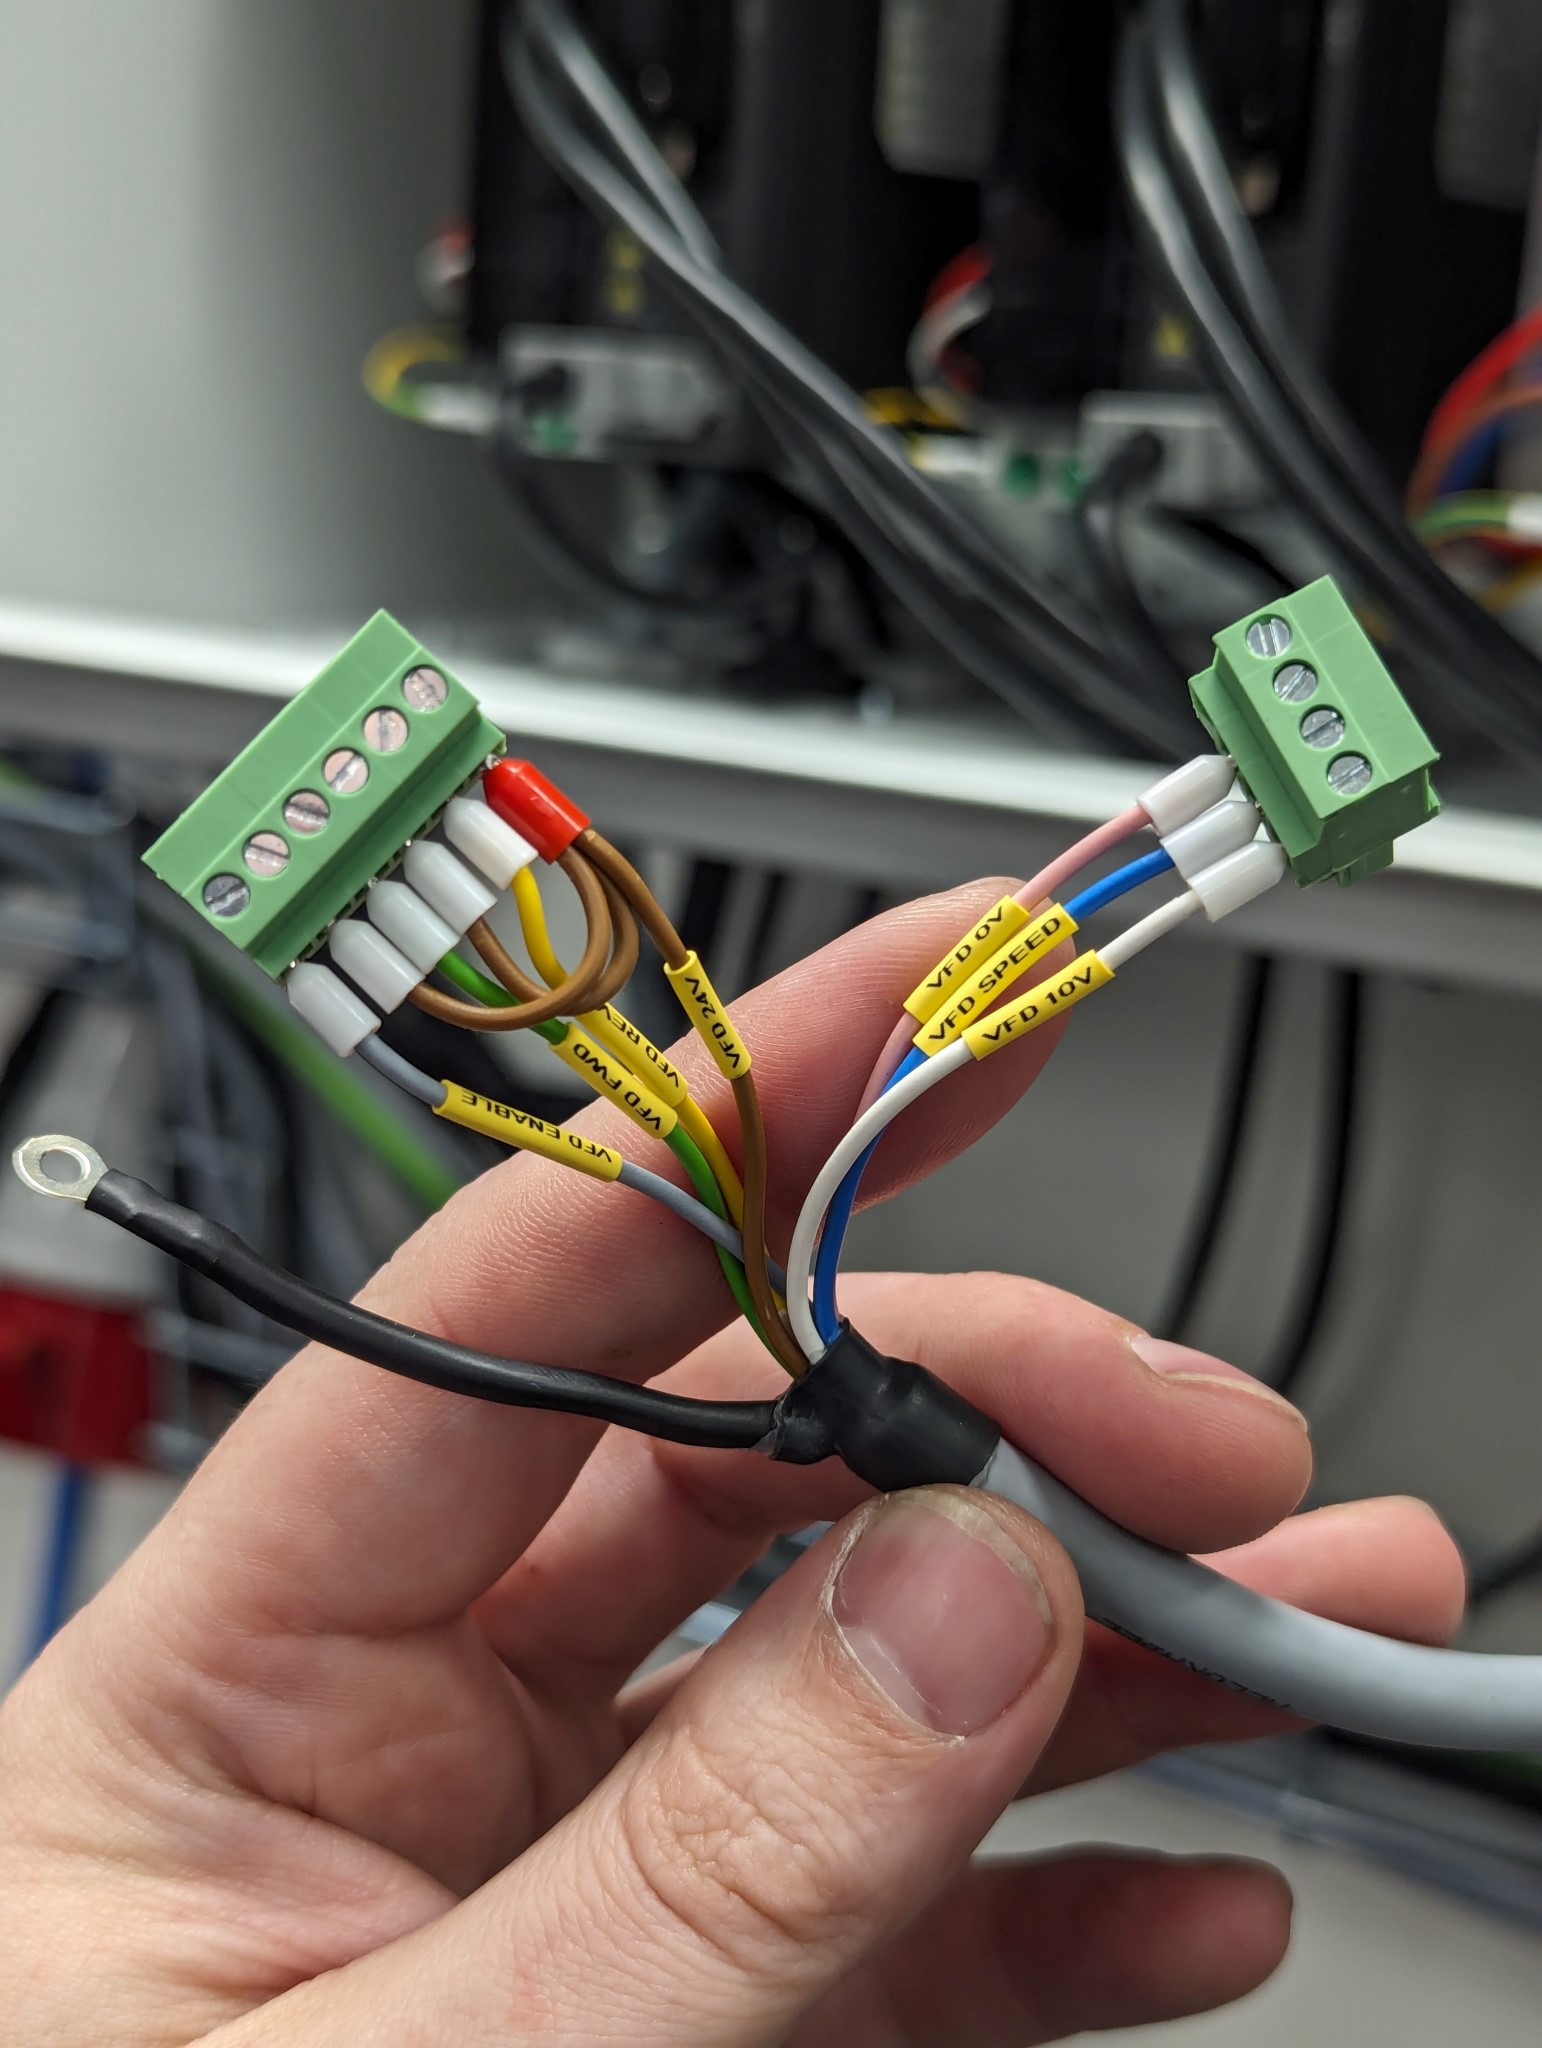
I also used a shielded cable for the control cable that goes from the VFD to the Mesa 7i96S board. I wasn't as picky with the termination of the shield here however and used a pigtail. Hopefully this work fine anyway.


I didn't have any shielded two-wire cable so for the fault signal from the VFD I used unshielded cables but these will be replaced shortly. I did this as an interim solution because I wanted to be absolutely sure that the motion stops if there is any fault with the spindle motor.


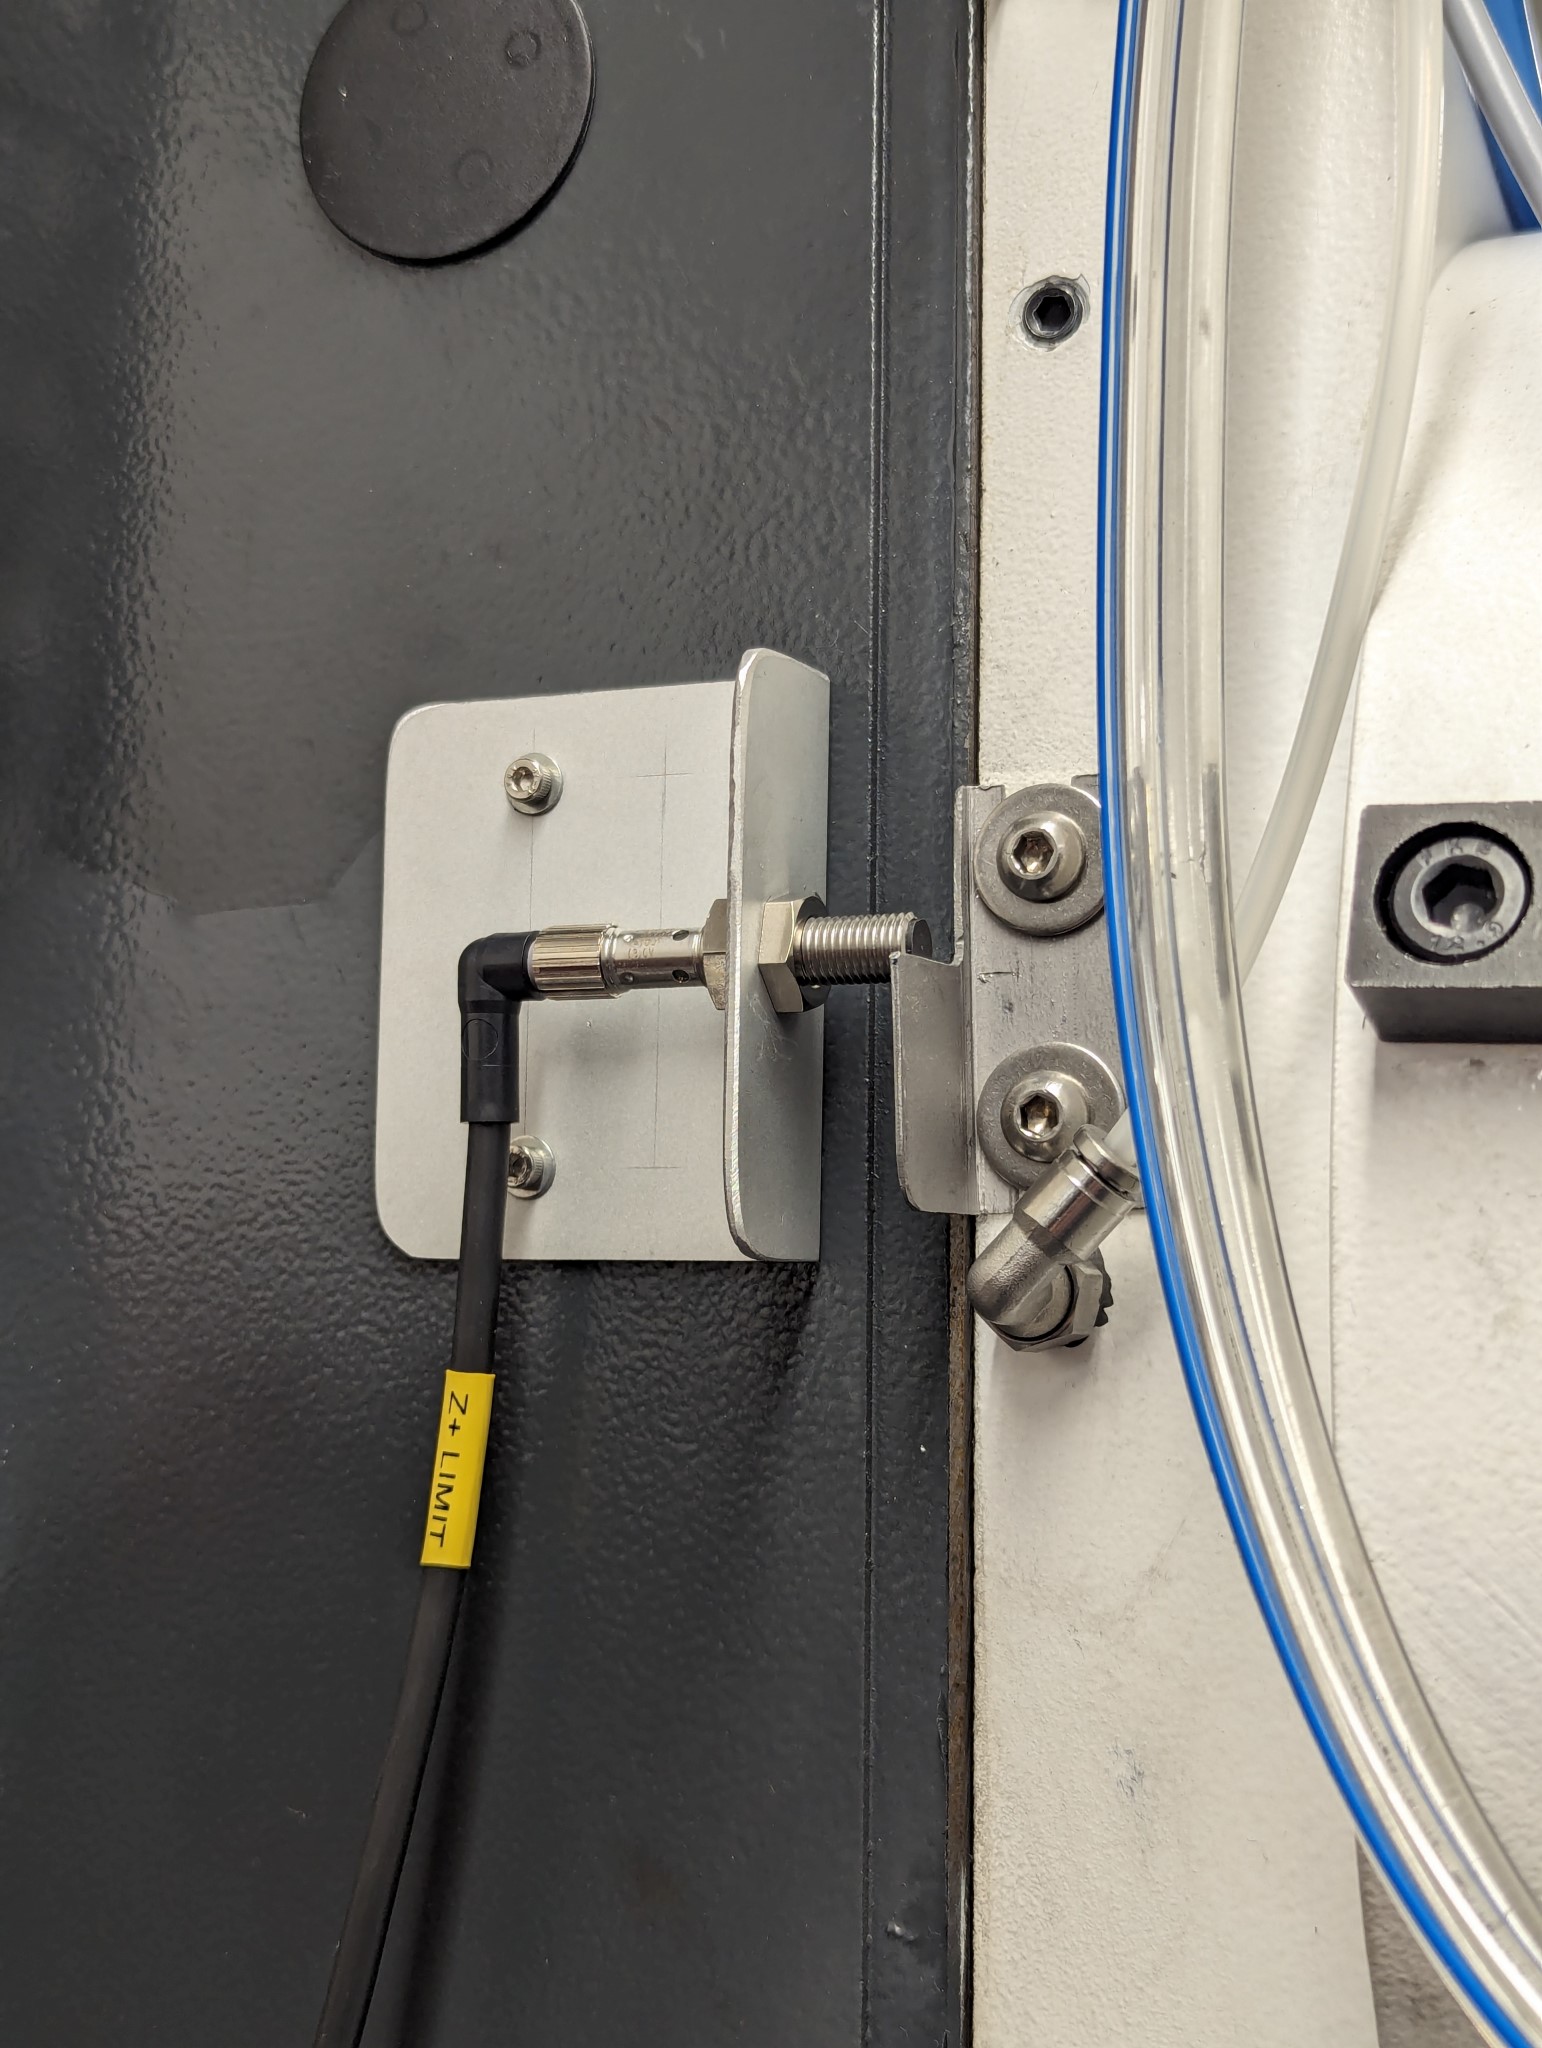
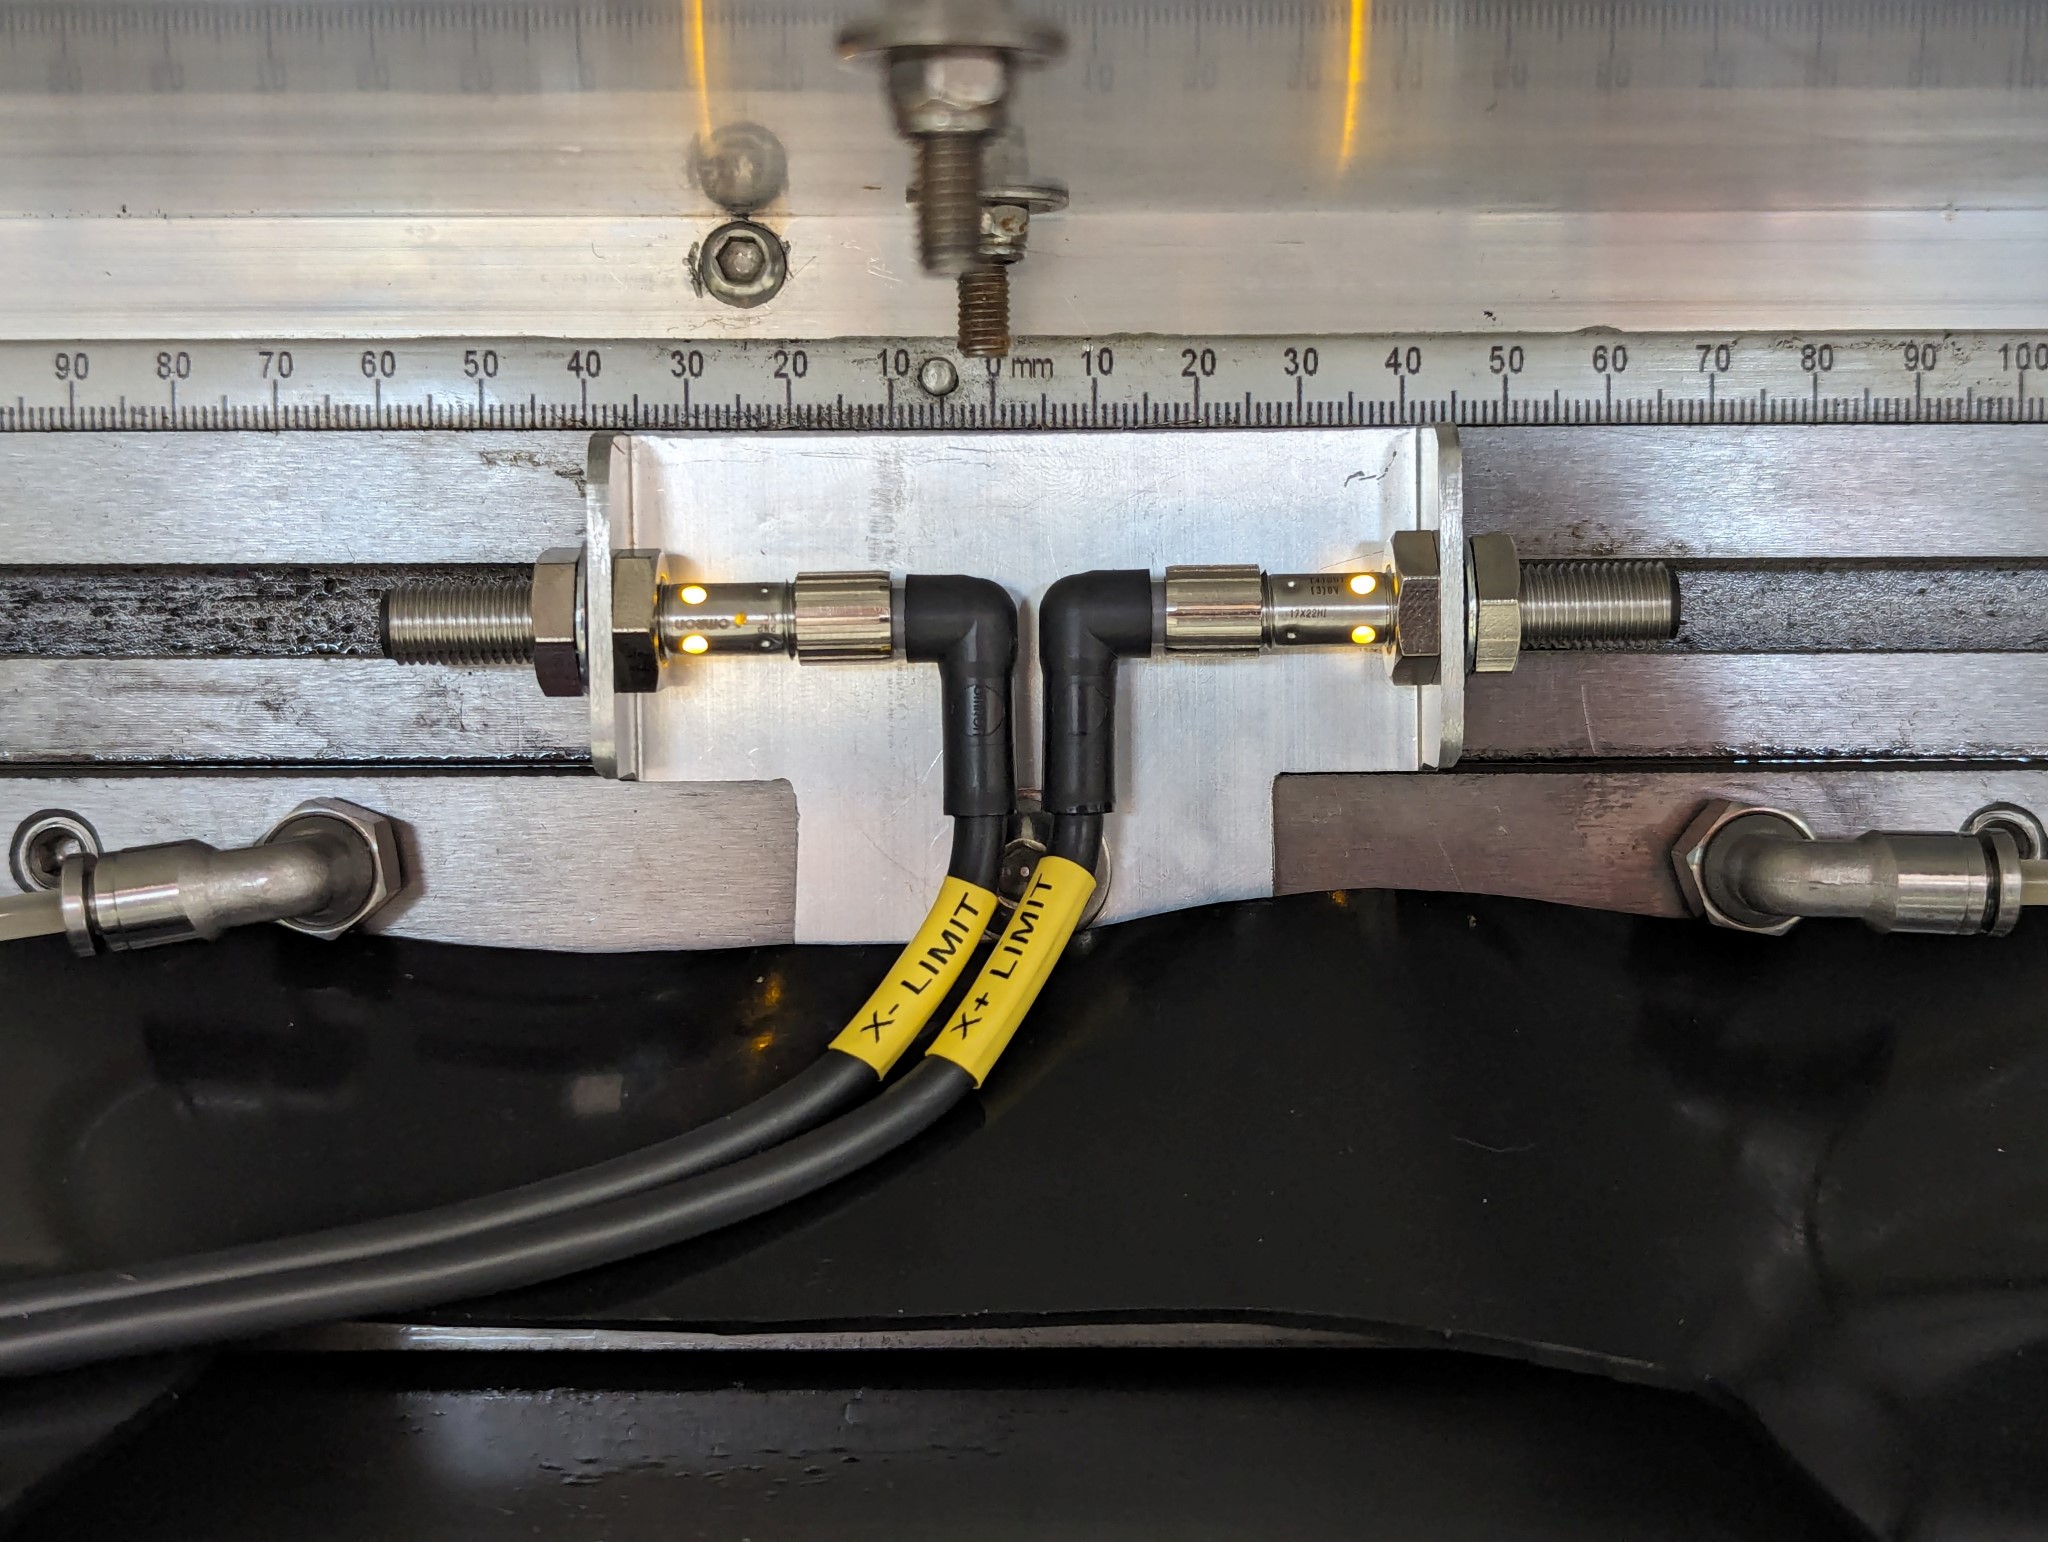
For limit switches I used inductive Omron E2BS08KS02MCB2 sensors. I have one sensor at the end of the travel of each axis apart from the z-axis which only has a sensor at the top.


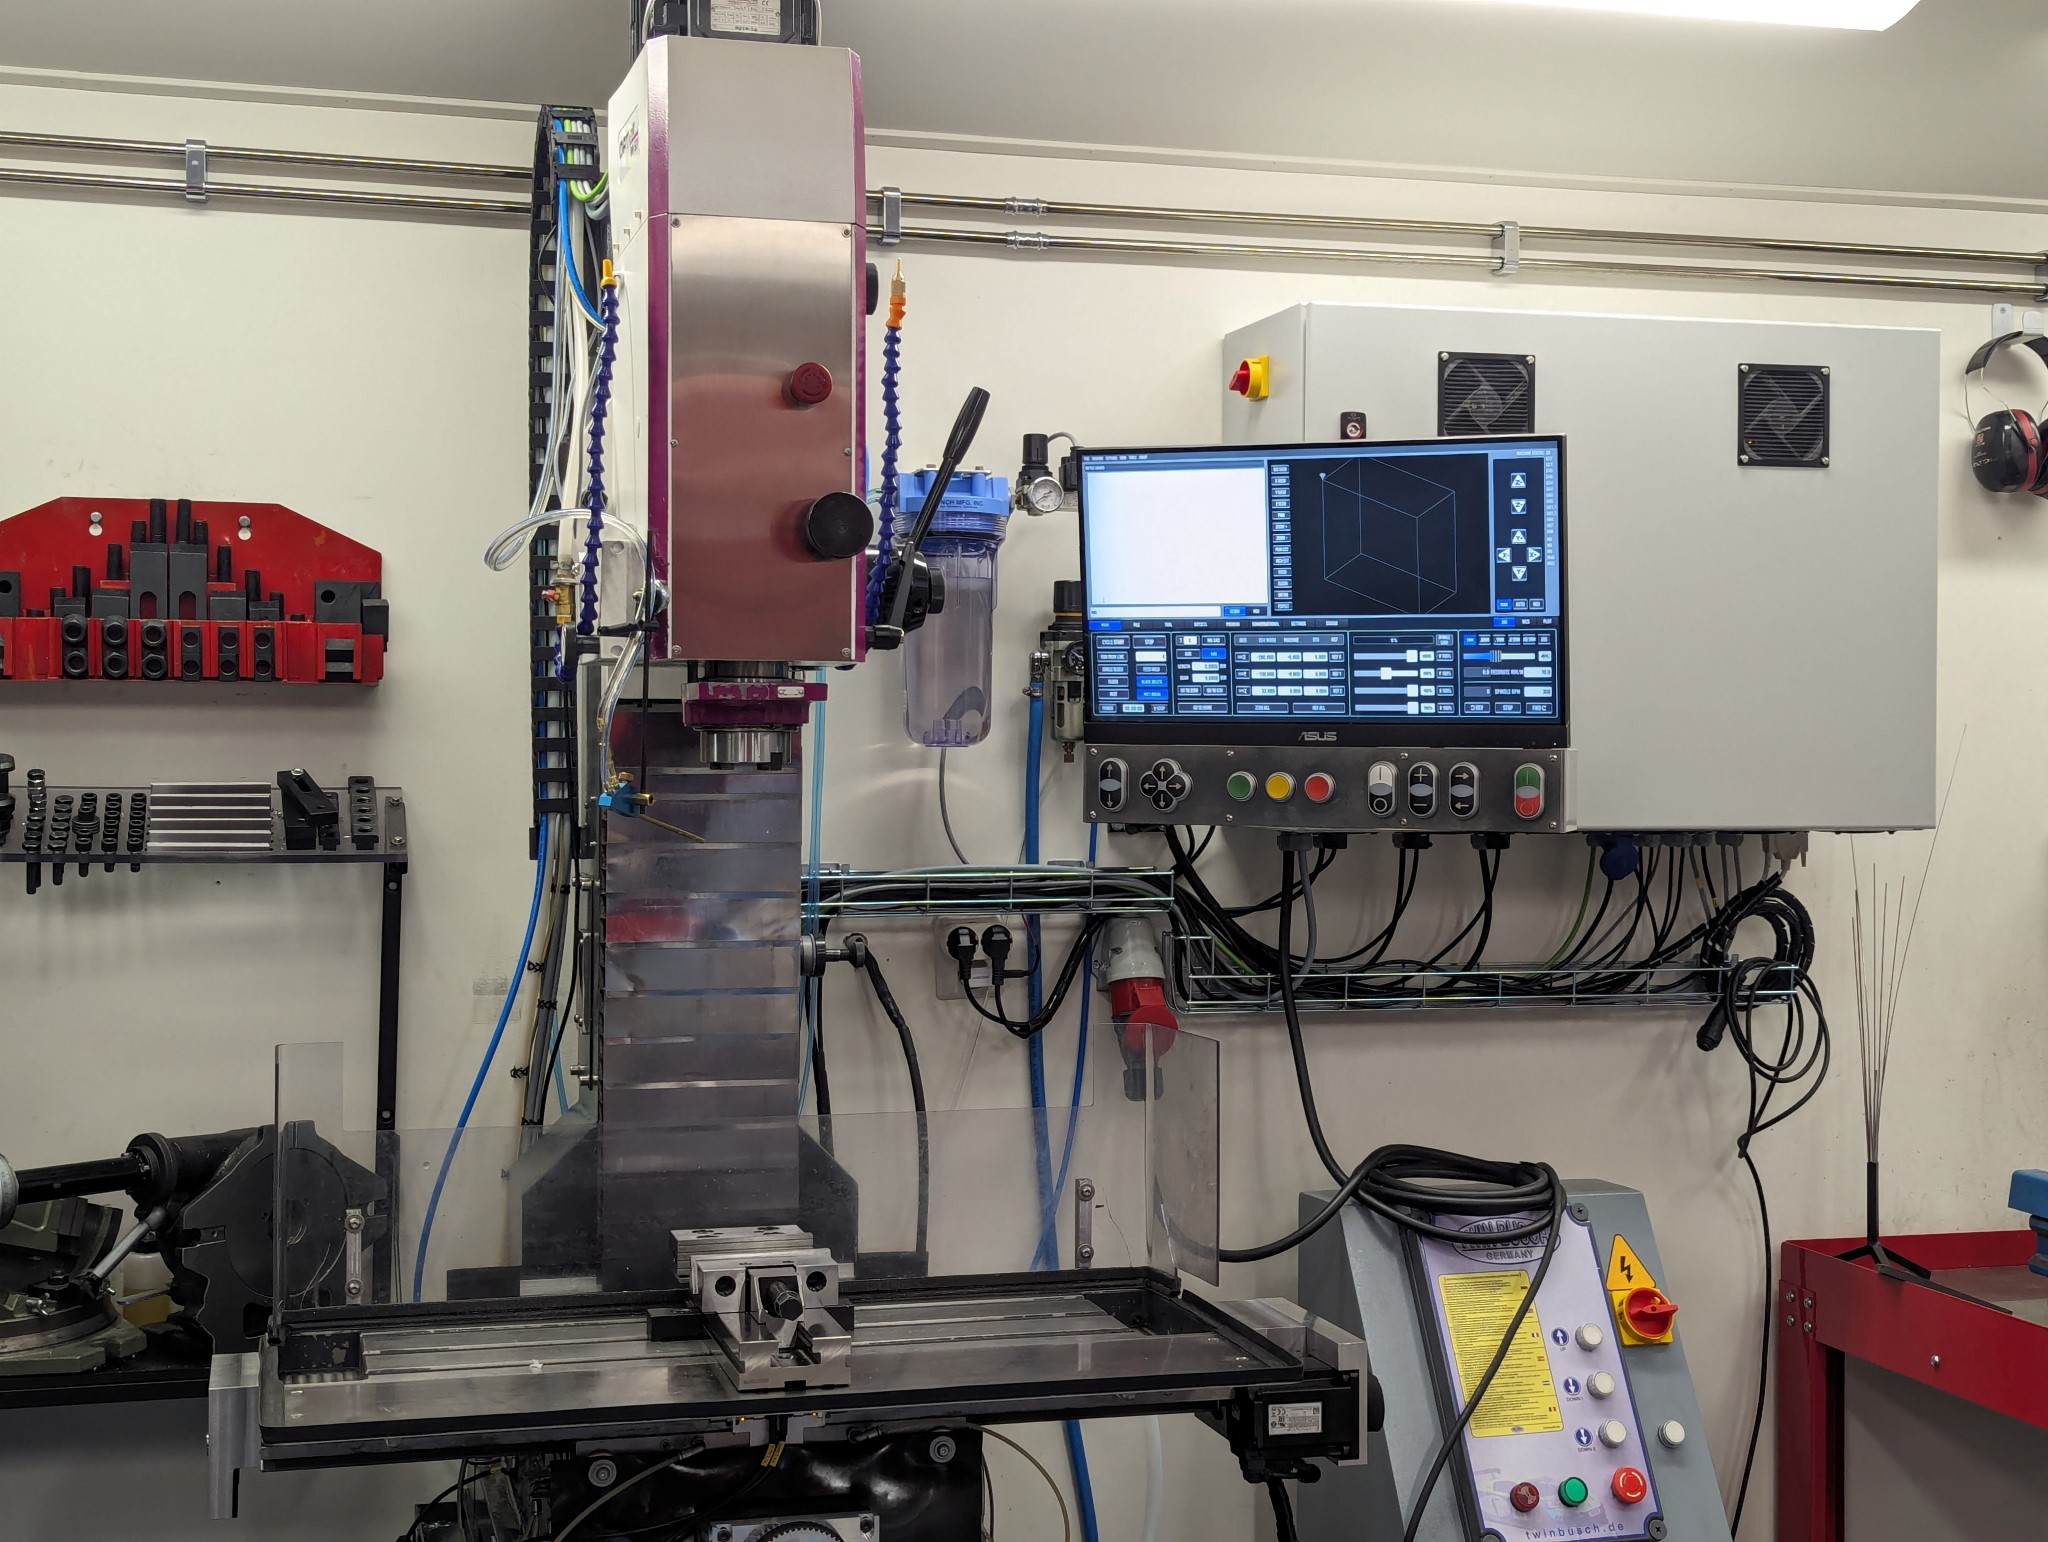
Here is how the machine looks at the moment.


I need to setup the limit switches in INI/HAL files and properly test them before I can do any serious milling however. I also currently don't have any encoder connected so I don't have closed loop RPM control or the ability to do rigid tapping at the moment.

In preparation for an encoder I installed a shielded 8-wire cable between the mill and the electrical cabinet. I just need to find the right encoder now. Preferably I'd want a 5v encoder that work with the Mesa 7i96S without the need for an optocoupler or voltage level shifter. However finding the right encoder has proven a bit more challenging than I first had anticipated. Any recommendations are very welcome image missing /media/kunena/emoticons/smile.png

I've found this Omron model which seems interesting but I'm not sure if it's the right specification and it mentions a maximum cable length of 2m in the specification which seems a bit short (if I'm reading the specification correctly). The shielded 8-wire cable I have already installed is about 5 meters long.

www.ia.omron.com/product/item/2500/


The following user(s) said Thank You: tommylight

Please Log in or Create an account to join the conversation.

Time to create page: 0.181 seconds
Powered by Kunena Forum