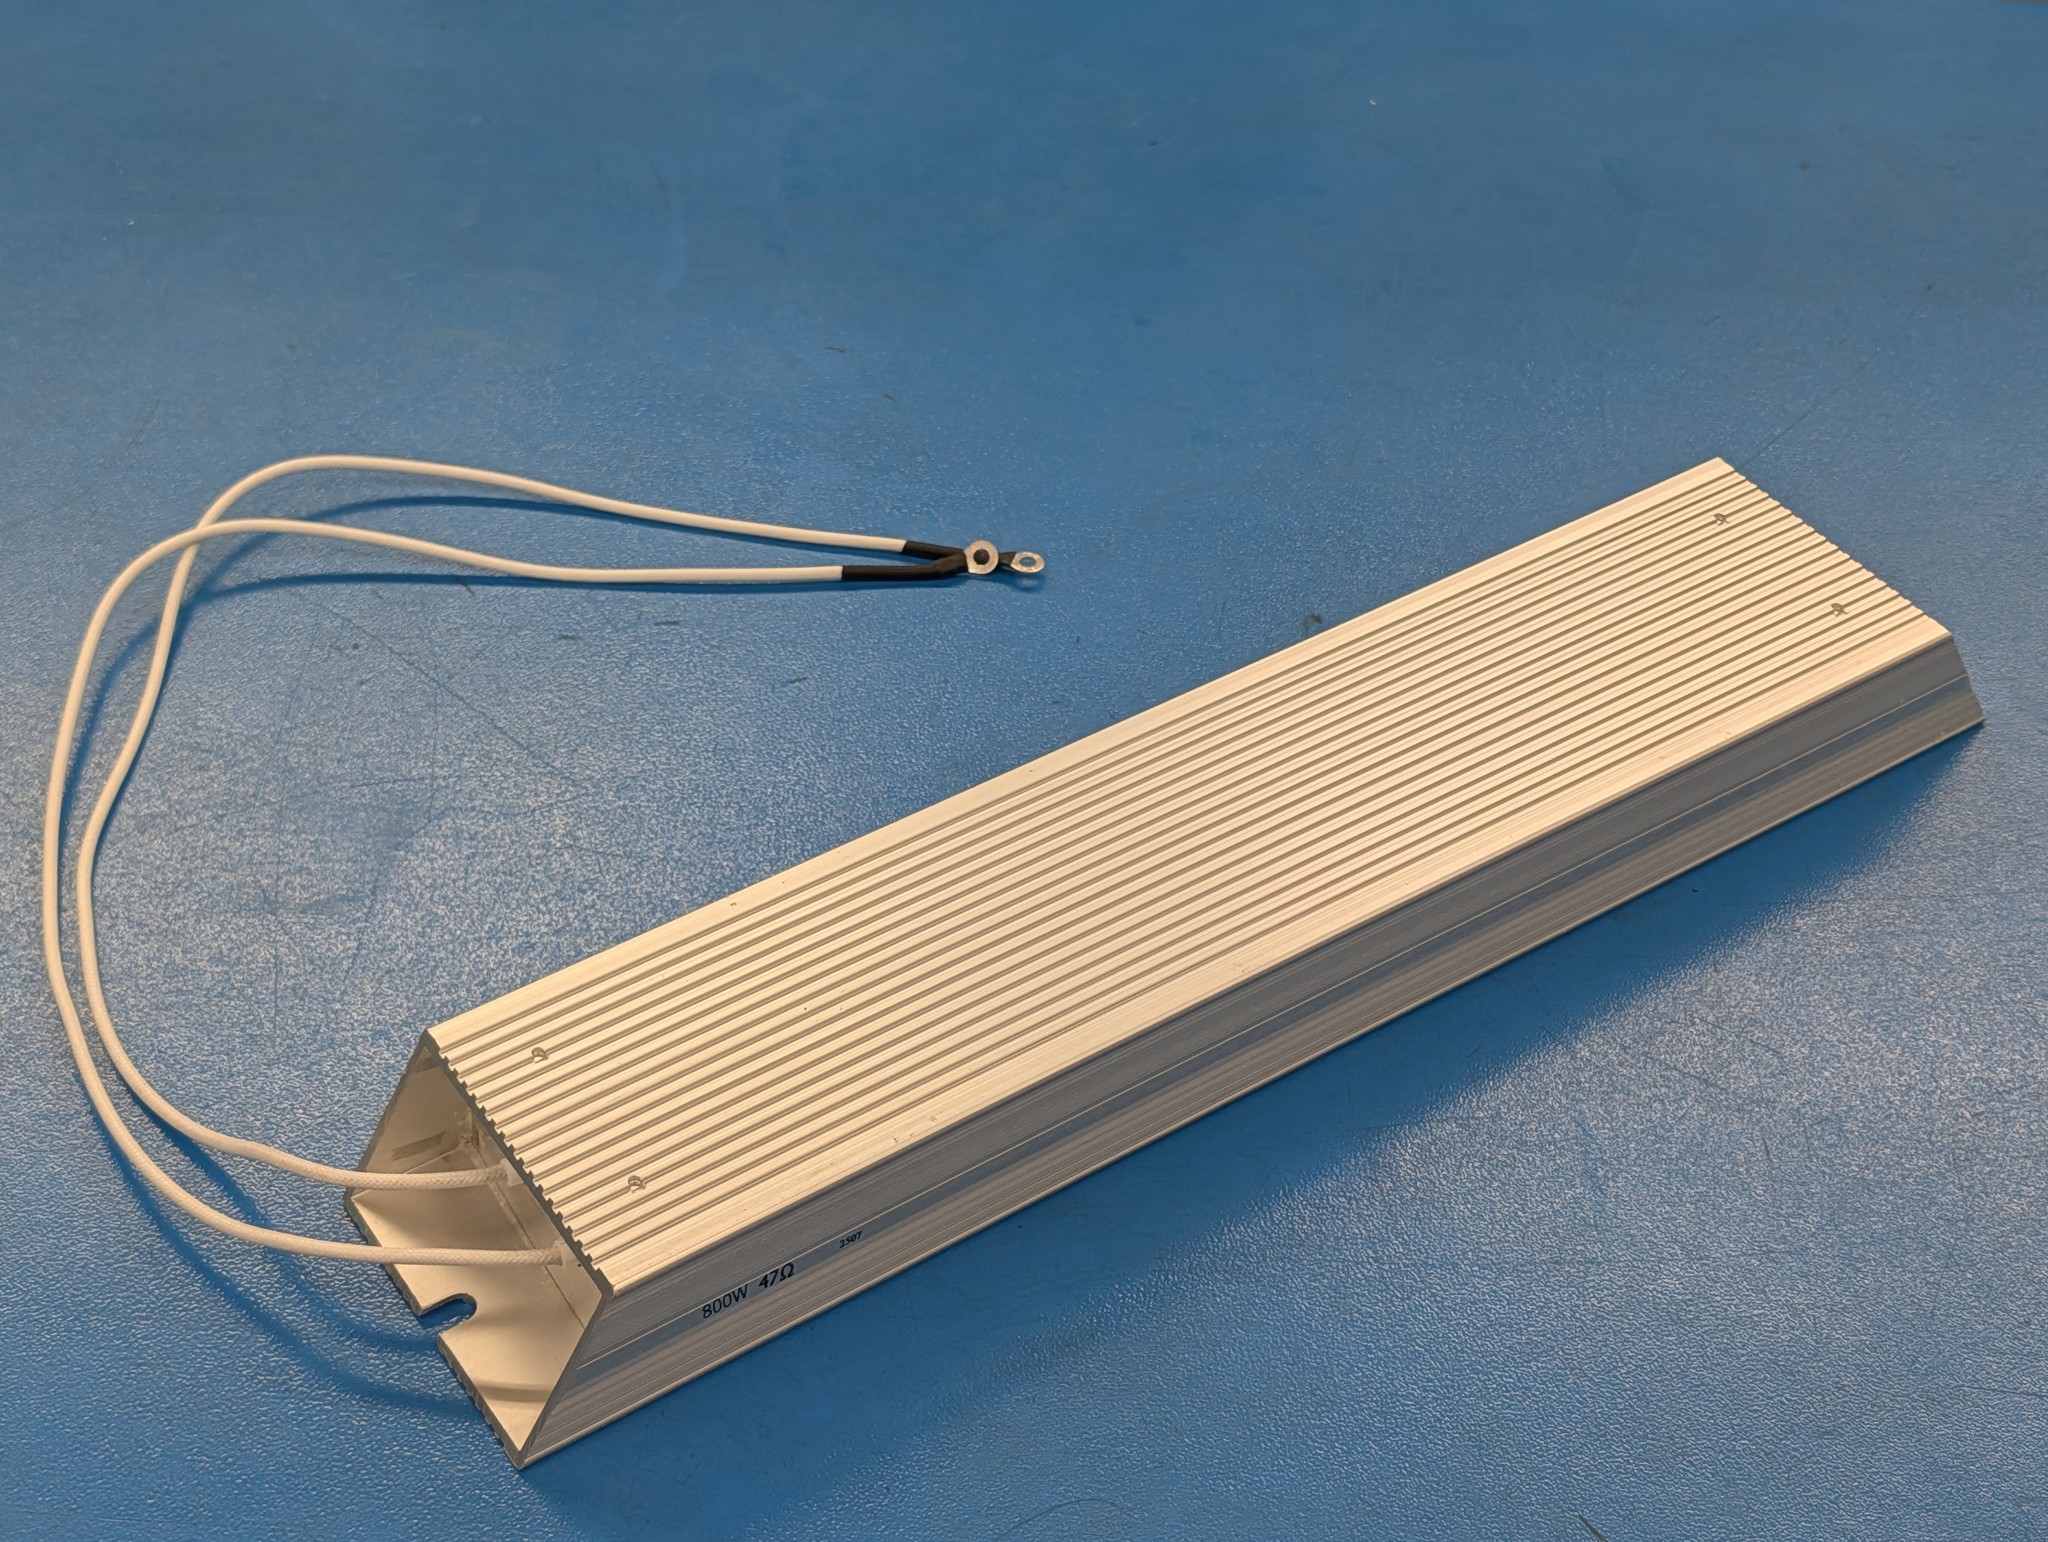
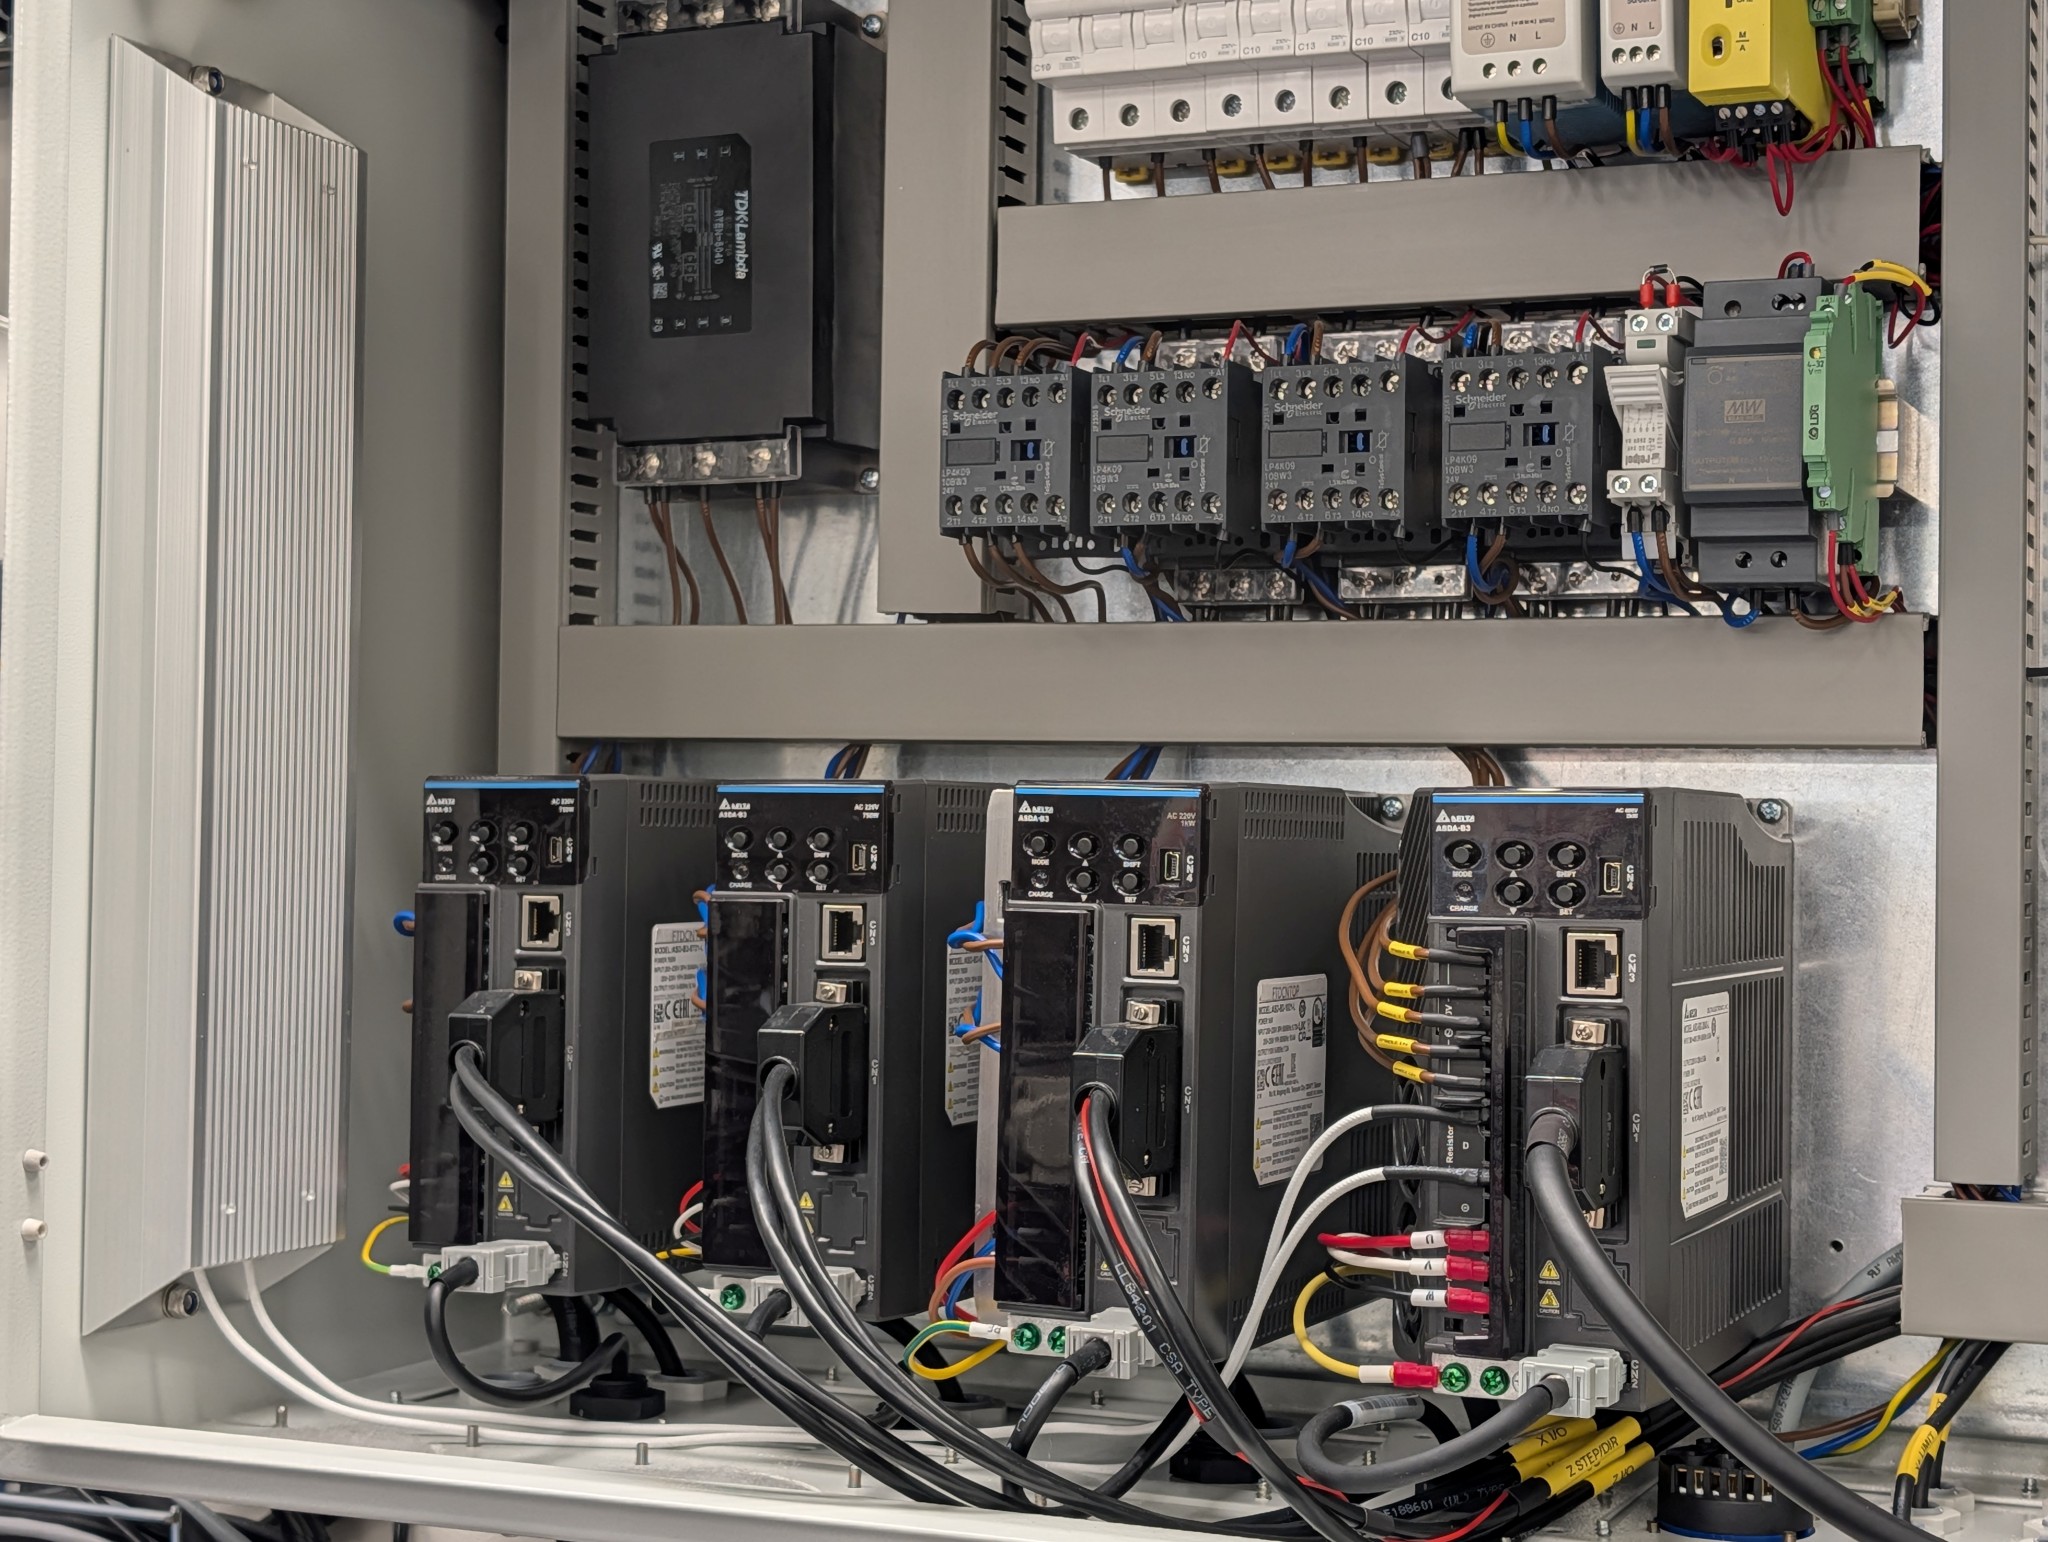
I received the braking resistor yesterday and mounted it on the left side of the cabinet. The cables that came with it were just long enough to reach all the way to the spindle drive.
With the braking resistor installed and the parameters set in the spindle drive the faults when stopping the spindle from high RPM disappeared.
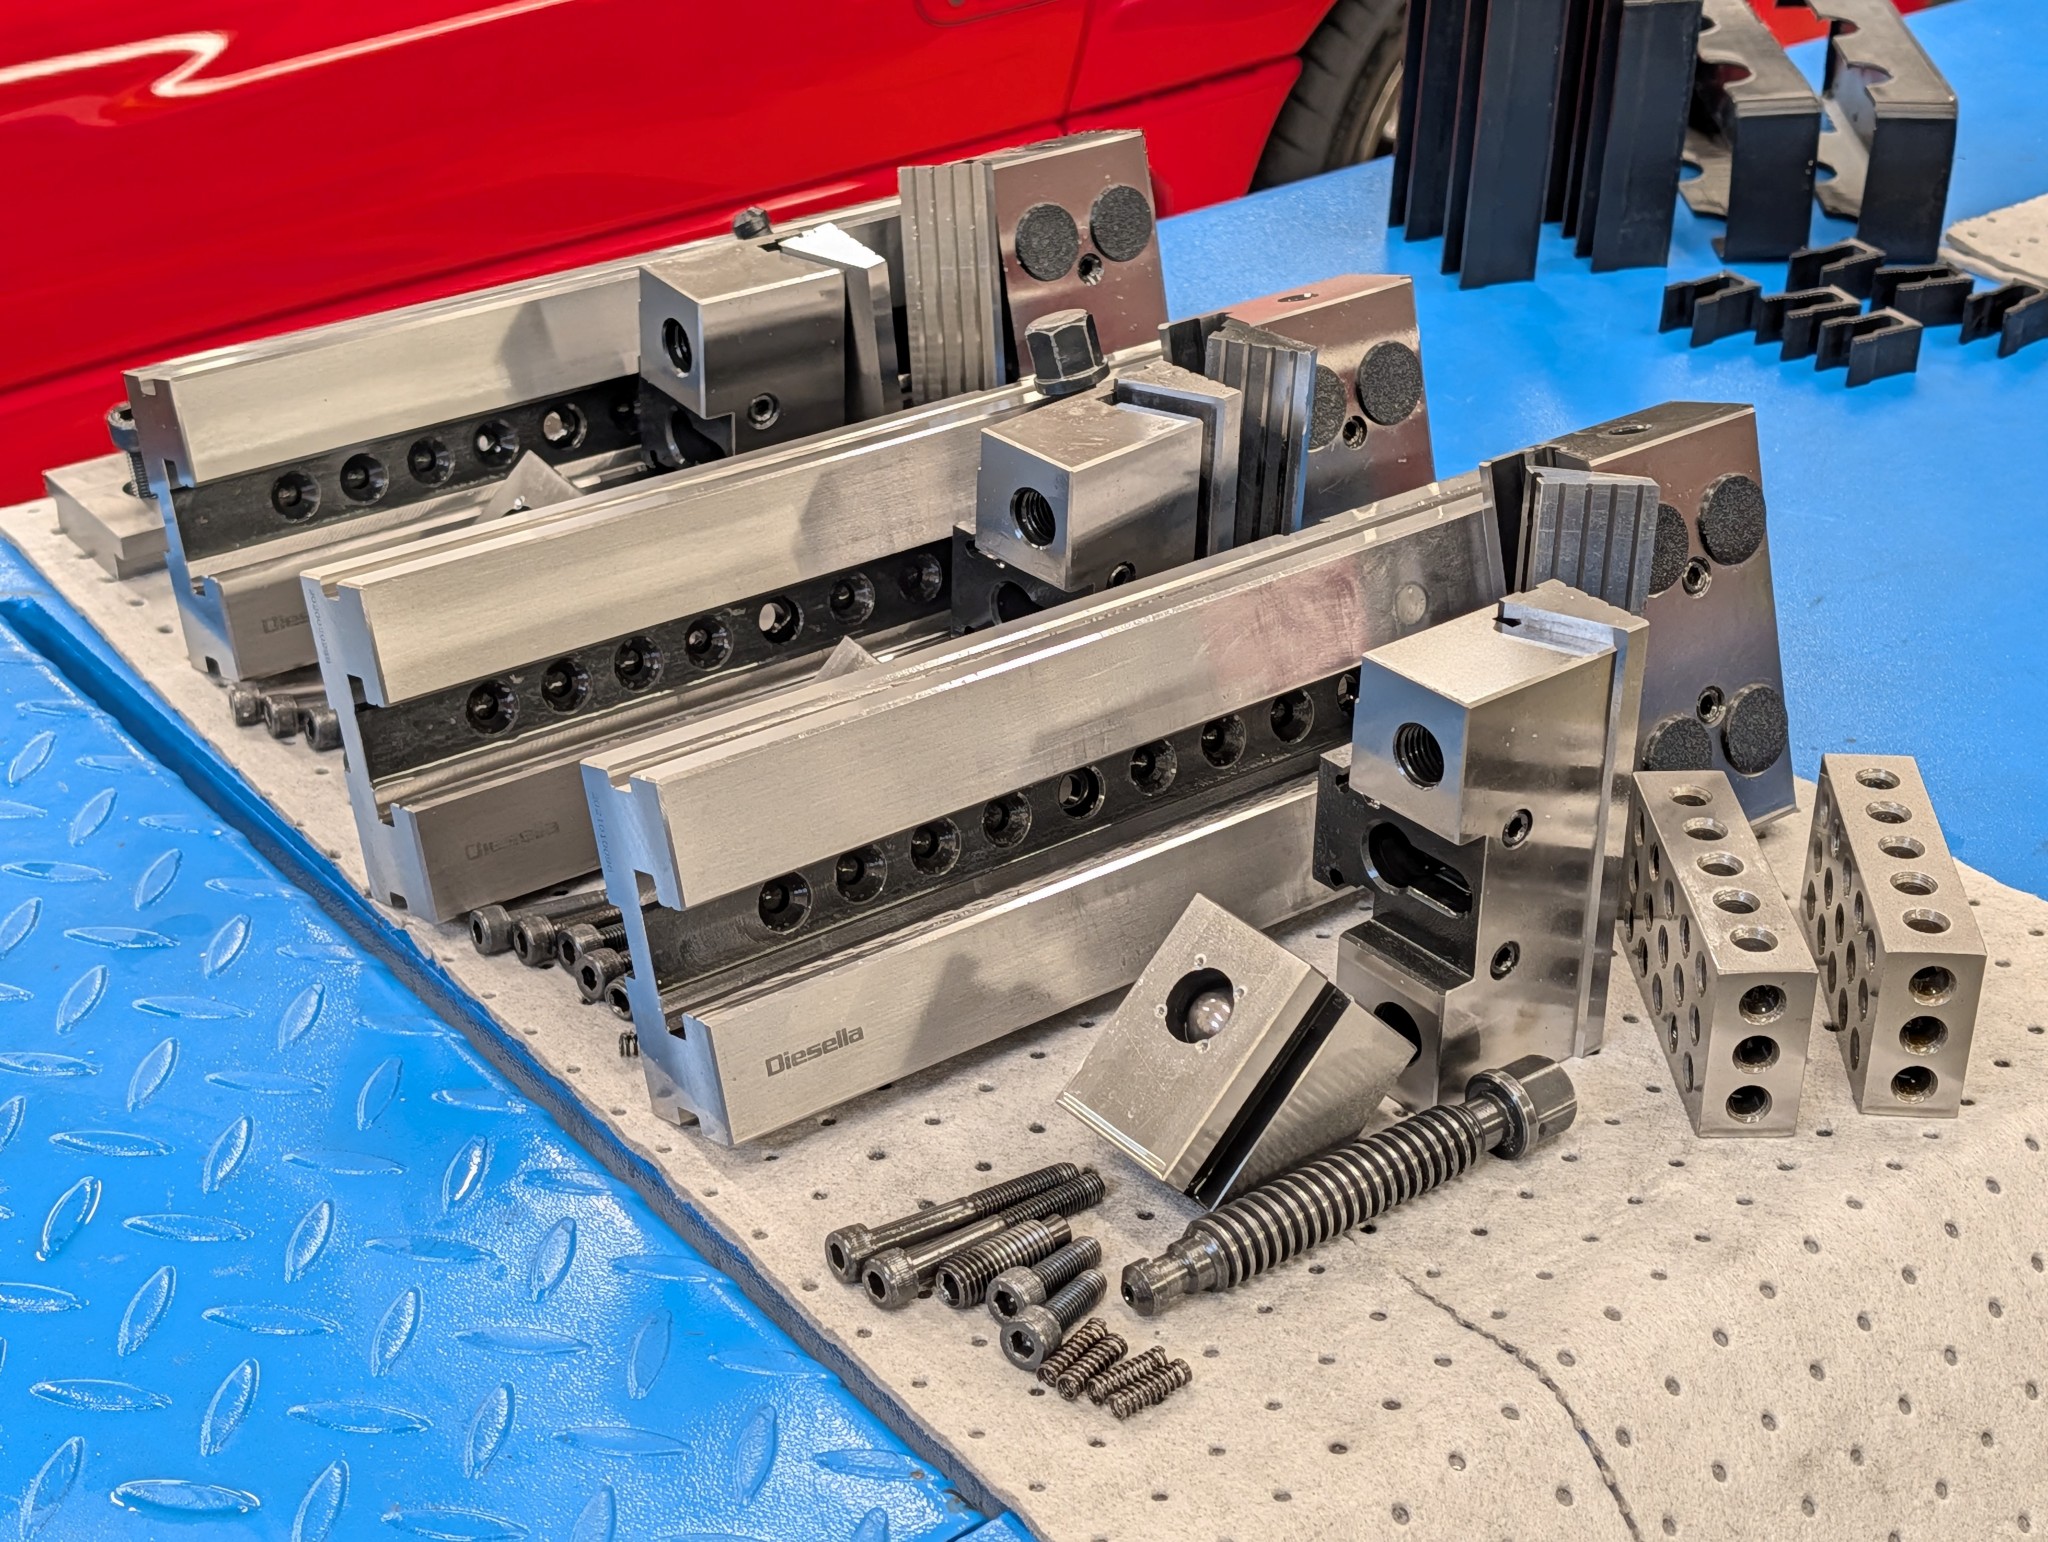
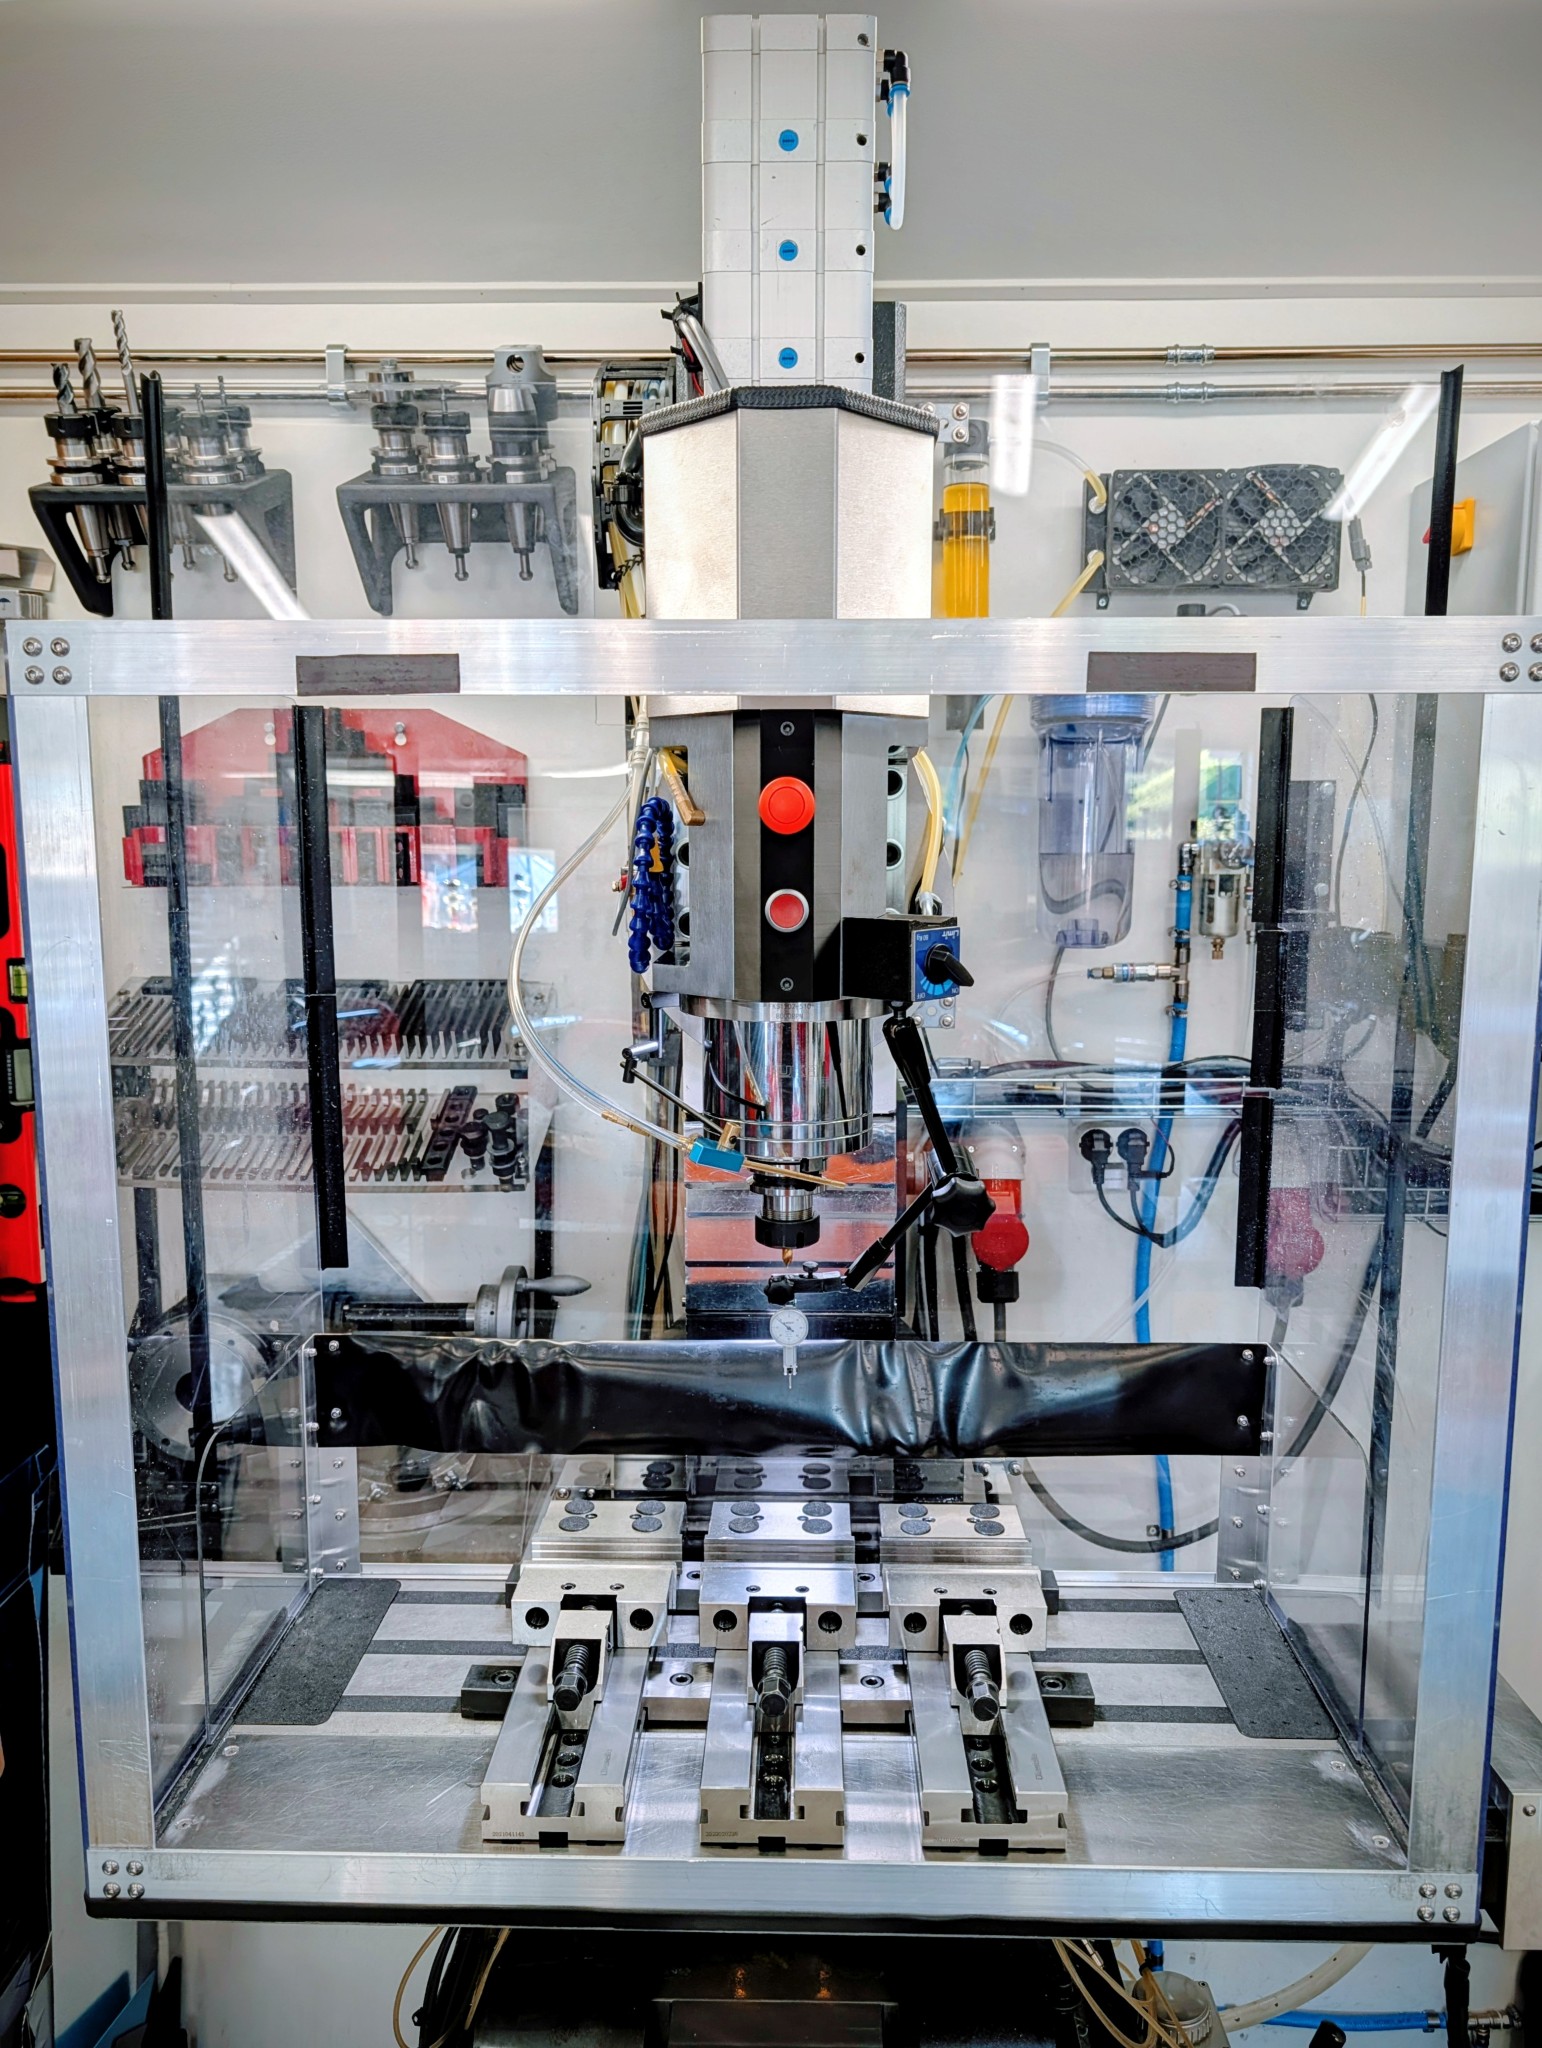
As the machine seemed to be ready for the first test cuts I cleaned the vices in the parts cleaner and installed them.
Getting all three of them trammed in took it's time as usual...
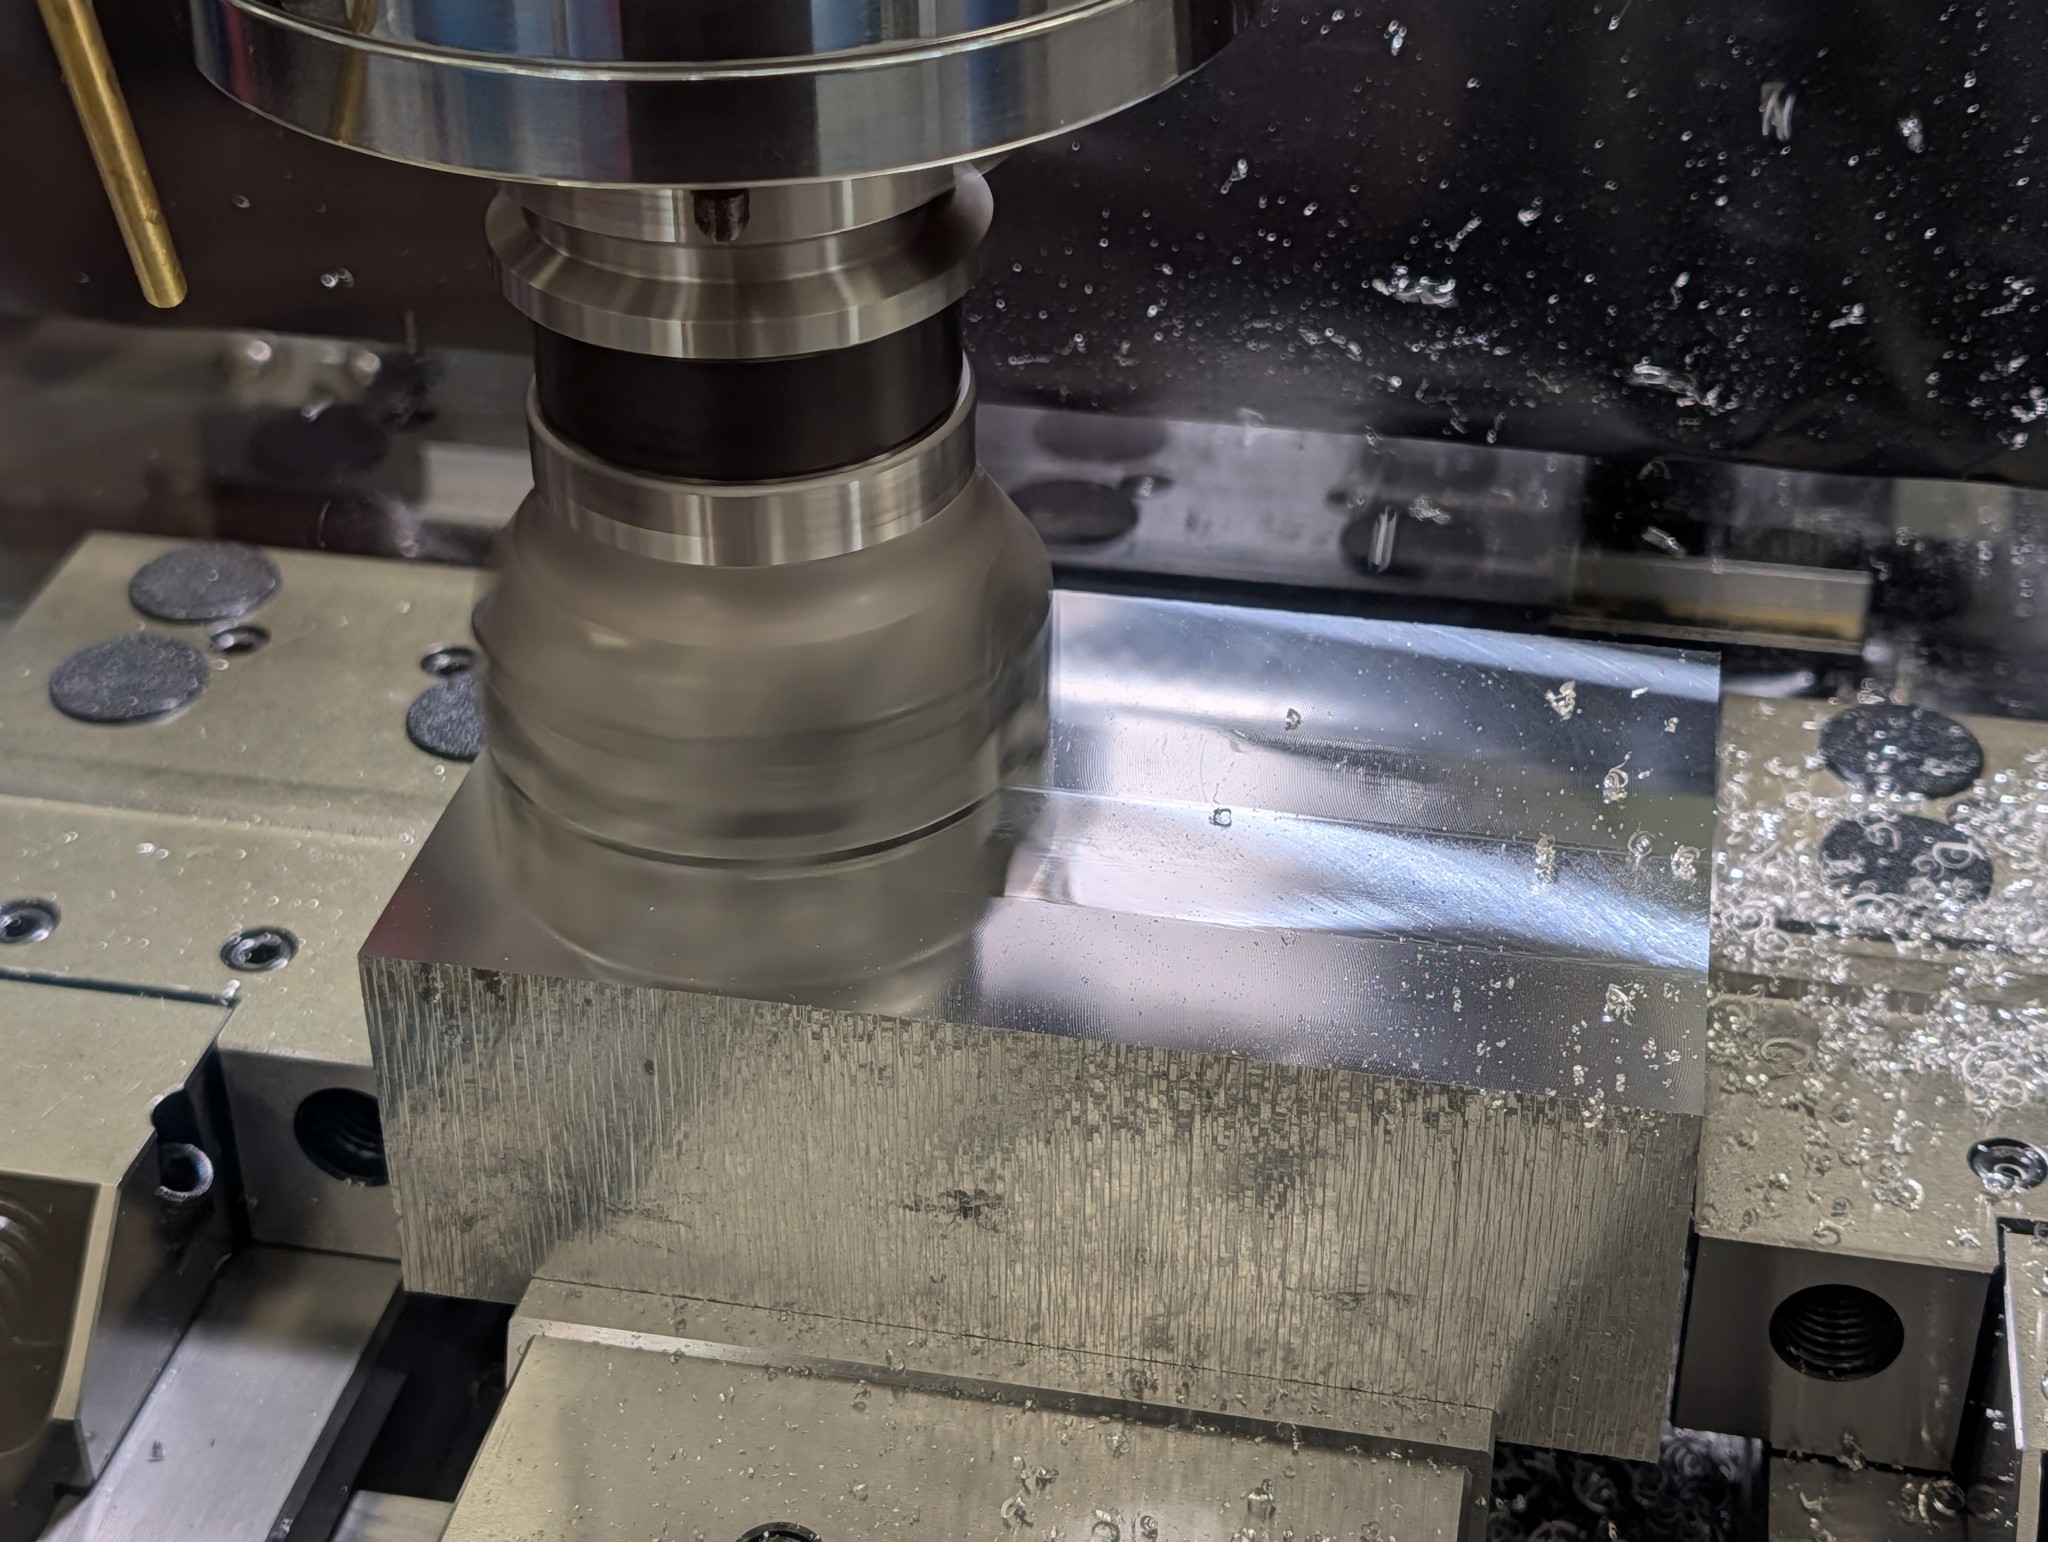
For the first nervous test cuts with the new spindle I used a piece of 7075 aluminum.
I started with an 80 mm face mill and immediately noticed a clear improvement in surface finish which I hadn't expected.
Next I milled the sides with a 16mm DLC coated solid end mill. The resulting finish was something I've never seen on this machine before.
This was just a quick cut with a width of 0,5 mm so this feels very promising. I'll report back when I've milled a few real parts.