
- Posts: 77
- Thank you received: 1
Rigid Tapping Help
- NCPatrol
- Offline
- Senior Member
-

Less
More
8 years 3 months ago - 8 years 3 months ago #115033
by NCPatrol
Replied by NCPatrol on topic Rigid Tapping Help
This is Serries 2 Boss 5...I don't know that any of the Boss series came with a drawbar, though there is some conflicting information out there on this topic.
This head is very different from a standard Bridgeport head in that it was 100% designed for CNC out of the box - ball screws, no quill, etc. I believe the back gear setup is entirely different too.
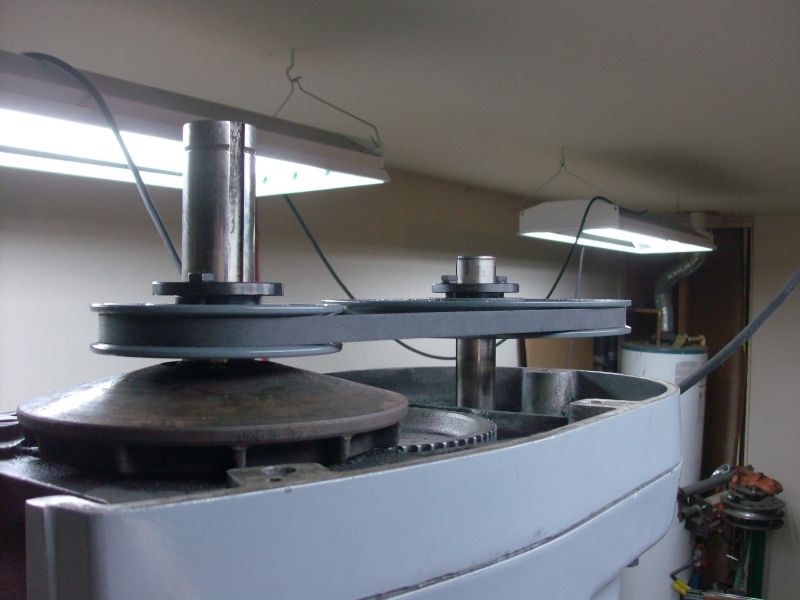
This is the only pic I can find of my head at the moment. The encoder is on the shaft closest to you, left side of the picture. That shaft's speed remains constant relative to the motor. The gear train is directly below that.
This head is very different from a standard Bridgeport head in that it was 100% designed for CNC out of the box - ball screws, no quill, etc. I believe the back gear setup is entirely different too.
This is the only pic I can find of my head at the moment. The encoder is on the shaft closest to you, left side of the picture. That shaft's speed remains constant relative to the motor. The gear train is directly below that.
Last edit: 8 years 3 months ago by NCPatrol.
Please Log in or Create an account to join the conversation.
- andypugh
- Offline
- Moderator
-

Less
More
- Posts: 19899
- Thank you received: 4655
8 years 3 months ago #115034
by andypugh
Replied by andypugh on topic Rigid Tapping Help
You didn't answer the "it" question.
If "it" is the commanded spindle speed then you would expect a disparity.
But have you monitored the spindle encoder velocity pin? Note that it measures in revs per _second_.
If "it" is the commanded spindle speed then you would expect a disparity.
But have you monitored the spindle encoder velocity pin? Note that it measures in revs per _second_.
Please Log in or Create an account to join the conversation.
- andypugh
- Offline
- Moderator
-
Less
More
- Posts: 19899
- Thank you received: 4655
8 years 3 months ago #115036
by andypugh
Replied by andypugh on topic Rigid Tapping Help
Is the shaft hollow? Is there a true-speed shaft available down the bore?
Please Log in or Create an account to join the conversation.
- NCPatrol
- Offline
- Senior Member
-
Less
More
- Posts: 77
- Thank you received: 1
8 years 3 months ago #115039
by NCPatrol
"It" was referencing to the rpm shown on the linuxcnc display. Simple tapping program with spindle speed of 400. Out of back gear, displays shows ~400 and actual spindle speed (assumed) matches. In back gear, display still shows 400 but spindle speed is much slower. (Still looking for exact back gear ratio.)
The spindle is not hollow. Don't believe there's a way to get true speed in that shaft when in back gear.
Replied by NCPatrol on topic Rigid Tapping Help
andypugh wrote: You didn't answer the "it" question.
If "it" is the commanded spindle speed then you would expect a disparity.
But have you monitored the spindle encoder velocity pin? Note that it measures in revs per _second_.
"It" was referencing to the rpm shown on the linuxcnc display. Simple tapping program with spindle speed of 400. Out of back gear, displays shows ~400 and actual spindle speed (assumed) matches. In back gear, display still shows 400 but spindle speed is much slower. (Still looking for exact back gear ratio.)
The spindle is not hollow. Don't believe there's a way to get true speed in that shaft when in back gear.
Please Log in or Create an account to join the conversation.
- andypugh
- Offline
- Moderator
-
Less
More
- Posts: 19899
- Thank you received: 4655
8 years 3 months ago #115042
by andypugh
Replied by andypugh on topic Rigid Tapping Help
What is the display showing, though? Is it connected to the encoder or to the command, in HAL?
If nothing else it sounds like you need to add this HAL component:
linuxcnc.org/docs/2.7/html/man/man9/gearchange.9.html
Which I think was designed for a Bridgeport.
Before assuming that the system isn't working I think it is worth putting a halmeter on the encoder velocity just in case. (I agree this is looking unlikely now)
Please Log in or Create an account to join the conversation.
- OT-CNC
- Offline
- Platinum Member
-

Less
More
- Posts: 617
- Thank you received: 75
8 years 3 months ago - 8 years 3 months ago #115064
by OT-CNC
Replied by OT-CNC on topic Rigid Tapping Help
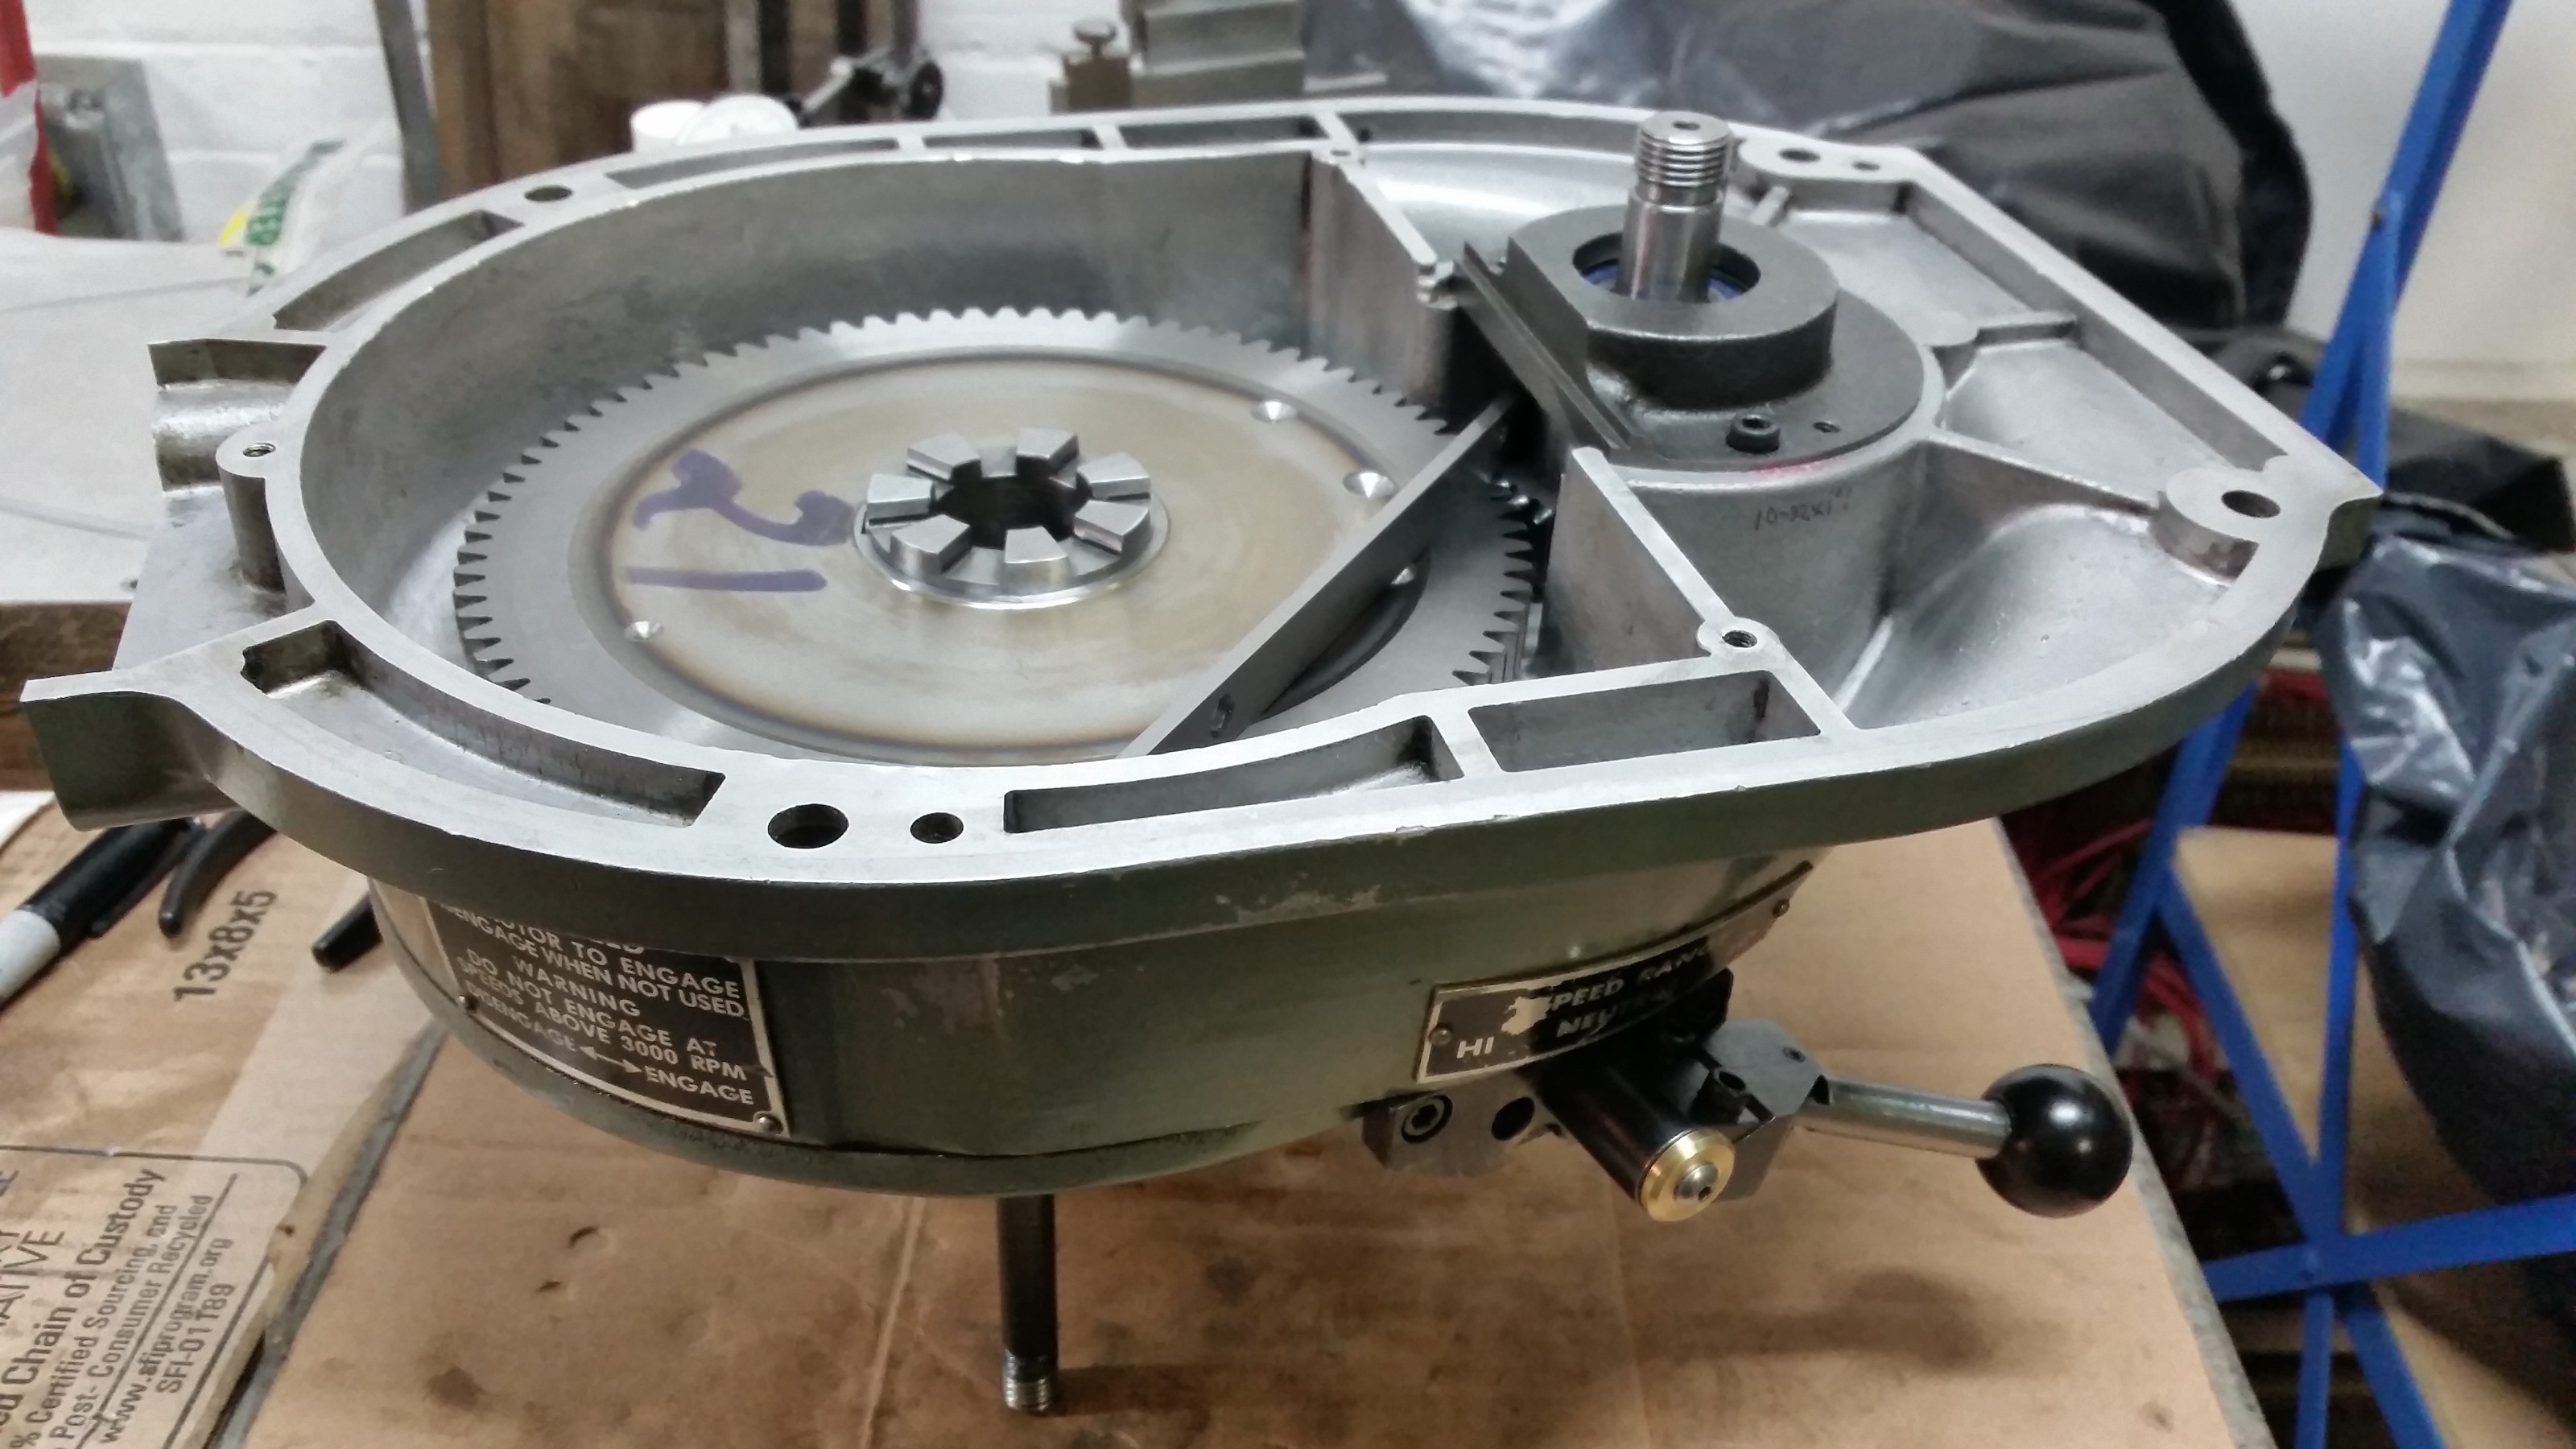
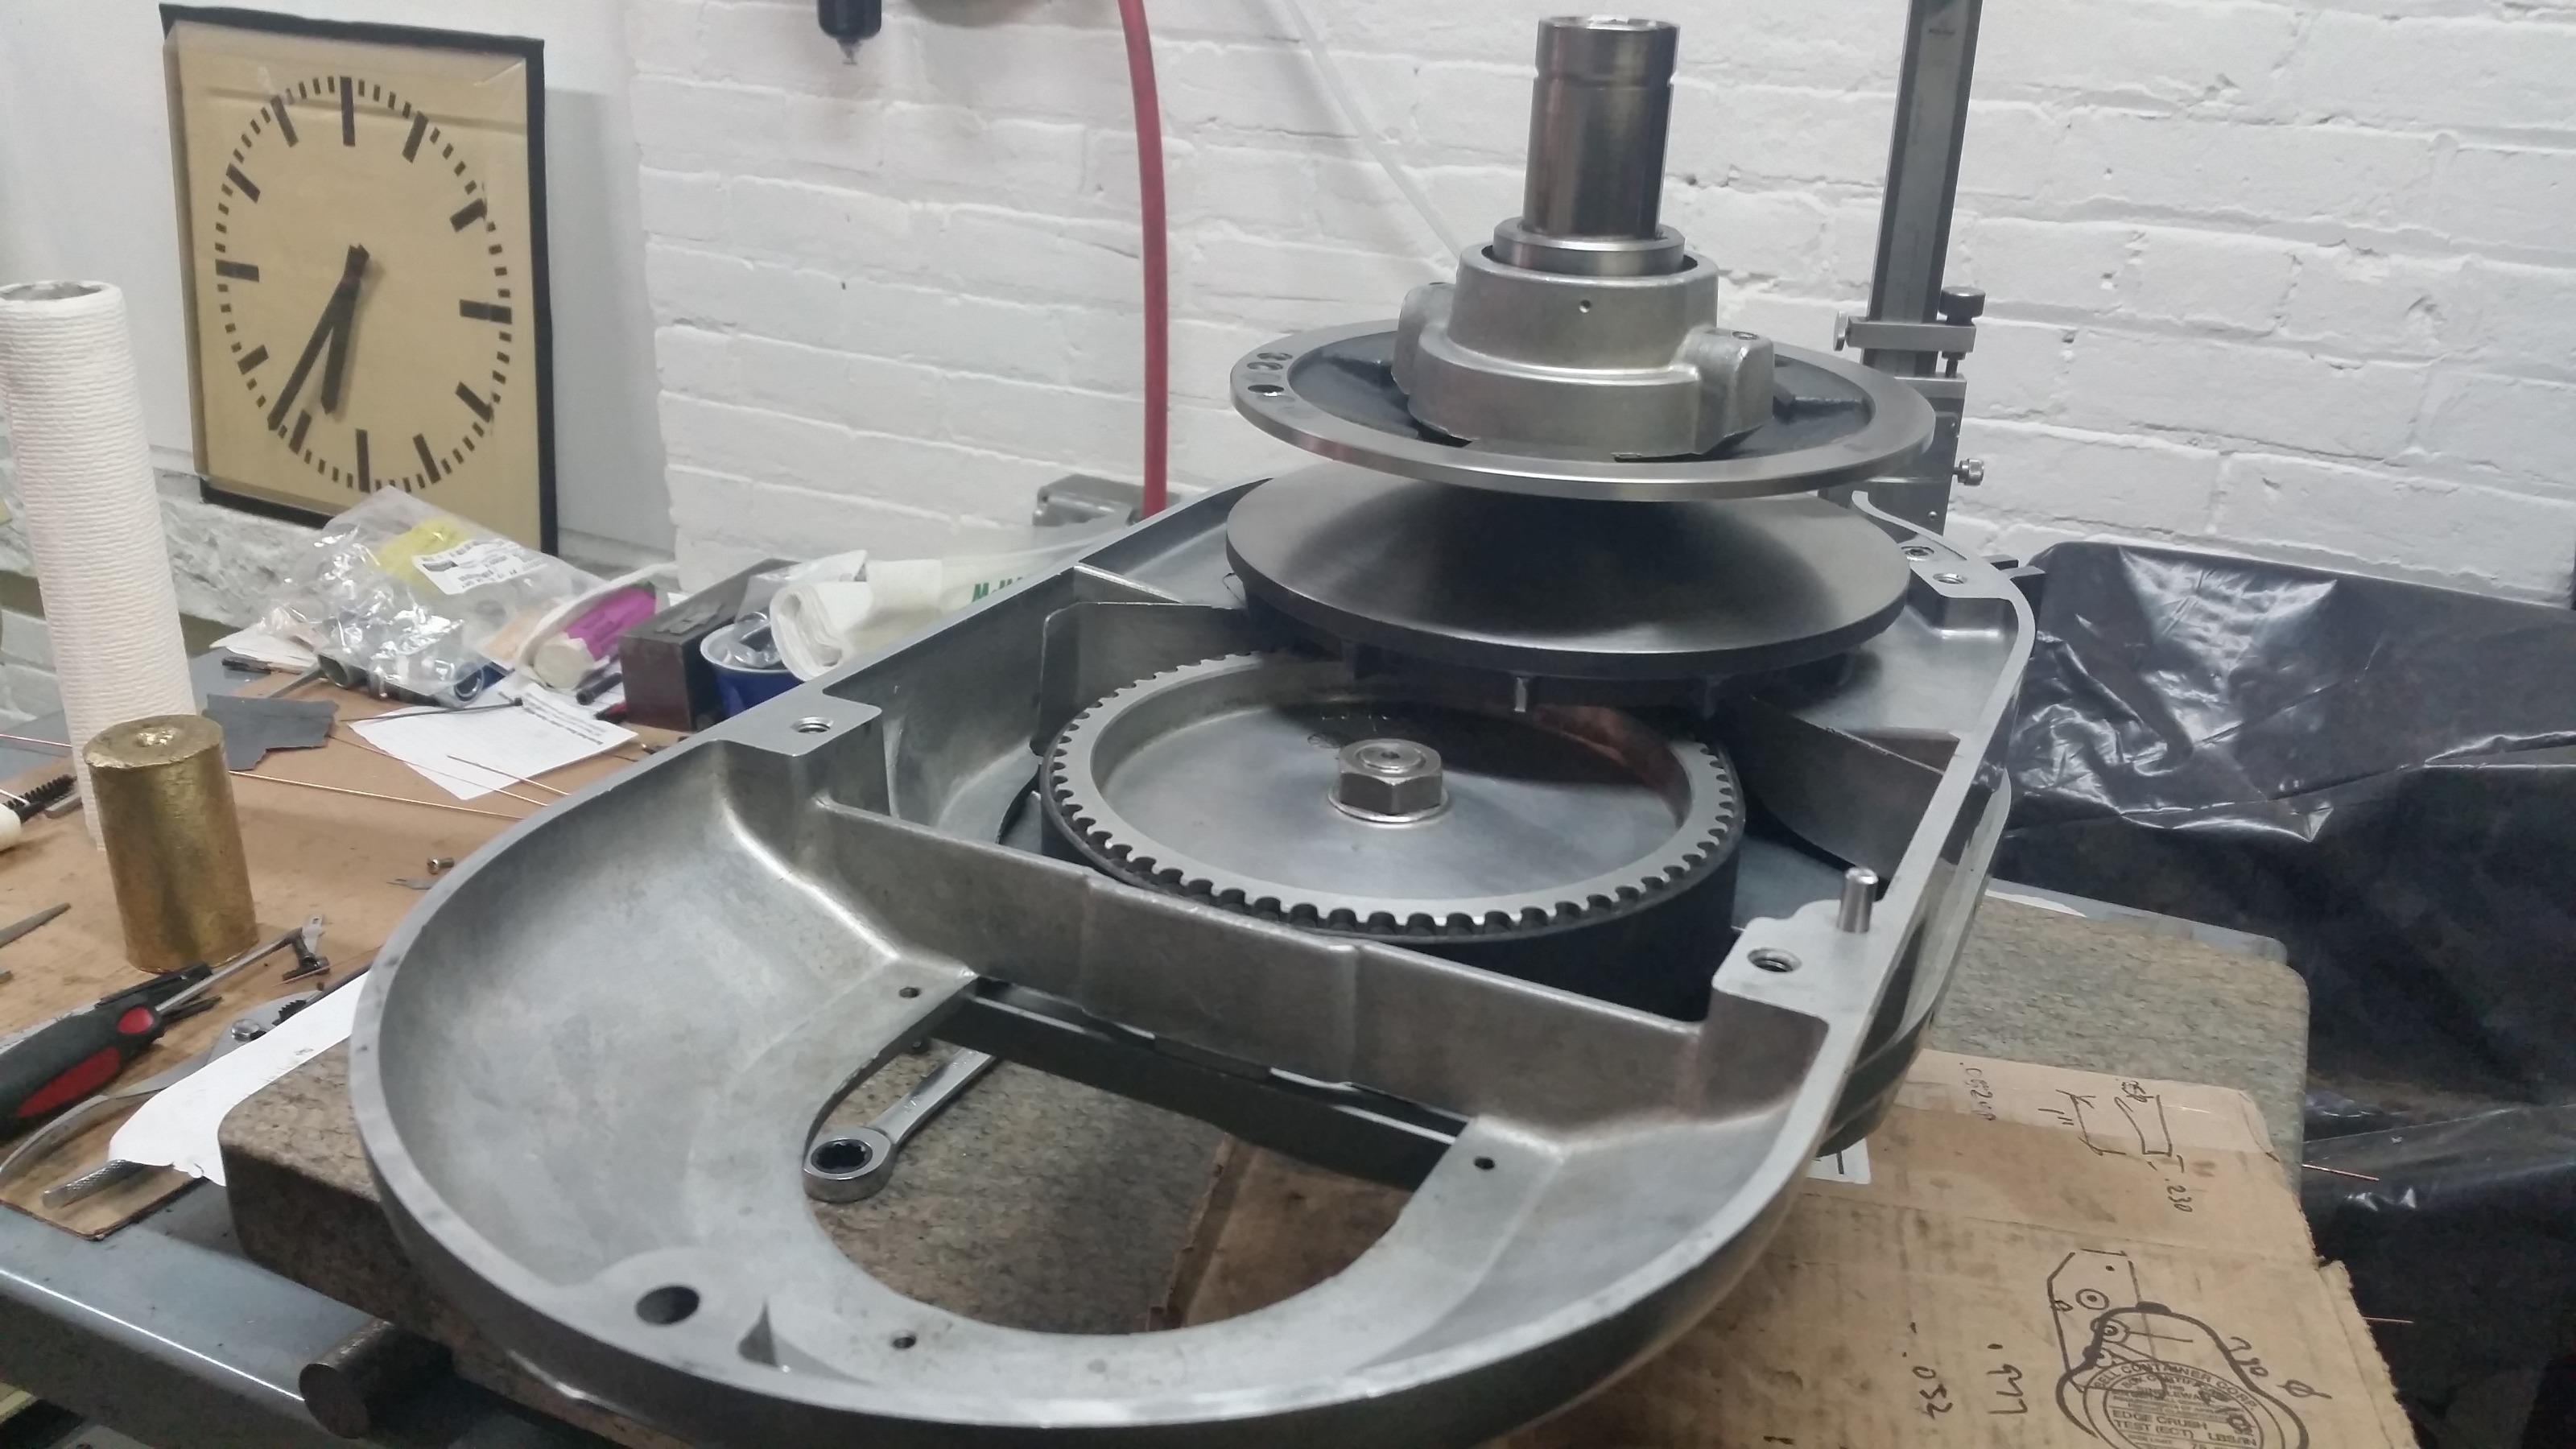
On the Bridgeports the upper shaft (where the vari-disc goes) will separate from the lower which is connected to the high/lo back gear. The lower hub is splined and drives the spindle. I recently tore the head apart on my machine to do some service and to add an encoder. I found there is really no practical way to fit one inside directly mounted to the splined gear hub as the hub moves up and down. I added the encoder to the top like on the OP's machine. I use KS tooling and don't have a draw bar.
NCpatrol's machine is different than my standard knee mill but I bet the backgear mechanism is similar. His has the annoying varidiscs replaced with a fixed pulley. We just have to figure out the lower gear ratio. I failed to count the gears on mine and have not yet configured that correctly for back gear. I'll have another look. In the mean time, if anyone knows the back gear ratio please post. Thanks!
Andy, thanks for posting the gear change link. I have been meaning to add that to my mill.
NCpatrol's machine is different than my standard knee mill but I bet the backgear mechanism is similar. His has the annoying varidiscs replaced with a fixed pulley. We just have to figure out the lower gear ratio. I failed to count the gears on mine and have not yet configured that correctly for back gear. I'll have another look. In the mean time, if anyone knows the back gear ratio please post. Thanks!
Andy, thanks for posting the gear change link. I have been meaning to add that to my mill.
Last edit: 8 years 3 months ago by OT-CNC. Reason: format
Please Log in or Create an account to join the conversation.
Time to create page: 0.502 seconds