
- Posts: 1635
- Thank you received: 595
Schaublin 125-CNC retrofit.
- RotarySMP
- Offline
- Platinum Member
-

Less
More
3 years 10 months ago #259581
by RotarySMP
Replied by RotarySMP on topic Schaublin 125-CNC retrofit.
I had to edit my answers as I am juggling video files on the LCNC computor, screen grabing on the MBP, and also on the Zbook.
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
3 years 10 months ago #259582
by RotarySMP
Replied by RotarySMP on topic Schaublin 125-CNC retrofit.
"The ringing is indicative of excessive holding TQ in the motor driver. If you put your hand on it, can you feel it ringing when it is sitting still ?"
No, I feel nothing, also the Osci plot when no motion is commanded is completely flat.
No, I feel nothing, also the Osci plot when no motion is commanded is completely flat.
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
3 years 10 months ago #259583
by RotarySMP
Replied by RotarySMP on topic Schaublin 125-CNC retrofit.
". p05-10 & p05-11 these are the internal TQ limits, what are these settings ?"
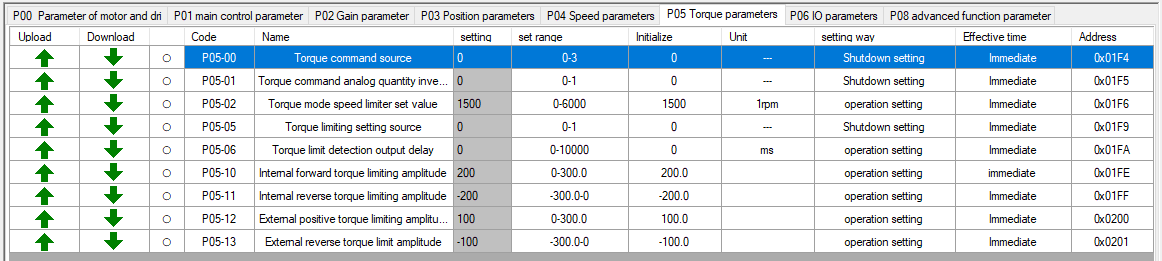
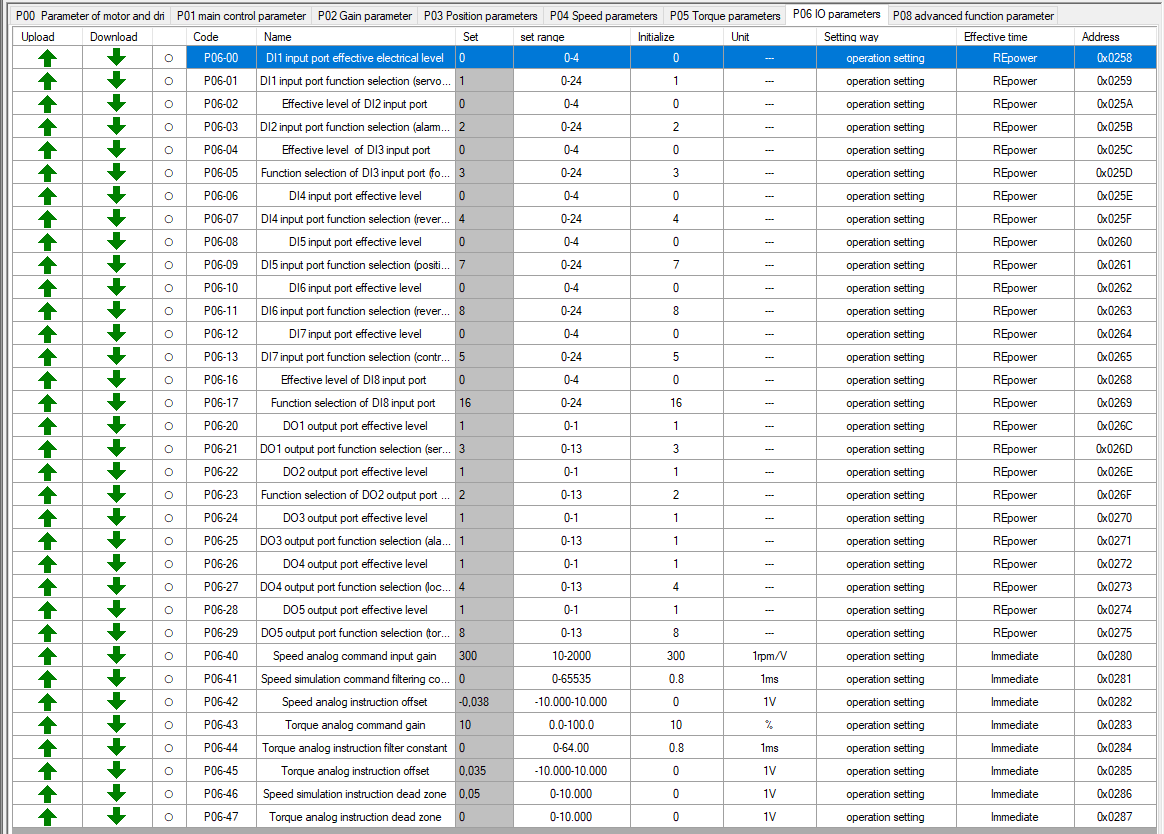
"p06-40 is the input gain value, this will matter once we know the values for the motor max speed, and the lead screw pitch. Given that you have been able to use the lathe and it seems to be making parts that are the correct size, it seems like the encoder counts are correct for the pitch."
Motormaxspeed= 3000rpm.
Lead screw pitch is 4mm in X. Everything here has been the X axis so far. Belt reduction is 2:1.
(Leadscrew pitch is 6mm in Z, Reduction 3:1 )
Correct, I have the encoder counts set correctly for those balls screws , reductions and quadrature. On both axis it is 5000 counts/mm
"p06-40 is the input gain value, this will matter once we know the values for the motor max speed, and the lead screw pitch. Given that you have been able to use the lathe and it seems to be making parts that are the correct size, it seems like the encoder counts are correct for the pitch."
Motormaxspeed= 3000rpm.
Lead screw pitch is 4mm in X. Everything here has been the X axis so far. Belt reduction is 2:1.
(Leadscrew pitch is 6mm in Z, Reduction 3:1 )
Correct, I have the encoder counts set correctly for those balls screws , reductions and quadrature. On both axis it is 5000 counts/mm
- smc.collins
- Offline
- Platinum Member
-
Less
More
- Posts: 723
- Thank you received: 139
3 years 10 months ago - 3 years 10 months ago #259597
by smc.collins
Replied by smc.collins on topic Schaublin 125-CNC retrofit.
sorry Mark, was typing on my phone. so if motor speed is 3000rpm and reduced 2:1 motor speed at the lead screw is a whopping 1500rpm , so 1500/4 is 375mm minute, or .35m/min or 5.8mm/sec
Try this first, turn your max motor speed upto 6000rpm, on both axis.
see if that resolves or improves the makeup gain situation. recalculate your velocity's from leadscrew pitch enter those values in your ini file
Try this first, turn your max motor speed upto 6000rpm, on both axis.
see if that resolves or improves the makeup gain situation. recalculate your velocity's from leadscrew pitch enter those values in your ini file
Last edit: 3 years 10 months ago by smc.collins.
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
3 years 10 months ago #259614
by RotarySMP
Replied by RotarySMP on topic Schaublin 125-CNC retrofit.
"1500/4 is 375mm minute"
1500x4 = 6000mm/minute

I have it limited in the INI to 3m/min, which is more than fast enough for such small travels.
1500x4 = 6000mm/minute
I have it limited in the INI to 3m/min, which is more than fast enough for such small travels.
- smc.collins
- Offline
- Platinum Member
-
Less
More
- Posts: 723
- Thank you received: 139
3 years 10 months ago - 3 years 10 months ago #259639
by smc.collins
Replied by smc.collins on topic Schaublin 125-CNC retrofit.
linuxcnc calculates vout from voltage and velocity
if you have 3m/m in your ini over a 10v span, than you need to make sure the drive gives 3m/m over the same span.
that is why you have the gain error. yes my math was backwards, I've been busy trying to solve a different issue.and my brain crossed some wires.
so let me illustrate your gain issue.
of you send a command of 3v, do you get 1m/m ?
if you send 6v do you get 2m/m
lets say the machine could go say 5m/min
same thing
you voltage scaling to velocity is effected by you values in your ini. afaict, your drives are runnig below the requested velocity as it stands. So you can lower you total max velocty setting this in the ini, or increase the drives total velocity to match.
the other possibility, with your current overshoot, is that your declared acceleration rate in your ini is higher than what the drive can achieve.
can you zoom that scop output more ??
Last edit: 3 years 10 months ago by smc.collins.
The following user(s) said Thank You: RotarySMP
Moderators: piasdom
Time to create page: 0.166 seconds