Planning - Bridgeport Interact 1 linuxCNC Retrofit

More
10 years 8 months ago #69855 by csbrady
I started down the path of using modbus for my VFD but decided it would be much simpler to use +10v output and some GPIO lines to manage the VFD.

I suggest adding a couple extra lines to handle fault conditions. It's important to have a VFD fault trigger an estop. I didn't have this for some time and find that cutters that are not rotating do not cut well. The reverse is also a good idea, a signal to stop the VFD when there is a machine estop. I also added line to reset the VFD when an estop is cleared. These 3 signals insure that the machine and spindle are always in sync.

Please Log in or Create an account to join the conversation.

More
10 years 8 months ago #69859 by cncnoob1979
Andy; csbrady,

I'm thinking I will be going the GPIO route as well. Its just frustrating that the MODBUS is not implemented correctly in these VFD's. As I knew beforehand. However, given the fact that I will be manually changing spindle speeds via Vari drive control, I think this will be the best future proof of the spindle setup.

I do have multiple inputs/output pins available. I will have to look through your code csbrady to see how you implemented yours and do the same with mine.

Now I'm off to read Hal and tutorials on how to implement these changes. I'm thinking that to limit the GPIO to only 0-10V will be difficult for me to get my head around. I'm just now -barely- starting to understand how HAL works.

Please Log in or Create an account to join the conversation.
More
10 years 8 months ago #69860 by andypugh

cncnoob1979 wrote: Now I'm off to read Hal and tutorials on how to implement these changes. I'm thinking that to limit the GPIO to only 0-10V will be difficult for me to get my head around. I'm just now -barely- starting to understand how HAL works.


It's actually quite easy, you just need to use one of the motion.spindle-speed-out-*-abs pins:

linuxcnc.org/docs/2.7/html/man/man9/motion.9.html

Please Log in or Create an account to join the conversation.
More
10 years 8 months ago - 10 years 8 months ago #69901 by cncnoob1979
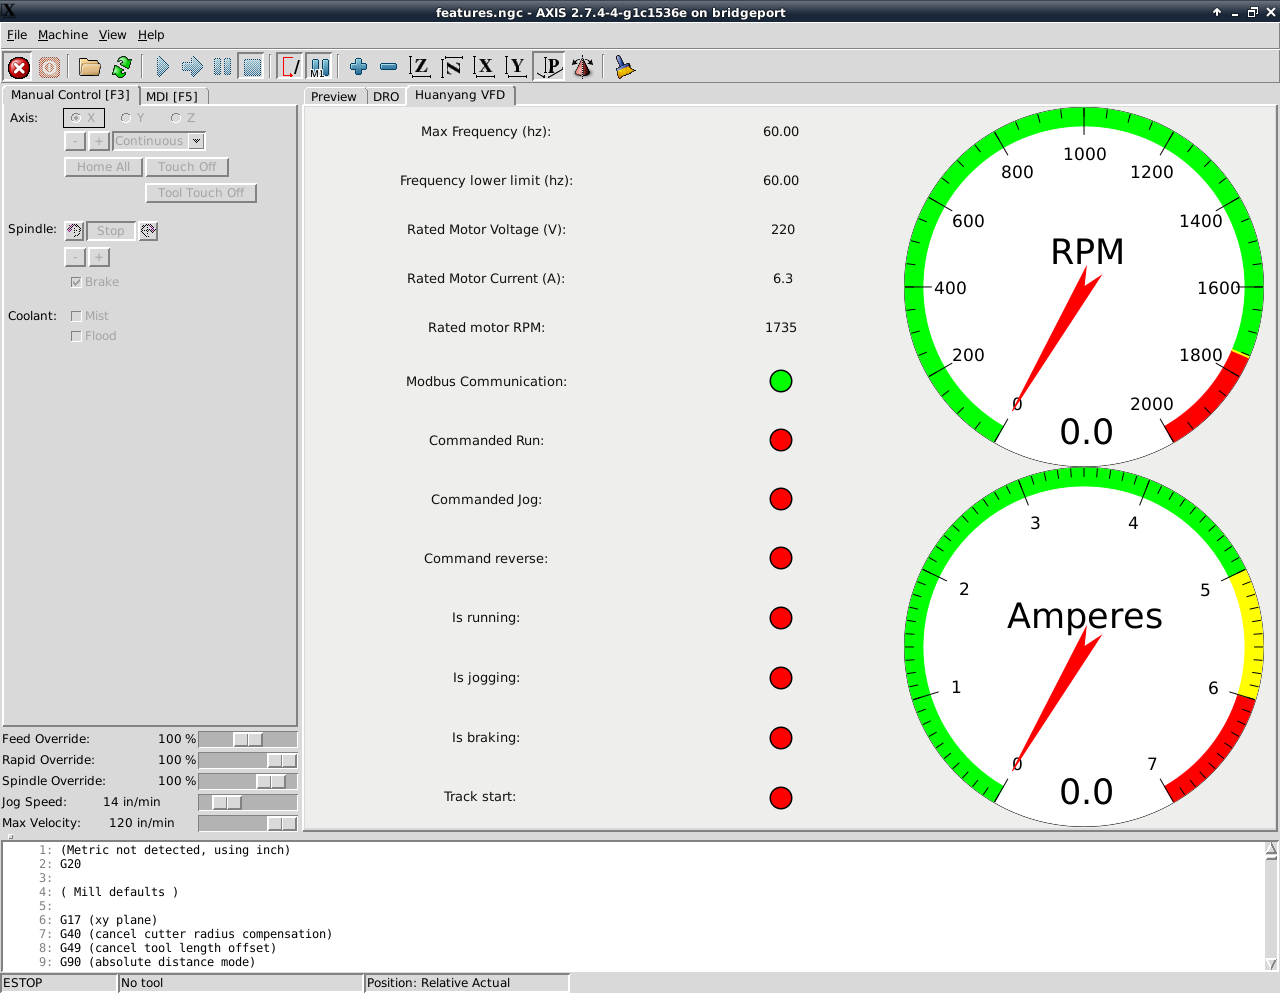
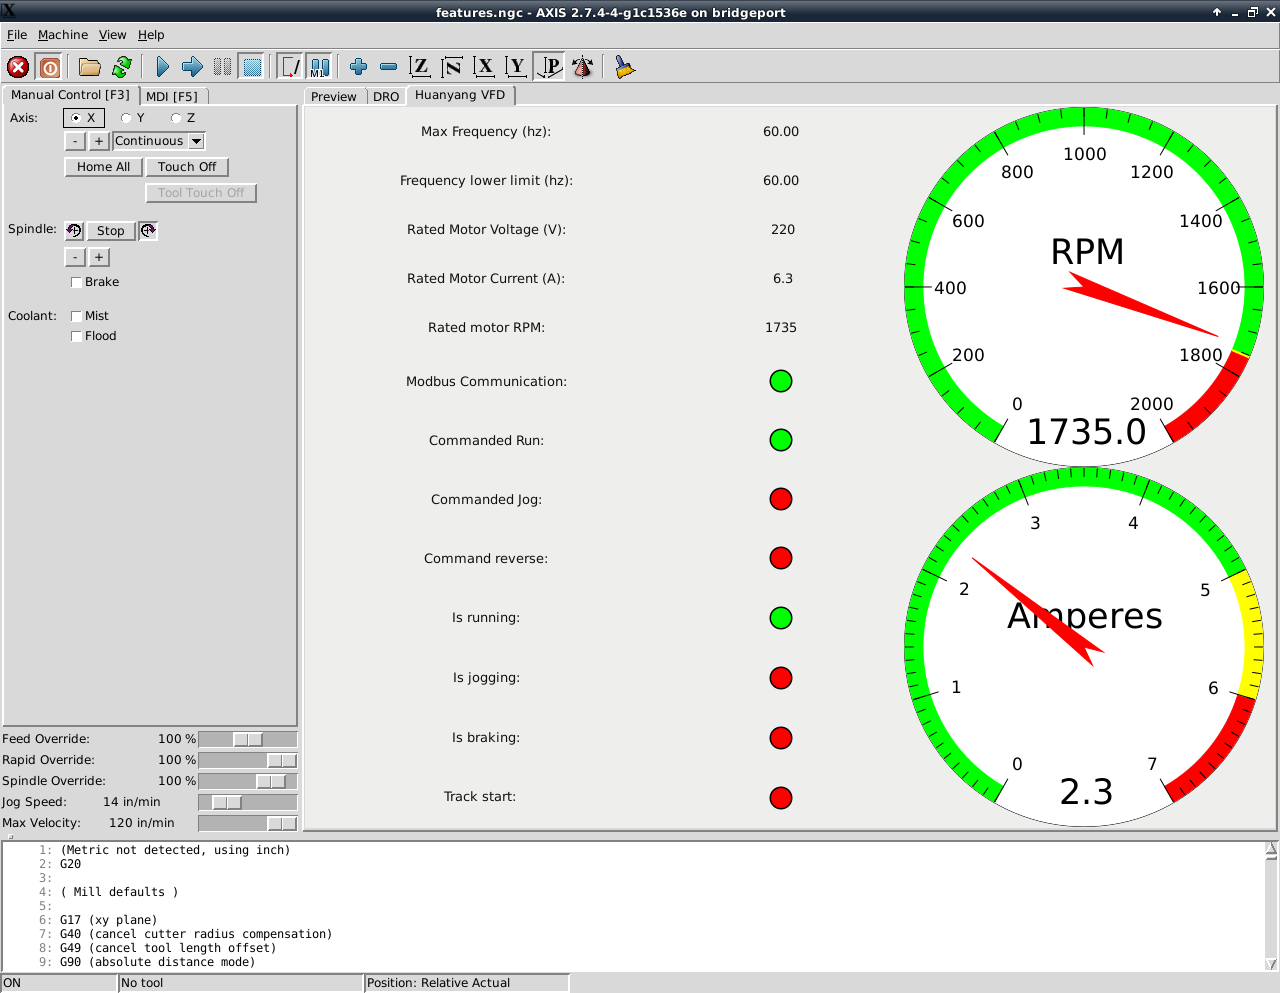
Since I had everything set for the MODBUS hy_VFD I decided to give it another go.

image missing http://i346.photobucket.com/albums/p431/swill008/2015-11/4DAFC32D-01F6-4342-A620-51D8CFDF01A8_zpsrui3dyv7.jpg

I have it working basically as an off/on reverse switch. I may change it down the road. The recent changes pushed to the git for hy_vfd [sept 2015ish] changed pin names and made this somewhat more difficult.

Had to comment out each item that made me crash and comeback to edit the pins.

Good thing I'm hardheaded as my wife would say. After completing it, I was thinking that it was rather easy.

You don't know, what you don't know.

Anyone looking for details on the setup just ask me I'll do my best to explain what I had to go through.
Last edit: 10 years 8 months ago by cncnoob1979.

Please Log in or Create an account to join the conversation.

More
10 years 8 months ago - 10 years 8 months ago #70123 by cncnoob1979
I embedded the VFD into a tab, edited a few things that user "vre" had created. I like it the way it is setup now, im thinking about making the dials into horizontal bars instead.


Now I have a question. Not being a programmer and still very new, I would like to know if it is possible for:

1)Pause any movement/program
2)Linuxcnc to prompt a user with commanded spindle speed [either from g-code or MDI command]
3)Acknowledgement "OK" or Cancel
4)IF OK, then continue with program
5)IF Cancel, stop program

This would allow me to set the spindle speed manually, I am using a variable speed head.

I have read about how to implement variables using user M-Code, but I'm not sure if this would be what I would need?
motion.spindle-inhibit? Perhaps?

Does anyone know where to point me to? I'm not sure what to search to find the information im looking for. Ive tried Google but so far nothing has came up that I think would apply.

How to prompt a user for input to set a variable

Spindle Control with gear change


I have looked at a somethings posted by Andy with the spindle motion out pin, it would seem that I could place something in-between spindle command and every time the spindle is commanded, send that to a user as a prompt.

Given that multiple people have to manually change spindle speeds to accommodate milling/lathe I feel as if this is already implemented and I'm over looking it somewhere. I wouldn't think everyone has an encoder on their spindle :)

Sorry if im not using proper terminology, Im getting there! :woohoo:
Last edit: 10 years 8 months ago by cncnoob1979.

Please Log in or Create an account to join the conversation.

More
10 years 8 months ago #70132 by csbrady
cncnoob,

Forgive me, but I don't see why you would want to do it this way. You can set the speed via the VFD and there is no need to use the manual speed control. The VFD gives you plenty of range and can easily be controlled directly from the controller. You already have the modbus interface working so it should not be difficult to manage the speed. This way you just set the speed in the gcode and your done.

I never touch the manual speed control on my machine. It's much more convenient to manage it from the controller.

Please Log in or Create an account to join the conversation.

Time to create page: 0.821 seconds
Powered by Kunena Forum
