
- Posts: 170
- Thank you received: 13
scurve trajectory planner
- papagno-source
- Offline
- Elite Member
-

Less
More
1 year 7 months ago #324089
by papagno-source
Replied by papagno-source on topic wait to prediction reading gcode
Hi everyone.
I wanted to ask if a stop function for reading gcode blocks has been provided, via an ISO command.
Several CNCs have a stop for reading prediction.
Siemens uses a command called stopre
Rexroth uses a command called wait
etc..
This is important when performing mathematical calculations in the part program and associating values to variables.
In these cases, the prediction must be stopped, the next gcode must be executed line by line, in order to perform the calculations correctly, and then resume the prediction.
If the prediction is not stopped, the calculations could be wrong, because they are performed before updating other previous calculations.
Please Log in or Create an account to join the conversation.
- Aciera
- Offline
- Administrator
-

Less
More
- Posts: 4819
- Thank you received: 2177
1 year 7 months ago - 1 year 7 months ago #324092
by Aciera
Replied by Aciera on topic wait to prediction reading gcode
sounds like a synch or queuebuster command to stop the interpreter read ahead. As an example M66 will do this
There is a sim config that uses a python remap to create a custom Gcode:
github.com/LinuxCNC/linuxcnc/tree/master...remap/stop-lookahead
Code:
M66 E0 L0
There is a sim config that uses a python remap to create a custom Gcode:
github.com/LinuxCNC/linuxcnc/tree/master...remap/stop-lookahead
Last edit: 1 year 7 months ago by Aciera.
Please Log in or Create an account to join the conversation.
- Grotius
- Offline
- Platinum Member
-

Less
More
- Posts: 2419
- Thank you received: 2349
1 year 7 months ago #324150
by Grotius
Replied by Grotius on topic linuxcnc scurve motion planner
Hi all,
* Note, the topic name was changed up to 2 times by someone, haha.
Today i added look ahead. This took almost half a day. It's a tiny file, but took a lot off time.
Here is the look_ahead_source_code_file
Now i did a test run tonight using a line fillet algo : file_path_standard_subseg_line_fillet
This is a simple optimizer algo, that is handy for simple runtests.
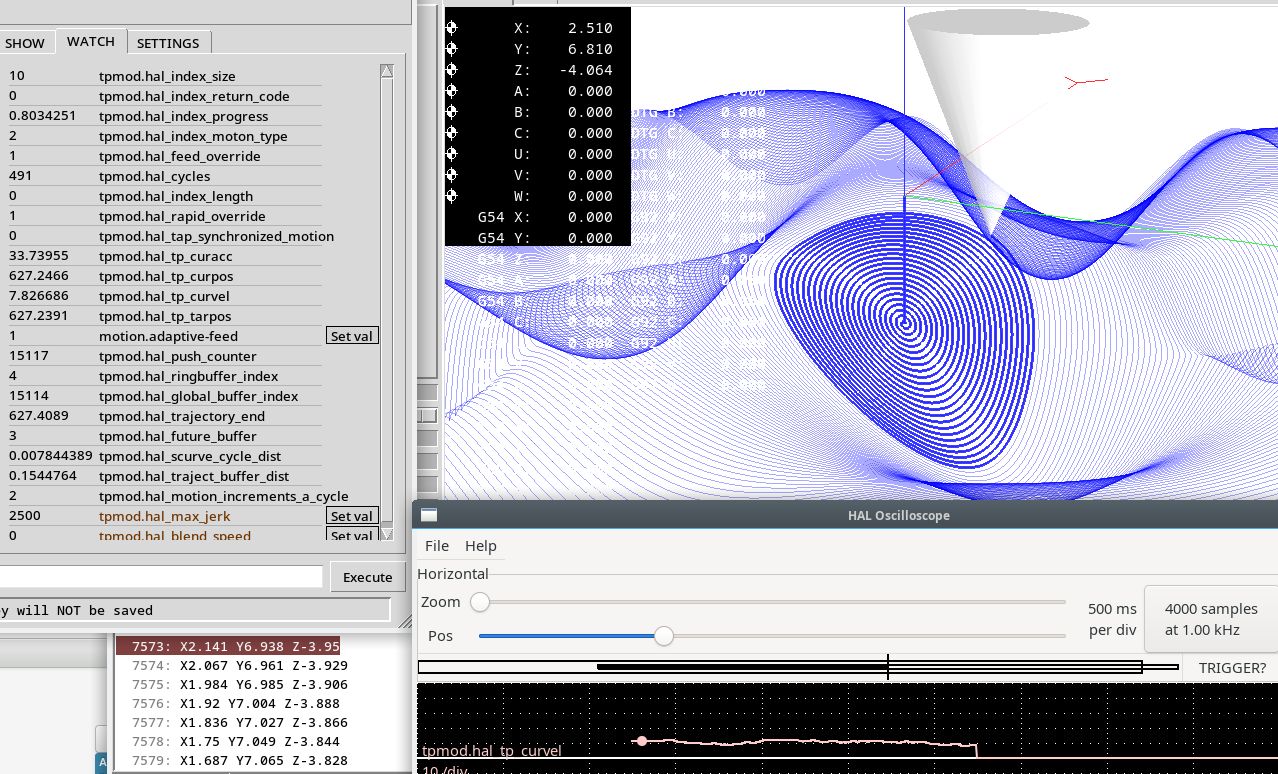
The test is done on the extreme spiral_on_surface file. With tiny segments 0.001mm and deviation P0.0001 Q0.0
Some hal values:
Git sources are updated.
The first donation is recieved. Thanks !
 See the github readme file for more info !
* Note, the topic name was changed up to 2 times by someone, haha.
Today i added look ahead. This took almost half a day. It's a tiny file, but took a lot off time.
Here is the look_ahead_source_code_file
Now i did a test run tonight using a line fillet algo : file_path_standard_subseg_line_fillet
This is a simple optimizer algo, that is handy for simple runtests.
The test is done on the extreme spiral_on_surface file. With tiny segments 0.001mm and deviation P0.0001 Q0.0
Some hal values:
- incements_a_cycle = 2 (planner skips extra gcode segment to keep up with scurve new position)
- ring buffer size = 10
- total loaded segments from program start = 15117
- future buffer, items that are ready to perform, including fillet segments = 3
- cycle dist, is the distance in mm for current servo cycle = 0.0078 mm
- hal traject buffer dist, total todo segments length. ( sum off future buffer ) = 0.1544764 mm
Git sources are updated.
The first donation is recieved. Thanks !
The following user(s) said Thank You: akb1212, tommylight, HalaszAttila, pommen, rodw, Aciera, Darium, anton610, Unlogic
Please Log in or Create an account to join the conversation.
- Grotius
- Offline
- Platinum Member
-
Less
More
- Posts: 2419
- Thank you received: 2349
1 year 7 months ago #324204
by Grotius
Replied by Grotius on topic linuxcnc scurve motion planner
Hi all,
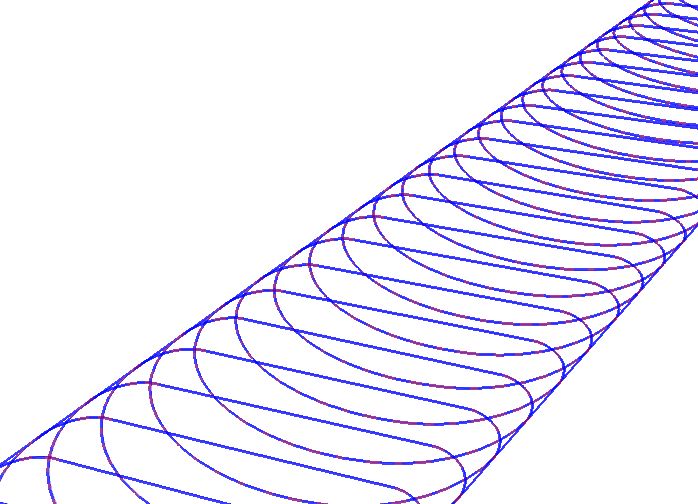
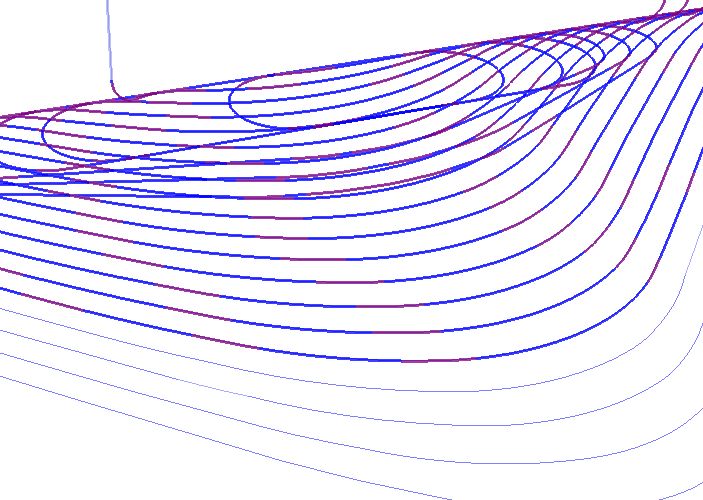
Today i did a test using the clothoid algo.
It turns out, when doing a fast clothoid fit, (using deviation as trim dist) this takes around 0.5ms.
Everything is going well.
When using the excact clothoid fit method, it takes time up to ~200ms when it has difficulties to find a fit.
I will find a solution for this later on.
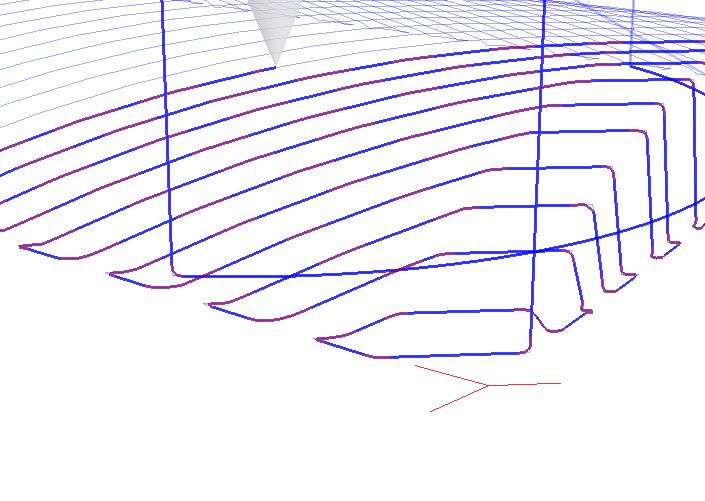
Most off time the clohtoid fits are ok. I have seen cases where the clothoid fit result looks like overfitting.
This could be investegated later on.
Here some 3d clothoid fit examples. Using look ahead = using endvel.
So far i am happy with the results.
Github is updated.
Today i did a test using the clothoid algo.
It turns out, when doing a fast clothoid fit, (using deviation as trim dist) this takes around 0.5ms.
Everything is going well.
When using the excact clothoid fit method, it takes time up to ~200ms when it has difficulties to find a fit.
I will find a solution for this later on.
Most off time the clohtoid fits are ok. I have seen cases where the clothoid fit result looks like overfitting.
This could be investegated later on.
Here some 3d clothoid fit examples. Using look ahead = using endvel.
So far i am happy with the results.
Github is updated.
The following user(s) said Thank You: akb1212, HalaszAttila, rodw, Aciera, Darium, Unlogic, VRNF
Please Log in or Create an account to join the conversation.
- Aciera
- Offline
- Administrator
-
Less
More
- Posts: 4819
- Thank you received: 2177
1 year 7 months ago #324212
by Aciera
What exactly do you mean by 'overfitting'?
Replied by Aciera on topic linuxcnc scurve motion planner
I have seen cases where the clothoid fit result looks like overfitting.
What exactly do you mean by 'overfitting'?
The following user(s) said Thank You: Grotius
Please Log in or Create an account to join the conversation.
- ihavenofish
- Offline
- Platinum Member
-
Less
More
- Posts: 1029
- Thank you received: 286
1 year 7 months ago #324262
by ihavenofish
Replied by ihavenofish on topic linuxcnc scurve motion planner
i assume he means the overshooting on the lower right in the last image.
The following user(s) said Thank You: Grotius, Aciera
Please Log in or Create an account to join the conversation.
Time to create page: 0.276 seconds