Advanced Search

Search Results (Searched for: )

  • paulmag
  • paulmag's Avatar
08 Oct 2026 22:43

Axis interface and "useful" conversational scripts in python

Category: AXIS
I have added a zip file containing subroutines and python scripts I use on Axis I have them listed below some I have made and others I have tweaked to work in Python3 (not all needed doing).

Contained in Python Scripts Folder

    Engrave.py              A script to create a single line of text.

    Ruler.py                A script to generate a ruler with markings.

    Bezel.py                A script to create a rotary scale with or without number markings.

    Contour.py              A script to enable creating toolpaths on a variety of shapes Circle,oval,rectangle,slot,polygon and path with a range of modifiers.

    Face.py                 A script to generate toolpath to cut a defined area.

    Grill.py                A script to generate a set of holes for a grill in a variety of shapes with user definable settings.

    Holecircle.py           Script runs from within linuxcnc to create toolpath to drill holes on a PCD.

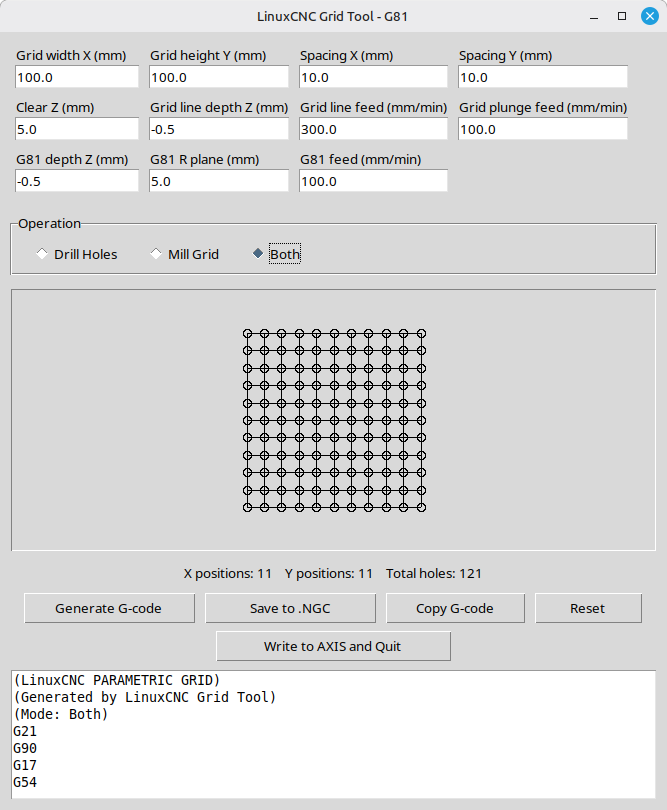
    Grid_G81.py             Script to drill a grid of hole or mill a grid of lines or both useful when creating sacrificial work beds on a router.

    PresetG54.py            Script to create a preset file for G54 offset.

    Pocket.py               Script to create toolpaths to cnc machine round and rectangular pockets.

    pcd_hole_circle.py      Script to generate toolpath to drill holes on a PCD or save as a csv file.
 

Subroutines
Contained in the Subroutines folder

     g54_here.ngc           Sets G54 offset at current position
     
     go_to_home.ngc         returns tool to G54 x and y position after raising Z

     safe_g28.ngc           Sends the tool back to absolute machine home after raising Z

     z_touch.ngc            simple subroutine to set Z height with a touch probe 
  • tommylight
  • tommylight's Avatar
08 Oct 2026 19:49

Usefull Open Source software, vibe coded in Rust

Category: Off Topic and Test Posts

github.com/storytold
Open each project, on the right side click on "releases", then click on the version you want for Linux or Win or...
Several packages for Linux usually, so choose first for aarch if using Raspberry PI, or X86_64 as .deb or as .appimage, where appimage does not install just make it executable in permissions and double click, or use the deb to install with gdebi.
Did not test, just downloaded all as they might disappear since they are all free versions of very expensive software from a very nasty company.
  • kn612
  • kn612
08 Oct 2026 17:47 - 12 Oct 2026 13:10
Replied by kn612 on topic Servo Driver Plasma Retrofit

Servo Driver Plasma Retrofit

Category: Plasmac

Thanks guys, between setting accel to 10in/s2 and dialing in the bias this machine is really smooth now.

Upgraded to debian 13 and master branch.  Thanks for fixing the inmux missing from hal and the cut recovery is working great again.

 
  • jazzkramer
  • jazzkramer
07 Oct 2026 23:05
Replied by jazzkramer on topic Is this a bug?

Is this a bug?

Category: Plasmac

Sorry, I see now there are other posts about this error... I had some lags in the forum and I could not read them... I'm going to read them now.. I apologize for this thread, in case I don't find a solution I will go back here ;)
  • jazzkramer
  • jazzkramer
07 Oct 2026 22:53
Is this a bug? was created by jazzkramer

Is this a bug?

Category: Plasmac

Hi guys, 

I'm using QTPlasma 2.9-237.307 Powerd by QtVCP
since a long time, maybe now, it will became a job... :P :P (Let's see)

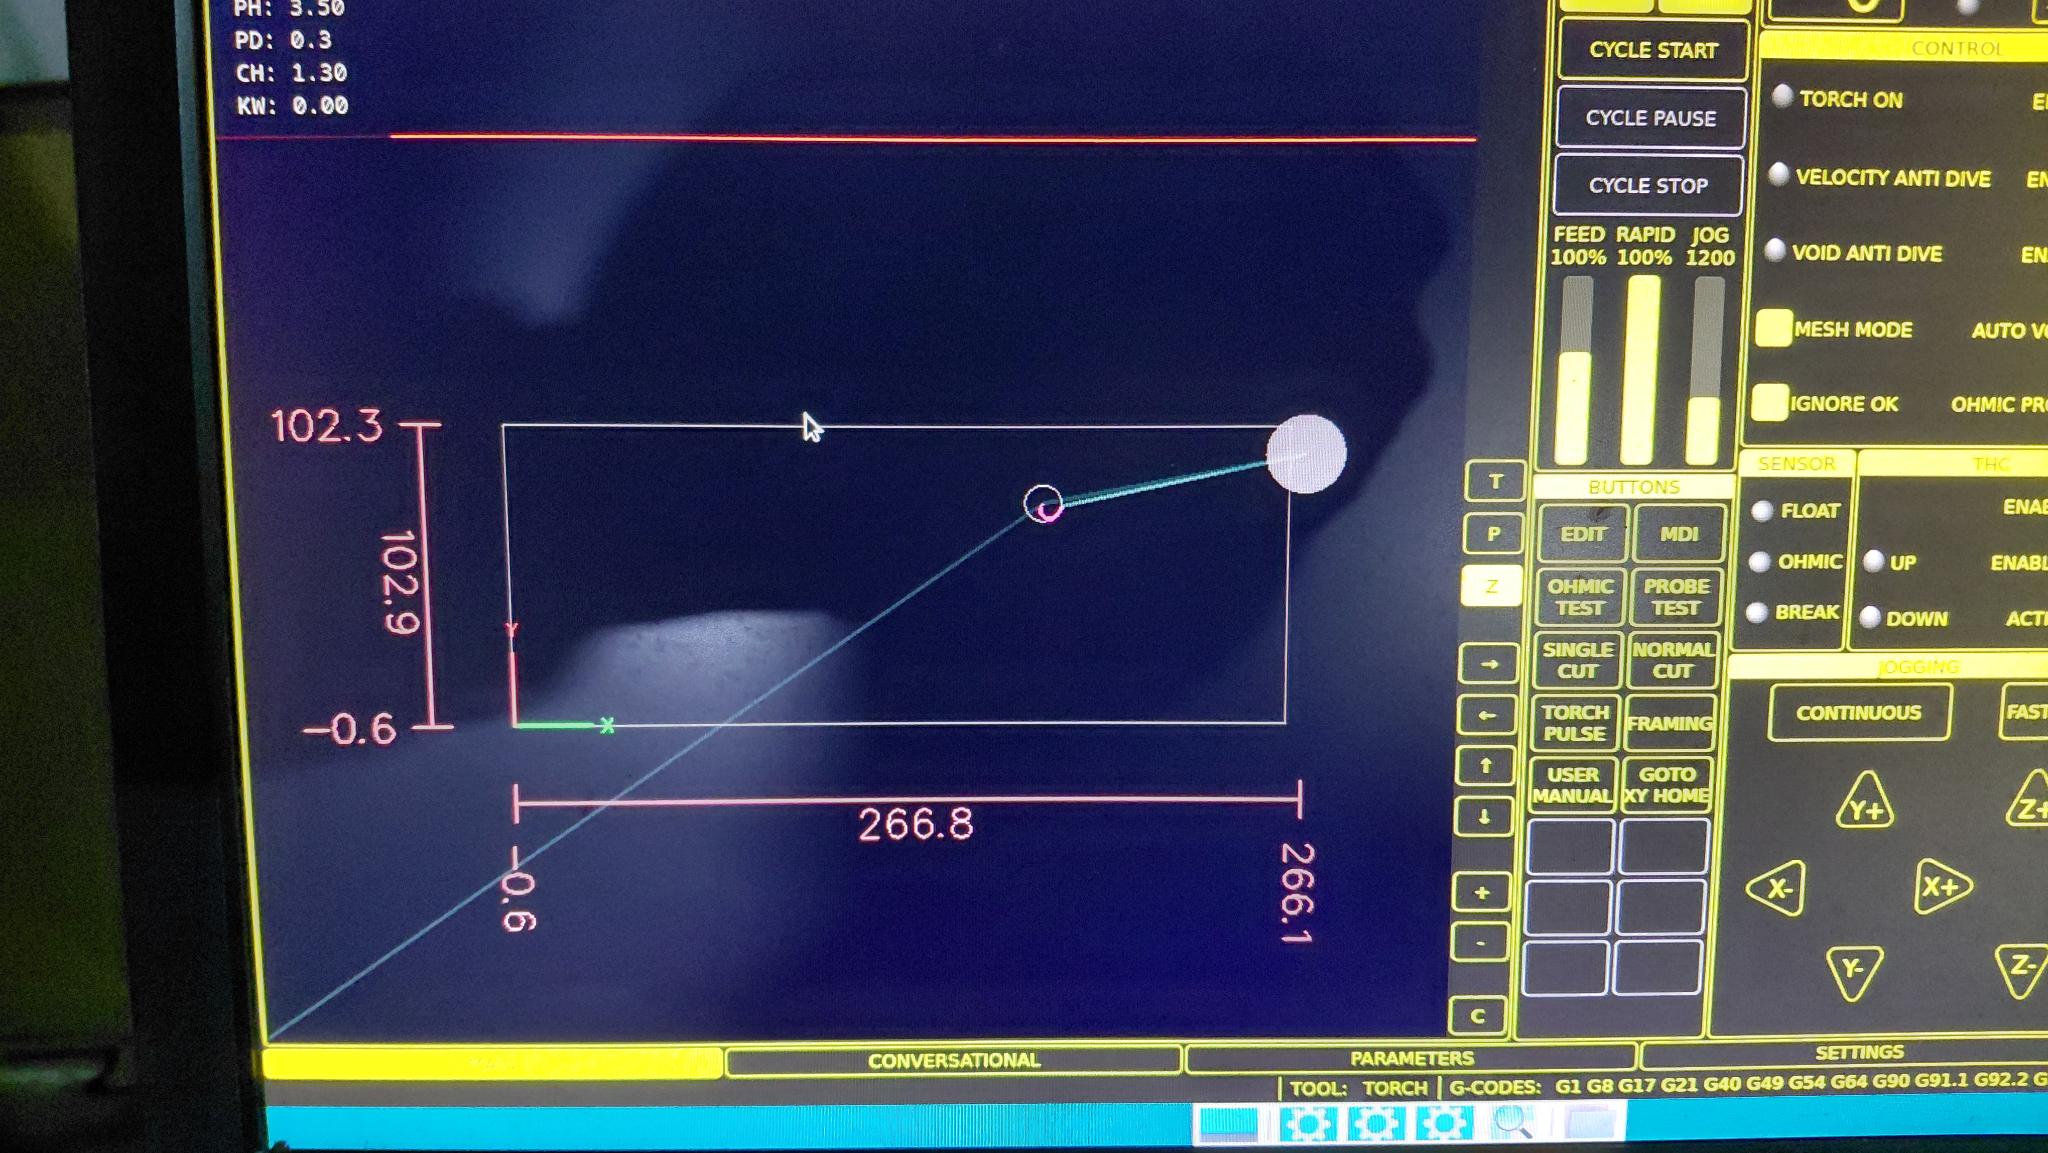
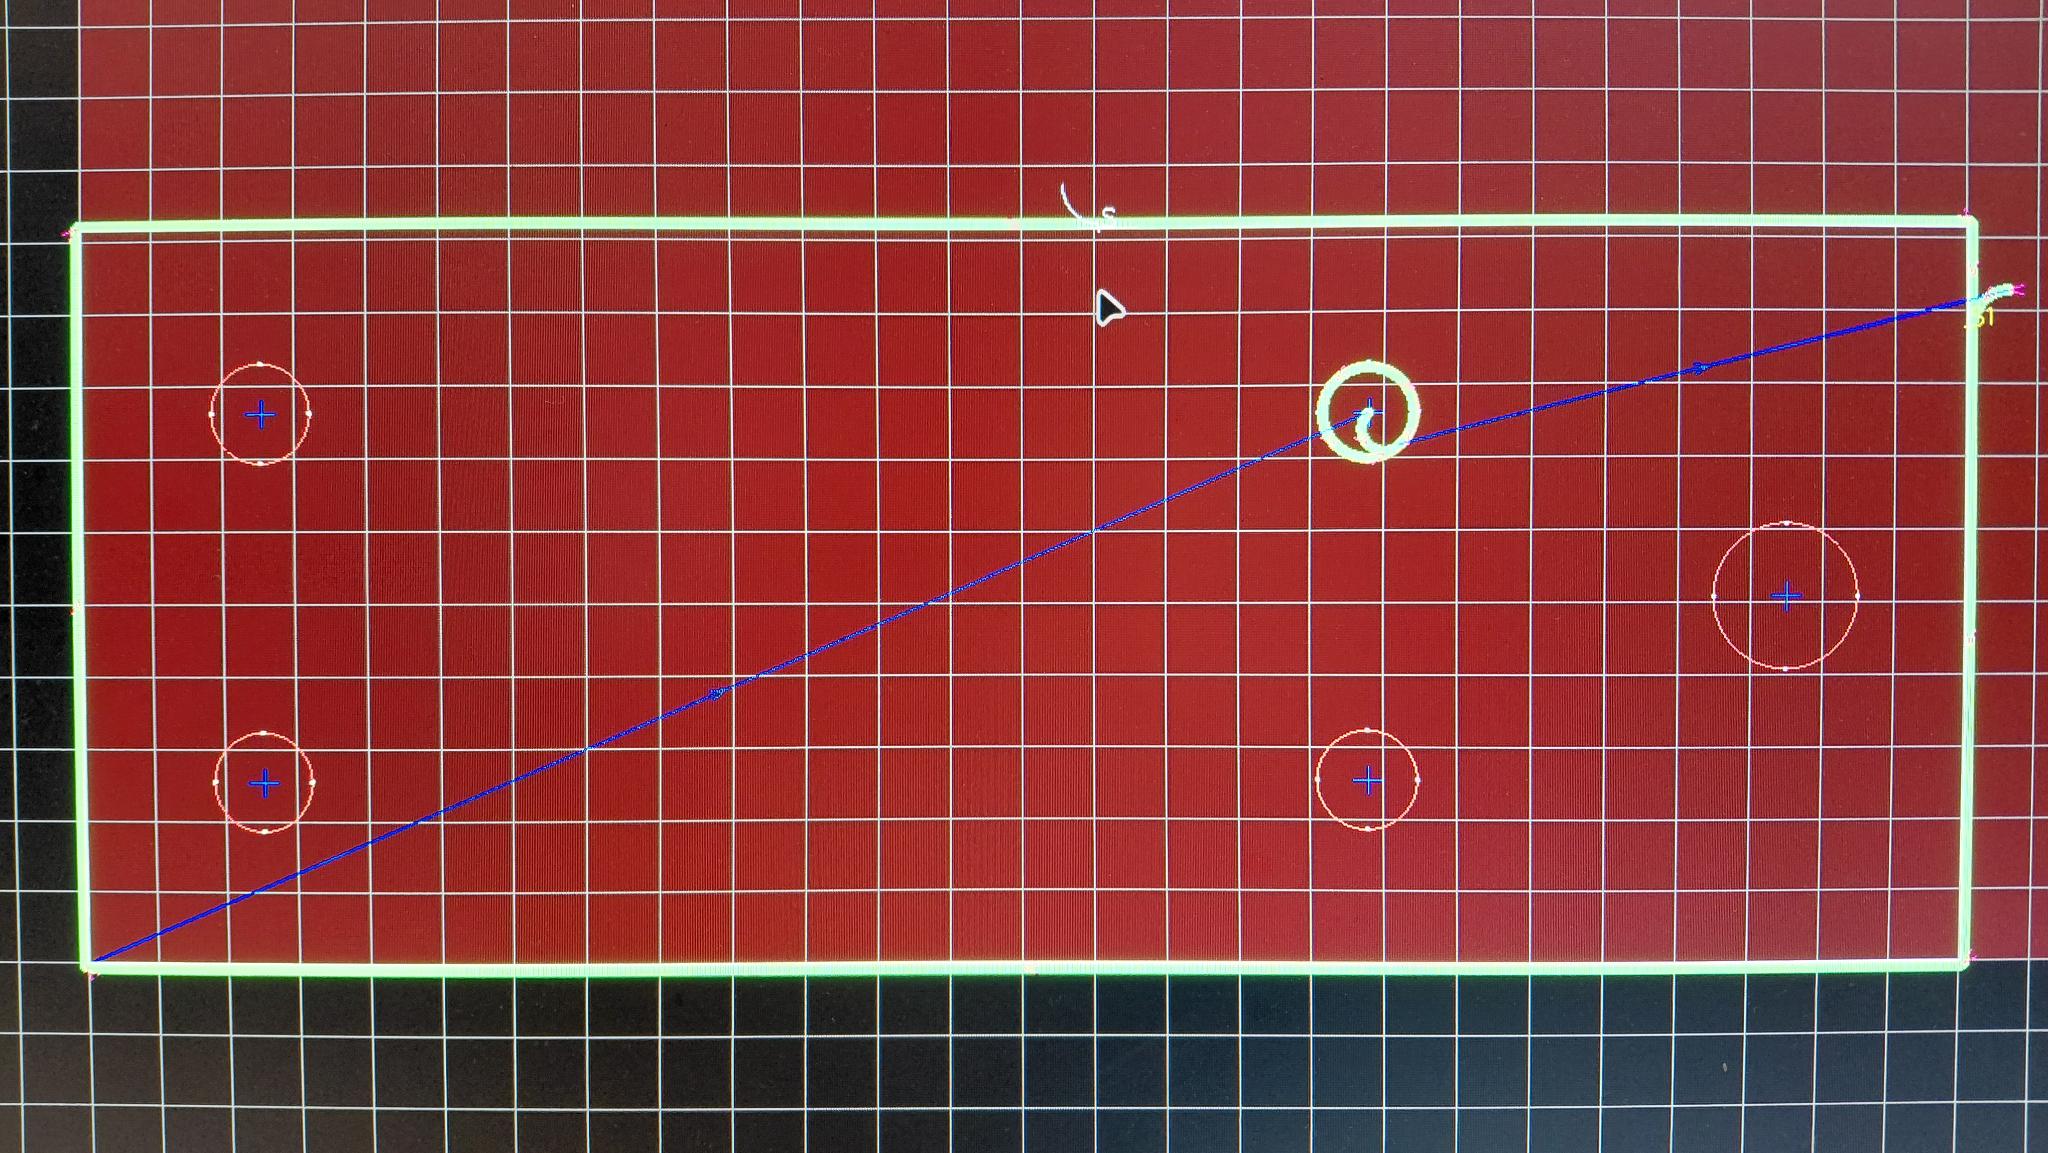
I'm doing some parts to fix the roof of "my shop", a plate with some holes, and PlasmaC does not want to make one hole... It just start the arc inside the hole and when it touch the real circumference it stops and it jumps to the next shape of the plate... others holes are ok. 
Is my code good? It was generated by SheetCam-TNG. I tried to recur (ignore arcok.. mesh.. always the same wrong path)
Any ideas? Thanks! :) :)
In the photo you see one hole only, just to test I modified the file, but it shows the same mistaken path as the complete code here:

;     file name: Piastra piegata per soffitto.ngc
; date and time: Wed Oct 07 2026    11:26:34 AM
; postprocessor: LinuxCNC PlasmaC.scpost rev: 0.5
;
;begin pre-amble
 G21 (units: metric)
 G40 (cutter compensation: off)
 G90 (distance mode: absolute)
 M52 P1 (adaptive feed: on)
 M65 P2 (enable THC)
 M65 P3 (enable torch)
 M68 E3 Q0 (velocity 100%)
 G64 P0.254 Q0.025 (tracking tolerances: 0.254mm)
#<holes>      = 2
#<h_velocity> = 60
#<h_diameter> = 32
#<oclength>   = 4
;end pre-amble
;
;begin material setup
 T0 M6 (select plasma tool)
 G43 H0 (apply tool offsets)
 M190 P20 (plasma, mield steel 1/4" material)
 M66 P3 L3 Q2 (wait for valid change)
 F#<_hal[plasmac.cut-feed-rate]>
;end material setup
 G0 X177.8 Y76.2
 M3 $0 S1 (plasma start)  ****THIS FIRST HOLE IS NOT WORKING
 M67 E3 Q100
 G3 X182.184 Y71.816 I2.192 J-2.192
 G3 X182.184 Y71.816 I-4.384 J4.384
 M5 $0 (plasma end)
 G0 X177.8 Y25.4
 M3 $0 S1 (plasma start)
 G3 X182.184 Y21.016 I2.192 J-2.192
 G3 X182.184 Y21.016 I-4.384 J4.384
 M5 $0 (plasma end)
 G0 X234.338 Y44.171
 M3 $0 S1 (plasma start)
 G3 X241.579 Y44.171 I3.62 J3.62
 G3 X241.579 Y44.171 I-6.629 J6.629
 M5 $0 (plasma end)
 G0 X25.4 Y25.4
 M3 $0 S1 (plasma start)
 G3 X21.016 Y29.784 I-2.192 J2.192
 G3 X21.016 Y29.784 I4.384 J-4.384
 M5 $0 (plasma end)
 G0 X25.4 Y76.2
 M3 $0 S1 (plasma start)
 G3 X21.016 Y80.584 I-2.192 J2.192
 G3 X21.016 Y80.584 I4.384 J-4.384
 M5 $0 (plasma end)
 G0 X266.12 Y53.358
 M3 $0 S1 (plasma start)
 G3 X261 Y48.238 I0 J-5.12
 G1 X261 Y0
 G2 X260.35 Y-0.65 I-0.65 J0
 G1 X0 Y-0.65
 G2 X-0.65 Y0 I0 J0.65
 G1 X-0.65 Y101.6
 G2 X0 Y102.25 I0.65 J0
 G1 X260.35 Y102.25
 G2 X261 Y101.6 I0 J-0.65
 G1 X261 Y48.238
 M5 $0 (plasma end)
 ;
 ;begin post-amble
 G40 (cutter compensation: off)
 G90 (distance mode: absolute)
 M65 P2 (enable THC)
 M65 P3 (enable torch)
 M68 E3 Q0 (velocity 100%)
 M5 $-1 (backup stop)
 ;end post-amble
 ;
 ;begin statistics
 ;Pierces = 6
 ;   Cuts = 6,    Length = 997.75mm
 ;end statistics
 ;
 M30 (end program)

Any ideas?

 
  • tommylight
  • tommylight's Avatar
07 Oct 2026 20:18

Turn G-code: conversational lathe cycle generator for LinuxCNC (12 cycles)

Category: Show Your Stuff
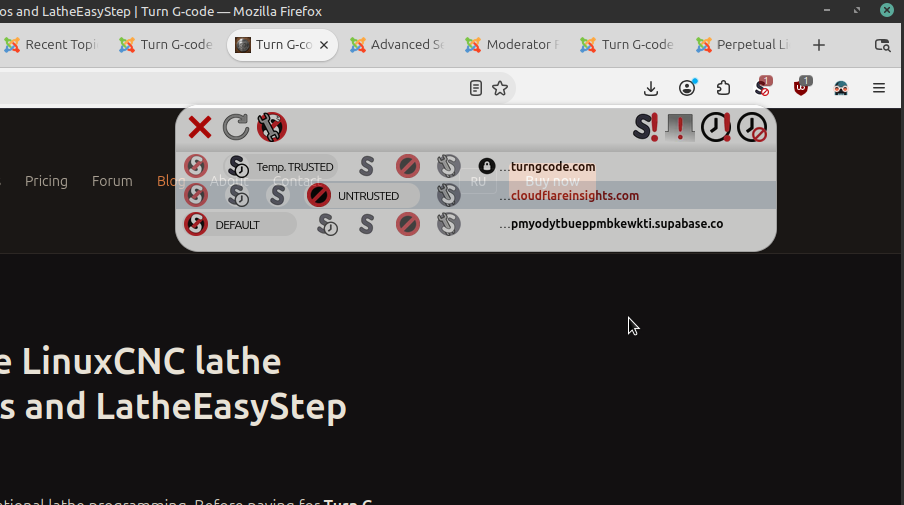
Not CloudFlare, the one bellow with "supabase" domain name.
-
CloudFlare is very good at what they do, and they do a lot, but the main thing is they figured out how to protect websites from DDOS attacks, and beat AKAMAI in their caching game.
  • Odessit
  • Odessit
07 Oct 2026 19:05

Turn G-code: conversational lathe cycle generator for LinuxCNC (12 cycles)

Category: Show Your Stuff

Thanks Tom, and sorry for misreading you on the wiki.
▎ About the script: that's Cloudflare Web Analytics (static.cloudflareinsights.com), the visit counter of Cloudflare, which hosts the site. No cookies, no tracking across sites, just page view counts so I can see which pages people actually read. NoScript flags it, and the site works fine without it, so blocking it is totally OK.
▎ If anyone still has edit access to the wiki CAM page, I'd be glad to have a line for Turn G-code there (commercial, 15-day trial), next to SheetCAM and the others.
  • paulmag
  • paulmag's Avatar
06 Oct 2026 23:51 - 06 Oct 2026 23:55

Axis interface and "useful" conversational scripts in python

Category: AXIS

OK (hope this works)

First Python3 script "linuxcnc_grid_tool_G81_axis.py" this can be run eother from within axis and loads toolpath directly into axis or from desktop using python on Geady or terminal and save to .NGC file.

The script I use to engrave a grid on my sacrificial MDF machine bed and drill fixing holes at grid intersections

I have 12 scripts in total available to upload and also 5 subroutines i can upload them individually or as a zip.


  • tuxcnc
  • tuxcnc
06 Oct 2026 21:43
Replied by tuxcnc on topic Re-designing the Gmoccapy DRO

Re-designing the Gmoccapy DRO

Category: Gmoccapy

Yeah that's also a possibility, but the duplicated "G54" consumes too much space IMHO.
 

There is no way to avoid this.
If we assume that G54 needs to be displayed somewhere, then we might as well display it several times and we need to have room for G59.3 (two more characters).
What I pasted above was painted in Inkscape, in Gmoccapy there will be a different font, so it will look a little different.
I adopted the rule that everything that may be needed must be displayed, but the position in the current coordinate system should be displayed as large as possible and cannot be confused with anything else (hence the different colors).
Of course, someone may have a better idea, but this issue should not be considered in terms of what is beautiful and what is not for whom, it should only be useful and safe.
  • tommylight
  • tommylight's Avatar
06 Oct 2026 21:07

Turn G-code: conversational lathe cycle generator for LinuxCNC (12 cycles)

Category: Show Your Stuff

Thanks Tom, fair points. Understood about the wiki - open source only, I'll leave it.

I did not say that, at least id did not want to say that, i meant i am sure about SheetCAM, but not about the rest, so if the rest have trial versions, it should also be possible to add yours, and i mentioned where the password should be, but last i checked the wiki was 15 years ago.
-
First, thank you for making me feel a lot better about this, i checked your website, and the first thing you mention is the fact that LinuxCNC has such tools. Thank you for the respect.
Also checked the comparison, but i can not decide anything as i have very little experience with a CNC lathe, so i will leave that to others to decide for themselves.
-
As for the website, see the attached picture, it is trying to run a script that points to a fuzzy website, see above the mouse.
This should be easy to remove, just check your HTML/CSS/JS files for that web name and remove it.
It also may be functional, but since everything works fine without it, you might as well remove it.

Again, thank you for being fair and respectful, very much appreciated.
  • HansU
  • HansU's Avatar
06 Oct 2026 19:37
Replied by HansU on topic Re-designing the Gmoccapy DRO

Re-designing the Gmoccapy DRO

Category: Gmoccapy
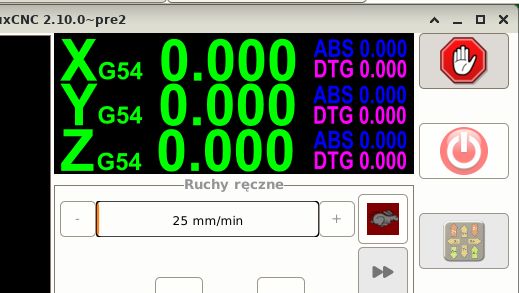


Yeah that's also a possibility, but the duplicated "G54" consumes too much space IMHO.
  • HansU
  • HansU's Avatar
06 Oct 2026 19:36
Replied by HansU on topic Re-designing the Gmoccapy DRO

Re-designing the Gmoccapy DRO

Category: Gmoccapy

Not sure why A and B needs the smaller text size, but looks ok.


Just keeping the current arrangement:
linuxcnc.org/docs/devel/html/image/gui/i.../gmoccapy_5_axis.png

You are removing information though, the Abs might deserve a switch, maybe on click/tap? maybe with some kind of hint, clicking on dtg changes it to abs?


Yeah that's what I meant with "toggle the display of the right part." So don't rotate the displayed values, only switch between Abs and DTG in the right part.
  • Odessit
  • Odessit
06 Oct 2026 19:31

Turn G-code: conversational lathe cycle generator for LinuxCNC (12 cycles)

Category: Show Your Stuff

Thanks Tom, fair points. Understood about the wiki - open source only, I'll leave it.

Good idea about the comparison chart, here it is:
turngcode.com/en/blog/turn-gcode-vs-free-linuxcnc-lathe-tools/

To be honest about the overlap: the basics (turning, facing, boring, chamfer/radius, simple threading) are covered by the free Lathe Macros and LatheEasyStep too, and LatheEasyStep does free contours and keyway slotting, which Turn G-code doesn't. Where Turn G-code is different: multi-start threads, tapered threads over the full length (G76 only tapers the entry/exit), set run-in/run-out, concave sphere and the face spiral, it runs standalone on Linux or Windows without touching the config, and has output options for controls without G76.

If anything in the table about the free tools is wrong, please correct me and I'll fix it.
  • tommylight
  • tommylight's Avatar
06 Oct 2026 18:48

Turn G-code: conversational lathe cycle generator for LinuxCNC (12 cycles)

Category: Show Your Stuff

I do not know the Wiki password, and the PM is disabled on this forum ( i think). That info should be in the Wiki, see if you can find something like "how to edit pages" or similar.
SheetCam is not a trial version, it is a limited output version (at least it was), no idea about the others but i tend to think they also have usable limited versions, not trials.
Either way, Open Source project so only open source stuff should be here, and that puts us in a bind as there is often talk about Fusion360 and other payed stuff.
-
We do have several versions of lathe conversational and macros, all free and open source and included with LinuxCNC, but i have limited experience with them, so i would really appreciate if someone else can share what is different or what is better in your software.
BTW, if it turns out we already had everything your software can do, i will really be disappointed, as i allowed this based on you being a member here for quite some time, and hoping you already checked before putting me in a very bad position.
So here is an idea, make a comparison chart between the included stuff and your software, that helps a lot in winning customers.
  • angelnu
  • angelnu
06 Oct 2026 18:44
Replied by angelnu on topic mesa 7i97T + 7i84U

mesa 7i97T + 7i84U

Category: Driver Boards

Sorry, I meant 4.7K

Ok I will buy it at eusurplus on their website they have it in stock, I live in Spain.
Thank you very much for your answers
Displaying 406 - 420 out of 11518 results.
Time to create page: 1.883 seconds
Powered by Kunena Forum