
- Posts: 22011
- Thank you received: 7491
Another plasma component...
- tommylight
- Offline
- Moderator
-

Less
More
7 years 4 months ago #137149
by tommylight
Regards,
Tom
P.S.
Just did a short video about Mesa 7i92 and an Acer laptop that works perfectly with Linuxcnc even when wired through a network switch, uploading it to YouTube and starting a new thread for more info.
Replied by tommylight on topic Another plasma component...
Hmmmmm not exactly, I said in general I am wary of not typing my info on web sites, the usual network admin paranoia. In your case I literally saw your personal phone number and thought " oh good I'll call him tomorrow! "rodw wrote:
Well its been an eventful night! I was blessed by a phone call from Tommy which was nice. He was a bit worried about security if he contacted me via my web site but rest assured we use a leading, highly secure cloud hosted ecommerce provider called neto which is 51% owned by Telstra, our monopolistic telecommunications giant here in Australia. If they have any security gaps, the whole country will be in trouble!
Regards,
Tom
P.S.
Just did a short video about Mesa 7i92 and an Acer laptop that works perfectly with Linuxcnc even when wired through a network switch, uploading it to YouTube and starting a new thread for more info.
Please Log in or Create an account to join the conversation.
- Grotius
- Offline
- Platinum Member
-

Less
More
- Posts: 2419
- Thank you received: 2349
7 years 4 months ago #137154
by Grotius
Replied by Grotius on topic Another plasma component...
@Phill,
You can post your code over here. G90 is good.
I and J offset's are the core members to be calculated when using snippet's for circles and arc's in all 4 quadrant's.
If it's G90.1 or G91.1 does not matter for me at this moment.
I have not looked so far myself to load in g-code line's into the real time memory and do some calculation's with it relating to code snippet's. But it's overall a interesting item. The probe over distance has also become a very succesful item. So why not adapt some code snippets.
The only worry i have is to keep it a real time interacting solution (component solution)
I don't like pre defined g-code solution's like multiple g-code lines for a simple probing sequence etc.
Then user cannot change it real time in the field at the machine.
Please Log in or Create an account to join the conversation.
- phillc54
- Offline
- Platinum Member
-
Less
More
- Posts: 5711
- Thank you received: 2100
7 years 4 months ago - 7 years 4 months ago #137448
by phillc54
Replied by phillc54 on topic Another plasma component...
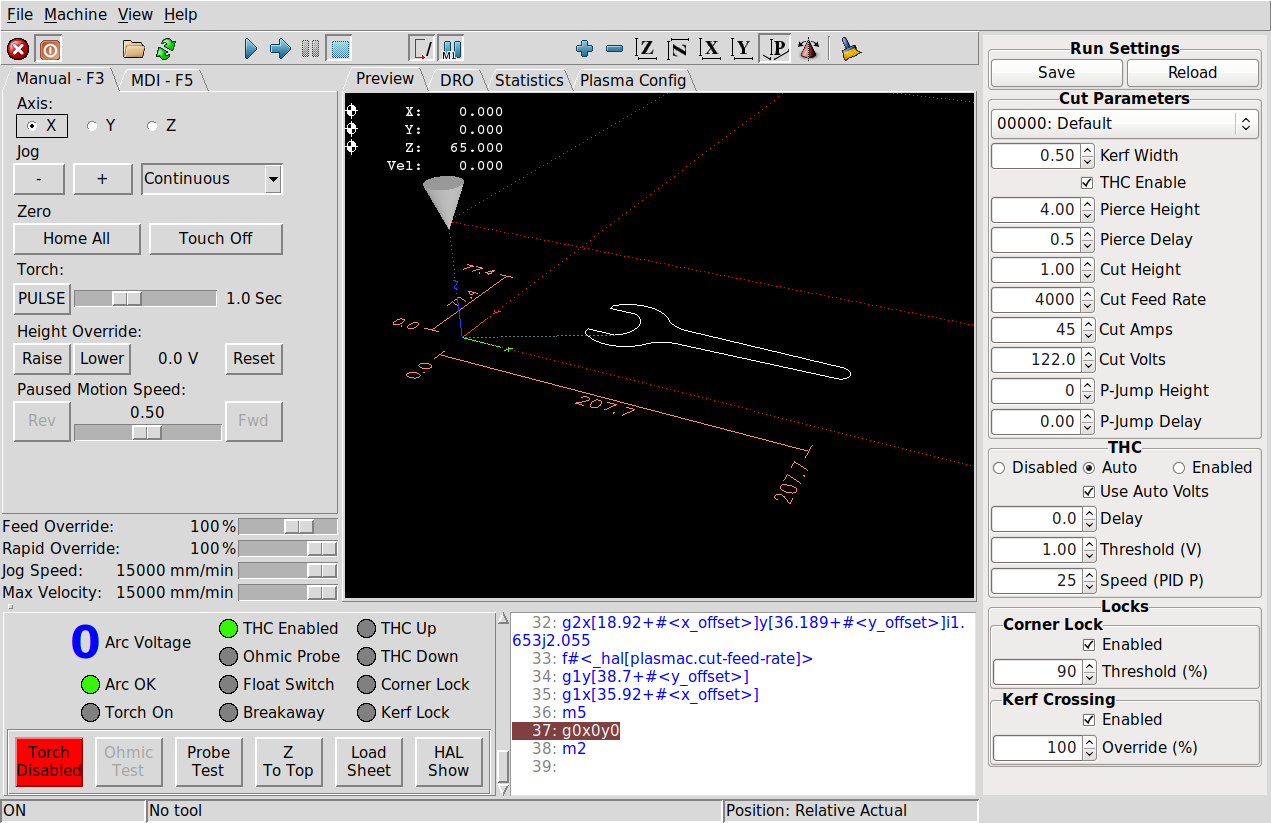
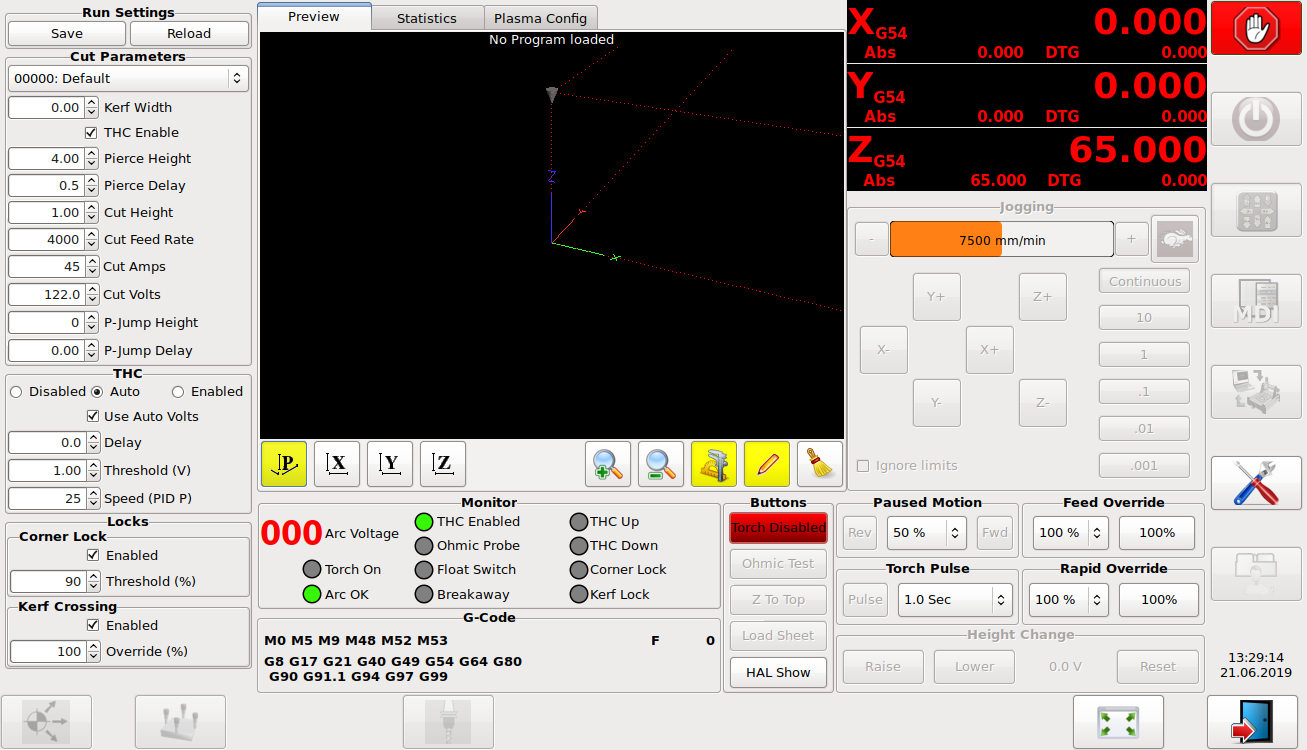
For all you folk with widescreen monitors I have made a Run Panel that shows at the side of the GUI rather than as a tab.
To use this do an upgrade then edit your ini file.
For Axis, the panel sits at the right hand side and at the moment you will get a permanent error in the terminal saying it is waiting for a component to be ready. This doesn't appear to affect the machine operation and there is a pull request in the LinuxCNC repo for a fix.
Comment out the two EMBED lines an uncomment the GLADEVCP line.
For Gmoccapy the panel sits at the left hand side.
Comment out the first three EMBED lines and uncomment the next three EMBED lines.
Axis:
Gmoccapy:
Cheers, Phill.
To use this do an upgrade then edit your ini file.
For Axis, the panel sits at the right hand side and at the moment you will get a permanent error in the terminal saying it is waiting for a component to be ready. This doesn't appear to affect the machine operation and there is a pull request in the LinuxCNC repo for a fix.
Comment out the two EMBED lines an uncomment the GLADEVCP line.
Code:
# run panel in tab behind preview
EMBED_TAB_NAME = Plasma Run
EMBED_TAB_COMMAND = gladevcp -c plasmac_run -x {XID} -u ./plasmac_run.py -H plasmac_run.hal plasmac_run_tab.glade
# run panel in panel on right side
#GLADEVCP = -c plasmac_run -u ./plasmac_run.py -H plasmac_run.hal plasmac_run_panel.glade
For Gmoccapy the panel sits at the left hand side.
Comment out the first three EMBED lines and uncomment the next three EMBED lines.
Code:
# run panel in tab behind preview
EMBED_TAB_NAME = Plasma Run
EMBED_TAB_LOCATION = ntb_preview
EMBED_TAB_COMMAND = gladevcp -c plasmac_run -x {XID} -u ./plasmac_run.py -H plasmac_run.hal plasmac_run_tab.glade
# run panel in panel on left side
#EMBED_TAB_NAME = Plasma Run
#EMBED_TAB_LOCATION = box_left
#EMBED_TAB_COMMAND = gladevcp -c plasmac_run -x {XID} -u ./plasmac_run.py -H plasmac_run.hal plasmac_run_panel.glade
Axis:
Warning: Spoiler!
Gmoccapy:
Warning: Spoiler!
Cheers, Phill.
Last edit: 7 years 4 months ago by phillc54.
Please Log in or Create an account to join the conversation.
- rodw
- Offline
- Platinum Member
-
Less
More
- Posts: 12170
- Thank you received: 4153
7 years 4 months ago #137462
by rodw
Replied by rodw on topic Another plasma component...
Well it just so happens I did a bit more work on my machine while Phill was doing this upgrade.
Just a heads up you may need to manually copy the new display settings into your ini file. I was getting gcode errors becasue I did not have a feed rate because the whole plasma run tab was missing! The new Gmoccappy wide screen works well.
The other issue I had was that the new HAL connections to allow adaptive feed and disableTHC features.
Anyway, the good news is once I had pins that actually got the adaptive feed working, I sorted out some code snippets and cutting rules for holes for Sheetcam and it all works nicely.
Please Log in or Create an account to join the conversation.
- thefabricator03
- Visitor
-

7 years 4 months ago #137464
by thefabricator03
Rod,
Do you mind sharing your sheetcam post for Plasmac that has the new disable function.
Replied by thefabricator03 on topic Another plasma component...
rodw wrote: Anyway, the good news is once I had pins that actually got the adaptive feed working, I sorted out some code snippets and cutting rules for holes for Sheetcam and it all works nicely.
Rod,
Do you mind sharing your sheetcam post for Plasmac that has the new disable function.
Please Log in or Create an account to join the conversation.
- rodw
- Offline
- Platinum Member
-
Less
More
- Posts: 12170
- Thank you received: 4153
7 years 4 months ago - 7 years 4 months ago #137469
by rodw
Yes, I will when I'm back at work. I did not change much today, the magic is in the cutting rules., not the post processor.
Replied by rodw on topic Another plasma component...
thefabricator03 wrote:
rodw wrote: Anyway, the good news is once I had pins that actually got the adaptive feed working, I sorted out some code snippets and cutting rules for holes for Sheetcam and it all works nicely.
Rod,
Do you mind sharing your sheetcam post for Plasmac that has the new disable function.
Yes, I will when I'm back at work. I did not change much today, the magic is in the cutting rules., not the post processor.
Last edit: 7 years 4 months ago by rodw.
Please Log in or Create an account to join the conversation.
Moderators: snowgoer540
Time to create page: 0.447 seconds