
- Posts: 12170
- Thank you received: 4153
Another plasma component...
- rodw
- Offline
- Platinum Member
-

Less
More
7 years 3 months ago #140885
by rodw
Phill, if you come back to this, could you make sure there is something that can disable this parsing? Somehow, it does not feel right to build features that modify the Gcode as a user might not want to enable this type of behaviour.
Replied by rodw on topic Another plasma component...
phillc54 wrote: I have deferred work on the arc addition to the GCode parser for a while as there are problems if any words use named or numbered parameters or expressions. I will possibly release one that will just report an error if it cannot work it out but to do it 'properly' is a major job.
Phill, if you come back to this, could you make sure there is something that can disable this parsing? Somehow, it does not feel right to build features that modify the Gcode as a user might not want to enable this type of behaviour.
The following user(s) said Thank You: tommylight
Please Log in or Create an account to join the conversation.
- robertspark
- Offline
- Platinum Member
-
Less
More
- Posts: 915
- Thank you received: 216
7 years 3 months ago #140902
by robertspark
Replied by robertspark on topic Another plasma component...
what do you want to do the to / with the gcode?
what would plasmac be looking for?
or wanting to do?
what would plasmac be looking for?
or wanting to do?
Please Log in or Create an account to join the conversation.
- JTknives
- Offline
- Elite Member
-

Less
More
- Posts: 243
- Thank you received: 32
7 years 3 months ago #140905
by JTknives
Replied by JTknives on topic Another plasma component...
So I don’t know if this belongs here or in a new post. If it needs to be moved let me know and I will delete it and start a thread.
Im not a Linux programming genius, hell I could barely manage getting it installed. I don’t know if what I’m wanting can be added to the plasmaC or would need to be its own thing. The steel I cut is all high dollar stuff. Yesterday I cut up a 11”x23” sheet of stainless that cost me $100. So a mess up can be really costly and go down hill fast. Now I can’t cut it real fast as I’m running a 30xp and sitting at around 20”/min. I’m using sheetcam to nest and save it as a number attached to that sheet so I can load it back up and add more parts later and know what’s already been cut out. My issue is finding the exact starting corner. I have been using a square to get it square to the table and then bringing the torch down and moving over till I just barely touch the edge. Then set this as -.375 in g54 for x and y. This gives my just enough to clear the edge of the sheet. I do this because I set the edge of the parts at the edge of the sheet in sheet cam. This has eliminated the fudge factor guessing for me.
Yesterday I was wondering why could I not have a touch off button. The torch has ohmic so it could use that. Back when I ran cnc machines the new hass mills would load up a touch off tool. You would manually eyeball it over the corner and hit the touch off button. It would come down in the Z and find the top. Then move over in the X any Y a programmed amount and then come down a set amount and move over till it touches the side. It would set that as X and then retract and do the same for Y. It would then enter these numbers into the G54 offset.
If I could somehow build this function into my machine I would be tickled pink. We won’t bring up the other feature that would put it over the top. Well why not just mention it at least. Another machine I ran would touch off in 2 places on an edge and rotate the axis in the machine so the x and y would like up parallel to the sheet/part.
Please Log in or Create an account to join the conversation.
- docwelch
- Offline
- Senior Member
-

Less
More
- Posts: 58
- Thank you received: 25
7 years 3 months ago #140913
by docwelch
Replied by docwelch on topic Another plasma component...
Robert,
I have been working on a post-processor for Fusion360 to use with plasmac and asked about making some changes in the g-code parser to handle the speed change when cutting circles as well as adjusting the kerf width due to cutting slower, and even extending the cut past the end of the circle with the torch off. Phill decided this was probably still better handled in the post-processor. There are a number of things that make this difficult to do from a "finished" g-code file as compared to doing it in a post-processor. And, it appears he has found a new issue we would have to overcome with the current g-code parser to implement it as well.
Steven
Please Log in or Create an account to join the conversation.
- rodw
- Offline
- Platinum Member
-
Less
More
- Posts: 12170
- Thank you received: 4153
7 years 3 months ago #140921
by rodw
Something like this?
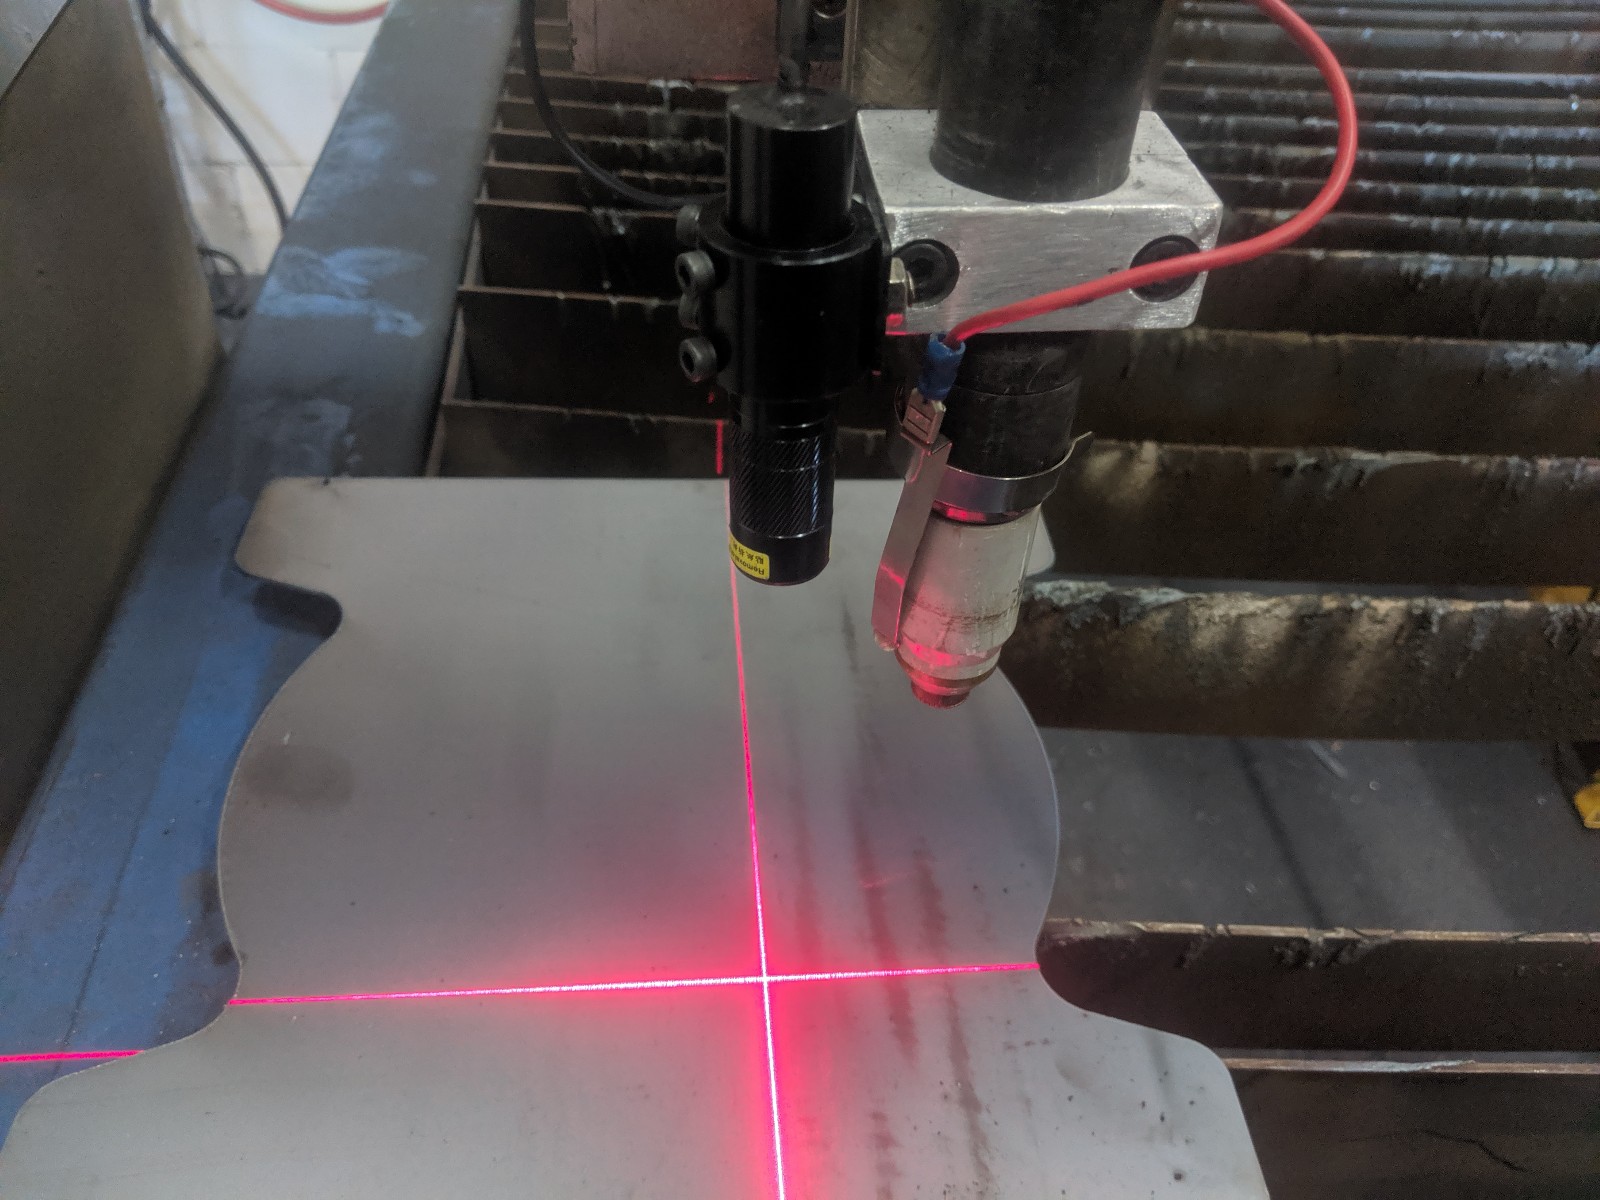
I just progrrammed a gcode macro in Gmoccappy to move to the offset and touch off X & Y
All I did was fire the torch to create a spot at position 0,0 and jog precisely to 0,0 to determine the required offset.
See: forum.linuxcnc.org/show-your-stuff/32029...ild?start=470#137114
Read down a bit as there is more detail.
Replied by rodw on topic Another plasma component...
JTknives wrote: So I don’t know if this belongs here or in a new post. If it needs to be moved let me know and I will delete it and start a thread.
Im not a Linux programming genius, hell I could barely manage getting it installed. I don’t know if what I’m wanting can be added to the plasmaC or would need to be its own thing. The steel I cut is all high dollar stuff. Yesterday I cut up a 11”x23” sheet of stainless that cost me $100. So a mess up can be really costly and go down hill fast. Now I can’t cut it real fast as I’m running a 30xp and sitting at around 20”/min. I’m using sheetcam to nest and save it as a number attached to that sheet so I can load it back up and add more parts later and know what’s already been cut out. My issue is finding the exact starting corner. I have been using a square to get it square to the table and then bringing the torch down and moving over till I just barely touch the edge. Then set this as -.375 in g54 for x and y. This gives my just enough to clear the edge of the sheet. I do this because I set the edge of the parts at the edge of the sheet in sheet cam. This has eliminated the fudge factor guessing for me.
Yesterday I was wondering why could I not have a touch off button. The torch has ohmic so it could use that. Back when I ran cnc machines the new hass mills would load up a touch off tool. You would manually eyeball it over the corner and hit the touch off button. It would come down in the Z and find the top. Then move over in the X any Y a programmed amount and then come down a set amount and move over till it touches the side. It would set that as X and then retract and do the same for Y. It would then enter these numbers into the G54 offset.
If I could somehow build this function into my machine I would be tickled pink. We won’t bring up the other feature that would put it over the top. Well why not just mention it at least. Another machine I ran would touch off in 2 places on an edge and rotate the axis in the machine so the x and y would like up parallel to the sheet/part.
Something like this?
I just progrrammed a gcode macro in Gmoccappy to move to the offset and touch off X & Y
All I did was fire the torch to create a spot at position 0,0 and jog precisely to 0,0 to determine the required offset.
See: forum.linuxcnc.org/show-your-stuff/32029...ild?start=470#137114
Read down a bit as there is more detail.
Please Log in or Create an account to join the conversation.
- tommylight
- Away
- Moderator
-

Less
More
- Posts: 22011
- Thank you received: 7491
7 years 3 months ago #140922
by tommylight
Replied by tommylight on topic Another plasma component...
@JTknives
Probe screen ??? You already have the sensor, so a bit of editing and it should work.
The only problem is the torch need some empty space around the corner of the material to go below material and does your nozzle/shield extend enough outside to touch the sides of the material.
Probe screen ??? You already have the sensor, so a bit of editing and it should work.
The only problem is the torch need some empty space around the corner of the material to go below material and does your nozzle/shield extend enough outside to touch the sides of the material.
Please Log in or Create an account to join the conversation.
Moderators: snowgoer540
Time to create page: 0.713 seconds