Fusion 360 post processor file for Plamac

More
6 years 7 months ago #159037 by docwelch
I got a working solution to the circles being broken into many arcs problem over on the Fusion360 forum from Bob Schultz. I have incorporated that solution into my Fusion360 post processor. I will post this over in the PlasmaC Post Processors topic that Phil recently started.

Steven
The following user(s) said Thank You: phillc54, tommylight, rodw

Please Log in or Create an account to join the conversation.

More
6 years 7 months ago #159112 by CFE
Thankyou again Steven very much appreciated that you have shared the post processor. Your solution will make a big difference, having managed to incorporate the small hole processing and center punch mark features and by taking the time to produce a manual.

Please Log in or Create an account to join the conversation.

More
6 years 5 months ago #167069 by dvn4life1972
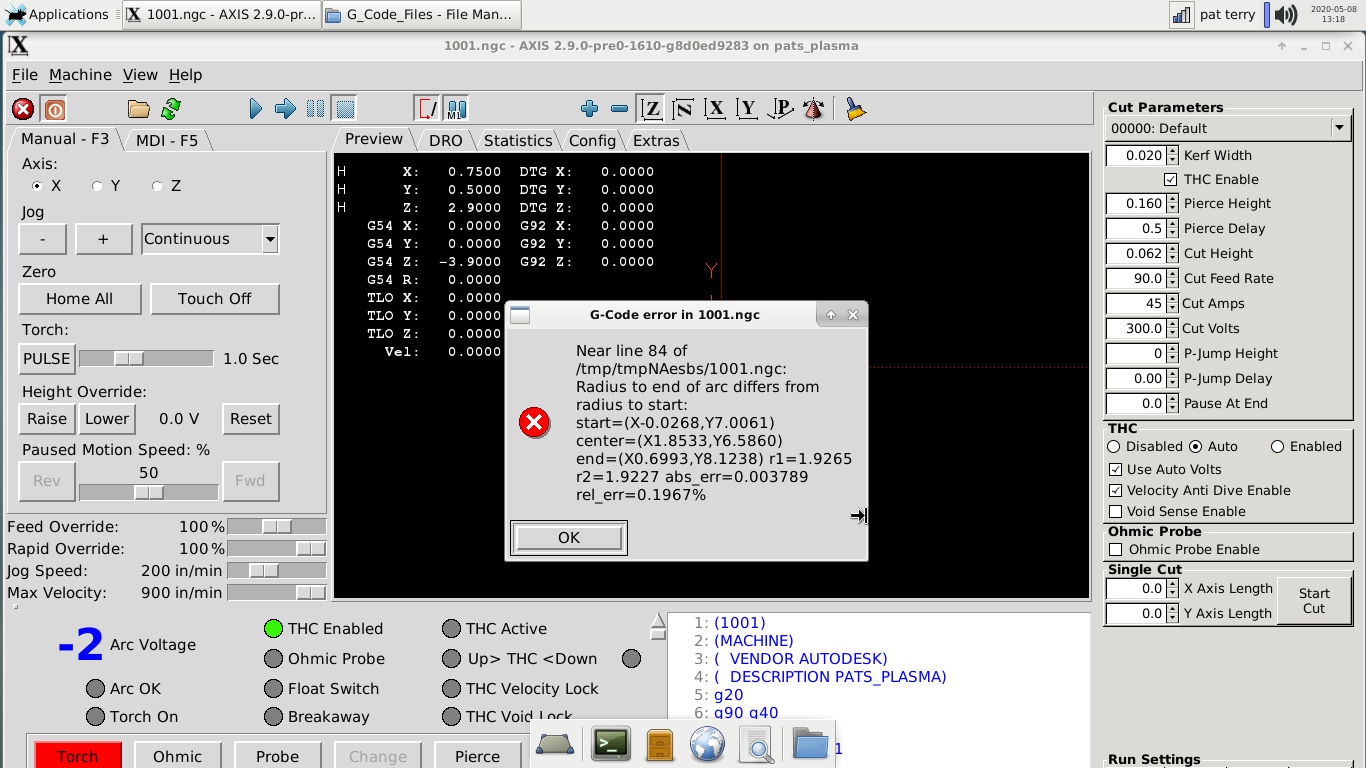
I appreciate the time and effort put into this pp. I couldn't dream of making an attempt at it. I've tried to use it several times, and I keep getting the same type of error at the machine when I load the gcode file. I've attached a screenshot of the error message as well as attached the gcode file itself.

Pat

Please Log in or Create an account to join the conversation.

More
6 years 5 months ago #167088 by phillc54
Maybe it needs some more digits of precision for the calculations.

You could try changing CENTER_ARC_RADIUS_TOLERANCE_INCH to say 0.004

linuxcnc.org/docs/2.8/html/config/ini-co...l#gcode:ini-features
The following user(s) said Thank You: dvn4life1972

Please Log in or Create an account to join the conversation.

More
6 years 4 months ago #173168 by islander261
Please bear with me as I am not skilled at using Fusion 360 and the CAM features. I am also not skilled in describing the geometry of Cartesian moves.

I needed to make a piece of equipment that required solid modeling to get all the parts right. So I built up a model in Fusion 360 with little effort ( I am an old ProE hand). Then I went to CAM several of the sheet steel parts to cut out with the plasma cutter using PlasmaC for the control. I used the PlasmaC post processor for Fusion 360 posted at the top of the topics. It took a bit of work to get everything setup and going but in the end I was able to get the models posted without any reported errors. Upon loading the Gcode into Plasmac I was greeted with errors on some of the arc moves. While the start and end points of the arcs were correct the posted I and J values were not on the blocks that error-ed out. The first thing I did notice was that the posted precision was rather excessive for imperial units, I reduced the posted precision to 4 places for imperial units with no change in the reported errors on loading. Because these are simple rectilinear parts I was able to manually fix the code to produce the parts.

The errors always occurred with two types of moves. A G2 (clockwise move) with the arc in the 4th quadrant and a G3 ( counter clockwise move) with the arc in the 2nd quadrant. The errors are very repeatable with minor geometry changes producing the same errors. So for now it is back to Inkscape and SheetCam for me.

One other thing, is there a way in Fusion 360 to do nesting? I like to cut a whole sheet of mixed parts at a time. I know how to do it manually by using work piece offsets but that isn't nice and graphically easy to do.

John

Please Log in or Create an account to join the conversation.

More
6 years 3 months ago #175372 by CFE
In the 'Property' section of the Post Process dialog box in Fusion change the "MergeCircles" value to "NO" this will fix the radius differs issue
The following user(s) said Thank You: dvn4life1972

Please Log in or Create an account to join the conversation.

Moderators: snowgoer540
Time to create page: 0.409 seconds
Powered by Kunena Forum