Showstopper Plasma Cutter retrofit

More
2 years 1 month ago #309809 by rodw

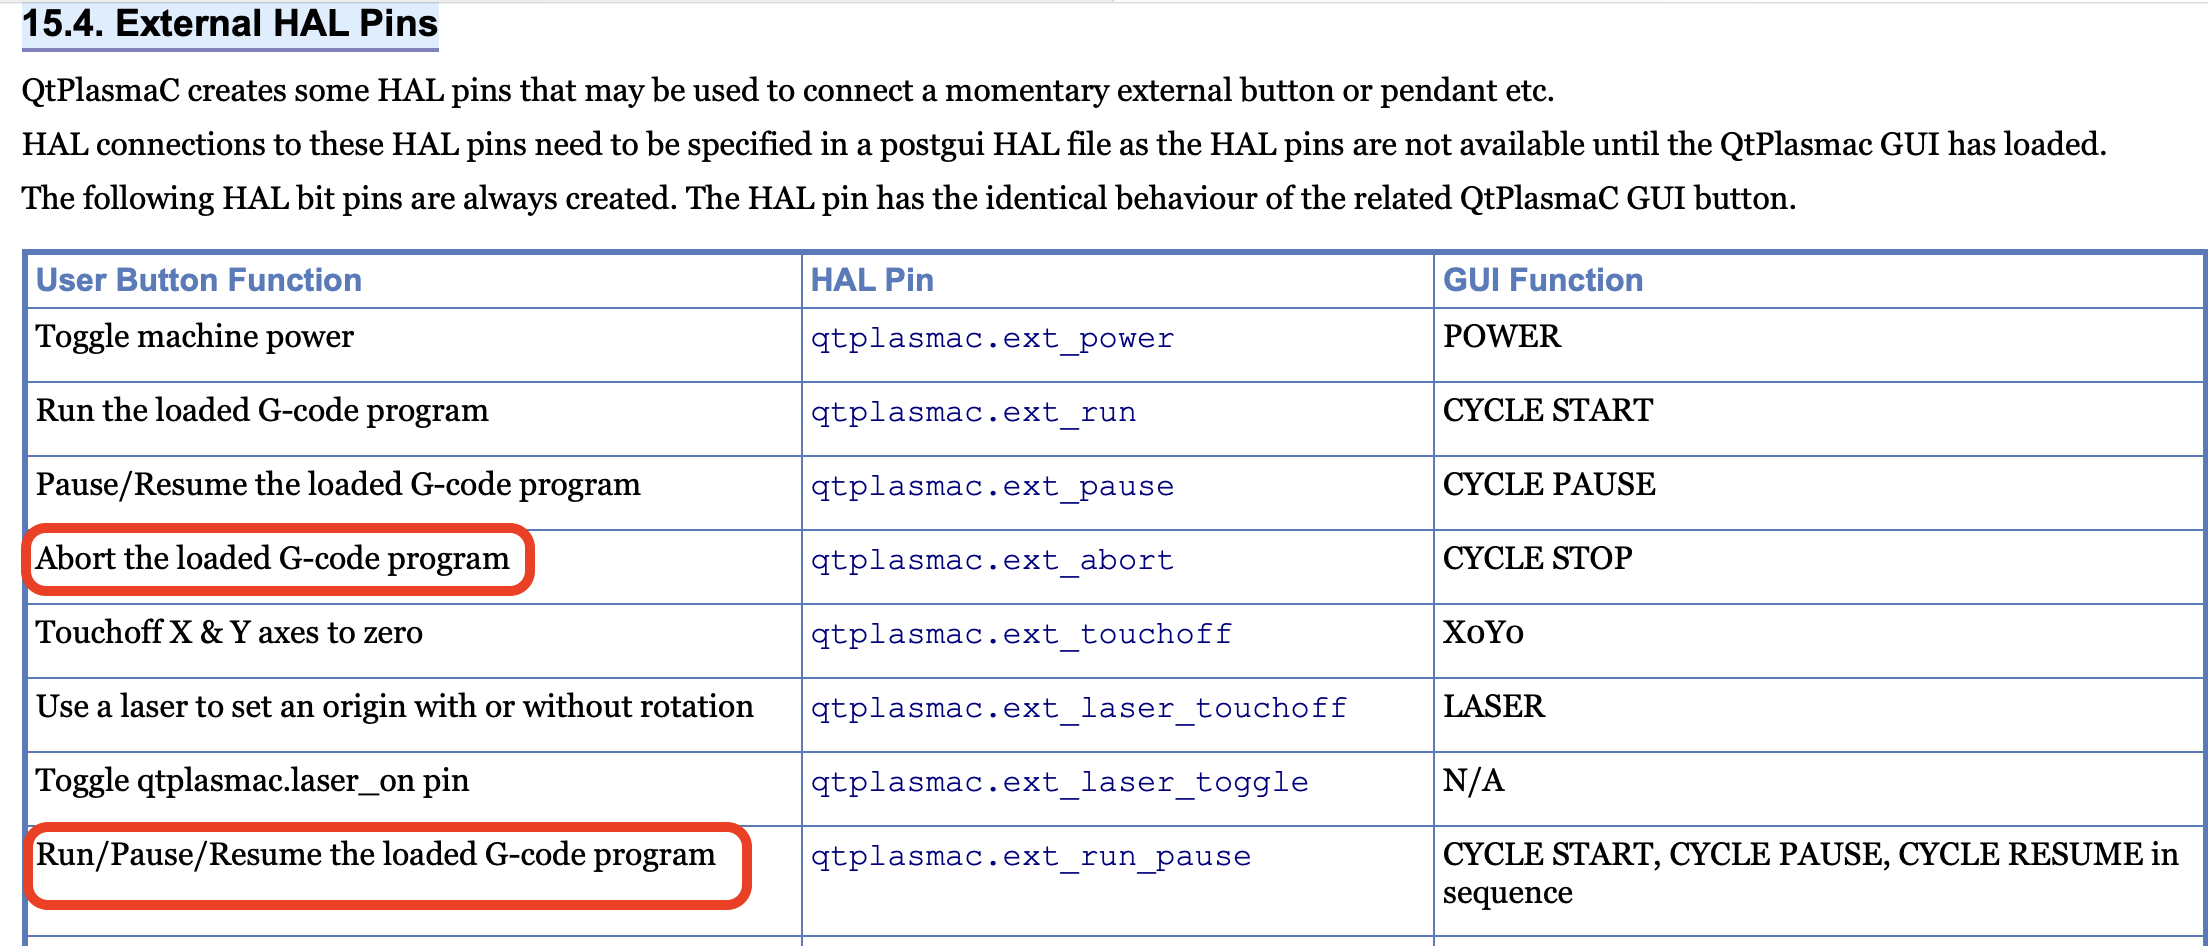
It may be easier to use two of the existing external hal pins rather than using runstep.hal.
Warning: Spoiler!
Thanks, that is long standing years old work by Todd right when I started my initial Linuxcnc build you are consigning to the tip! 
I need to review the pendant.hal. QTplasmac must use some more of halui. I wrote a component  to enable the buttons  to jog in directions + and - at slow and fast speed enabled by ~ so it must be in there as the rest I used for years.

It would be helpful if the docs had a list of signal names and extenal pins QTplasmac uses for those of us who want to use linuxcnc features unfettered by the GUI.


Please Log in or Create an account to join the conversation.

More
2 years 1 month ago #309810 by SteveatSteelCut
Does all of this have to be sorted out before running?I tried cutting a few tests just to see if I can run before at this stage.It seemed to be working, I was just changing some of the speeds in the material settings and now it is not happy to probe. I even restarted qtplasmac and still the same thing.I find it strange that I don't know how anything has changed but it is unhappy. I even changed the speeds back that I had changed and it didn't help.

Please Log in or Create an account to join the conversation.

More
2 years 1 month ago #309811 by phillc54
Did you inadvertently change the Pierce Height to something too large above the probed material height.

Please Log in or Create an account to join the conversation.

More
2 years 1 month ago #309812 by phillc54

It would be helpful if the docs had a list of signal names and extenal pins QTplasmac uses for those of us who want to use linuxcnc features unfettered by the GUI.

We could possibly do something like that, I usually just do something like:
Code:
halcmd show sig > ~/Downloads/halsignals.txt
The following user(s) said Thank You: rodw

Please Log in or Create an account to join the conversation.

More
2 years 1 month ago #309813 by SteveatSteelCut
Pierce height is 3.8. We wondering if something happened and now it thinks it is 3.8 inches. But now it seems to have worked itself out.

I turned the torch off (on the interface) and cycled start, and it worked.
Turned the torch back on and it appears to be working again now. 

At least its cutting now, i will work on stabilizing the torch and see if I can get the circles cutting right.

Please Log in or Create an account to join the conversation.

More
2 years 1 month ago #309868 by SteveatSteelCut
Hey guys,
back to the same problem as before.
We successfully cut a few files and then we got the same error with the height would exceed z axis max limit.
Tried to disable the torch and start program: Same error.
Loaded the last successful file that we cut and tried cycle start: Same error.
Closed qtplasmac, restarted, homed etc. Loaded same successful file that we cut: Same error.
Any suggestions?
I am wondering if the g code filter is a problem. Creating g code from hypertherm nestmaster and running it through a filter.
However it doesn't explain it working a few times in a row and then failing. I have also tried changing to different material setting that I have saved and running the program again to see if it helps.

Please Log in or Create an account to join the conversation.

Time to create page: 0.269 seconds
Powered by Kunena Forum
