Mill atc configuration

More
3 years 1 month ago - 3 years 1 month ago #279820 by Artur_1617
Replied by Artur_1617 on topic Mill atc configuration
This we have now in spindle setup   net spindle-index-enable <= hm2_5i25.0.encoder.04.input-index
After delete net spindle-input-index <= hm2_5i25.0.encoder.04.input-index and net spindle-input-index <= hm2_5i25.0.encoder.04.reset
Rigid tapping now working but orient stop working.
Last edit: 3 years 1 month ago by Artur_1617.

Please Log in or Create an account to join the conversation.
More
3 years 1 month ago #279826 by Aciera
Replied by Aciera on topic Mill atc configuration
Hm, not sure if this works but replace this:

net spindle-index-enable <= hm2_5i25.0.encoder.04.input-index

with this:

net spindle-index-enable <= hm2_5i25.0.encoder.04.input-index
net orient-enable => and2.1.in0
net spindle-input-index => and2.1.in1
net encoder-reset <= and2.1.out => hm2_5i25.0.encoder.04.reset

Don't forget to 'loadrt/addf' the 'and2.1' component
The following user(s) said Thank You: Artur_1617

Please Log in or Create an account to join the conversation.
More
3 years 1 month ago - 3 years 1 month ago #279844 by Artur_1617
Replied by Artur_1617 on topic Mill atc configuration
Now rigid tapping working and encoder count is set to 0 after hit index.Start orient after tapping with encoder count no past 232 encoder count working ok.But if turn spindle cw 50 times and stop. orient-pid.command and orient-pid.feedback is 50.0When orient start orient-pid.feedback is reset to 0 but orient-pid.command is still 50.0 spindle turn and not stop.
 Actual hal   
 

File Attachment:

File Name: Frezarka_z...9-05.hal
File Size:17.88 KB
Last edit: 3 years 1 month ago by Artur_1617.

Please Log in or Create an account to join the conversation.

More
3 years 1 month ago #279862 by Aciera
Replied by Aciera on topic Mill atc configuration
Something went wrong with that Hal file upload.
I don't think we should be resetting the encoder count, so i would suggest to revert the last change.


So remove this:

net spindle-index-enable <= hm2_5i25.0.encoder.04.input-index
net orient-enable => and2.1.in0
net spindle-input-index => and2.1.in1
net encoder-reset <= and2.1.out => hm2_5i25.0.encoder.04.reset

and replace with this:

net spindle-index-enable <= hm2_5i25.0.encoder.04.input-index


And remove the 'loadrt/addf' for the 'and2.1' component.


I would try again with this and check 'orient-pid.command' and 'orient-pid.feedback'. Maybe that points us in the right direction. Other than that I have run out of ideas for the moment and I don't have a system to test spindle.orient with.
The following user(s) said Thank You: Artur_1617

Please Log in or Create an account to join the conversation.

More
3 years 1 month ago #279937 by Artur_1617
Replied by Artur_1617 on topic Mill atc configuration
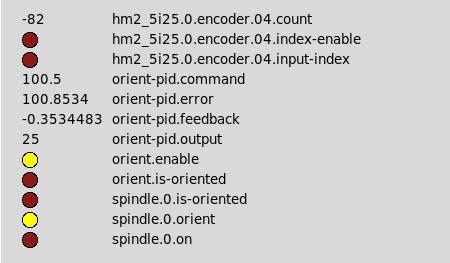
On 1screenshoot we have working orient with pid.coomand and pid.error after 100 turns of spindle and spindle turn and not stop. The pid feedback was to 100 but after hit index is set to 1
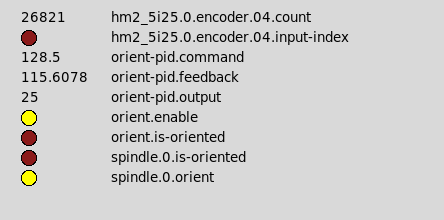
Aciera I make the change from Your last post today morning Rigid tapping working but Orient want to back to 0 encoder count 2scrrenshot
Anybody work with both orient and rigid tapping?


File Attachment:

File Name: Frezarka_z...05-2.hal
File Size:17.88 KB

Please Log in or Create an account to join the conversation.

More
3 years 1 month ago #279970 by Artur_1617
Replied by Artur_1617 on topic Mill atc configuration
I found solution.
In toolchange.ngc go to write (today tested and working)
M3 S30
G33.1 Z 0.1 K0.1
M2
After that command spindle is indexed and on position 1-4 encoder counts which is easier to setup orient pid becouse all time start from the same position.
Last things for now;
1. When orient point is close to 116encoder count for example 117 then back to 115 but passing by 116 and orient.is-oriented is set to High. Need to delay this. If is on 116 encoder position 1 second then orient.is-oriented go High.
2. Is possible make some output checking if encoder position is 114-117 then output is high? spindle.is-oriented go to high only for moment.

Please Log in or Create an account to join the conversation.

Time to create page: 0.084 seconds
Powered by Kunena Forum
