
- Posts: 1635
- Thank you received: 595
Schaublin 125-CNC retrofit.
- RotarySMP
- Offline
- Platinum Member
-

Less
More
4 years 10 months ago - 4 years 10 months ago #228457
by RotarySMP
Replied by RotarySMP on topic Schaublin 125-CNC retrofit.
Wow, you answered all my thoughts about, what are these dL/dT filters, or whatever they are talking about. Thanks a lot Ralph.
Should the load reactor get mounted close to the VFD or close to the motor?
At this stage it is easier to just plop the motor back in and use it, as the Variator is there, whereas making a set of poly-Vee pulleys might be beyond the capacity of the Boley. It will be interesting whether i can come up with a sensible control logic for VFD + CVT + Back gear. If I only do VFD + Back gear, guys like Andy have already written the comp.
Mark
Last edit: 4 years 10 months ago by RotarySMP.
Please Log in or Create an account to join the conversation.
- spumco
- Offline
- Platinum Member
-
Less
More
- Posts: 2180
- Thank you received: 905
4 years 10 months ago #228466
by spumco
Replied by spumco on topic Schaublin 125-CNC retrofit.
As close to the VFD as you can get.
Diagram taken from my Hitachi manual.
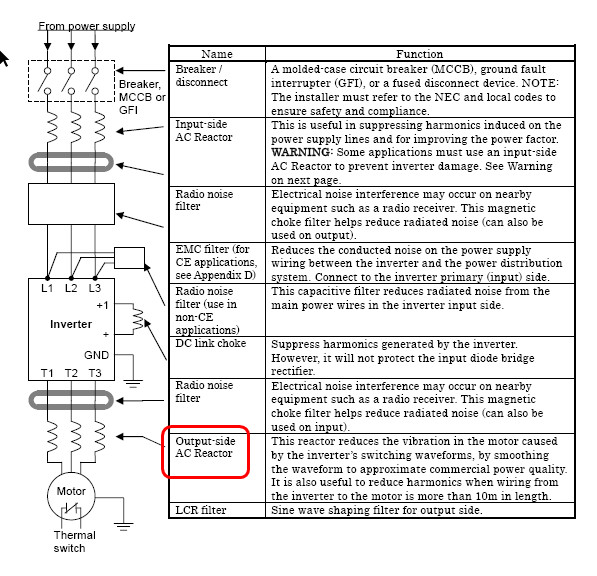
Diagram taken from my Hitachi manual.
The following user(s) said Thank You: RotarySMP, anfänger, DoWerna
Please Log in or Create an account to join the conversation.
- spumco
- Offline
- Platinum Member
-
Less
More
- Posts: 2180
- Thank you received: 905
4 years 10 months ago #228504
by spumco
Replied by spumco on topic Schaublin 125-CNC retrofit.
And another thing...
Even if your Boley is a little light for big poly-v pulleys, your Maho sure ain't. Add a chuck or mandrel to the horizontal spindle, clamp a tool in the vise, and pop out a couple of pulleys CNC-style.
The tricky bit is getting the 40 degree cutter to match the belt profile. Iscar and others sell poly-v specific inserts, but you could always fiddle around with an HSS threading bit to get the angles good enough.
Fabbing the pulleys on the Maho should make the Schaublin jealous enough it'll reassemble itself in an attempt to regain Alpha-Lathe status.
-R
The following user(s) said Thank You: RotarySMP, anfänger
Please Log in or Create an account to join the conversation.
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
4 years 10 months ago #228516
by RotarySMP
Replied by RotarySMP on topic Schaublin 125-CNC retrofit.
I already bought one, and it is shipping. Thanks for adding clarity Ralph.
Mark
Mark
Please Log in or Create an account to join the conversation.
- anfänger
- Offline
- Platinum Member
-
Less
More
- Posts: 647
- Thank you received: 267
4 years 10 months ago #228519
by anfänger
Replied by anfänger on topic Schaublin 125-CNC retrofit.
Pulleys you get usually for a reasonable price. I bought them for my lathe conversion als well.
It’s a great thread here. I didn’t know about line reactors (Netzdrossel in German) I’ll get one for my lathe. Though I will still limit the range from 30 to 50hz cause the main Schaft also Runs the Pump for the hydraulic clutches.
Have you considered using a manual switch to chose between the the two windings? Or two modern 24v contractors or a „wendeschütz“ they are way smaller then they used to be.
Please Log in or Create an account to join the conversation.
- arvidb
- Offline
- Platinum Member
-
Less
More
- Posts: 459
- Thank you received: 158
4 years 10 months ago #228522
by arvidb
Replied by arvidb on topic Schaublin 125-CNC retrofit.
But, but, but, the variator is so cool, why replace it even if the original motor breaks? I think you owe it to this machine, and its creators, to keep it in. 
For the control logic, perhaps something like this would work:
1) Aim to keep the motor speed as high as possible, to maximize power.
2) Use the variator as much as possible since it can set the reduction while running (and only while running?).
3) "Manually" set the gearbox to the lower speed range, only if you need the torque (or if you know the next cut will use only very low spindle speeds). How is the gearbox controlled? Either use some special codes in the G-code to engage/release it; set it using a "software switch", or use an electrical switch and feedback its setting into LinuxCNC.
4) Finally use the VFD and the feedback from the spindle to get to the target speed.
This maximizes the use of the gearing during constant surface velocity cuts.
I'm assuming here that there is no way to get LinuxCNC to report the spindle speed range needed during "the next cut". If there is, then you could of course automate the gearbox too.
It will be interesting whether i can come up with a sensible control logic for VFD + CVT + Back gear. If I only do VFD + Back gear, guys like Andy have already written the comp.
For the control logic, perhaps something like this would work:
1) Aim to keep the motor speed as high as possible, to maximize power.
2) Use the variator as much as possible since it can set the reduction while running (and only while running?).
3) "Manually" set the gearbox to the lower speed range, only if you need the torque (or if you know the next cut will use only very low spindle speeds). How is the gearbox controlled? Either use some special codes in the G-code to engage/release it; set it using a "software switch", or use an electrical switch and feedback its setting into LinuxCNC.
4) Finally use the VFD and the feedback from the spindle to get to the target speed.
This maximizes the use of the gearing during constant surface velocity cuts.
I'm assuming here that there is no way to get LinuxCNC to report the spindle speed range needed during "the next cut". If there is, then you could of course automate the gearbox too.
The following user(s) said Thank You: RotarySMP
Please Log in or Create an account to join the conversation.
Moderators: piasdom
Time to create page: 0.311 seconds