
- Posts: 12170
- Thank you received: 4153
Another plasma component...
- rodw
- Offline
- Platinum Member
-

Less
More
7 years 5 months ago #132502
by rodw
I'm actually struggling with this. I have about 6 different tips for my machine. (30A, 40A, 60A, 80A, 100A, 120A) Here is the metric cut chart for my machine with a 9-8211 (80 amp) tip
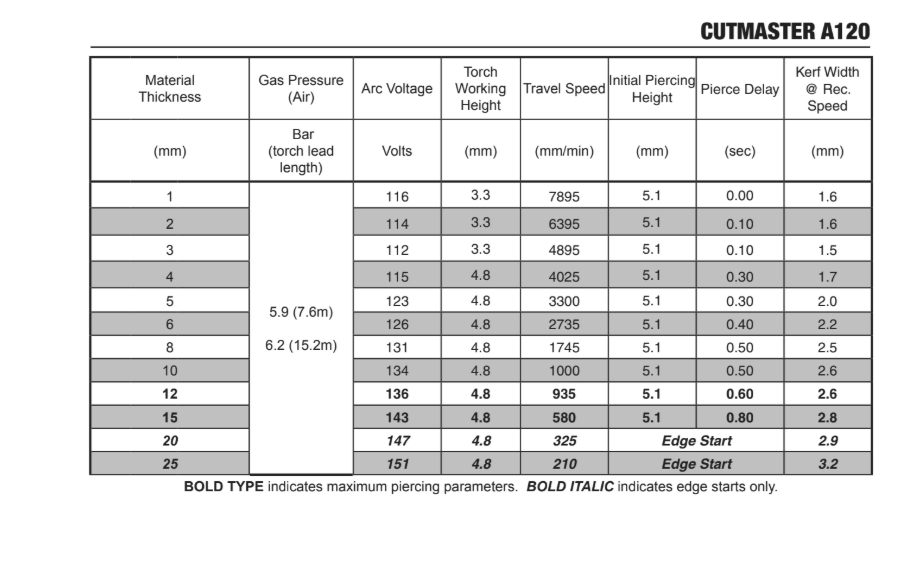
The key parameter we want is the Tool Diameter or kerf width
There are 10 different kerf widths for this tip alone.
The kerf widths for mild steel for my machine range from 1.4mm to 4.4 mm. I think I'd have to create a series of 30 odd tips 0.1mm apart that don't really relate to anything.
I'm not thinking the tip definitions add anything other than complexity.
I personally think unless you moved to a fully relational database, what we need would be met by simply adding a unique ToolID and a kerf width to the existing materials table records.
Replied by rodw on topic Another plasma component...
phillc54 wrote: Guys,
I have a mostly working concept for tool handling in the configs.
I'm actually struggling with this. I have about 6 different tips for my machine. (30A, 40A, 60A, 80A, 100A, 120A) Here is the metric cut chart for my machine with a 9-8211 (80 amp) tip
The key parameter we want is the Tool Diameter or kerf width
There are 10 different kerf widths for this tip alone.
The kerf widths for mild steel for my machine range from 1.4mm to 4.4 mm. I think I'd have to create a series of 30 odd tips 0.1mm apart that don't really relate to anything.
I'm not thinking the tip definitions add anything other than complexity.
I personally think unless you moved to a fully relational database, what we need would be met by simply adding a unique ToolID and a kerf width to the existing materials table records.
Please Log in or Create an account to join the conversation.
- BigJohnT
- Offline
- Administrator
-

Less
More
- Posts: 3981
- Thank you received: 994
7 years 5 months ago #132503
by BigJohnT
Replied by BigJohnT on topic Another plasma component...
I'm using a database for my plasma cut data on my GUI just for that reason that there are so many different options and kerf width changes with material, thickness and nozzle.
JT
JT
The following user(s) said Thank You: rodw
Please Log in or Create an account to join the conversation.
- rodw
- Offline
- Platinum Member
-
Less
More
- Posts: 12170
- Thank you received: 4153
7 years 5 months ago #132504
by rodw
Yes, I shared some example python scripts and SQL tables a long time ago somewhere in this thread but I had not taken into account the LinuxCNC tool table.. I'll see if I can find it.
Replied by rodw on topic Another plasma component...
BigJohnT wrote: I'm using a database for my plasma cut data on my GUI just for that reason that there are so many different options and kerf width changes with material, thickness and nozzle.
JT
Yes, I shared some example python scripts and SQL tables a long time ago somewhere in this thread but I had not taken into account the LinuxCNC tool table.. I'll see if I can find it.
Please Log in or Create an account to join the conversation.
- rodw
- Offline
- Platinum Member
-
Less
More
- Posts: 12170
- Thank you received: 4153
7 years 5 months ago #132505
by rodw
Replied by rodw on topic Another plasma component...
rodw wrote:
BigJohnT wrote:
Yes, I shared some example python scripts and SQL tables a long time ago somewhere in this thread but I had not taken into account the LinuxCNC tool table.. I'll see if I can find it.
Well, that was quick!. it is on page 2. forum.linuxcnc.org/plasma-laser/35449-an...nent?start=10#119922
I might revisit this work as I did not look at it again.
But we don't wan to to make too much work for Phill.
Please Log in or Create an account to join the conversation.
- phillc54
- Offline
- Platinum Member
-
Less
More
- Posts: 5711
- Thank you received: 2100
7 years 5 months ago #132506
by phillc54
Cheers, Phill.
Replied by phillc54 on topic Another plasma component...
How would you then relate that to a LinuxCNC tool.I personally think unless you moved to a fully relational database, what we need would be met by simply adding a unique ToolID and a kerf width to the existing materials table records.
Cheers, Phill.
Please Log in or Create an account to join the conversation.
- BigJohnT
- Offline
- Administrator
-
Less
More
- Posts: 3981
- Thank you received: 994
7 years 5 months ago #132512
by BigJohnT
Replied by BigJohnT on topic Another plasma component...
G41.1 and G42.1 you can program the tool diameter on the fly...
JT
JT
The following user(s) said Thank You: phillc54
Please Log in or Create an account to join the conversation.
Moderators: snowgoer540
Time to create page: 0.826 seconds