Advanced Search

Search Results (Searched for: )

  • MaHa
  • MaHa
14 Sep 2025 22:04
Replied by MaHa on topic Touch off, OK button greyed out

Touch off, OK button greyed out

Category: AXIS
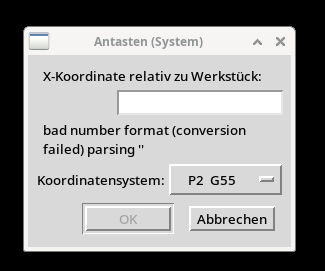
Had a look again, in the sim. When enter the first number or decimal point, 'file not open apears' in the dialog box.
When i delete all content of the input field, another message:

 
  • unknown
  • unknown
14 Sep 2025 22:02
Replied by unknown on topic G81 Spindle Reversal Between Each Hole

G81 Spindle Reversal Between Each Hole

Category: General LinuxCNC Questions

You might have some luck in remapping an unallocated gcode, but I'm unsure how this would integrate with your cam software.
linuxcnc.org/docs/html/remap/remap.html
  • unknown
  • unknown
14 Sep 2025 21:40
Replied by unknown on topic Touch off, OK button greyed out

Touch off, OK button greyed out

Category: AXIS

Best bet guys, since this an official release is to go to GitHub and raise an issue.
As it is there should be no "kinks".
Just out of interest does inputting 0.0 or some other variation work ? Just a guess .
  • juergen-home
  • juergen-home
14 Sep 2025 18:39
Replied by juergen-home on topic Touch off, OK button greyed out

Touch off, OK button greyed out

Category: AXIS

The same her with 2.9.5 on my real machine and simulation. I went back to 2.9.4.
  • tommylight
  • tommylight's Avatar
14 Sep 2025 18:07
Replied by tommylight on topic Help - Can't see the forest for the trees!

Help - Can't see the forest for the trees!

Category: O Codes (subroutines) and NGCGUI

Second line does not look correct, see my previous post.
You have a # in the wrong place behind a < , it should be in front of it.
  • LinuxCrashOut
  • LinuxCrashOut's Avatar
14 Sep 2025 17:54

HAL help needed for MPG wheel jogging and machine enabling logic

Category: HAL

Ok, I got some help and realized the mesa 7i76e was in mode 0, now it is in mode 2 and I can see the counts on hm2_7i76e.0.7i76.0.0.enc0.count

I am still lost about how the following works (as for the logic)

I would love to have one button that enables the jog for x axis for example, and then the mpg makes it move (while the button is pressed)


File Attachment:

File Name: empty_sample_0.4.hal
File Size:10 KB
  • scsmith1451
  • scsmith1451's Avatar
14 Sep 2025 17:39
Replied by scsmith1451 on topic Help - Can't see the forest for the trees!

Help - Can't see the forest for the trees!

Category: O Codes (subroutines) and NGCGUI

Don't know why file didn't come through, but I'm pasting it here:

o<auto-xy-zero> sub
<#factor> = 1 (Adjust for metric)
o100 if [#<_metric> EQ 1]
#<factor> = 25.4
o100 endif

#<X-move> = [#<_ini[LASER]laser-offset-x> * #<factor>]
#<Y-move> = [#<_ini[LASER]laser-offset-y> * #<factor>]
#<feedrate> = [20 * #<factor>]

; (Move table to program start)
G91 G0 X#<X-move> Y#<Y-move> F#<feedrate>
G10 L20 P0 X0 Y0 A0 ( Set X/Y DROs to zero )

o<auto-xy-zero> endsub

m2

Looks to me that all of the references are correctly formatted.

Regards,
  • Darium
  • Darium
14 Sep 2025 17:36 - 16 Sep 2025 16:54

G81 Spindle Reversal Between Each Hole

Category: General LinuxCNC Questions

Hi,
Is there any way to easily add spindle reversal each hole during drilling? I drill a lot and the my steel is too stringy regardless of speed and feed. i came across HASS video of it. this is the link 
.
is there any way I can modify G83 like that? or even better spindle reversal between pecks
  • MaHa
  • MaHa
14 Sep 2025 17:29
Replied by MaHa on topic Touch off, OK button greyed out

Touch off, OK button greyed out

Category: AXIS

That was not helpful. Now it's off the no reply list without solution.
As mentioned, any input but zero greys out the ok button. The real machine and sim in Virtualbox have the same issue.
In the dialogbox it says:  file not open
A gcode file is loaded, so this could point to an internal fault
 
Displaying 13471 - 13479 out of 13479 results.
Time to create page: 0.387 seconds
Powered by Kunena Forum