Some thoughts and some findings using PlasmaC

More
6 years 2 weeks ago - 6 years 2 weeks ago #186132 by phillc54
Yes, it would be possible that the last servo thread of Z motion hasn't completed when the torch is activated. A relatively easy fix if it is an issue.

EDIT: that would equate to about 0.016mm per 1000mm/min
Last edit: 6 years 2 weeks ago by phillc54.
The following user(s) said Thank You: snowgoer540

Please Log in or Create an account to join the conversation.

More
6 years 2 weeks ago - 6 years 2 weeks ago #186136 by PCW
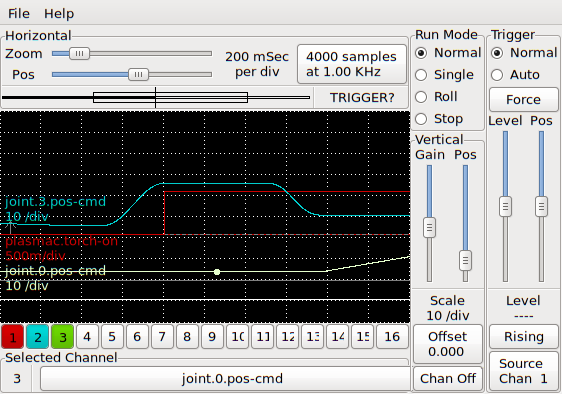
If you look at the time/division, Torch-on happens about 60 ms before the motion is complete
(so close to 60 servo periods). This is about 2.5 mm before the endpoint.
Last edit: 6 years 2 weeks ago by PCW.

Please Log in or Create an account to join the conversation.
More
6 years 2 weeks ago #186138 by tommylight
It is enough to repeatedly notice just by looking at it.
I have a stinking suspicion that is causing misfires very often.
PlasmaC is set in mode 0 for now, i do have a reed switch installed and ready to be wired to the input, but this same thing happened with mode 1 and since that was not my plasma source i could not experiment with it, not this one is also not mine but it is and will be in my shop for some more days. This one will delay the first torch on for about 1 sec then have no delay at all on all subsequent fires, it just fires instantly and never fails. It is a 120A Cebora, pretty old HF/HV pilot arc one with a THCAD300 installed on the outside.

ASUS ROG Crosshair VIII Impact - AMD X570

Please Log in or Create an account to join the conversation.
More
6 years 2 weeks ago #186152 by phillc54
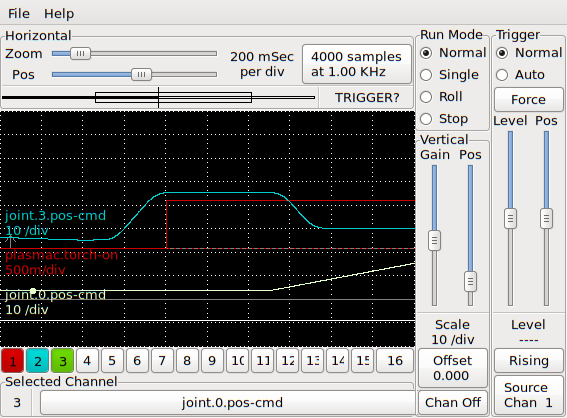
OK, I got that sorted as shown below but while doing it I noticed that motion starting after the pierce delay may be wrong.

At the moment it holds X/Y motion until cut height is reached which seems to really make a long pierce delay:
Warning: Spoiler!


Would it be better to allow motion as soon as the pierce delay has finished, it means that Z will move down to cut height when X/Y motion has begun:
Warning: Spoiler!
The following user(s) said Thank You: tommylight, snowgoer540

Please Log in or Create an account to join the conversation.

More
6 years 2 weeks ago #186167 by snowgoer540

phillc54 wrote: OK, I got that sorted as shown below but while doing it I noticed that motion starting after the pierce delay may be wrong.

At the moment it holds X/Y motion until cut height is reached which seems to really make a long pierce delay:

Warning: Spoiler!


Would it be better to allow motion as soon as the pierce delay has finished, it means that Z will move down to cut height when X/Y motion has begun:
Warning: Spoiler!


I have definitely noticed this before... :)

My vote is the latter. I think as soon as the pierce delay is expired it should start XY motion WHILE moving to cut height (which will all be part of the lead in anyways). While it doesn’t specifically mention XY motion, that was my interpretation of the Hypertherm THC manual’s chart showing what movements happen when for Z axis.

Also, for thicker materials, I always find myself adjusting the pierce delay to make it shorter, otherwise I get some unstable/unpredictable behavior at the beginning of the cut (because the pierce delay seems to be too long). In all cases, the material was already pierced when it flamed out.

I’m also willing to do some testing on this if you made a test branch. If that is something you’re interested in, it would be convenient to have a check box to toggle between the modes I would be testing (move to cut height then XY vs move to cut height at the same time as XY).

-Greg
The following user(s) said Thank You: phillc54

Please Log in or Create an account to join the conversation.
More
6 years 2 weeks ago - 6 years 2 weeks ago #186174 by snowgoer540
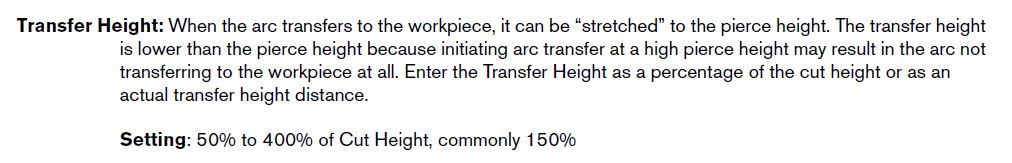
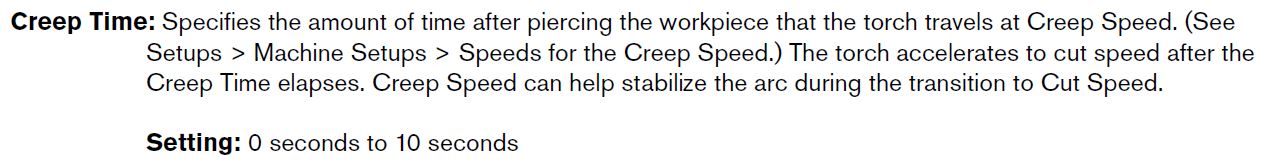
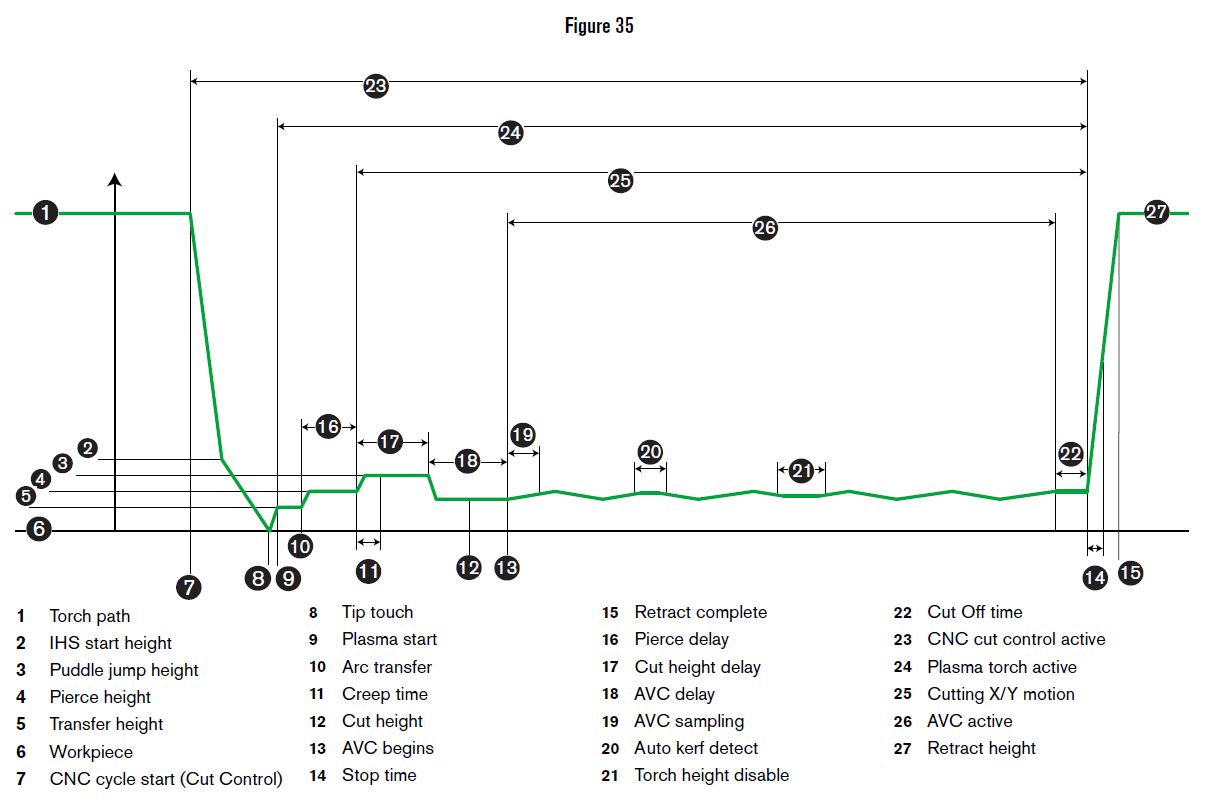
Actually, I take that back. The Hypertherm manual does specifically show when X/Y motion begins. It is number 25 on the chart below. Also, they use something called a "Transfer Height", which according to their definition is used to stretch the arc TO pierce height because on thick materials with a high pierce height, an arc transfer may not occur at all (Since I'm guessing this manual is meant for HD power sources that cut THICK material, "transfer height" probably isn't relevant for our setups, but it's interesting to note that it does exist).

Here's how I read the chart with starting with the torch touch (No. 8 on the chart):

a. Tip Touch (8)
b. Move to Transfer Height (5)
c. Plasma Start (9) and Plasma Torch becomes Active (24)
d. Arc Transfer (10) while moving to Pierce height (4)
e. Pierce Delay (16)
f. Cutting X/Y motion begins (25)
optional if puddle jump - g. Move to puddle Jump height (if set in our case) (3)
optional if puddle jump - h. Creep time (specifies the amount of time after piercing the workpiece that the torch travels at Creep Speed, the torch accelerates to cut speed after the creep time elapses) (11)
optional if puddle jump - i. Cut height delay (this is puddle jump delay in our terms) (17)
j. Torch moves to cut height (12) and AVC (THC for us) delay timer starts (18)
k. AVC (THC for us) starts sampling voltage (19) and starts controlling the torch (26)

Warning: Spoiler!


To me, that pretty definitively shows that X/Y should begin after the pierce delay expires WHILE moving to cut height.

Here's some of the terms from above out of the manual

Warning: Spoiler!

Warning: Spoiler!

Warning: Spoiler!
Last edit: 6 years 2 weeks ago by snowgoer540. Reason: Remembered the alphabet, apparently.
The following user(s) said Thank You: phillc54, rodw

Please Log in or Create an account to join the conversation.

Moderators: snowgoer540
Time to create page: 0.514 seconds
Powered by Kunena Forum