
- Posts: 5713
- Thank you received: 2100


Please Log in or Create an account to join the conversation.

Please Log in or Create an account to join the conversation.
tommylight wrote: Looks much better, when can i give it a run?
Thank you.
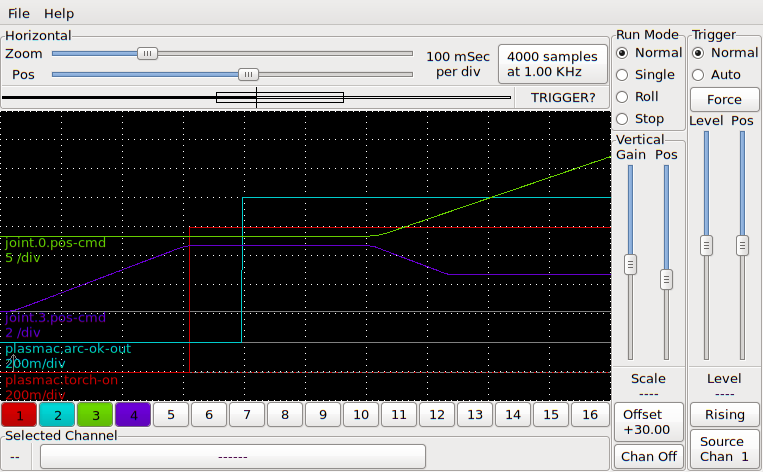
 Seems to work well from what I saw. Seems like it solved a lot of the joint following issues we were seeing as well.
Please Log in or Create an account to join the conversation.
), very long cables going from the machine to the plasma source, computer and monitor are also outside in the cold, etc, etc, .Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.


Please Log in or Create an account to join the conversation.