Mill atc configuration

More
3 years 2 months ago - 3 years 2 months ago #278553 by Artur_1617
Replied by Artur_1617 on topic Mill atc configuration
Maked the changes and;
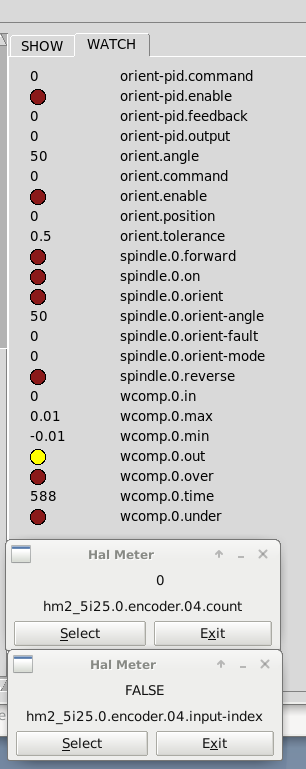
If turn spindle cww encoder.04.count go from 0 to 232 then set to 0 and go again 0 to 232 and we have some orient-pid.feedback working
If turn spindle cw encoder.04.count not count nothing only when past index show 1 and back to 0. After this orient not start orient-pid.feedback is 0
When orient direction is close for run cww start orient and still turning becouse not count on encoder.04.count input
Encoder 04 is true out of index and is false when is on index is important?
Screen11 after turn spindle cw
Screen12 after turn spindle ccw


File Attachment:

File Name: Frezarka_z...20-4.hal
File Size:17.96 KB
Last edit: 3 years 2 months ago by Artur_1617.

Please Log in or Create an account to join the conversation.
More
3 years 2 months ago #278557 by Aciera
Replied by Aciera on topic Mill atc configuration

If turn spindle cww encoder.04.count go from 0 to 232 then set to 0 and go again 0 to 232

Sounds like your encoder scale is not correct, so you'll have to fix that first.

Please Log in or Create an account to join the conversation.
More
3 years 2 months ago #278559 by Artur_1617
Replied by Artur_1617 on topic Mill atc configuration
Encoder is 58 imp per rev 58x4=232
But now see other things. When turn spindle with hand wery slow see encoder is couting onlt to 230 when On index. And start counting again when index is off. We loos two encoder count.

Please Log in or Create an account to join the conversation.

More
3 years 2 months ago #278563 by Aciera
Replied by Aciera on topic Mill atc configuration
so i guess you could try changing this (1/360):

setp scale.orient.gain 0.00277778

to this (1/230):
setp scale.orient.gain 0.004347826


It's late now and I've run out of time for today. Good luck.
The following user(s) said Thank You: tommylight, Artur_1617

Please Log in or Create an account to join the conversation.

More
3 years 2 months ago #278598 by Artur_1617
Replied by Artur_1617 on topic Mill atc configuration
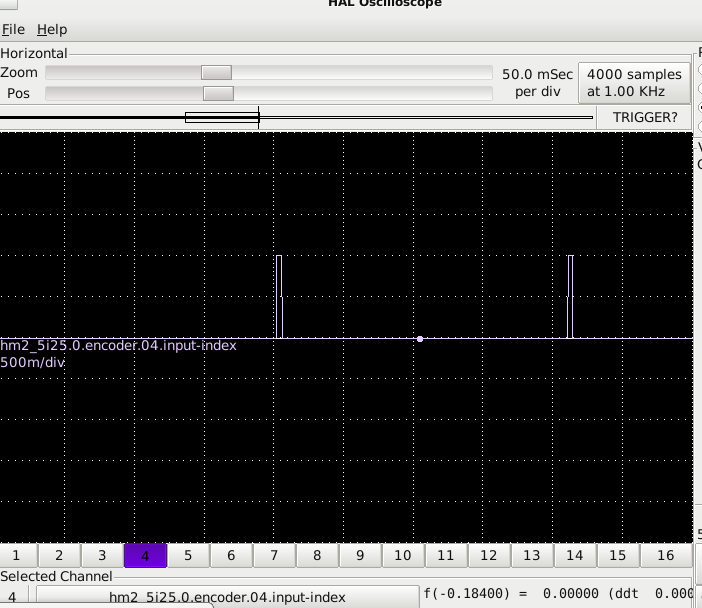
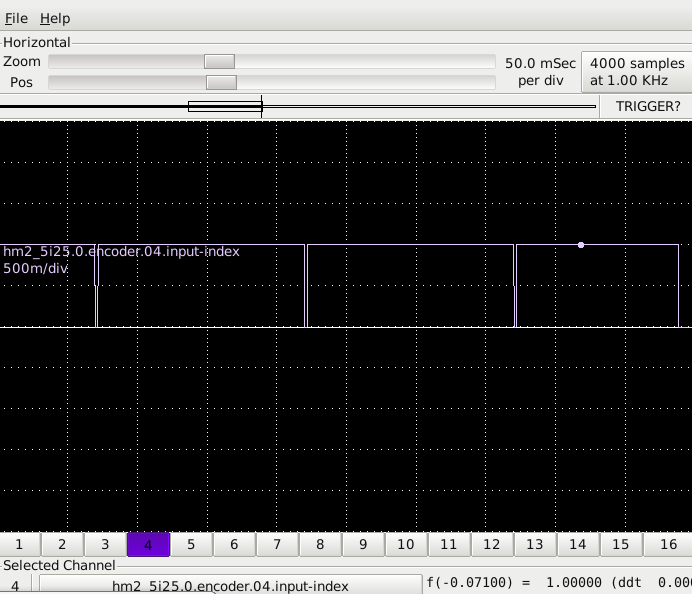
Im back to setup without orient for see index issue.
If spindle turn cw encoder.04.input-index when is out of index is false and on index is true this working ok.
But if spindle turn ccw when is out of index is false but after first past index is set to true and change to false on index
screen1 spindle run cw
screen2 spindle run cww
This is ok?


Please Log in or Create an account to join the conversation.

More
3 years 2 months ago #278606 by Aciera
Replied by Aciera on topic Mill atc configuration
That is strange. I don't think this can work properly because you have a shift in the positive edge of the signal.
What kind of sensor are you using?

Please Log in or Create an account to join the conversation.

Time to create page: 0.082 seconds
Powered by Kunena Forum