PlasmaC torch starting problem (Solved with help from the famous three)

More
6 years 7 months ago - 6 years 7 months ago #160543 by rodw
Replied by rodw on topic PlasmaC torch starting problem

Clive S wrote:

rodw wrote: Why don't you try a timedelay of say 0.2 to 0.5 seconds after torch on and use that as a ArcOK? Leave it on until the cut is finished.

It seems like your machine is not a candidate for synthesised ArcOK.


Would you mind expanding how to achieve that, ie where would the time delay be put and how do I change it as ArkOK.


Plasmac Mode 1 allows you attach an ArcOK signal (plasmac.arc_ok_in) so change modes and use the timedelay component with the in pin coming from the Torch On signal. (plasmac:torch-on) I'll let Phill confirm I have the right pins. Connect the timedelay.out pin to the ArcOK input.

I initially thought of using some sort of latch component but there did not seem to be one available in hal.
Last edit: 6 years 7 months ago by rodw.
The following user(s) said Thank You: Clive S

Please Log in or Create an account to join the conversation.

More
6 years 7 months ago - 6 years 7 months ago #160548 by Clive S

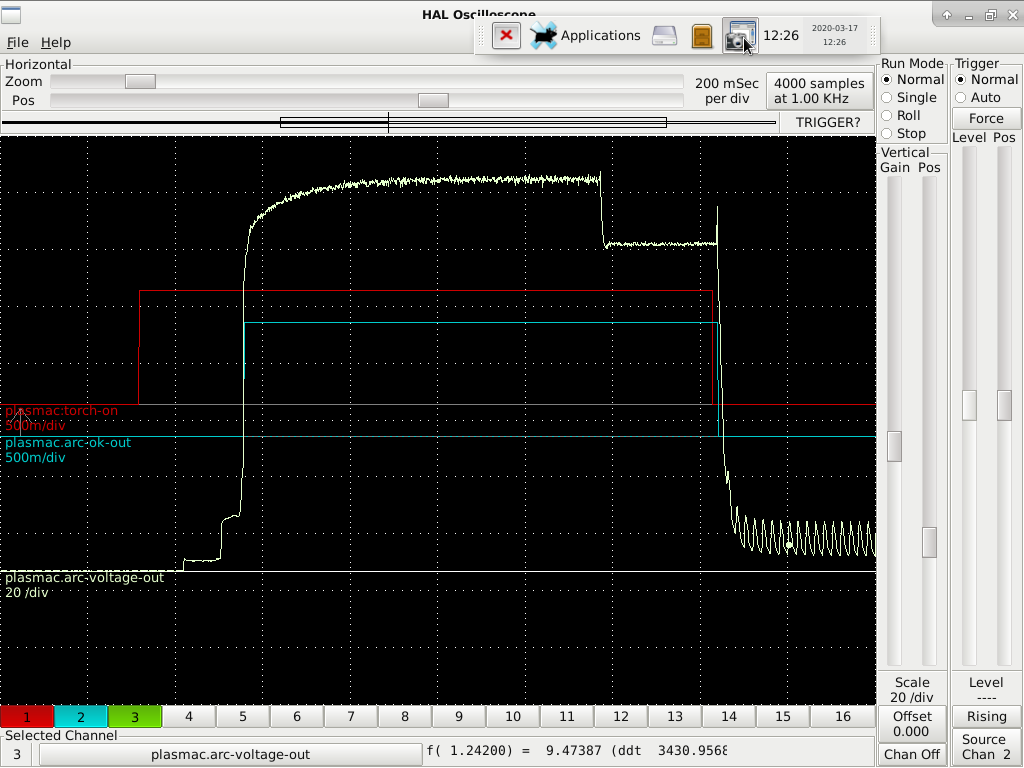
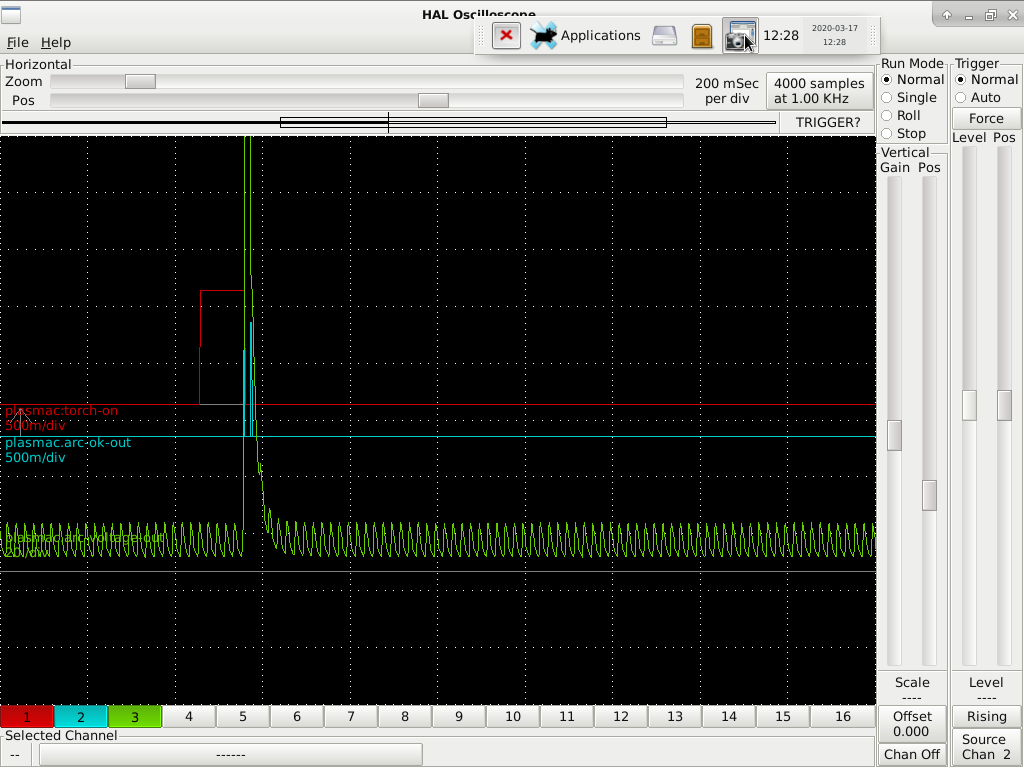
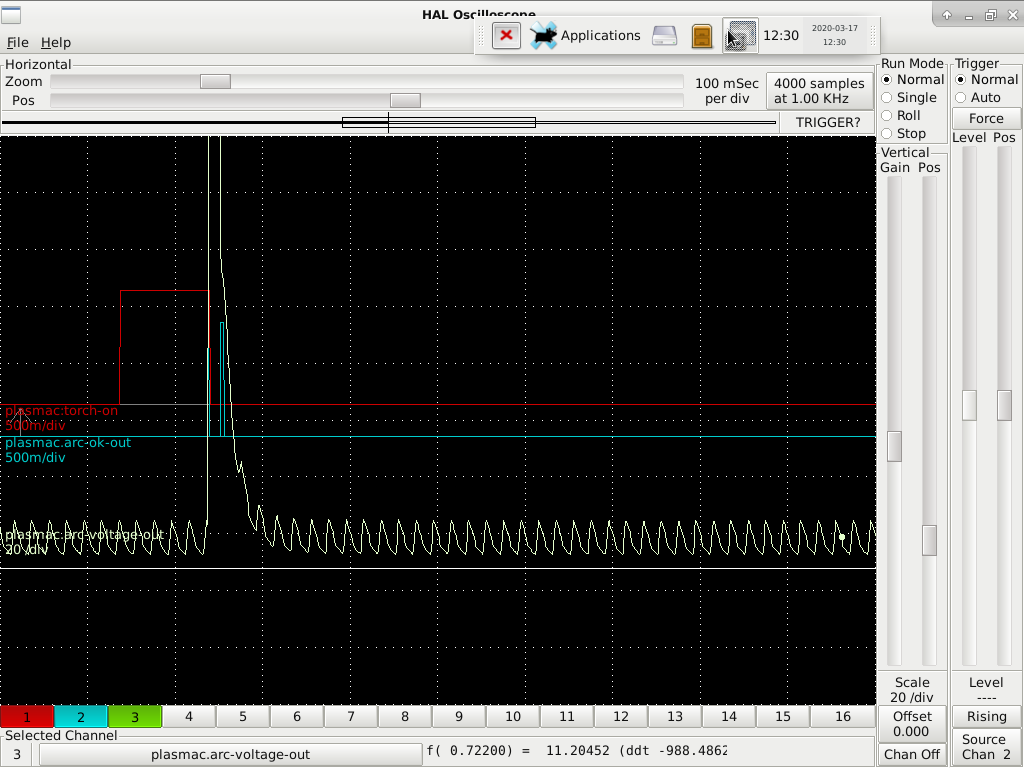
It would probably be worthwhile running Halscope on these pins plasmac:torch-on plasmac:arc-ok-out plasmac:arc-voltage-out

What is your Arc OK High set at?

ArcOK high is set at 200

screen shots. The top one is the first cut that works fine the next two are fails ie. arc fail


The above are at the 200 mSec per div scale and the below at at 100 mSec per div
Last edit: 6 years 7 months ago by Clive S.

Please Log in or Create an account to join the conversation.

More
6 years 7 months ago #160584 by rodw
Replied by rodw on topic PlasmaC torch starting problem
Clive, there is something wrong here with that sawtooth. that is oscillating in sympathy with with your 50 Hz mains power.
There is a noise issue in your system. I feel your pain.

From memory you have a 7i96,

Have you got an EMI Filter on the mains power? If you have not got an IEC connector you can get hard wired ones.

Is your plasma cutter earthed separate to your mains inlet to power?

Is your table grounded.

Have you got a central ground point with seperate wires back to every motor on your system that bridges all your linear rails? This also needs to be extended to your floating head etc. Hypertherm have a good document on this

BUt the most effective for me was the EMI filter.

Please Log in or Create an account to join the conversation.

More
6 years 7 months ago #160598 by Clive S

rodw wrote: Clive, there is something wrong here with that sawtooth. that is oscillating in sympathy with with your 50 Hz mains power.
There is a noise issue in your system. I feel your pain.

From memory you have a 7i96,

Have you got an EMI Filter on the mains power? If you have not got an IEC connector you can get hard wired ones.

Is your plasma cutter earthed separate to your mains inlet to power?

Is your table grounded.

Have you got a central ground point with seperate wires back to every motor on your system that bridges all your linear rails? This also needs to be extended to your floating head etc. Hypertherm have a good document on this

BUt the most effective for me was the EMI filter.


Rod.. Many thanks for the comments.
Re the above. I have built more that 12 machines and I think I understand the importance of grounding which you are correct to point out.
Yes I have a 7i96 and yes I have a hard wired 10A EMI filter

The actual plasma cuter does not have a separate ground (earth) connection so am relying on the 3 pin plug. I also have tried powering the plasma from another socket. I will also bond the case to the machine frame to see if that make a difference .

I have bonded the Z,X and Y axis to my star ground including all the stepper shields.

If you look on the first halscope there is no 50 HZ showing at the start of the trace and only comes in after the cut.
But on the failed cut it starts with the 50HZ.

I did not check to see the the 50HZ stopped when the air stopped purging. I will though in the morning.

control box photos.app.goo.gl/4Bfb1wv8APv84wAV6

Please Log in or Create an account to join the conversation.

More
6 years 7 months ago #160600 by phillc54
Wow, that is a mean spike you get 100mS after torch on for the second cut.

I can see that it gives an Arc OK then shoots past Arc OK High so turns Arc OK off and you lose the Torch On signal.

It is interesting that it doesn't occur on the first cut nor does the 20 odd V sawtooth pattern appear before the first cut.

So there a maybe a few different ways around this.
  1. install a current sensor in the torch lead and use that for an Arc OK signal
  2. I could add a Arc OK on delay so the arc voltage needs to be within limits for nnn amount of time before Arc OK is true
  3. I could add a Arc OK off delay so the arc voltage needs to be outside limits for nnn amount of time before Arc OK is false
  4. I could add a Arc OK High inhibit so Arc OK won't go false if the arc voltage is too high
The following user(s) said Thank You: Clive S

Please Log in or Create an account to join the conversation.

More
6 years 7 months ago #160602 by PCW
Replied by PCW on topic PlasmaC torch starting problem
Looks like the arc voltage may exceed your arc-ok high threshold
can you change the scaling and post it again?

Please Log in or Create an account to join the conversation.

Moderators: snowgoer540
Time to create page: 0.469 seconds
Powered by Kunena Forum