PlasmaC torch starting problem (Solved with help from the famous three)

More
6 years 7 months ago #160805 by rodw
Replied by rodw on topic PlasmaC torch starting problem
Jim Colt says:

A plasma torch with a pilot arc will fire a low power plasma arc in the air....this is a DC arc that goes from the torch electrode to the torch nozzle...and the force of the air blows the arc out through the nozzle (tip) orifice. The function? The pilot arc is designed to improve the ability of the plasma arc to transfer to the materials that needs to be cut......as the pilot arc approaches the plate, it burns through any surface issues (paint, rust, masking materials) and quickly transfers the arc....which electronically senses that current is now flowing through the work ground cable...and amperage ramps up (you will see the arc get more intense.

Older technology plasmas, and todays industrial mechanized plasma systems....use a pilot arc that is started with a high voltage, high frequency discharge between the nozzle and electrode to get the cutting air ionized. Newer technology air plasma systems use a "blowback start" ( a moving, spring loaded electrode in the torch) to ionize air, and are able to start a pilot arc without the use of high frequency.

www.pirate4x4.com/forum/shop-tools/95508...new-plasma-user.html

I would look at your pierce height. Its possible with the air flowing the arc does not have sufficient force to transfer to the material. Its clear that there is no current sensed through the work ground cable. Was your plasma designed to accpet a pilot arc torch? IS the new torch compatible?

Looks like you could implement ohmic sensing with the right shield cup BTW.
Other than that, I think you are out of options
The following user(s) said Thank You: Clive S

Please Log in or Create an account to join the conversation.

More
6 years 7 months ago #160807 by rodw
Replied by rodw on topic PlasmaC torch starting problem
At a guess, the sawtooth pattern could be as a result of the HF start lingering on.

Please Log in or Create an account to join the conversation.

More
6 years 7 months ago #160810 by phillc54
Clive, your machine may be a good candidate for something along these lines for Arc OK

Please Log in or Create an account to join the conversation.

More
6 years 7 months ago #160819 by tommylight
Clive, i am sorry for the mess we have created for you, and also sorry for having to ask you this, but several posts back i asked you to check the torch distance from the material after the first and the second probe, now Rod has mentioned the same thing, so please do check that.
Now on these plots it is clearly visible what is going on, and i have to agree with Phill's conclusion that PlasmaC is working properly and doing everything it should do.
So to recap:
-Please do not lower the low voltage threshold ever again, it did cause us some head scratching, and some stray answers .....,
-PlasmaC is configured and working correctly,
-Wiring is all good,
-The noise is present while the inverter power stage is on, so nothing to worry about, most probably,
-Please oh please lower the pierce height and the cut height ! :) :) :)
Pierce at 2mm and cut to 1mm, test and report back
P.S.
If you can find a reed relay, you can get the arcok signal that never fails and gives no false starts ever, but you do have to remove one of the thick cables on the plasma and replace it with a longer one, with 3 turns made out of it and the reed relay located inside those turns. Use a piece of old pen or similar to prevent the reed relay from braking, they usually are made out of thin glass.
The following user(s) said Thank You: Clive S

Please Log in or Create an account to join the conversation.

More
6 years 7 months ago #160833 by islander261
I may be missing something here. It seems to me that the PlasmaC generated Ark Ok signal should only be true when the plasmac torch on signal is true. I actually can't think of any case when this wouldn't be true. So may be the solution is the plasmac arc ok test AND plasmac torch on to set the plasmac generate arc ok signal.

I must admit that I have only ever used a CNC enabled plasma power supply that generated it's own OK to Move (arc ok ) signal.

John
The following user(s) said Thank You: Clive S

Please Log in or Create an account to join the conversation.

More
6 years 7 months ago #160846 by Clive S

phillc54 wrote:

which signal should I change to 1ms or 5ms or are you asking for the Hoz display set from 200ms to 5ms
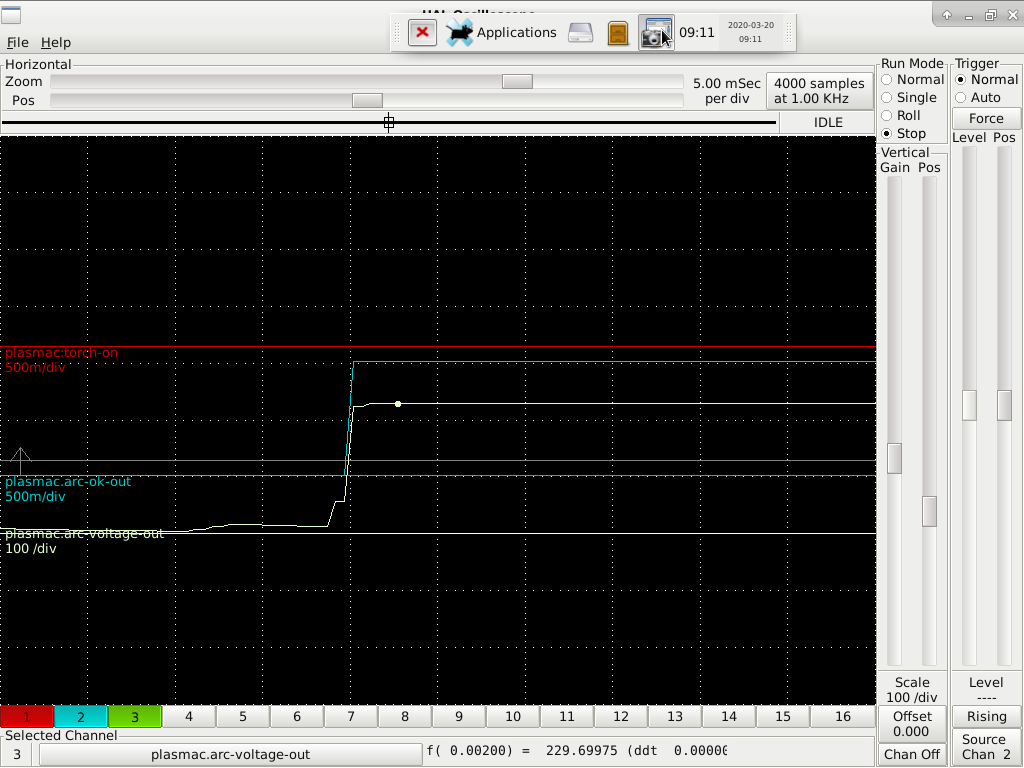
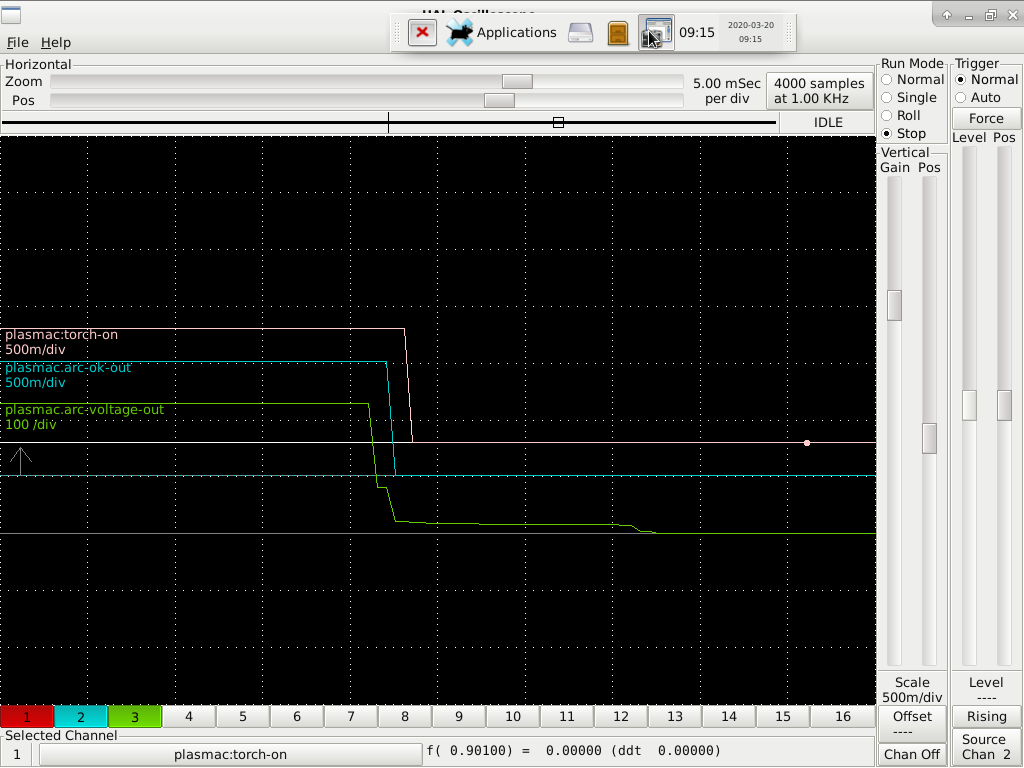
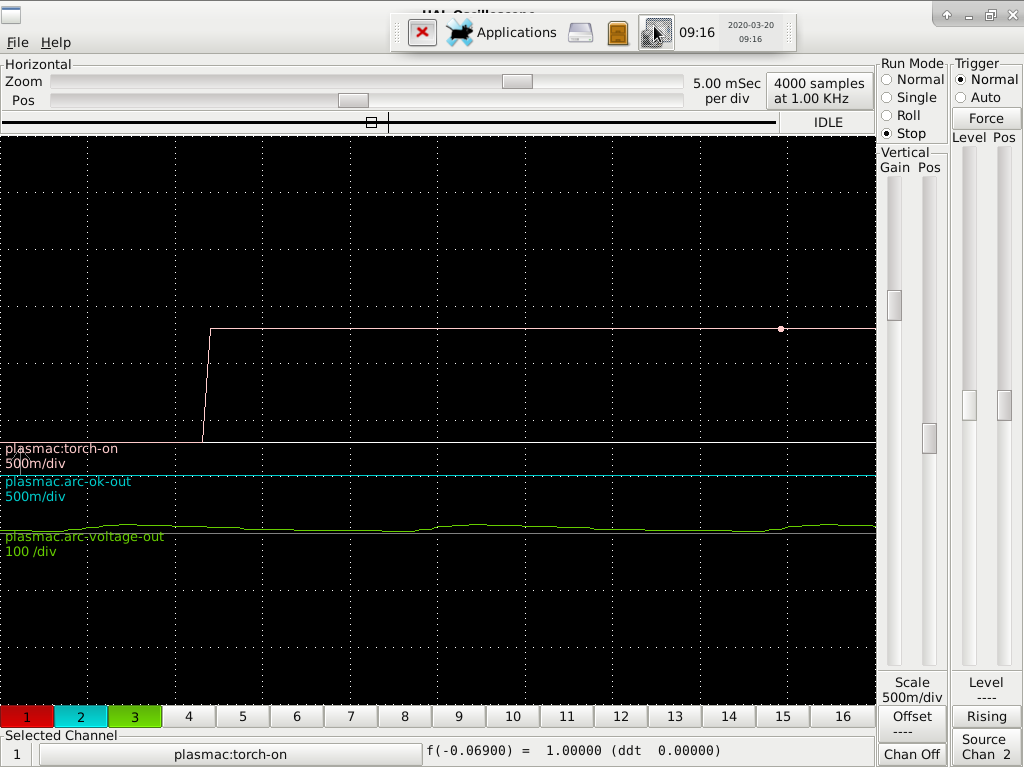
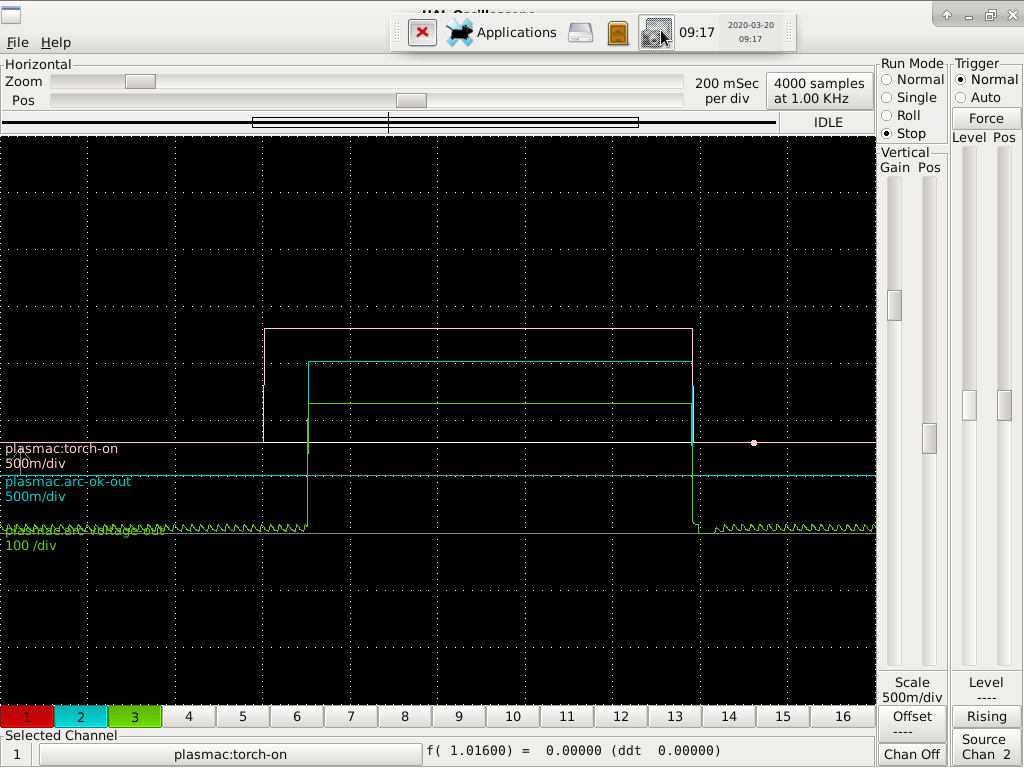
Yes, the horizontal thanks Clive so I can better see the timing of those signals.

.
fail 5ms
.
End trace 5ms

.
start trace 5ms

.
full trace 200ms

Please Log in or Create an account to join the conversation.

Moderators: snowgoer540
Time to create page: 0.186 seconds
Powered by Kunena Forum