
- Posts: 2203
- Thank you received: 486

Clive S wrote: Yes I will do it again in the morning all the others were set at about 80 this one was at 10V.
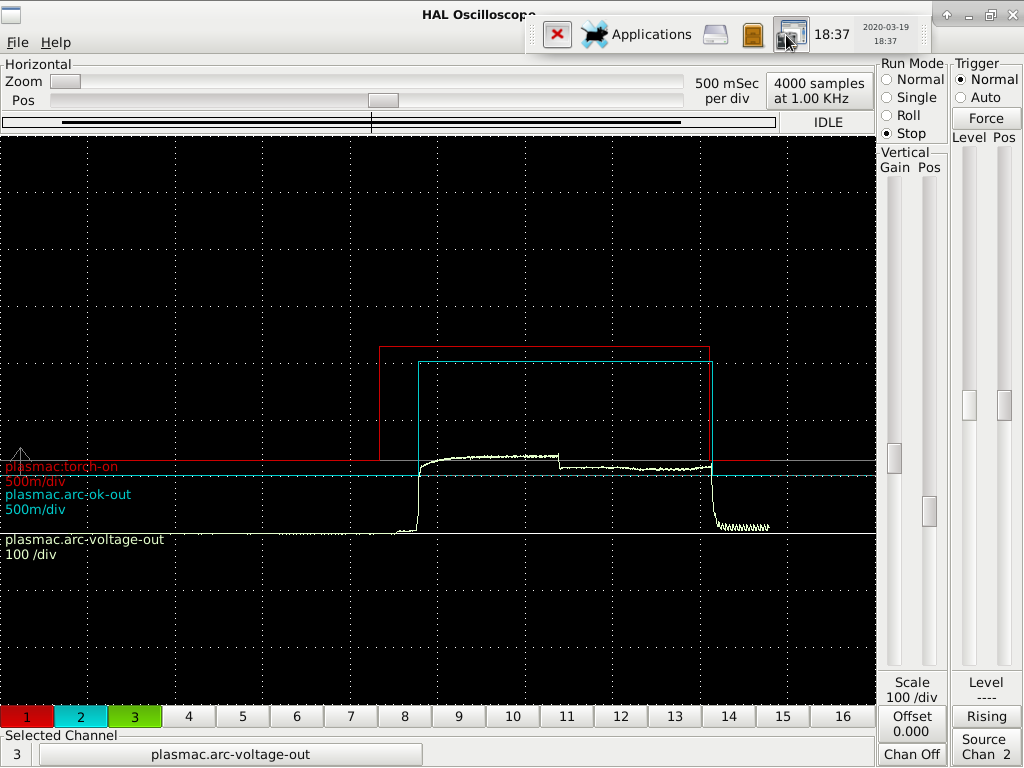
the arc-ok wave is only 1 V and the arc-volt ripple looks like 20V
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
Rod. I don't think I have a blowback style of torch it is a pilot arc type I believe the blowback type has moving parts inside mine does not.My guess is that on arc establishment of subsequent cuts (with air flowing) is that the blowback mechanism in the torch is shorted together (eg in arc starting mode). Remember that a blow back style torch creates the initial arc inside the torch with a dead short and then transfers it to the material. So the transfer of the arc does not occur for some reason.
I think the only thing you can do is service the torch and replace every consumable becasue by now are probably in a sad state.
If that does not work, it is how this particular machine is.
Please Log in or Create an account to join the conversation.
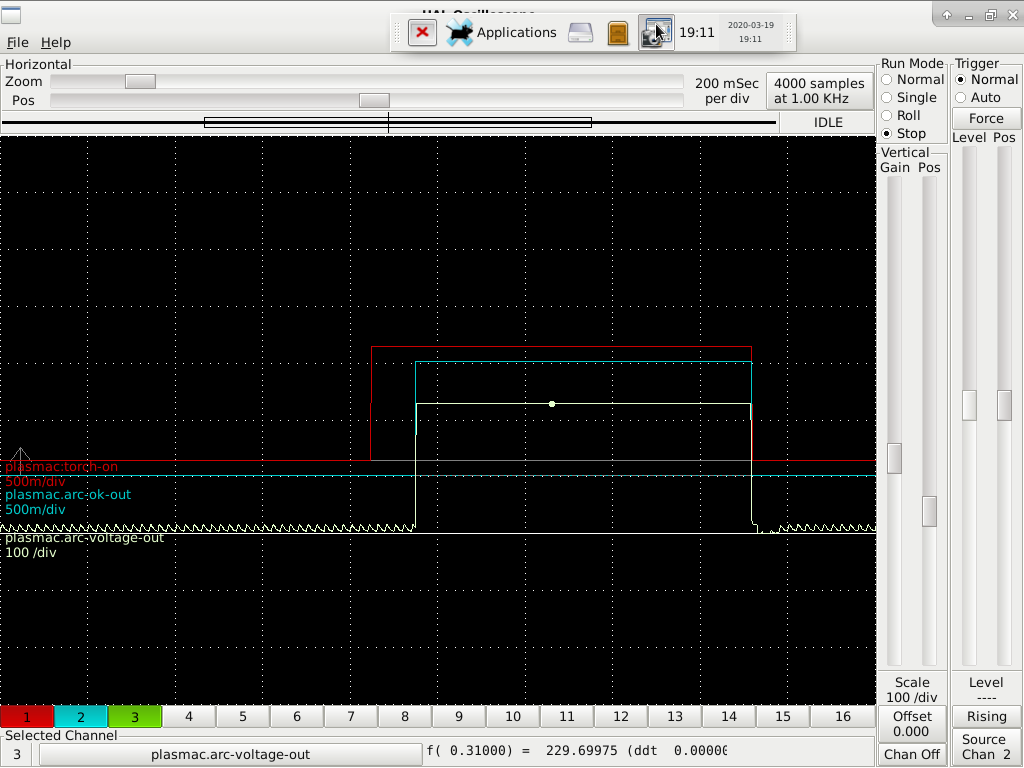
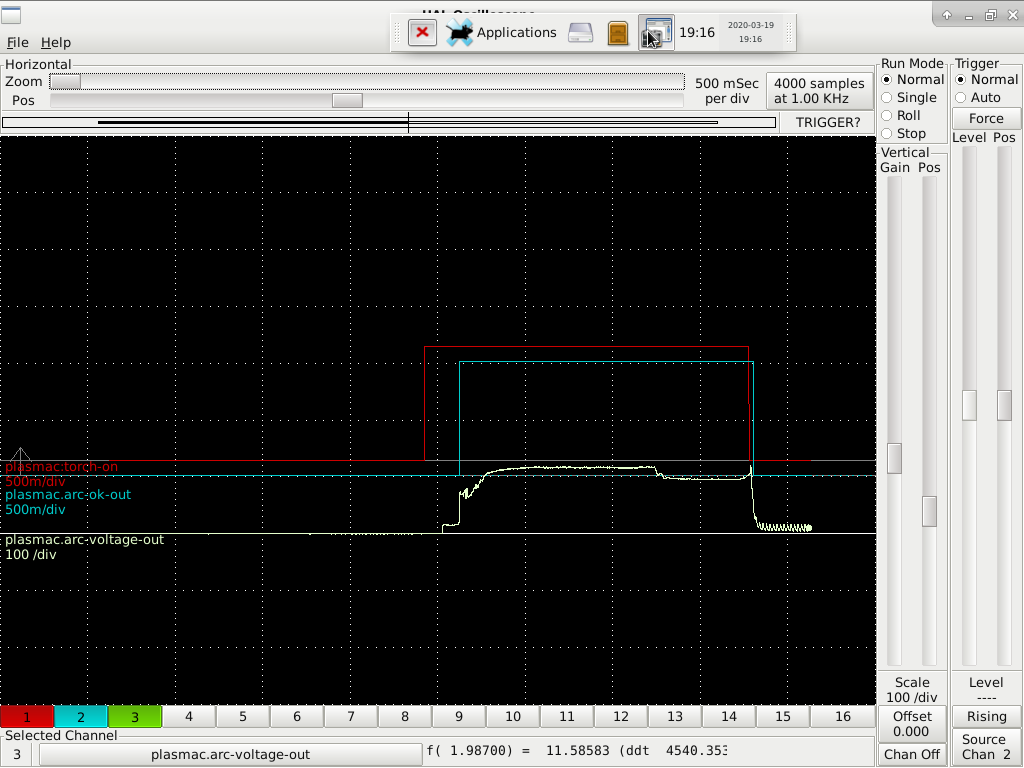
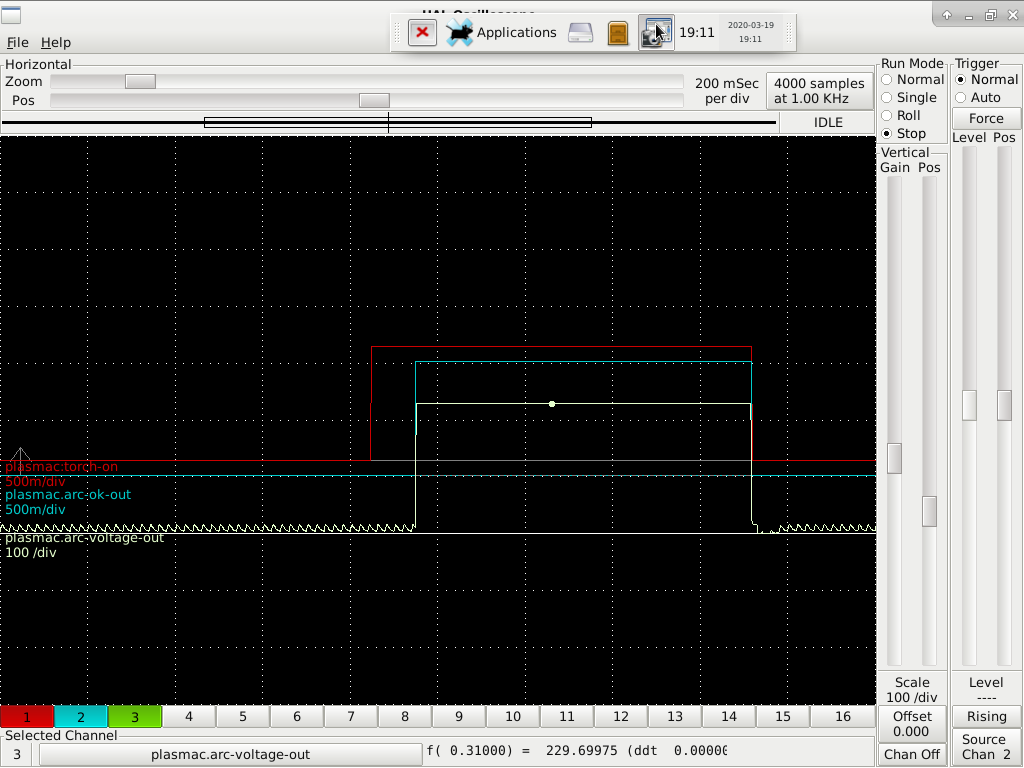
phillc54 wrote: From all these plots it seems to me that PlasmaC is doing what it should do.
My take is that the fails are reading the pilot arc and not the cutting arc.
It is interesting that the first cut is always good and the waveforms do show that.
From the plot below it looks to me like the voltage drops off before the arc ok and the torch on which would be correct behaviour on PlasmaC's part but it would be nice to confirm that with say a 1ms or 5ms division.
Warning: Spoiler!
Please Log in or Create an account to join the conversation.
Yes, the horizontal thanks Clive so I can better see the timing of those signals.which signal should I change to 1ms or 5ms or are you asking for the Hoz display set from 200ms to 5ms
Please Log in or Create an account to join the conversation.